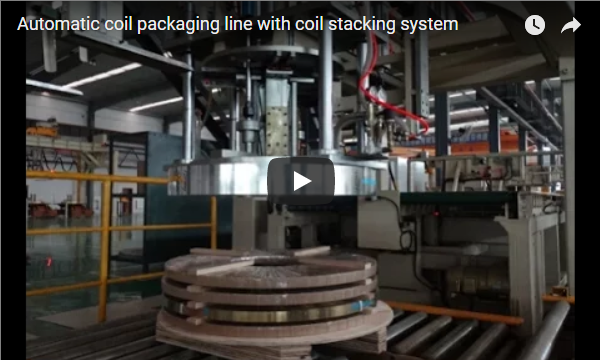
Samenvatting An automatic copper strip coil packing line moves each coil from the slitter to a wrapped, labelled pallet with almost no manual lifting. In our clip, about 48 s long, a copper coil lying flat runs on a yellow roller conveyor, is wrapped in clear film, travels on a pallet, gets its label and leaves by forklift. The line is built for coils of 80 to 5,000 kg, 750 to 1,400 mm OD and 17 to 400 mm width.
Inhoudsopgave
- Wat de video laat zien, in de juiste volgorde.
- Stations of a copper strip coil packing line
- Lijnspecificaties
- Takt-controle
- Selectiechecklist voor een verpakkingslijn voor koperen stripspoelen
- Bediening en veiligheid
- Veelgestelde vragen over techniek
- Volgende stap
- Gerelateerd lezen
- Bronnen
Wat de video laat zien, in de juiste volgorde.
The line combines yellow roller conveyors, a white and yellow handling frame with an overhead gantry, a wrapping station behind a yellow guard and a long white roller conveyor for pallets. A white control desk with two displays, a keypad, red and green buttons and a red emergency stop stands beside the conveyor.
- 0 tot ongeveer 4 seconden. A reddish-brown copper strip coil, lying flat with its eye up, is transferred onto the yellow roller conveyor.
- Ongeveer 4 tot 8 seconden. A worker in an orange hard hat and yellow vest stands at the control desk while the coil moves on toward the next station.
- Ongeveer 8 tot 16 seconden. At the wrapping station, behind the yellow guard, the coil is wrapped in clear film until it is fully covered.
- Ongeveer 16 tot 32 seconden. The wrapped coil, now on a pallet, travels along the long conveyor under the overhead gantry.
- Ongeveer 32 tot 36 seconden. At the end of the line the worker adjusts the wrapped coil on its pallet by hand.
- Ongeveer 36 tot 40 seconden. A label printer at the control desk prints the coil label.
- Ongeveer 40 tot 48 seconden. A forklift picks the wrapped pallet off the conveyor and takes it to storage.
Stations of a copper strip coil packing line
A copper strip coil comes off the slitter with its eye horizontal on the turnstile. The line turns it, straps it, wraps it, stacks it and reports the data back to production.
| Station on our line | Wat het doet |
|---|---|
| Coil turnstile (cross arm) | Takes coils off the slitter; 10 t per arm, 40 t total, 1,500 mm arm |
| Coil down-ender | Lifts and flips the coil eye-up; 20 to 30 s per cycle, handles widths from 15 mm |
| PET-omsnoeringsmachine | Straps through the eye, 3, 4 or 6 straps; about 15 s per cycle |
| Machine voor het wikkelen van geweven banden | Wraps the coil in PP woven sheet |
| Stapelaar met draaiplateau | Six stations; stacks to 1,000 mm high and 6,000 kg per pallet |
| Industrial PC control | Takes data from the slitting line or barcode reader, prints labels, shares packing data |
The clip shows the conveying, wrapping, pallet transfer, labelling and forklift pick-up part of that chain. Clear film, as in the clip, or PP woven sheet is chosen per customer and per storage time.
Lijnspecificaties
| Weeg-, verpakkings- en stapellijn voor koperen striprollen | Specificaties |
|---|---|
| Coil weight, handling and packing | 80 tot 5,000 kg |
| Buitendiameter spoel | 750 1,400 tot mm |
| Coil binnendiameter | 508 mm |
| Coil breedte | 17 400 tot mm |
| strapping | PET, 0.80 mm thick, 16 mm wide, 3, 4 or 6 straps |
| Woven wrap material | Kern van 55 mm, buitendiameter van 100 tot 450 mm, breedte van 90 tot 100 mm |
| Stapelen | 1,000 mm high with pallet, 6,000 kg per pallet, 4,000 kg per coil on the stacker |
| Power | 380 V, 50 Hz |
Takt-controle
For an illustrative target of 40 coils per hour, the takt is 3,600 ÷ 40 = 90 s per coil.
The down-ender needs 20 to 30 s and the strapping machine about 15 s per cycle, so both fit well inside 90 s. The strapping figure is the page value for one cycle. With 6 straps on a wide coil, we check the strapping time at your strap count, and add a second strapping head or a buffer if it runs close to the takt. Wrapping time depends on the coil width and the overlap, and we check it per coil range in the proposal.
Selectiechecklist voor een verpakkingslijn voor koperen stripspoelen
- Coil weight, OD, ID and width range from the slitter.
- Productie per uur, afgestemd op de cyclus van de snijmachine.
- Strap count, strap material and wrap material: clear film or PP woven.
- Stacking height and weight per pallet.
- Data link: slitting line, barcode reader, label content and the plant system.
- Forklift or conveyor take-off at the end of the line.
Bediening en veiligheid
On the clip the wrapping station sits behind a yellow guard, and the control desk carries a red emergency stop. At about 32 to 36 s the worker adjusts the wrapped coil on its pallet by hand at the end of the conveyor. A hand on a load that can still move is the move to design out. Adjustments on the pallet happen only with the conveyor stopped.
Stop, isolate and lock out the station before anyone reaches into the wrapping guard, clears a film break or works on the down-ender or stacker. The forklift pick-up zone at the end of the line is kept clear of people on foot while the forklift moves.
De geldende normen zijn afhankelijk van de bestemmingsmarkt. Voor CE-markten beschrijft ISO 12100 de risicobeoordelingsmethode en EN 415-10 de algemene eisen voor verpakkingsmachines, waaronder de beveiliging en de stopinrichting.
Veelgestelde vragen over techniek
Q: Which coils does the copper strip coil packing line take? A: Coils of 80 to 5,000 kg, 750 to 1,400 mm OD, 508 mm ID and 17 to 400 mm width.
Q: How many straps does the line apply? A: The PET strapping machine straps through the eye with 3, 4 or 6 straps, at about 15 s per cycle.
Q: How high can the line stack coils? A: Up to 1,000 mm including the pallet and 6,000 kg per pallet. The stacker takes single coils up to 4,000 kg, below the 5,000 kg handling limit.
Volgende stap
We dimensioneren een verpakkingslijn voor koperen stripspoelen in drie stappen:
- Dien uw lay-outtekening in. met de snijmachine-uitgang, spoelbereik, uitvoerdoel en stapelpatroon, om info@fhopepack.com.
- Ontvang binnen 48 uur een offerte., with the station list and the takt check per station.
- Plan een locatiebezoek so we confirm the floor space, the forklift route and the data link.
Gerelateerd lezen
- Weeg-, verpakkings- en stapellijn voor koperen striprollen
- Snijrol verpakkingslijn
- Rolverpakkingsmachines
- Spoelwikkelmachine met tape- en labelprinter
Bronnen
- Line specifications and stations: copper strip coil weighing, packing and stacking line product page
- Clip timing: scene timings taken from our clip, in steps of about 4 s
- Lijn in actie: onze video op YouTube
- Toepassingsgebied van de normen: ISO 12100:2010, EN 415-10: 2014
Laatst beoordeeld: 05-10-2026