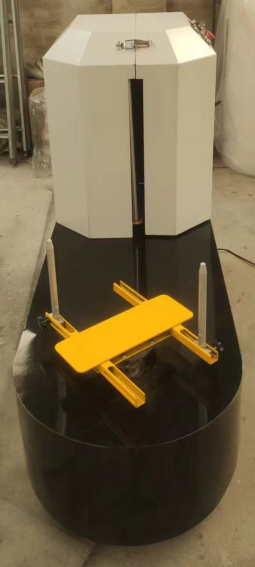
Santrauka Packaging engineers managing building wire, magnet cable, and conduit production lines face a structural trade-off between packaging speed, bundle containment, and material consumption. The FPCA horizontal eye-to-sky orbital wrapping series addresses this through dedicated rotating rings that feed packaging material directly through the coil eye while driven conical polyurethane rollers rotate the coil around its vertical axis. This guide provides exact engineering envelopes, physical overlap calculations, kinematic throughput figures, and utility requirements for the FPCA-200 and FPCA-300 lines, enabling procurement and plant engineering teams to validate equipment fit within 48 hours.
Turinys
- Kaip veikia ritės vyniojimo ciklas
- FPCA-200 and FPCA-300 model ranges
- Persidengimas ties OD ir ID – kodėl svarbu nustatyti ties OD
- Apvyniojimo laikas vienai ritei
- Plėvelės ir pakavimo medžiagos
- Controls and automation architecture
- Safety and regulatory standards
- Inžinerinės atrankos kontrolinis sąrašas
- Inžinerijos DUK
- Kitas žingsnis
- Susijęs skaitymas
- Šaltiniai
Kaip veikia ritės vyniojimo ciklas
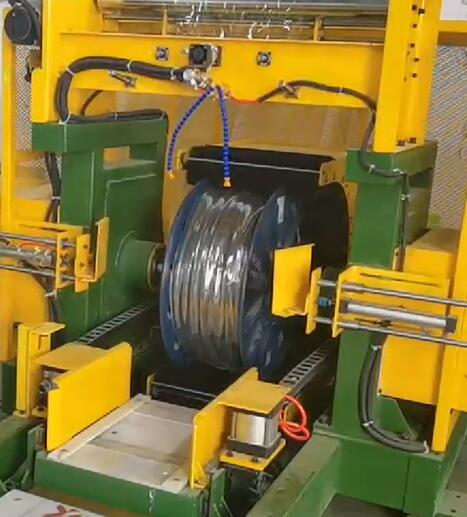
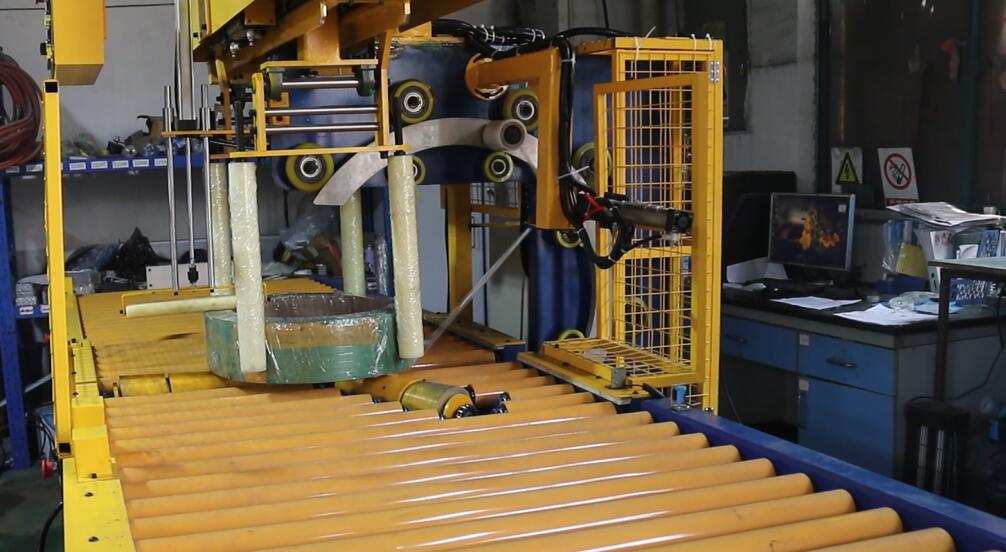
The FPCA series wraps coils placed horizontally in an “eye-to-sky” orientation. The orbital ring rotates on a vertical plane, carrying a material shuttle through the open core of the coil, while motorized conical rollers index the coil about its central vertical axis:
- Load and centre: the coil goes onto the coated conical rollers and guide rollers bring the section under the ring plane.
- Clamp and wrap: a top pneumatic press-down cylinder descends on the coil face to stop hop and layer displacement while the ring accelerates under VFD and feeds film through the eye, the rollers turning the coil in step.
- Cut and tuck: on semi-automatic units the operator cuts the web with a shielded blade holder; with the cut-and-clamp option a gripper catches the tail, severs it and smooths it onto the circumference.
- biudžeto įvykdymo patvirtinimas: the press cylinder retracts to its home limit so the coil can be taken off.
FPCA-200 and FPCA-300 model ranges
Machine frame selection depends strictly on the coil physical envelope, gross weight, and required material layer properties.
| Inžinerinis parametras | FPCA-200 | FPCA-300 |
|---|---|---|
| Ritės vidinis skersmuo (ID) | 150 – 400 mm | 250 – 510 mm |
| Ritės išorinis skersmuo (OD) | 250 – 500 mm | 400 – 900 mm |
| Ritės plotis / aukštis | 80 – 200 mm | 60 – 300 mm |
| Allowable Coil Weight | 2-50 kg | 20-200 kg |
| Įdiegta pavaros galia | 2.0 kW | 2.4 kW |
| Standard Electrical Service | AC 380V, 50 Hz (3-Phase) | AC 380V, 60 Hz (3-Phase) |
| Žiedo sukimosi greitis | 10–120 aps./min | 10–90 aps./min |
| Ciklo laikas vienai ritei | 20–30 s/ritė | 20–38 s/ritė |
| Calibrated Overlap Range | 20–80% (OD) | 10–90% (OD) |
| Suderinamos pakavimo medžiagos | PE, Stretch Film, PVC | LLDPE, PVC, PE Film, Crepe Paper |
Note: For plants requiring automated inline handling, the FPCW series (FPCW-200, FPCW-300, and FPCW-400) integrates upstream coiling systems with dedicated easy-loading mechanisms. Parameters for 400-class rings and non-standard line voltages (e.g., 208V, 480V) are confirmed on a project-specific basis.
Persidengimas ties OD ir ID – kodėl svarbu nustatyti ties OD
On a toroidal coil the ring advances the same axial distance per revolution, but surface travel grows with radius: the outer circumference is π × OD, the eye is π × ID. So the layer count accumulates by the ratio OD/ID.
Pavyzdys: ID 200 mm, OD 400 mm on an FPCA-200 gives a ratio of 2.0. With a 100 mm web at 50% outer overlap, the advance per revolution is 50 mm, giving two layers at the OD — and 2 × 2.0 = 4 layers at the eye, which is about 75% local overlap there.
That asymmetry is why overlap is set at the outer diameter. Calibrating to the eye instead starves the OD and leaves the weak points and moisture paths where the coil takes its handling loads. The PLC therefore works in OD advance rates: 20–80% on the FPCA-200, 10–90% on the FPCA-300.
Apvyniojimo laikas vienai ritei
Cycle time is revolutions divided by ring speed, plus acceleration, deceleration and coil exchange. Revolutions come from geometry: OD circumference divided by the advance per revolution (web width × (1 − overlap)).
- FPCA-200: a 350 mm OD coil with a 100 mm web at 50% overlap advances 50 mm, so π × 350 ÷ 50 ≈ 22 revolutions. At 90 r/min that is about 14.7 s of wrapping; with loading and unloading the cycle lands in the published 20–30 s band.
- FPCA-300: a 700 mm OD coil with an 80 mm web at 60% overlap advances 32 mm, so π × 700 ÷ 32 ≈ 69 revolutions, about 59 s at 70 r/min; a 450 mm OD coil at 90 r/min wraps in roughly 16 s, inside the 20–38 s band.
These are worked examples, not guarantees — real times depend on the recipe and the operator.
Plėvelės ir pakavimo medžiagos
FPCA friction-braked shuttles adjust web release tension to run different packaging media without stretching films past yield limits or tearing non-elastic papers:
- LLDPE tempiamoji plėvelė (17–35 µm): Primary solution for commercial building wire. Provides elastic recovery, puncture resistance, and complete optical transparency for barcode scanning.
- Polivinilchlorido (PVC) plėvelė: Rigid, high-clarity wrapping with high surface gloss. Offers mechanical resistance against jagged conductor ends in building cable segments.
- Polyethylene (PE) Flat Film: Cost-effective environmental protection against dust and liquid splash during containerized transit.
- Crepe Paper Tape (FPCA-300 Exclusive Compatibility): Heavy industrial cables, bare copper coils, and subsea umbilical segments often require mechanical abrasion resistance and breathability. The 2.4 kW drive on the FPCA-300 maintains controlled torque under the higher web tensions required for crepe paper and woven synthetic tapes up to 200 kg gross coil loads.
Controls and automation architecture
The FPCA series runs on an industrial PLC platform connected to a high-contrast operator HMI:
- Dual Inverter Synchronization: The orbital ring drive and the conical roller drive are operated by dedicated inverters. Modifying the speed ratio digitally scales the OD overlap percentage without mechanical gear swaps.
- Controlled Inverter Acceleration: S-curve frequency ramp-up prevents high starting torque from slipping the polyurethane drive wheels against the cast steel ring track.
- Index Proximity Sensing: Proximity switches detect ring rotation, bringing the material shuttle to a repeatable stop position at the operator access point at cycle end.
- Receptų valdymas: Operators can save target parameters (ring r/min, roller ratio, target overlap) for common coil SKU numbers, holding product changeover times under 30 seconds.
Safety and regulatory standards
A ring turns at speed with pinch points at the rollers, so access has to be closed:
- Fechtavimas: sheet-metal and mesh enclosures keep hands out of the orbital path while the machine runs.
- Užraktai: access doors carry dual-contact switches that remove power from the ring motor when opened.
- Kojų valdymas: the cycle is started from a shrouded foot switch, keeping the operator’s hands and body outside the rotating plane.
- Bazė: construction and risk mitigation follow ISO 12100 and the EN 415-10 packaging-machinery framework, with guarding confirmed by the site risk assessment.
Inžinerinės atrankos kontrolinis sąrašas
Six parameters decide the specification:
- Išmatavimai: smallest ID, largest OD and maximum stack height across every SKU.
- Eye clearance: the minimum coil ID must clear the shuttle plus the ring width, with margin.
- Svoris: 50 kg on the FPCA-200, 200 kg on the FPCA-300.
- Film or paper: LLDPE, PVC, PE or crepe paper — it sets the shuttle tension brake design.
- Pralaidumas: coils per hour, which decides between semi-automatic cutting and the fully automatic FPCW inline machines.
- Komunalinės paslaugos: voltage, 50 or 60 Hz, and air at 0.5–0.7 MPa.
Inžinerijos DUK
Q: Can an FPCA-200 take a 220 mm ID, 480 mm OD, 45 kg coil? A: Yes — ID, OD and weight are all inside the FPCA-200 window of 150–400 mm ID, 250–500 mm OD and 50 kg.
Q: When do you move up to the FPCA-300? A: When OD passes 500 mm (up to 900 mm), weight passes 50 kg (up to 200 kg), ID passes 400 mm, or when crepe paper is the wrap and the 2.4 kW drive is wanted.
Q: Why does film pile up in the eye? A: Because layer count scales with OD/ID. The same passes cross the eye as the outer perimeter, so a high-ratio coil reaches 70–90% overlap at the eye when the OD is set to 20–50%.
Q: Do coils need strapping before wrapping? A: Not when they come off a tight modern take-up winder — the press roller holds the turns while the first film layers build containment.
Q: How is overlap adjusted? A: On the HMI, by the speed ratio between the roller inverter and the ring drive — no belt or sprocket change.
Kitas žingsnis
- Pateikite produkto duomenis: Send minimum/maximum coil dimensions (ID, OD, width, weight), target throughput, and line power requirements to info@fhopepack.com.
- Review Layout Drawing & Proposal (24–48 Hours): Our applications team will return a machine layout drawing, calculated cycle times, shuttle clearance verification, and electrical schematics.
- Gamyklinis bandymas: Send sample wire coils to our manufacturing facility for wrap tightness verification, material consumption testing, and Factory Acceptance Testing (FAT).
Susijęs skaitymas
- Kabelių pakavimo mašinų sprendimų apžvalga
- FPCA-200 pusiau automatinis kabelių ričių vyniojimo aparatas
- FPCA-300 sunkiųjų ritinių pakavimo sistema
- Automatinė vyniojimo ir vyniojimo gamybos linija
- Žarnų ir plastikinių vamzdžių orbitinio vyniojimo įranga
Šaltiniai
- Tarptautinė standartizacijos organizacija: ISO 12100:2010 Mašinų sauga
- Europos standartizacijos komitetas: EN 415-10:2014 Pakavimo mašinų sauga
- FHOPEPACK Technical Manual: FPCA Series Operational Guidelines
Paskutinį kartą peržiūrėta: 2026-11-05