Executive summary
A packing line for steel cable and wire coil is chosen in three decisions: how the coil is made and strapped, how it is covered, and how it is stacked. We answer each with a module: a coiler with PP strapping, a shrink or stretch-wrap station, and robot or gantry stacking. Our cable coiling machines make coils of 240–460 mm OD at 2–2.5 coils per minute. A worked example sizes a line for 2 coils per minute.
Inhaltsverzeichnis
- Three decisions when configuring a cable coil packing line
- Robot stacking line: configuration and sequence
- Decision 1: coiling and strapping
- Decision 2: shrink or stretch wrap
- Decision 3: robot or gantry stacking
- Worked example: a 2 coil/min line
- Auswahlliste: Was Sie uns senden sollten
- Sicherheit: EN 415-10 und ISO 12100
- Häufig gestellte Fragen zur Technik
- Nächster Schritt
- Verwandte lesen
- Quellen
Three decisions when configuring a cable coil packing line
When a cable or wire maker asks us for a packing line, we offer it in three parts and ask two questions before we quote. Which covering does the market want, shrink film or stretch wrap? And how should the coils be stacked: what pallet size, what pattern, how high?
| Entscheidung | Unsere Möglichkeiten |
|---|---|
| 1. Make and secure the coil | automatic coiling with PP strapping |
| 2. Cover the coil | shrink film, or stretch-film wrapping |
| 3. Stack the coils | six-axis robot, or gantry stacker |
Robot stacking line: configuration and sequence
This is a robot stacking line. A coil, strapped with white PP bands, sits on a platform with red rubber pads. A U-shaped clamp comes down from above, grips it and carries it to the next station. There the coil is set on a turntable and covered with clear film. At the end, a six-axis robot picks each finished coil and places it on a wooden pallet inside a fenced cell.
Decision 1: coiling and strapping
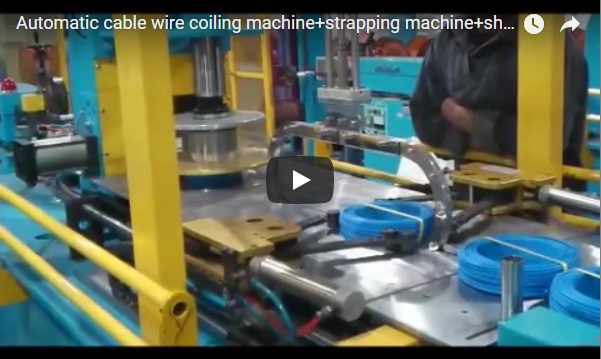
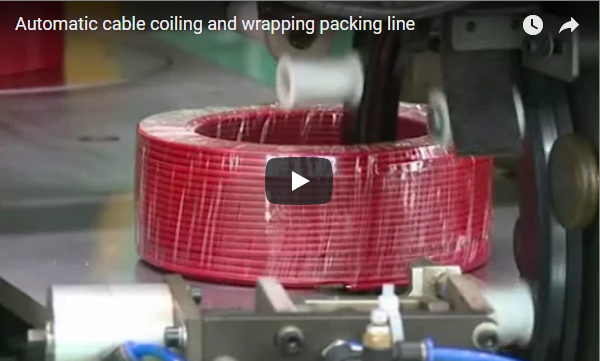
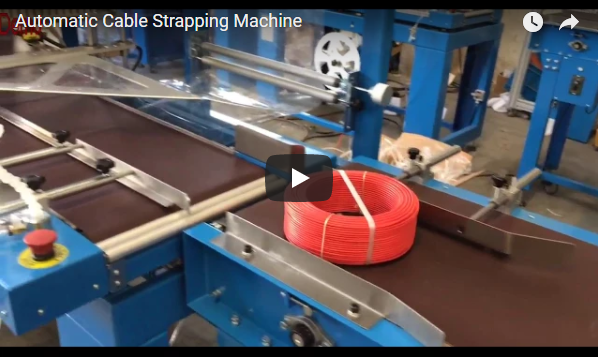
The coiler counts the length, winds the coil and cuts the cable, controlled by PLC and HMI. Strapping then ties the coil so it keeps its shape for covering and stacking.
| Artikel | Automatische Kabelwickelmaschine | Cable winding and strapping with stacking |
|---|---|---|
| Spule ID | 140 – 200 mm | 135 – 220 mm |
| Spule OD | 240 – 460 mm | 180 – 400 mm |
| Spulenhöhe | 60 – 100 mm | 80 – 130 mm |
| Coilgewicht | max. 50 kg | pro Projekt |
| Kabeldurchmesser | 3 – 15 mm | 1.5 – 6 mm |
| Schnelligkeit | 2–2.5 Spulen/min | up to 2 coils/min |
| Zählerzähler | 0.01–100 | 0.01–200 |
| Air / power | 6 bar; AC 380 V, 50 Hz, 3 phase | 6 bar; AC 380 V, 50 Hz, 3 phase |
The line runs online behind the extruder or offline from a payoff.
Decision 2: shrink or stretch wrap
Schrumpffolie puts a sleeve around the coil and shrinks it tight in a tunnel. It gives a closed, neat pack that shows the coil and label.
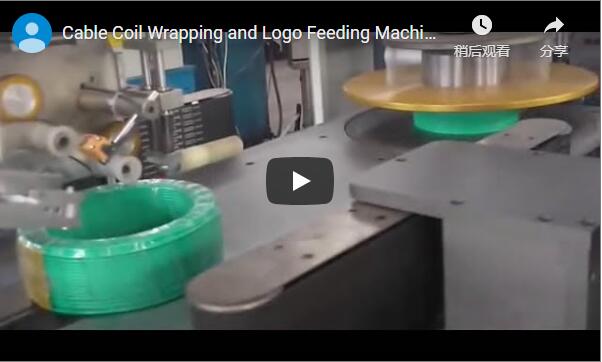
Stretchwickel runs film through the eye of the coil and around it. It needs no heat and handles larger coils. An optional device inserts the label under the film automatically.
Decision 3: robot or gantry stacking
A sechsachsiger Roboter picks coils from the end of the line and builds the pallet pattern you choose. One robot cell can change pattern by program.
A Portalstapler runs on a frame over the pallets. It suits long, straight lines and heavier coils.
With coiling, covering and stacking automated, one operator can monitor 4–6 lines.
Worked example: a 2 coil/min line
Illustrative case: cable leaves the extruder at 200 m/min and is packed in 100 m coils of 400 mm OD, 120 mm high, 20 kg each, on 1,200 × 1,000 mm pallets stacked to 1,000 mm.
| Schritt | Berechnung | Lösung |
|---|---|---|
| Coils needed per minute | 200 m/min ÷ 100 m | 2 coils/min |
| Coil size check | 400 mm OD, 120 mm high | inside the strapping-and-stacking range (OD 180–400 mm, height 80–130 mm) |
| Coiler speed | up to 2 coils/min | Streichhölzer |
| Coils per layer | 1,200 ÷ 400 = 3; 1,000 ÷ 400 = 2 | 6 |
| Schichten | 1,000 mm ÷ 120 mm, rounded down | 8 (960 mm) |
| Spulen pro Palette | 6 × 8 | 48 |
| Palettenwechsel | 48 ÷ 2 coils/min | alle 24 Minuten |
| Palettenladung | 48 × 20 kg | 960 kg |
Ergebnis. At 2 coils per minute the stacker builds a full pallet every 24 minutes. The coiler sets the pace, so the covering station and robot must keep up with it. If the line runs faster, the next step is a second coiler, not a faster robot.
Auswahlliste: Was Sie uns senden sollten
- Cable diameter, length per coil and line speed.
- Spulen-Innendurchmesser, Außendurchmesser, Höhe und Gewicht.
- Covering: shrink film or stretch wrap; label inside or outside.
- Stacking: robot or gantry, pallet size L × W, stacking height and pattern.
- Online behind the extruder, or offline.
- Voltage and air supply.
Sicherheit: EN 415-10 und ISO 12100
We design the line to EN 415-10 and assess its risks to ISO 12100. The clamp, the turntable and the robot are the moving hazards. The robot works inside a fenced cell, and we interlock the access door so the robot stops when it opens. The robot cell also follows the industrial robot safety standard ISO 10218. Guards and CE documents are agreed per project.
Häufig gestellte Fragen zur Technik
Q: Can one line pack several cable sizes? A: Yes, within the coil range of the coiler; lengths and parameters are set on the HMI.
Q: Shrink or stretch wrap: which costs less to run? A: Stretch wrap usually costs less to run, because it needs no heat; a shrink tunnel draws heating power all the time it is ready. Shrink film gives a closed pack. We compare film use and energy per coil for your sizes.
Q: Robot or gantry? A: A robot suits compact cells and pattern changes; a gantry suits long lines and heavier coils.
Q: Which standard applies? A: EN 415-10 for the line, with ISO 12100 for the risk assessment.
Nächster Schritt
- Send coil sizes, line speed and pallet pattern an info@fhopepack.com.
- Wir wählen the coiler, covering and stacking modules.
- Wir antworten innerhalb von 24 Stunden mit Layout und Angebot.
Verwandte lesen
- Automatische Kabelwickel-, Umreifungs- und Schrumpfverpackungsmaschine
- Wire cable rewinding and strapping machine, 24-hour running
- Economic cable coil packing machine
- Coil stacking and palletizing equipment
- Cable winding and strapping with stacking (product)
Quellen
- FHOPE product pages: automatic cable winding machine; cable winding and strapping with stacking
- FHOPE project notes on cable packing options and pre-quote questions
- Our robot stacking line shown above
- Durchgerechnetes Beispiel: illustrative Abbildungen
- Normen: EN 415-10; ISO 12100:2010
Letzte Überprüfung: 21.09.2026