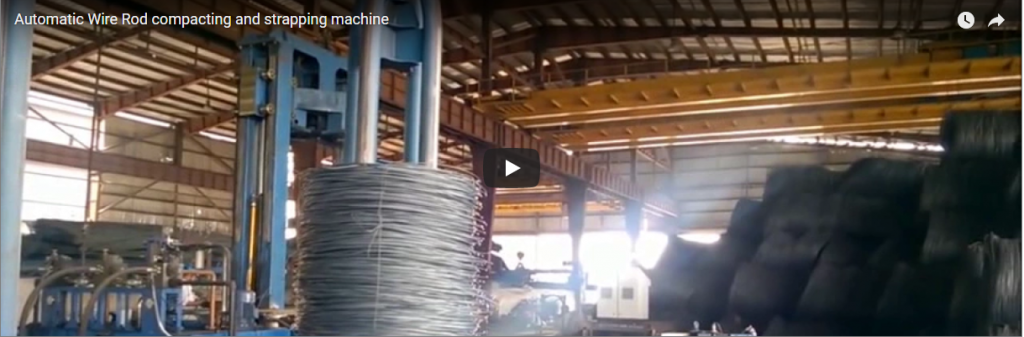
Executive summary This clip shows our wire coil strapping lines in a large wire plant. Many lines run side by side; on each, wire coils travel along yellow roller conveyors through strapping stations that band them, then move on to the line end. With many drawing machines, each strapping line serves a group of them.
Inhaltsverzeichnis
- Was der Clip zeigt
- Why many short lines
- How many lines
- Was wir pro Pflanze festgelegt haben
- Auswahl-Checkliste
- Sicherheit
- Häufig gestellte Fragen zur Technik
- Nächster Schritt
- Verwandte lesen
- Quellen
Was der Clip zeigt
| Schritt | Was Sie sehen |
|---|---|
| Halle | Many coil lines side by side in a large wire plant |
| Fördern | Coils travel on yellow roller conveyors |
| Strapping | Strapping stations band each coil |
| Betreiber | Staff move between lines |
| Auslauf | Strapped coils reach the line end |
Why many short lines
- Short routes. Each line sits near its drawing machines.
- No single choke point. One line stopping does not stop the plant.
- Shared design. All lines share spare parts.
- Step-by-step growth. Add lines as you add drawing machines.
How many lines
Durchgerechnetes Beispiel (zur Veranschaulichung).
| Artikel | Wert |
|---|---|
| Plant output (illustrative) | 600 Spulen pro Stunde |
| One strapping line (illustrative) | 80 Spulen pro Stunde |
| Lines needed, 600 ÷ 80 | 7.5, so 8 lines |
| Coils per line at 8 lines, 600 ÷ 8 | 75 Spulen pro Stunde |
| Spulengewicht (beispielhaft) | 1,000 kg |
| Tonnes per line, 75 × 1,000 kg | 75 t per hour |
Was wir pro Pflanze festgelegt haben
| Rahmen | Kommt drauf an |
|---|---|
| Bänder pro Spule | Coil weight and transport |
| Armbänder | PET oder Stahl |
| Conveyor | Coil size and layout |
| Zeilenanzahl | Plant output |
Auswahl-Checkliste
- Spulenaußendurchmesser, Innendurchmesser, Höhe und Gewicht.
- Gurte pro Spule.
- Plant output.
- Drawing machines per line.
- Grundriss.
- PET- oder Stahlband.
Sicherheit
- Keep clear of strapping heads while they move.
- Stay off roller conveyors.
- Sperren Sie die Sperre, bevor Sie eine Riemenstörung beheben.
- Für die CE-Märkte ist die Maschine nach ISO 12100 und EN 415-10 ausgelegt.
Häufig gestellte Fragen zur Technik
Q: Why many lines instead of one? A: Short routes, no single choke point, and lines grow with the plant.
Q: How many lines does a plant need? A: Plant output divided by line rate; 8 lines in the worked example.
Q: What strap is used? A: PET or steel, chosen by coil weight and transport.
Q: Can lines be added later? A: Yes, as drawing machines are added.
Q: Do lines share parts? A: Yes, all lines use the same design and spares.
F: Welche Normen gelten? A: Für CE-Märkte gelten ISO 12100 und EN 415-10.
Nächster Schritt
We match wire coil strapping lines in three steps:
- Reichen Sie Ihre Layoutzeichnung ein. with coil sizes, plant output and layout, to info@fhopepack.com.
- Sie erhalten innerhalb von 48 Stunden ein Angebot. mit den Maschinendaten und dem Layout.
- Buchen Sie eine Standortbesichtigung so we confirm the plant layout.
Verwandte lesen
- Stahldrahtspulen-Wickel-, Aufricht- und Stapellinie
- Drahtbindemaschine für Bewehrungsstahl- und Stangenbündel
- Komplettwickelmaschine für kleine Spulen
- Spulenverpackungsmaschine
Quellen
- Maschineninhalt: FHOPE-Entwicklungsteam, 04.10.2026
- Clip: das Video auf YouTube
- Line count: our worked example, illustrative values
- Geltungsbereich der Normen: ISO 12100:2010; EN 415-10: 2014
- Frist für die Angebotsabgabe: Genehmigtes Haus CTA (Angebot innerhalb von 48 Stunden)
Letzte Überprüfung: 21.09.2026