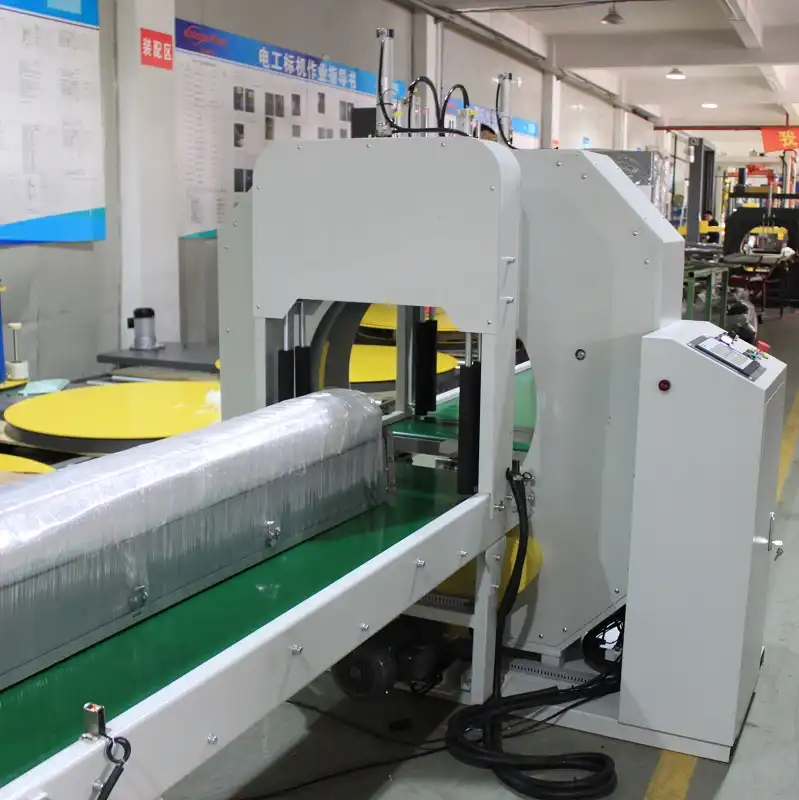
บทสรุปผู้บริหาร Our automatic horizontal orbital bar wrapping machine spiral wraps bundles of round, square, and hexagonal steel bars as they traverse through a high-speed rotating ring. The integrated pneumatic clamp-and-cut mechanism automatically secures and severs the stretch film at cycle completion, enabling fully unattended inline operation. For dense metal profiles, bundle structural payload limits the equipment frame long before reaching the ring diameter clearance. For example, a 6 m solid steel bar of 20 mm diameter weighs approximately 14.8; consequently, a standard 100 kg load-rated wrapper reaches its mechanical threshold with just บาร์ 6, regardless of remaining ring aperture space.
สารบัญ
- วิธีที่เครื่องจักรห่อมัดแท่งเหล็ก
- เหตุใดน้ำหนักจึงเป็นตัวกำหนดรุ่น
- แท่งต่อมัด
- หน้าต่างรุ่น
- เครื่องตัดและป้อนฟิล์มแบบไร้คนควบคุม
- สาธารณูปโภคและความปลอดภัย
- รายการตรวจสอบการคัดเลือก
- คำถามที่พบบ่อยด้านวิศวกรรม
- ขั้นตอนต่อไป
- การอ่านที่เกี่ยวข้อง
- แหล่งที่มา
วิธีที่เครื่องจักรห่อมัดแท่งเหล็ก
In continuous finishing mills and metal processing facilities, the horizontal orbital wrapper integrates directly inline with powered roller handling systems. Bundles move horizontally through the rotating center without secondary overhead crane rigging or manual reorientation. The automated wrapping sequence executes across four coordinated stages:
- การป้อนข้อมูลและการจัดทำดัชนี Powered V-groove or flat conveyor rollers advance the rigid bundle toward the orbital ring. A heavy-duty retro-reflective optical photocell detects the leading bar edge to initiate the wrapping sequence.
- Orbital Spiral Wrapping. The precision-machined aluminum casting ring rotates the film carriage circumferentially around the longitudinal axis of the bundle while the conveyor drives linear transfer. This dual-axis motion generates a continuous, helical protective layer.
- Pneumatic Cut and Clamp. At the trailing bundle edge, a pneumatic scissor-action mechanical cutter severs the film web while an automated gripper holds the leading film tail for seamless introduction onto the next workpiece.
- การระบายออก Powered outfeed conveyors evacuate the tightly strapped bundle onto downstream accumulation tables or automatic strapping stations.
Dual variable-frequency drives (VFD) govern ring angular velocity and linear conveyor speed independently. Packaging overlap is fully adjustable from 10% to 90% via the HMI touchscreen, governed by the kinematic relationship:
Overlap % = [1 - (V_conveyor / (N_ring × W_film))] × 100%
ที่ไหน:
V_conveyor= Linear line speed (m/min)N_ring= Orbital ring rotation speed (r/min)W_film= ความกว้างของแผ่นฟิล์มที่ใช้งานได้จริง (เมตร)
เหตุใดน้ำหนักจึงเป็นตัวกำหนดรุ่น
Carbon steels, alloy steels, and stainless bars exhibit high volumetric mass densities (~7,850 kg/m³). In industrial packaging engineering, orbital wrappers are categorized simultaneously by their internal ring diameter (geometric envelope) and dynamic roller load capacity (structural payload). For metal bar bundles, maximum bearing load is almost universally exceeded before the workpiece envelope fills the orbital ring diameter.
The nominal mass of solid round steel bars is calculated as:
Mass per metre (kg/m) = ρ × (π / 4) × d²
ที่ไหน:
ρ(density of steel) = 7,850 kg/m³d= Bar diameter (m)
Reference mass calculations for common stock sizes:
- 20 mm solid bar: Cross-sectional area = 0.000314 m²; linear mass = 2.47 กก. / ม. A standard 6 m industrial length weighs 14.8.
- 12 mm solid bar: Cross-sectional area = 0.000113 m²; linear mass = 0.89 กก. / ม. A standard 6 m industrial length weighs 5.3.
แท่งต่อมัด
Total package weight is determined by dividing the conveyor frame and bearing dynamic load ratings by single-bar mass. Sizing parameters for standard 6 m industrial bar bundles:
| เส้นผ่าศูนย์กลางบาร์ | Unit Weight (6 m Bar) | Max Count (100 kg Limit) | Max Count (200 kg Limit) |
|---|---|---|---|
| 12 มม | ~ 5.3 กก | 18 bars (Total: ~95.4 kg) | 37 bars (Total: ~196.1 kg) |
| 20 มม | ~ 14.8 กก | 6 bars (Total: ~88.8 kg) | 13 bars (Total: ~192.4 kg) |
The “Heavy but Slim” Engineering Dilemma
Thirteen 20 mm bars nested in a tight hexagonal packing configuration create a bundle cross-section of only 80–100 mm outer diameter (OD). While total mass (~192 kg) demands a heavy-duty frame like the E600 series, standard large-aperture chassis typically specify a minimum working dimension of 200 mm OD.
This lower boundary is not caused by ring clearance. It is governed by tooling geometry:
- Cylinder Stroke Limits: Standard vertical hold-down pneumatic cylinders run out of stroke, failing to clamp bundles under 200 mm securely against high centrifugal film tension.
- Conveyor Bridge Gaps: The longitudinal distance between infeed and outfeed cantilever rollers leaves a physical gap at the ring center. Thin bundles sag under their own concentrated deadweight, potentially catching on frame edges.
For such profiles, our engineering team integrates extended-stroke pneumatic stabilizer cylinders and intermediate powered bridge rollers coated with 90 Shore A polyurethane to safely process slim, heavy bundles without surface marking or sagging. Always verify bundle envelope dimensions at the widest diagonal corners (OD_envelope = √(Width² + Height²)).
หน้าต่างรุ่น
| รุ่น | Usable Bundle OD | Dynamic Weight Limit | Min. Workpiece Length | ความเร็วในการห่อเชิงเส้น |
|---|---|---|---|---|
| E300 | 100 – 300 มม | 15–100 กก | ≥ 1,000 มม | 5–15 ม./นาที |
| E400 | 100 – 400 มม | 15–100 กก | ≥ 1,200 มม | 5–25 ม./นาที |
| E600 | 200 – 600 มม | 20–200 kg (Upgradable) | ≥ 800 mm (W/ Bridge Support) | ออกแบบตามสั่ง |
การขอ E300 และ E400 come standard with 2,000 mm heavy-duty motor-driven infeed and outfeed roller conveyors, variable conveying speeds of 6–12 m/min, and balanced ring drives operating at 20–90 r/min.
การขอ E400 features a versatile multi-material core carriage supporting stretch film, VCI anti-corrosion film, crepe paper, and woven PP tape on standard 50 mm or 76 mm cores.
งานหนัก E600 includes dual-sided adjustable guide rollers to prevent axial bundle wandering during wrapping, alongside high-durometer rubber-lagged vertical press rollers that stabilize bundles against rotational torque.
เครื่องตัดและป้อนฟิล์มแบบไร้คนควบคุม
The automatic clamping, feeding, and cutting unit eliminates operator intervention during active packaging cycles:
- Automated Clamping and Feeding: At cycle initialization, a pneumatic gripper extends the film tail into the ring orbit. The bundle forward travel traps the film web against the steel bars, releasing the mechanical gripper as tension establishes.
- Precision Pneumatic Cut: Upon completing the programmed wrap count at the trailing end, a double-acting pneumatic cylinder drives a serrated industrial cutter blade to slice the film cleanly.
- Home Position Indexing: A proximity sensor and motor dynamic brake lock the rotating ring in its precise mechanical zero-position after each cycle, ensuring the film tail matches the gripper alignment.
- การวินิจฉัยข้อผิดพลาด: Integrated PLC software monitors roll exhaustion, film breaks, pneumatic pressure drops, and photo-eye occlusions, showing real-time alarms on the operational stack light and HMI panel.
The central Siemens/Mitsubishi PLC features standard I/O communication blocks, allowing full integration into upstream automated bar bundle stackers and downstream automated strapping cells.
สาธารณูปโภคและความปลอดภัย
| ประโยชน์ใช้สอย / คุณสมบัติ | E300 / E400 Systems | E600 Heavy-Duty System |
|---|---|---|
| พลังงานไฟฟ้า | 2.5 กิโลวัตต์, 380 โวลต์, 3 เฟส, 50/60 เฮิรตซ์ | 4.5 กิโลวัตต์, 380 โวลต์, 3 เฟส, 50/60 เฮิรตซ์ |
| ระบบจ่ายอากาศอัด | 0.5–0.8 MPa (5–8 bar), Clean/Dry Air | 0.5–0.8 MPa (5–8 bar), Flow ≥ 0.3 m³/min |
| เรขาคณิตของม้วนฟิล์ม | Outer Diameter: 100–200 mm; Width: 100–200 mm | Outer Diameter: 150–250 mm; Width: 150–250 mm |
| ข้อกำหนดพื้นฐาน | Reinforced concrete, level within ±2 mm, load bearing ≥ 1.0 t/m² | Reinforced concrete, level within ±2 mm, load bearing ≥ 2.5 t/m² |
CE & Industrial Safety Compliance
All machines incorporate smooth frequency-inverter acceleration/deceleration curves to prevent mechanical shock loads. Guarding and perimeter interlocks meet strict regional safety regulations:
- ISO 12100:2010: Standardized machinery risk assessment and hazard reduction verification.
- ห้องน้ำในตัว 415-10:2014: Dedicated safety requirements for automated modular packaging machinery.
- วงจรความปลอดภัย: Dual-channel Category 4/PLe emergency stop circuits, interlocking access tunnel guards, and entry/exit safety light curtains with muting capabilities for material passage.
รายการตรวจสอบการคัดเลือก
When specifying an orbital bar wrapping line, supply the following mechanical parameters:
- Material profile (solid round, structural hex, square bar, alloy grade).
- Individual bar dimension: Outer diameter (mm), length (mm), and unit weight (kg).
- Bundle configuration: Target bar count per bundle and calculated aggregate weight (kg).
- Bundle envelope: Minimum and maximum bundle cross-sectional outer diagonal (mm).
- Throughput target: Required bundles per hour and line linear speed (m/min).
- Packaging medium: LLDPE stretch film (17–35 µm), VCI rust-inhibiting film, woven polypropylene, or reinforced kraft paper.
- Integration scope: Standalone workstation with gravity staging vs fully automated inline tie-in.
คำถามที่พบบ่อยด้านวิศวกรรม
Q: How do you accurately calculate the weight of a solid 6 m, 20 mm steel bar?
A: Weight is derived from base density: 7,850 kg/m³ × [π × (0.010 m)²] × 6 m = 14.80 kg.
Q: How many 20 mm bars can be processed on a 100 kg rated wrapper?
A: At 14.8 kg per 6 m length, a 100 kg rated machine accepts a maximum bundle of 6 bars (6 × 14.8 kg = 88.8 kg). Processing 7 bars raises bundle weight to 103.6 kg, exceeding bearing payload ratings. A 200 kg rated unit is required for bundles up to 13 bars.
Q: Why cannot a standard E600 wrap an 80 mm diameter steel bar bundle despite falling well within the weight capacity? A: Large machines use vertical hold-down cylinders and roller spans designed for 200–600 mm envelopes. On an 80 mm bundle, standard cylinders bottom out before clamping, and the bar bundle sags across the center conveyor gap. Sizing this application requires engineered intermediate bridge rollers and extended cylinder strokes.
Q: Can the orbital wrapper run unattended without an operator? A: Yes. The automatic pneumatic cut-and-clamp unit grabs, breaks, and indexes the packaging film at each bundle transition without manual assistance.
Q: What sets the minimum bundle length on the E300 (1,000 mm)? A: The bundle must span the center gap between infeed and outfeed conveyors while staying supported by at least two live roller sets on each side to prevent tipping or jamming in the ring.
ขั้นตอนต่อไป
Our packaging engineering group configures bar wrapping equipment tailored to specific material handling requirements:
- ส่งข้อมูลจำเพาะของสายการผลิต: Send product profiles, bundle dimension distributions, and plant layout drawings to info@fhopepack.com.
- Technical Proposal within 48 Hours: Receive a complete engineering quote detailing ring sizing, kinematic overlap calculations, conveyor load ratings, and footprint layouts.
- Engineering Site Survey & Line Review: Finalize mechanical interfaces, VFD synchronization protocols, and integration points with our engineering design team.
การอ่านที่เกี่ยวข้อง
- Horizontal stretch wrapper E300 series
- Automatic horizontal stretch wrappers catalogue
- Video library: Automatic bar wrapping machines and compact orbital wrappers
- Video library: Heavy-duty rod orbital wrappers and bar packaging systems
- Video library: Non-ferrous metal, copper sheet, and bronze bar wrapping
แหล่งที่มา
- Fhopepack Engineering: E300 horizontal stretch wrapper specifications and cut-and-feed data
- Fhopepack Engineering: E400 orbital stretch wrapper data and multi-material carriage options
- Fhopepack Engineering: E600 heavy-duty horizontal wrapper load capacities
- Fhopepack Technical Media: Automated bar wrapping machine in factory test operation
- องค์การมาตรฐานสากล: ISO 12100:2010 ความปลอดภัยของเครื่องจักร — หลักการทั่วไปสำหรับการออกแบบ
- มาตรฐานยุโรป: EN 415-10:2014 ความปลอดภัยของเครื่องจักรบรรจุภัณฑ์ — ข้อกำหนดทั่วไป
- Density Reference: Metals and Alloys Densities, The Engineering ToolBox
แก้ไขล่าสุด: 04 กันยายน 2026





