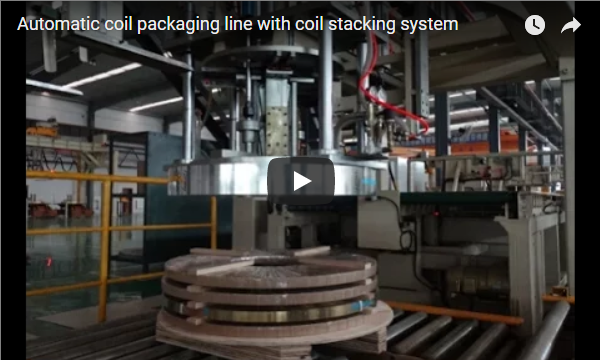
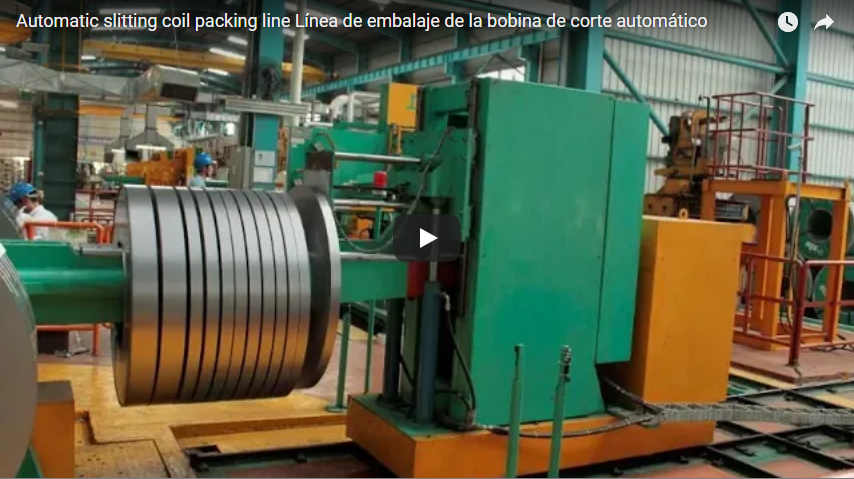
บทสรุปผู้บริหาร สายการบรรจุขดลวดตัดสำหรับศูนย์บริการรวมเอาการจัดเรียง การจัดตำแหน่ง การรัด การห่อแบบมีรู การชั่งน้ำหนัก และการเรียงซ้อนเข้าไว้ในกระบวนการทำงานอัตโนมัติเพียงขั้นตอนเดียว การกำหนดค่านี้ช่วยให้ศูนย์บริการตัดขดลวดสามารถประมวลผลขดลวดแคบๆ ได้โดยตรงจากแท่นหมุนเครื่องตัดโดยไม่ต้องใช้แรงงานคน ระบบได้รับการออกแบบมาเพื่อรองรับขดลวดที่มีน้ำหนักสูงสุด 4,000 กก. และความกว้าง 500 มม. สำหรับสายการผลิตแบบแถบแคบ หรือขนาดที่ใหญ่กว่าสำหรับการกำหนดค่าแบบงานหนัก
ภาพรวมสินค้า
This guide explains how a slit coil packing line integrates downstream processing for slitting service centers, from the station sequence and capacity matching to the specifications used to size the equipment.
เส้นทางนี้มีสถานีใดบ้าง?
The line runs each coil from the slitter output to the final pallet stack through six stations:
- ดาวน์เอนเดอร์: Tilts coils from the “eye-to-wall” orientation of the slitter turnstile to an “eye-to-sky” position, which is critical for stable downstream conveyance and stacking. The hydraulic unit runs an independent 60-second down-ending cycle and handles slit widths of 20–350 mm on a pick-up horn with about 1,800 mm of stroke [manufacturer rating].
- สถานีศูนย์กลาง: Aligns the coil with the conveyor center line using sensors and a lifting table. Proper centring ensures that strapping is applied evenly and that the coil stacks straight on the pallet.
- หน่วยสายรัด: Applies PET or steel straps radially through the coil eye at three, four, or six indexing points.
- ห่อหุ้มวงโคจร: Passes paper or stretch film through the coil eye for full coverage while support rollers rotate the coil.
- Inline weighing and labelling: Records net and gross weight and applies a barcode label for tracking.
- สถานีเรียงซ้อน: A stacking arm or gantry stacker places coils eye-to-sky onto wooden pallets, with timber separators between layers to prevent shifting in transit.
กำลังการผลิตของสายการผลิตสอดคล้องกับเครื่องตัดอย่างไร?
The packing line must clear all narrow coils from one mother coil before the next mother coil arrives at the slitter. Cycle time is set by the number of strips per mother coil and the strapping time per coil; strapping is typically the slowest station and paces the whole line.
For narrow-strip setups, the line is designed to pack 25–40 coils per hour. At 40 coils per hour, the line has 90 seconds per coil. If a slitter produces 20 strips per mother coil, the total packing time is 20 multiplied by 90 seconds, equaling 30 minutes. If the slitter’s cycle time is shorter than this, coils will queue on the turnstile. In such cases, the configuration may require a buffer conveyor, a second strapping head, or a faster stacker to maintain throughput.
ขดลวดแบบแคบและแบบกว้างมีข้อกำหนดอย่างไรบ้าง?
ข้อกำหนดต่างๆ เป็นไปตามความกว้างและน้ำหนักของขดลวด และตารางด้านล่างแสดงการเปรียบเทียบระหว่างสองรูปแบบนี้ สายการผลิตขดลวดแบบช่องแคบรองรับขดลวดที่มีความกว้างสูงสุด 500 มม. และน้ำหนัก 4,000 กก. โดยมีเส้นผ่านศูนย์กลางภายนอก (OD) สูงสุด 1,500 มม. หรือ 2,100 มม. ตามคำขอ และเส้นผ่านศูนย์กลางภายใน (ID) 508 มม. หรือ 610 มม. ส่วนสายการผลิตขดลวดแบบช่องกว้างรองรับขดลวดที่มีความกว้าง 450–1,900 มม. ด้วยอัตราการผลิตที่ช้ากว่า เพื่อให้เหมาะสมกับน้ำหนักที่มากขึ้นและขนาดที่ใหญ่กว่า ความแม่นยำในการเรียงซ้อนบนเครื่องเรียงซ้อนแบบโครงสร้างคานจะได้รับการยืนยันในแต่ละโครงการ
| พารามิเตอร์ | เส้นขดลวดช่องแคบ | สายขดลวดกว้าง |
|---|---|---|
| กำลังการผลิตบรรจุ | 25–40 คอยล์ต่อชั่วโมง | 5–8 คอยล์ต่อชั่วโมง |
| ความกว้างของขดลวด | กว้างถึง 500mm | 450 – 1,900 มม |
| น้ำหนักขดลวด | มากถึง 4,000 กก | ยืนยันตามแต่ละโครงการ |
| คอยล์ OD | สูงสุด 1,500 มม. หรือ 2,100 มม. ตามคำขอ | ยืนยันตามแต่ละโครงการ |
| คอยล์ ID | 508 มม. หรือ 610 มม | ยืนยันตามแต่ละโครงการ |
| ที่รัด | PET หรือเหล็กกล้า แรงดึง 2,000–22,000 นิวตัน | ยืนยันตามแต่ละโครงการ |
| การห่อทับซ้อน | % 10-90 | ยืนยันตามแต่ละโครงการ |
เวลาในการรัดสายคำนวณอย่างไร?
เวลาในการรัดสายเป็นข้อจำกัดหลักที่ส่งผลต่อความเร็วของสายการผลิต การรัดสายแต่ละครั้งใช้เวลาประมาณ 15 ถึง 35 วินาที บนหัวรัดอัตโนมัติสำหรับพลาสติก PET หรือเหล็ก เวลาทั้งหมดขึ้นอยู่กับจำนวนสายที่ต้องการต่อม้วน
For example, four straps at 15 seconds each take 60 seconds, which fits within the 90-second budget for a 40-coils-per-hour line. However, four straps at 35 seconds each take 140 seconds, which limits the line speed to approximately 25 coils per hour. Heavy coils requiring six straps take even longer and run at the lower end of the capacity range. Turntable indexing and conveyor transfer add time on top of the strap cycles, measured per layout. A related turntable-stacker configuration straps at a 15-second cycle with automatic 3/4/6-strap sequences [manufacturer rating].
ใช้วัสดุห่อหุ้มอะไรบ้าง?
เครื่องห่อแบบวงโคจรจะส่งวัสดุผ่านรูของขดลวดขณะที่ขดลวดหมุน การซ้อนทับกันระหว่างชั้นจะถูกตั้งค่าระหว่าง 10% ถึง 90% ผ่าน PLC การเลือกใช้วัสดุขึ้นอยู่กับข้อกำหนดในการจัดส่งและสภาพการจัดเก็บ
Stretch film is used for protection against dust and moisture during storage. VCI (Volatile Corrosion Inhibitor) paper is selected for steel coils that require rust protection during sea freight. Woven fabric provides a tougher outer layer for additional protection. Composite wraps, such as VCI paper under stretch film, combine both functions to suit different customer needs [manufacturer rating].
กระบวนการเรียงซ้อนทำงานอย่างไร?
The stacker picks packed coils using an electromagnet or vacuum system and places them eye-to-sky on wooden pallets; coils per pallet and stack height follow the coil’s OD, width, and weight. Maximum stacking capacity reaches 6,000 kg per pallet at 1,000 mm stack height including the pallet [manufacturer rating]. Timber separators between layers keep tall stacks stable and prevent shifting in transit.
พาเลทที่ผลิตเสร็จแล้วจะถูกลำเลียงโดยสายพานลำเลียงแบบลูกกลิ้งไปยังโซนจัดส่ง ในสายการผลิตอัตโนมัติเต็มรูปแบบ พาเลทที่ผลิตเสร็จแล้วอาจถูกห่อ ชั่งน้ำหนัก และติดฉลากแยกต่างหากจากฉลากของแต่ละม้วน เพื่อให้มั่นใจได้ถึงการตรวจสอบย้อนกลับและการปกป้องอย่างสมบูรณ์
มีระดับการทำงานอัตโนมัติแบบใดบ้าง?
Three automation levels suit different service center needs; the table lists what each adds. The basic level replaces manual crane-and-hook handling with controlled machines; the fully automated level also sorts coils by width, OD, and stacking logic in the program.
| ระดับอัตโนมัติ | อุปกรณ์หลัก |
|---|---|
| สายผลิตภัณฑ์พื้นฐานขนาดกะทัดรัด | รถเข็นม้วนสาย, ปลายลงเอียงได้ 90°, แท่นหมุนสำหรับรัดสายแบบกึ่งอัตโนมัติ, เครนยก หรือเครื่องเรียงซ้อนแม่เหล็ก |
| สายการผลิตอัตโนมัติมาตรฐาน | เครื่องหยิบและยกสินค้าผ่านประตูหมุน, เครื่องชั่งน้ำหนักแบบอินไลน์, เครื่องมัดสินค้าอัตโนมัติหรือกึ่งอัตโนมัติ, เครื่องยกแบบรถเข็น |
| สายการผลิตอัตโนมัติเต็มรูปแบบ | รถขนขดลวดและรถยกแบบคว่ำ, ระบบรัดอัตโนมัติ, การห่อแบบมีรู, การเรียงซ้อนบนโครงเหล็ก, การห่อพาเลท, การชั่งน้ำหนักและการติดฉลาก |
ข้อกำหนดด้านการควบคุมและสาธารณูปโภคมีอะไรบ้าง?
สายการผลิตนี้ควบคุมด้วย PLC รุ่น Siemens S7-1200 หรือ S7-1500F พร้อม HMI รุ่น S7-1500F เป็น PLC ที่มีระบบป้องกันความเสียหาย (fail-safe) สำหรับฟังก์ชันด้านความปลอดภัยในสายการผลิตอัตโนมัติเต็มรูปแบบ ระบบทำงานด้วยไฟ 3 เฟส 380–480 V, 50/60 Hz อุปกรณ์นิวแมติกต้องการแรงดันลม 5–8 บาร์ จึงต้องวางแผนระบบสาธารณูปโภคเหล่านี้ ณ สถานที่ติดตั้งก่อนการติดตั้งจริง
เราจะมั่นใจเรื่องความปลอดภัยได้อย่างไร?
Safety is a critical design aspect. Moving coils, the stacker, and strapping heads present main hazards. Automatic zones are fenced, and light curtains and safety interlocks are fitted at the stacking and strapping stations. They stop the stacker and heads when an operator enters the zone.
สำหรับตลาด CE นั้น ISO 12100 กำหนดวิธีการประเมินความเสี่ยง และ EN 415-10 กำหนดข้อกำหนดทั่วไปสำหรับเครื่องจักรบรรจุภัณฑ์ มาตรฐานเหล่านี้ใช้เป็นข้อมูลอ้างอิงในการออกแบบ การรับรองเครื่องจักรที่ส่งมอบจะได้รับการยืนยันในข้อตกลงการสั่งซื้อโครงการ เราไม่เรียกร้องใบรับรองแยกต่างหาก
ข้อมูลใดบ้างที่จำเป็นสำหรับการตั้งค่าจริง?
To size the line accurately, provide the following data; it allows precise calculation of cycle times and equipment selection.
- ช่วงความกว้างของขดลวด เส้นผ่านศูนย์กลางภายนอก เส้นผ่านศูนย์กลางภายใน และน้ำหนัก สำหรับขดลวดทั้งแบบแคบและแบบกว้าง
- จำนวนแถบต่อขดลวดแม่แบบและเวลาของรอบการตัด
- จำนวนสายรัดต่อม้วน และชนิดของสายรัด (PET หรือเหล็ก)
- วัสดุห่อหุ้มที่นิยมใช้: ฟิล์ม กระดาษ VCI หรือผ้าทอ
- ข้อกำหนดเกี่ยวกับขนาดพาเลท ความสูงของกองซ้อน และการใช้ตัวคั่น
- ความต้องการด้านการชั่งน้ำหนัก การติดฉลาก และการเชื่อมต่อกับระบบ ERP
Send this data to receive a line proposal with the station list, strapping time check, and layout — delivered within 48 hours after we confirm the details.
การอ่านที่เกี่ยวข้อง
- ภาพรวมสายการผลิตบรรจุขดลวดอัตโนมัติ
- สายการบรรจุหีบห่อ
- ระบบสายการบรรจุอัตโนมัติ
- รายละเอียดเครื่องบรรจุขดลวด
- การจัดการม้วนกรีดและสายการบรรจุ
- ระบบบรรจุภัณฑ์ขดลวดตัดอัตโนมัติ
แหล่งที่มา
- FHOPE product pages: slit coil handling and packaging line; automatic slit coil packaging system; automatic slitting coil packaging line with turntable stacker
- ISO 12100 (risk assessment); EN 415-10 (packaging machines)
แก้ไขล่าสุด: 29 กันยายน 2026