Rezumat Our compact horizontal orbital stretch wrappers spiral film around single aluminum profiles and small bundles as they pass through the rotating ring. Three standard models cover cross-sectional package diagonals of 50–100 mm (E100), 50–200 mm (E200) și 100–300 mm (E300). Because film width, linear conveyor speed, and ring rotational speed dictate surface overlap, we engineer ring geometry and drive ratios simultaneously to guarantee protective integrity and throughput.
Cuprins
- Cum funcționează încapsulatorul de profil
- Trei modele compacte
- Măsurarea diametrului exterior al pachetului
- Viteză, lățime film și suprapunere
- Manipularea filmelor fără personal
- Utilități și siguranță
- Listă de verificare pentru selecția unui încapsulator de profil
- Întrebări frecvente despre inginerie
- Next step: from drawing to proposal
- Citire conexă
- Surse
Cum funcționează încapsulatorul de profil
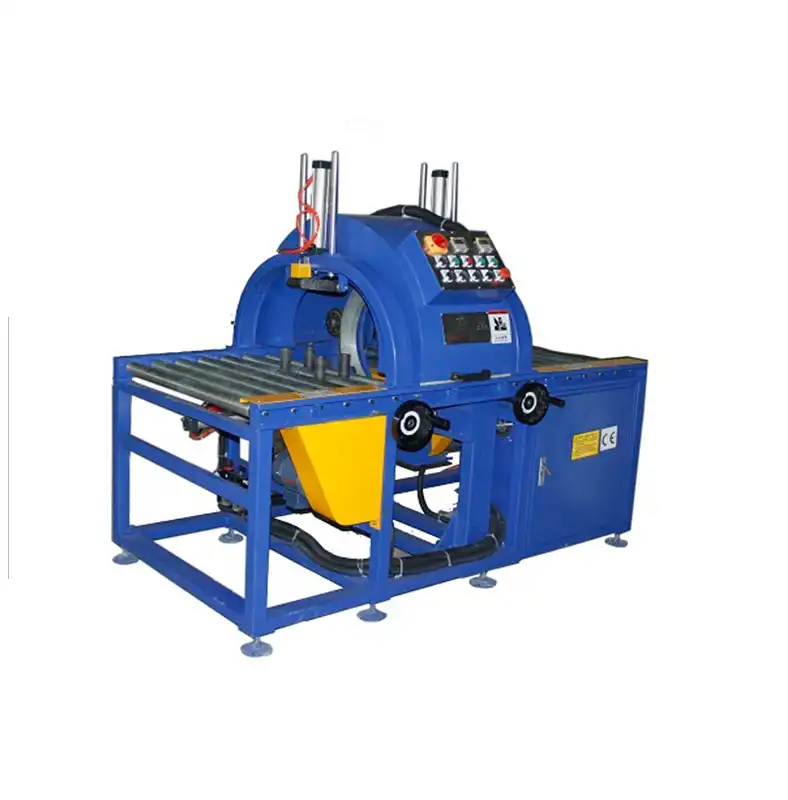
Our horizontal orbital stretch wrapper transports extrusions along motorized infeed and outfeed roller conveyors directly through a central rotating ring. A photoelectric sensor tracks the profile leading edge, triggering the orbital ring drive, determining the exact wrapping start position, and controlling the trailing-edge cutting cycle. Non-marking, polyurethane-coated side guide rollers maintain the workpieces firmly along the conveyor centerline, preventing lateral shifting or orbital torque twist during high-speed rotation.
Ring rotation and linear conveyor travel are powered by independent variable-frequency drives (VFD). This configuration allows operators to adjust ring RPM and linear travel speed separately via the PLC touch screen. The drive system incorporates controlled S-curve acceleration and deceleration ramps, ensuring soft starts, smooth stops, and accurate automatic homing so that every profile bundle begins its wrapping cycle at the exact mechanical reference point.
Trei modele compacte
All three standard compact models share an identical material handling footprint: a 2,000 mm motorized infeed conveyor and a 2,000 mm motorized outfeed conveyor. The mechanical film carriage accepts standard stretch film rolls with an external diameter of 100–200 mm mounted on a standard 50 mm (2-inch) core.
| Parametru | E100 | E200 | E300 |
|---|---|---|---|
| Package OD (Diagonal) | 50 – 100 mm | 50 – 200 mm | 100 – 300 mm |
| Lungimea pachetului | ≥ 1,000 mm | ≥ 1,000 mm | ≥ 1,000 mm |
| Capacitate de greutate utilă | 8-100 kg | 8-100 kg | 15-100 kg |
| Viteza de rotație a inelului | 20–120 RPM | 10–120 RPM | 20–90 RPM |
| Wrapping linear speed | 3–15 m/min | Confirmed by profile geometry | 5–15 m/min |
| Conveyor speed (Infeed/Outfeed) | 6–12 m/min (Adjustable) | 6–12 m/min (Adjustable) | 6–12 m/min (Adjustable) |
| Lățimea rolului de film | 50 – 100 mm | 100 – 200 mm | 100 – 200 mm |
| Overlap ratio range | 10-90% | 10-90% | 10-90% |
Our technical specifications separate wrapping linear speed through the ring from conveyor transit speeds. Because structural profiles with irregular fins create varying aerodynamic and mechanical resistance, wrapping speeds for intermediate cross-sections (E200) are matched to your profile drawings during application review.
Măsurarea diametrului exterior al pachetului
The effective package outside diameter (OD) corresponds to the maximum cross-sectional diagonal of the profile or packed bundle, rather than width or height alone. The orbital ring clearance must accommodate this diagonal plus carriage clearance margins.
Package OD = √(Width² + Height²)
Illustrative engineering calculations:
- 60 × 40 mm architectural extrusion:
√(60² + 40²) = √(3600 + 1600) ≈ 72.1 mm. Fits within the E100 operational envelope (50–100 mm). - 150 × 120 mm extrusion bundle:
√(150² + 120²) = √(22500 + 14400) ≈ 192.1 mm. Requires the E200 or E300 platformă. - 250 × 150 mm industrial bundle:
√(250² + 150²) = √(62500 + 22500) ≈ 291.5 mm. Fits within the E300 envelope (100–300 mm).
For heavy extrusions or master packaging exceeding 300 mm OD, our engineering line transitions to heavy-duty horizontal orbital wrappers accommodating 300–1,500 mm envelopes.
Viteză, lățime film și suprapunere
With each full revolution of the orbital ring, the profile moves forward by a specific pitch distance, generating a continuous helical spiral. This linear displacement per revolution is calculated as:
Advance Pitch (mm/rev) = (Linear Wrapping Speed in m/min × 1,000) ÷ Ring Speed in RPM
The advance pitch directly governs the surface overlap ratio. To achieve a nominal 50% overlap for transit surface protection, the linear advance pitch must not exceed half of the applied film roll width:
Max Advance Pitch (50% Overlap) = Film Width ÷ 2
| Model | Lățimea filmului | Viteza soneriei | Max Advance for 50% Overlap | Max Linear Speed at 50% Overlap |
|---|---|---|---|---|
| E100 | 100 mm | 120 RPM | 50 mm / rev | 6.0 m / min |
| E300 | 200 mm | 90 RPM | 100 mm / rev | 9.0 m / min |
The theoretical maximum speed of 15 m/min on the E100 is achieved only at lower overlap percentages (e.g., 20–30% for internal transport). For a standard 6 m profile running at 6 m/min under 50% overlap, net transit wrapping time is exactly 60 seconds, excluding pneumatic cut, clamping, and conveyor transfer cycles. Kinematic operational parameters are pre-programmed via PLC recipes during factory acceptance testing.
Manipularea filmelor fără personal
Each wrapper integrates an automatic pneumatic clamping and cutting unit for fully hands-off, unmanned cycles. At cycle start, the pneumatic tail holder positions the film web across the profile path. As the ring rotates, the film is anchored against the workpiece; the clamp then releases automatically. At cycle conclusion, an integrated pneumatic blade cuts the film tail clean, and the holding mechanism secures the web for the next bundle.
Film tension is controlled through an adjustable mechanical friction brake with roller compensation. For delicate thin-wall profiles or fragile powder coatings, the E100 offers an optional powered pre-stretch film carriage providing 100–250% mechanical elongation to reduce unit containment force while minimizing plastic consumption. Conveyor options across all models include non-marking polyurethane rollers, modular PVC flat belts, or driven chain tracks for customized infeed integration.
Utilități și siguranță
| Utilitate / Specificații | Technical Standard (E100 / E200 / E300) |
|---|---|
| Sarcină electrică conectată | Aproximativ. 2.5 kW |
| Alimentare electrică standard | 380 V, 3-Phase, 50/60 Hz (Custom voltages available upon request) |
| Necesar de alimentare pneumatică | 0.5–0.7 MPa (Clean, dry compressed air; consumption ~30 NL/min) |
| Arhitectura de control | Siemens / Mitsubishi PLC with industrial color touch-screen HMI |
| Diagnostic & Safety Systems | Triple-color visual beacon, acoustic fault alarm, circuit E-stops |
Safety engineering meets global plant compliance. Moving components, rotating rings, and transmission drive belts are fully enclosed by sheet-steel safety shrouds with transparent maintenance inspection doors. For CE-marked installations, machine design complies with ISO 12100: 2010 (Evaluarea și Reducerea Riscurilor) și RO 415-10: 2014 (Safety Requirements for Modular Packaging Machines). Electrical switchgear complies with EN 60204-1 safety standards.
Listă de verificare pentru selecția unui încapsulator de profil
- Maximum cross-section envelope: Measure maximum outer width and height to confirm package OD:
√(W² + H²). - Profile length boundaries: Minimum length must exceed 1,000 mm for dual-station roller span stability.
- Cerințe de debit: Required profiles/bundles per hour to size ring RPM and line indexing speeds.
- Surface overlap specification: Target protective overlap percentage (typically 30–60%) based on storage duration and transport modes.
- Surface coating sensitivity: Anodized, mill-finish, or powder-coated surfaces determine PU guide roller durometer and film tension.
- Film carriage selection: Standard mechanical brake versus powered pre-stretch unit (100–250%).
- Integration mode: Standalone off-line operation or direct in-line synchronization downstream of an automated extrusion saw line.
Întrebări frecvente despre inginerie
Q: Which orbital model is required for a single 60 × 40 mm aluminum profile?
A: The E100 model. Its calculated diagonal is √(60² + 40²) ≈ 72.1 mm, which sits cleanly within the E100 working range of 50–100 mm OD.
Q: Can the E100 operate at 15 m/min while maintaining a 50% film overlap? A: No. At the maximum ring rotational speed of 120 RPM and using a standard 100 mm film roll, the maximum allowable linear travel speed for a 50% overlap is 6.0 m/min. Achieving 15 m/min requires dropping the overlap to approximately 20%.
Q: Does the system require manual cutting or film taping between cycles? A: No. All models include an automatic pneumatic film clamp-and-cut station. The film tail is clamped at the start, wrapped in, pneumatically sliced with a heated or serrated cutter, and held firmly for the subsequent workpiece.
Q: What is the minimum workable profile length? A: Standard machines process workpieces down to 1,000 mm. Shorter profiles require specialized intermediate bridge roll transitions to bridge the gap across the orbital ring center.
Q: What equipment options exist for bundle cross-sections larger than 300 mm? A: Packages exceeding 300 mm OD transition to our heavy-duty horizontal orbital wrappers, which provide ring working envelopes from 300 mm up to 1,500 mm.
Next step: from drawing to proposal
We engineer and configure horizontal stretch wrappers according to your specific extrusion cross-sections and packing speeds:
- Submit your profile drawings: Send cross-sectional dimensions, bundle configurations, and required pieces-per-hour to info@fhopepack.com.
- Primiți o propunere de inginerie în termen de 48 de ore: We provide ring size selection, motor drive power calculations, line layout footprints, and cycle-time evaluations.
- Line integration & trial verification: Ship sample profiles for physical film tension testing and factory acceptance configuration.
Citire conexă
- E100 Horizontal Stretch Wrapper Specifications
- E200 Horizontal Stretch Wrapper Specifications
- E300 Horizontal Stretch Wrapper Specifications
- Large Bundle Aluminum Profile Wrapping Machine Line
Surse
- Specificațiile mașinii: Fhope E-Series Horizontal Orbital Stretch Wrappers
- Standarde de siguranță pentru mașini: ISO 12100:2010 Securitatea mașinilor — Principii generale de proiectare
- Siguranța utilajelor de ambalare: EN 415-10:2014 Cerințe de siguranță pentru mașinile de ambalat
- Electrical Safety Norms: IEC 60204-1 Safety of Machinery — Electrical Equipment of Machines
Ultima recenzie: 21.09.2026





