**Zusammenfassung**
>
> Radial strapping runs a steel strap through the coil eye and around the coil wall, so the wraps cannot telescope or spring loose. On a roll line the coil turns on rollers between straps, so the strapping head stays in one place and each strap lands at the next position. Our equivalent solution takes 19–32 mm steel strap and places 2, 3, 4 or 6 straps per coil. This page covers how the coil is indexed, how many straps to use, how much strap each coil takes, and the preventive maintenance the strapping head needs.
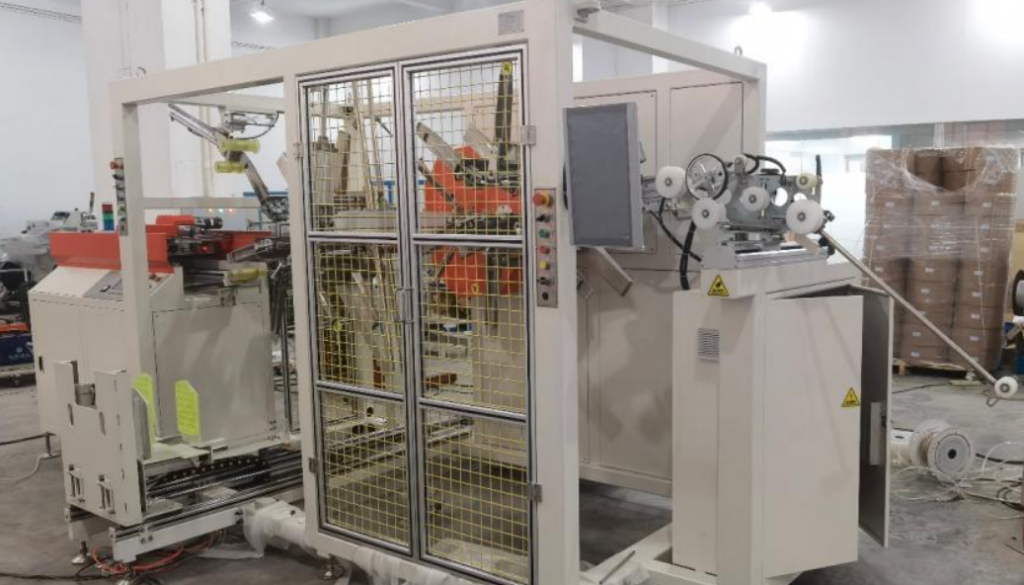
In this setup the radial strapper stands over an in-line roller station carrying a heavy steel coil, eye along the line. A guide arm on a two-axis carriage indexes in and out of the coil bore and up and down to the coil wall, and the driven rollers turn the coil between straps.
Railings run along the conveyor, hydraulic or pneumatic hoses feed the carriage, and the control box with its display and emergency stop sits beside the machine.
Inhaltsverzeichnis
- Radial and circumferential strapping
- How the coil is indexed
- How many straps per coil
- Riemenlänge pro Spule
- Strapping head, tension and joints
- Schutz der Spulenkanten
- Auswahl-Checkliste
- Sicherheit
- Häufig gestellte Fragen zur Technik
- Nächster Schritt
- Verwandte lesen
- Quellen
Radial and circumferential strapping
The two strap directions do different jobs:
| Strap | Path | What it holds |
| :--- | :--- | :--- |
| Radial (eye-through) | through the eye, across both faces and over the outer wrap | the wraps against each other, so the coil cannot telescope |
| Circumferential | around the outside diameter | the outer wrap, so the tail cannot spring open |
Heavy hot-rolled and cold-rolled coils often get both. Radial straps go on first, then circumferential straps hold the outer layer. A radial machine on the roll line handles the eye-through straps without lifting the coil off the conveyor.
How the coil is indexed
The strapping head and its strap guide arch stay on a fixed frame. The arm carries the strap guide through the coil eye, the head pulls the strap tight and closes the joint, and the arm withdraws. The rollers under the coil then turn it to the next angle, and the cycle repeats.
1. Coil stops on the rollers, centred under the head.
2. The guide arm enters the eye.
3. The strap is fed, tensioned, joined and cut.
4. The arm withdraws and the rollers turn the coil to the next position.
5. After the last strap the coil runs out to the next station.
Because the rollers turn the coil, the head stays fixed and the line needs no separate coil turning station. Where the coil cannot turn, for example on a static station, our rotating head and arch that turns 360° is the alternative. Cycle time per strap and the maximum coil weight on the turning rollers are confirmed at quote.
How many straps per coil
**Angle between straps = 360° ÷ number of straps.**
| Straps | Angle | Typical use |
| :--- | :--- | :--- |
| 2 | 180° | light, narrow coils |
| 3 | 120° | medium coils |
| 4 | 90° | standard heavy coils |
| 6 | 60° | wide or soft coils, long sea transport |
Even spacing matters more than strap count. If two straps sit close together, the coil can open on the other side.
Riemenlänge pro Spule
A radial strap crosses the coil wall twice and the coil width twice. **Strap length ≈ 2 × wall + 2 × coil width + joint, where wall = (OD − ID) ÷ 2.** Take a coil with OD 1,800 mm, ID 610 mm and width 1,200 mm (example):
| Prüfen | Berechnung | Ergebnis |
| :--- | :--- | :--- |
| Wall | (1,800 − 610) ÷ 2 | 595 mm |
| Strap length, before joint | 2 × 595 + 2 × 1,200 | 3,590 mm |
| Strap per coil, 4 straps | 4 × 3,590 | 14,360 mm (about 14.4 m) |
The joint overlap depends on the joint type and is confirmed at quote. Use this to size the strap coil feeder and to plan strap changes per shift.
Strapping head, tension and joints
Our radial strapping head takes 19–32 mm steel strap. In our slitting coil packing line the head runs two strap drives on dual servo motors, with separate feed, take-up and tensioning, and it pulls up to 22,000 N of adjustable tension. That much force needs a solid frame, so the head is mounted for easy access during maintenance.
Joints can be sealless, by notching, or welded. A PET strapping head for up to 32 mm PET strap is a lower-cost option on lighter coils. The head blows out strap debris from the nip unit, which keeps chips from wearing the parts. A strapping head can run up to about 1 million cycles.
Schutz der Spulenkanten
Steel strap at full tension can dent the coil edges and the eye. Corner protectors or cardboard inserts between strap and coil spread the load. On our lines an automatic corner protector or cardboard applicator places them before the strap is tensioned.
Auswahl-Checkliste
1. Spulen-Außendurchmesser, Innendurchmesser und Breitenbereich.
2. Coil weight and material: hot-rolled, cold-rolled, coated or painted.
3. Coils per hour on the line.
4. Straps per coil and strap width.
5. Steel or PET strap, and joint type.
6. Edge protection needs.
Sicherheit
The machine is designed to EN ISO 12100:2010 for risk assessment, EN 415-10 for packaging machine safety and EN 60204-1 for electrical equipment. The moving guide arm, the strap under tension and the turning coil are the main hazards. Railings keep people away from the conveyor, and the emergency stop sits on the control box. Guarding and CE documents are agreed per project.
Häufig gestellte Fragen zur Technik
Q: What is the difference between radial and circumferential strapping?
A: Radial straps go through the eye and hold the wraps together. Circumferential straps go around the outside and hold the outer wrap.
Q: How many radial straps does a coil need?
A: Usually 2, 3, 4 or 6, spaced evenly at 360° ÷ number of straps.
Q: How much strap does one coil use?
A: About 2 × wall + 2 × width per strap, plus the joint. A 1,800 mm OD, 1,200 mm wide coil takes about 14.4 m for 4 straps.
Q: Steel or PET strap?
A: Steel for heavy hot-rolled coils. PET up to 32 mm costs less on lighter coils.
Q: Does the coil have to leave the conveyor?
A: No. The rollers turn the coil between straps, so it stays on the line.
Nächster Schritt
1. **Send your coil sizes, weights and coils per hour** to info@fhopepack.com.
2. **We set** strap count, strap width and joint type.
3. **Wir antworten Ihnen innerhalb von 24 Stunden** mit einem Angebot und einem Kostenvoranschlag.
Verwandte lesen
- [Radial steel coil strapping machine (product)](https://www.fhopepack.com/steel-coil-strapping-machinery/Radial-steel-coil-strapping-machine.html)
- [Circumference steel coil strapping machine (product)](https://www.fhopepack.com/steel-coil-strapping-machinery/circumference-steel-coil-strapping-machine.html)
- [Steel coil radial strapping machine](https://www.fhopepack.com/videos/steel-coil-radial-strapping-machine/)
- [Cold roll coil packaging without transit corrosion and scratches](https://www.fhopepack.com/videos/how-to-eliminate-transit-corrosion-and-surface-scratches-in-high-output-cold-roll-coil-packaging/)
- [Steel coil stretch wrapping and stacking](https://www.fhopepack.com/videos/next-generation-steel-coil-packaging-solutions-integrated-stretch-wrapping-and-stacking-technology/)
Quellen
- FHOPE product pages: radial steel coil strapping machine; automated radial strip coil strapping machine by PET
- FHOPE quotation: steel coil packing line, automatic steel strapping station
- EN ISO 12100:2010; EN 415-10; EN 60204-1
- The radial strapping machine shown above
Letzte Überprüfung: 21.09.2026