ملخص تنفيذي
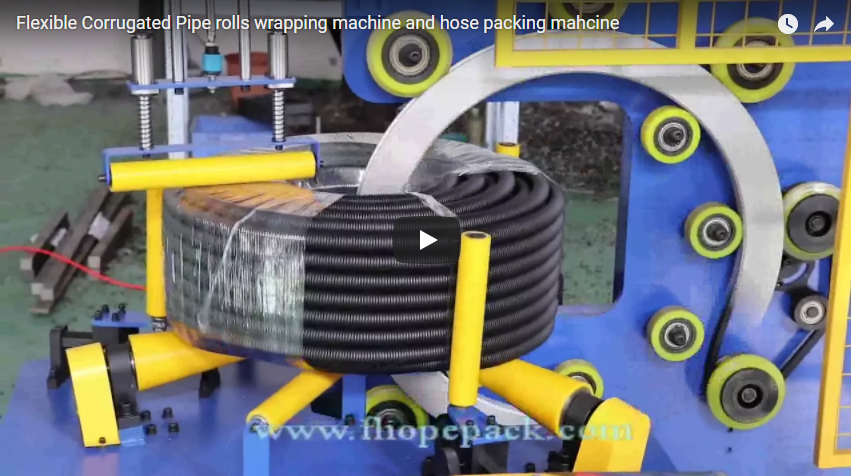
A vertical hose coil wrapping machine applies orbital stretch film through the center eye of a light, elastomeric or corrugated pipe coil standing on edge. A high-speed rotating ring guides the packaging film carriage through the hollow core while motor-driven cradle rollers rotate the coil along its horizontal axis, laying down a continuous protective spiral wrap. Designed specifically for garden hoses, corrugated electrical conduits, and drip tubing coils, the industrial FPH series balances film consumption and load stability: the FPH-300N handles coil outer diameters from 500 to 1,000 mm and unit loads from 10 to 100 kg within an automated 23–35 s cycle. The engineering guide below details mechanical kinematics, overlap calculations, anti-crush tension control, and safety integration under EN 415-10 standards.
جدول المحتويات
- Why Hose Coils Require Vertical (Eye-Horizontal) Orbital Wrapping
- Kinematic Principles: How the Vertical Ring Wrapper Operates
- Technical Specifications: FPH-200 vs. FPH-300N
- Engineering Sizing Calculation: 20 m Corrugated Drain Coil
- Parameter Optimization: Overlap Rate, Film Tension, and Anti-Crush Control
- Technical Selection Checklist for Line Engineers
- Industrial Safety Integration: EN 415-10 and ISO 12100 Compliance
- Engineering Frequently Asked Questions (FAQ)
- Application Engineering & Direct Inquiry Protocol
- الأنظمة ذات الصلة ومصادر إضافية للقراءة
- Engineering Sources and References
Why Hose Coils Require Vertical (Eye-Horizontal) Orbital Wrapping
Extruded corrugated drainage conduits, flexible PVC hoses, and PEX plumbing coils present unique post-extrusion packaging challenges: they are inherently lightweight, flexible, and springy. Manual stretch wrapping requires an operator to repeatedly pass a film dispenser through the inner center eye. This process is labor-intensive, causes uneven containment tension, and creates bottlenecks on high-speed extrusion lines running at 15–30 m/min.
Standard horizontal turntable stretch wrappers are ineffective for loose coil geometries:
- عدم الاستقرار الهيكلي: When laid flat (“eye-to-sky”) on a rotating turntable, lightweight corrugated coils slide off-center due to centrifugal force or sag under high axial film tension.
- Incomplete Surface Encapsulation: Turntables cannot pass protective material directly through the hollow eye to bind individual pipe wraps together.
استخدم vertical orbital wrapping system (coil standing on edge, eye oriented horizontally) resolves both processing constraints:
- Self-Weight Stabilization: The coil’s deadweight sits directly inside a dual-roller cradle, keeping the product centered between parallel drive shafts without requiring heavy clamping fixtures.
- Toroidal Wrapping Path: A precision-machined rotating cast-aluminum ring guides the film reel through the coil eye continuously, sealing the outer circumference, sidewalls, and interior eye in a single automated process.
Kinematic Principles: How the Vertical Ring Wrapper Operates
            [ Rotating Orbital Ring ]
                   /         \
         +--------/-----------/--------+
         |       /   Coil    /         |
         |      |   (Edge-  |          |
         |      |  Standing)|          |
  [Guide |      |    (O)    |    Guide]|
  Roller]|       \   Eye   /    [Roller|
         +--------\-------/------------+
[==Drive Rollers==]- Loading and Positioning: The operator rolls the bound coil into the machine throat, threading the open eye over the bottom segment of the orbital ring, resting the product on two polyurethane-coated drive cradle rollers.
- Radial Alignment: Adjustable side guide rollers slide inward against the coil flanks to keep narrow profiles upright during rotation without scratching the pipe exterior.
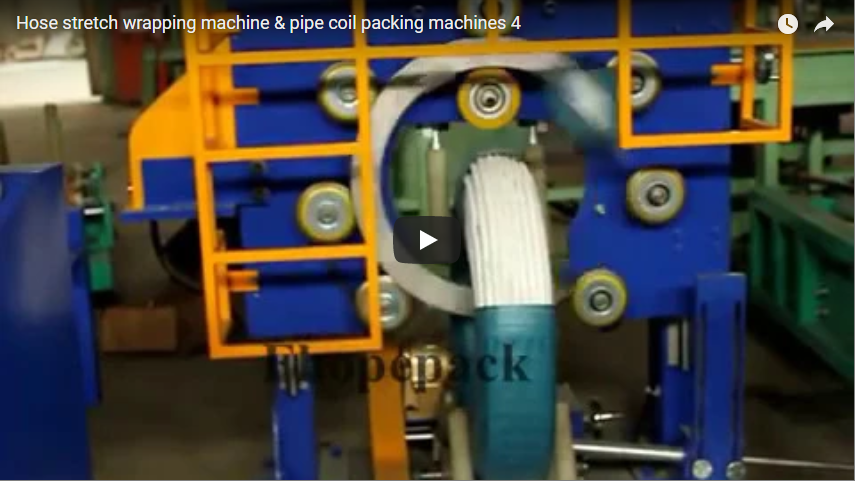
- Synchronized Orbital Motion: Upon cycle initiation, the orbital ring accelerates via variable frequency drive (VFD). Simultaneously, the cradle rollers rotate the coil around its horizontal centerline.
- Toroidal Layer Deposition: As the film carriage orbits through the hollow eye, the rotating coil creates a progressive spiral overlap along the entire circumferential body.
- Cycle Completion and Film Severing: Once the coil completes a 360° rotation (monitored by an inductive proximity switch or rotary encoder), the ring stops at its home park position. The film is cut manually or by a pneumatic pneumatic-blade assembly, allowing the sealed coil to exit via a gravity roller ramp.
Dual inverters independently control the orbital ring speed (RPM) and cradle roller feed velocity (m/min), allowing precise digital control over the surface overlap percentage.
Technical Specifications: FPH-200 vs. FPH-300N
The FPH product family accommodates various industrial hose profiles, from micro-irrigation lines to multi-layer reinforced agricultural suction pipes.
| معامل | FPH-200 (Compact Series) | FPH-300N (Standard Production) |
|---|---|---|
| Inner Diameter Range (ID) | 300 – 600 مم | 300 – 700 مم |
| Outer Diameter Range (OD) | 400 – 900 مم | 500 – 1,000 مم |
| عرض/ارتفاع الملف (W) | 50 – 200 مم | 100 – 300 مم |
| الحمولة | 5-50 كجم | 10-100 كجم |
| Orbital Ring Max Speed | 20–90 دورة/دقيقة | 20–120 r/min (VFD adjusted) |
| مدة دورة التعبئة والتغليف | 15-35 ثانية لكل لفة | 23–35 s per coil (size dependent) |
| نطاق تداخل الفيلم | 20% to 90% (programmable) | 20% to 90% (programmable) |
| سعة محرك الدفع | 1.5 kW (Ring: 0.75 kW / Rollers: 0.75 kW) | 1.9 kW (Ring: 1.1 kW / Rollers: 0.75 kW) |
| الخدمة الكهربائية | AC 380 V, 50 Hz, 3-Phase (or to order) | AC 380 V / 480 V, 50/60 Hz, 3-Phase |
| وسائط التغليف المتوافقة | LLDPE Stretch Film, PVC Wrap | LLDPE, HDPE Woven Tape, Crepe Paper |
| Packaging Material Roll Dimensions | Core ID: 50 mm; Roll OD: 100–180 mm; Width: 90–100 mm | Core ID: 50/76 mm; Roll OD: 100–200 mm; Width: 90–150 mm |
Engineering Sizing Calculation: 20 m Corrugated Drain Coil
To determine machine fit and cycle times, consider an illustrative flexible drainage coil:
- Pipe nominal OD: 65 mm
- Coil inner core diameter (mandrel ID): 400 mm
- Pack configuration: 3 pipe widths across (Coil Width = 3 × 65 mm = 195 mm)
- الطول الإجمالي: 20.0 م
1. Geometric Coil Build-up Analysis
| Layer Tier | Centerline Diameter (D_layer) | Circumference per Wrap | Length per Layer (3 wraps) | Cumulative Length |
|---|---|---|---|---|
| الطبقة الرابعة (الأساسية) | 400 مم + 65 مم = 465 مم | π × 0.465 m = 1.46 m | 3 × 1.46 م = 4.38 م | 4.38 م |
| طبقة 2 | 465 mm + (2 × 65 mm) = 595 mm | π × 0.595 m = 1.87 m | 3 × 1.87 م = 5.61 م | 9.99 م |
| طبقة 3 | 595 mm + (2 × 65 mm) = 725 mm | π × 0.725 m = 2.28 m | 3 × 2.28 م = 6.84 م | 16.83 م |
| Layer 4 (Partial) | 725 mm + (2 × 65 mm) = 855 mm | π × 0.855 m = 2.68 m | Balance: 20.0 − 16.83 m = 3.17 m | 20.00 م |
- Final Coil Outer Diameter (OD):
ID + (2 × Total Pipe Tiers × Pipe OD) = 400 mm + (2 × 4 × 65 mm) = 920 mm - Envelope Match: The dimensions (ID: 400 mm, OD: 920 mm, Width: 195 mm) fit the processing window of the طراز FPH-300N (ID 300–700 mm; OD 500–1,000 mm; Width 100–300 mm).
2. Kinematic Cycle Time & Film Delivery
- مواصفات الفيلم: 100 mm nominal film width (
W_film); Target overlap at outer diameter (Overlap_OD): 50٪. - Effective Linear Feed per Ring Revolution (
S_pitch):S_pitch = W_film × (1 - Overlap_OD) = 100 mm × (1 - 0.50) = 50 mm (0.05 m) - Required Ring Revolutions for One 360° Coil Rotation:
Total Revolutions (N) = (π × OD) / S_pitch = (3.1416 × 0.920 m) / 0.05 m = 57.8 ≈ 58 revolutions - Wrapping Time Calculation at Target Production Speed (120 r/min ring velocity):
T_wrap = (N / Ring_Speed) × 60 s = (58 / 120) × 60 s ≈ 29.0 s
التقييم الهندسي: The calculated 29-second cycle sits comfortably within the 23–35 s specification window of the FPH-300N.
Geometric Film Differential: Because the inner core circumference (π × 0.40 m ≈ 1.26 m) is substantially smaller than the outer circumference (π × 0.92 m ≈ 2.89 m), film coverage in the eye is naturally denser:
- Outer overlap: 50%
- Inner overlap:
100% - [(100% - 50%) × (400 mm / 920 mm)] ≈ 78.3%This natural differential provides reinforced binding tension at the core while saving material along the outer surface.
Parameter Optimization: Overlap Rate, Film Tension, and Anti-Crush Control
      [Film Carriage Brake System]
            |
            v  (Adjustable 5–25 N)
      ( Stretch Film ) ===> [Coil Outer Shell]
                                  |
   Radial Force (F_r) <-----------+
*Must not exceed wall collapse threshold*- Overlap Rate Settings:
- 20% to 35% Overlap: Economical dust cover and shipping tie; minimizes overall film weight.
- 50% to 65% Overlap: Industry standard for commercial pipe packaging; provides moisture resistance, structural bundling, and scuff protection during flat-bed freight.
- 70% to 85% Overlap: Hermetic wrap; prevents UV discoloration and air ingress during prolonged outdoor storage.
- Tension vs. Pipe Hoop Strength (Anti-Crush): Thin-walled corrugated PE/PP tubes collapse under high radial tension. The FPH series uses a mechanical friction brake and spring-loaded compensator arm on the ring carriage to keep film payout tension between 5 نيوتن و 25 نيوتن. Solid elastomeric rubber hoses can run up to 35 N for tighter packaging.
- Rotational Velocity Calibration: Setting the inverter frequency balances cradle roller speed against ring velocity. For lighter coils (less than 15 kg), start with ring speeds of 40–60 r/min. This prevents dynamic imbalance and keeps the coil from bouncing out of the rollers before reaching the target 100–120 r/min.
Technical Selection Checklist for Line Engineers
Before sizing an FPH wrapper, confirm your coil parameters with your packaging equipment team:
- الخصائص الفيزيائية للمنتج: Wall profile (corrugated vs. smooth-wall), material grade (HDPE, LDPE, PVC, EPDM rubber), and radial crush resistance rating.
- Coil Dimensional Extremes: Minimum and maximum ID, OD, coil axial width, and finished bundle weight.
- Packaging Media Type: Cast LLDPE stretch film (17–35 µm thickness), cross-laminated HDPE protective film, or VCI anticorrosion crepe paper rolls.
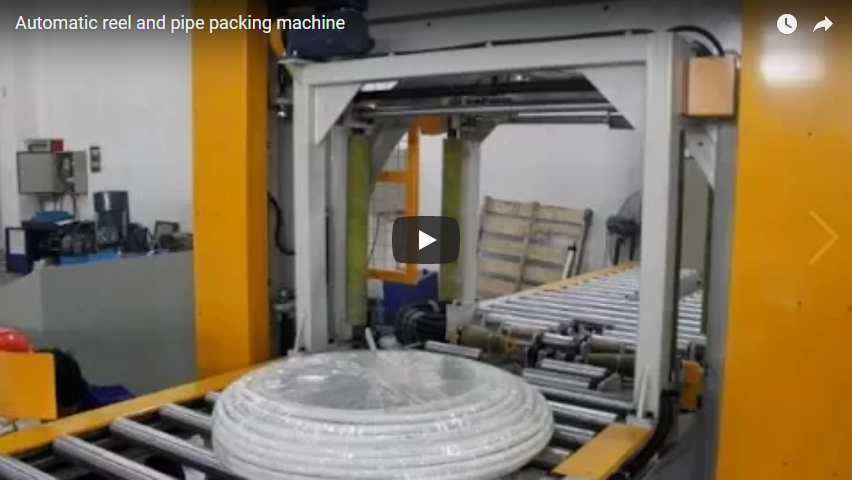
- Line Integration Level: Standalone manual cell (off-line manual load/unload) or continuous automatic line linked directly to a coiler accumulator.
- Electrical / Pneumatic Requirements: Factory line power (e.g., 220 V / 380 V / 480 V, 50/60 Hz) and clean, dry air supply (0.5–0.7 MPa) for auto-cut-and-clamp setups.
Industrial Safety Integration: EN 415-10 and ISO 12100 Compliance
The high-speed orbital ring and motorized lower rollers present potential pinch points and rotational hazards during automatic operation.
+------------------------------------------------------+
|                 YELLOW PERIMETER GUARD               |
|    +--------------------------------------------+    |
|    |           [ Upper Ring Guard ]             |    |
|    |                                            |    |
|    |   +--[Pneumatic Top Hold Roller]--+        |    |
|    |   |                               |        |    |
|    | [Side Guides]    [COIL]     [Side Guides]  |    |
|    |   |                               |        |    |
|    |   +-----[Cradle Drive Rollers]----+        |    |
|    +--------------------------------------------+    |
|      [ Safety Light Curtain / Interlocked Door ]     |
+------------------------------------------------------+- Standard Mandates: Machinery designed to meet EN-415 10 (Safety of Packaging Machines: Wrapping Machines) and risk-assessed under ISO 12100: 2010.
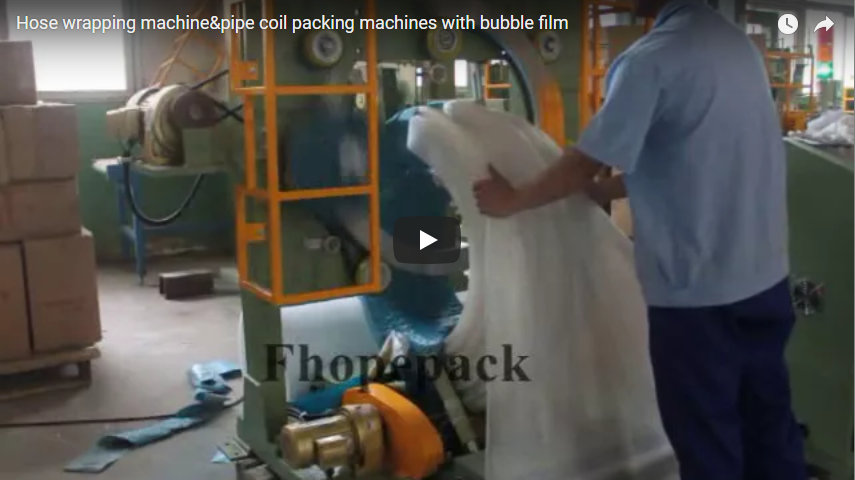
- No Manual Product Stabilization: Operators must never steady, touch, or hold a rotating coil by hand during operation.
- Mechanical Restraints: Side guide rollers hold the coil vertical. For narrow coils with high height-to-width ratios, an optional overhead pneumatic top hold-down roller prevents tipping during cycle start-up.
- Perimeter Guarding & Interlocks: Standard setups include a fixed structural yellow steel frame covering the upper drive ring segment. Automatic cells feature Category 4 / PLe safety light curtains across the load opening or interlocked access doors that trigger an instant emergency ring stop if breached.
- Controls & Jogging: Operators use a low-speed jog mode to safely thread film tails. CE-compliant models include standard mushroom-head emergency stop buttons and lockable main disconnect switches (OSHA LOTO compliant).
Engineering Frequently Asked Questions (FAQ)
Q: Can a single FPH machine run both large agricultural hoses and small electrical conduits? A: Yes, as long as both coil sizes fit within the certified inner diameter (ID), outer diameter (OD), and width ranges. Side guide rollers adjust quickly via handwheels, and inverter presets save specific ring-to-roller speed ratios for different products.
Q: How do you prevent lightweight coils from lifting out of the cradle rollers? A: Very light plastic coils (under 10 kg) can experience lift from the upward pull of the film carriage. We manage this by soft-starting the ring via the VFD and using an optional overhead, spring-loaded hold-down roller to keep the coil seated on the lower drive rollers.
Q: Can the machine handle VCI crepe paper or woven HDPE tape instead of stretch film? A: Yes. The orbital film carriage can be fitted with core adaptors and mechanical band brakes sized for non-stretch woven PP tape, VCI moisture-barrier paper, or micro-perforated agricultural stretch wrap.
Q: Which regulatory safety documents accompany the system? A: European Union shipments include a Declaration of Conformity to the Machinery Directive 2006/42/EC, harmonized under EN 415-10 and ISO 12100:2010, along with a complete electrical schematic manual compliant with EN 60204-1.
Application Engineering & Direct Inquiry Protocol
To evaluate an FPH vertical orbital wrapping configuration for your extrusion line:
- Provide Technical Parameters: Email your minimum/maximum coil ID, OD, axial width, maximum coil weight, and target cycles per hour to: info@fhopepack.com.
- Review Machine Sizing Analysis: Our engineering team will calculate kinematic overlap parameters, choose between the FPH-200 and FPH-300N platforms, and confirm required options (such as hold-down rollers, wide film carriages, or auto-cut units).
- Receive Application Quotation: We provide a formal technical proposal, dimensional footprint drawings, and a budgetary quote within 24 business hours.
الأنظمة ذات الصلة ومصادر إضافية للقراءة
- Hose Wrapping Machine FPH-300N (Product Catalog)
- Compact Hose Coil Wrapper FPH-200 Series
- Video: Automatic Hose Coil Wrapping Machine FPH-300
- Video: Flexible Corrugated Pipe Rolls Orbital Packing
- Video: Heavy-Duty HDPE Pipe Coil Packaging Solutions
Engineering Sources and References
- FHOPE Packaging Machinery System Specifications: FPH Series Orbital Eye-Through Wrappers.
- Engineering Kinematics: Orbital toroidal layer deposition and circumferential speed differentials.
- Machinery Safety Standards: EN 415-10 (Wrapping Machinery Safety Rules); ISO 12100:2010 (Basic Concepts and Risk Assessment Principles); EN 60204-1 (Safety of Machinery – Electrical Equipment of Machines).
Document Revision: 2.1 | Field Application Review Date: 2026-10-18