ملخص تنفيذي
Pipe coil wrapping and strapping work as a pair. The coiler winds a fixed length of pipe and straps it so the coil holds its shape; the wrapper then seals the strapped coil in film. The two machines must be sized together, because a coil the coiler can make is not always a coil the wrapper can take. Our FCL coilers cover pipe OD 4–63 mm, and our upright FPH-300N wrapper takes coils up to 1,000 mm OD and 300 mm wide.
This upright ring wrapper sits behind an orange guard frame. The operator guides a large coil and its white wrapping material into the ring, and the ring then runs the wrap while the coil turns on the support rollers.
جدول المحتويات
- Why pipe coils are strapped and then wrapped
- The coil-strap-wrap sequence
- Coiler sizes: FCL automatic pipe coiling range
- Wrapper limits: FPH-300N
- Worked example: matching coiler and wrapper
- قائمة التحقق من الاختيار
- السلامة: EN 415-10 و ISO 12100
- أسئلة وأجوبة هندسية
- الخطوة التالية
- القراءة ذات الصلة
- مصادر
Why pipe coils are strapped and then wrapped
Straps and film do different jobs. Straps carry the load: they stop a springy pipe coil from opening when it is lifted, stacked or dropped onto a pallet. Film carries the protection: it keeps dust, UV and moisture off the pipe and keeps the straps from cutting into the outer turns.
The order is strap first, wrap second. A coil wrapped before strapping can open inside the film. Strapping first holds the shape, and the film then goes on over a stable coil.
The coil-strap-wrap sequence
- لفه. The coiler counts the pipe length, cuts it and winds it onto the coiling head.
- حزام. Straps are placed through the coil eye at set points round the coil. The number of straps is set in the PLC.
- تحويل. The strapped coil leaves the coiler and is moved to the wrapper, by hand or by conveyor; the transfer method is set in the layout and confirmed at quote.
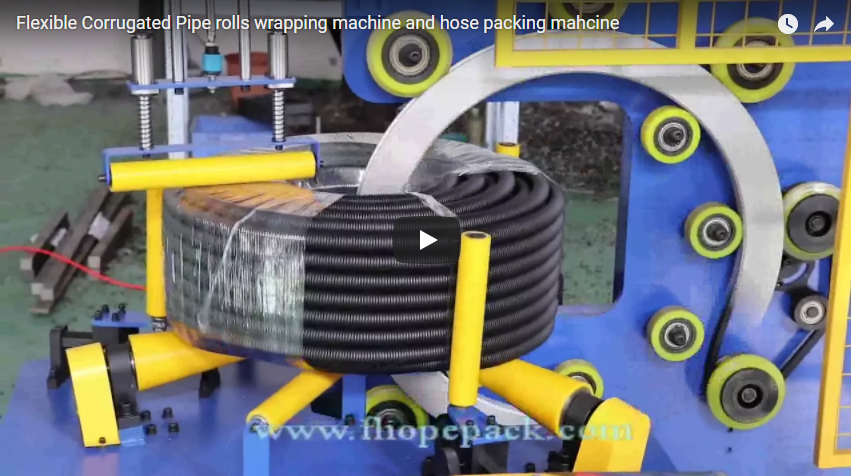
- التفاف. The coil stands on the wrapper rollers with the ring through its eye, and the ring wraps it in film.
- Label and stack. The wrapped coil is labelled and palletised.
For reference, our FPCL-W500 wire coiling and strapping machine uses 8–10 mm PP strap, 0.8 mm thick, with a friction-welded joint at the front of the coil that holds about 75–80% of the strap breaking load. The strap and strapping head on an FCL pipe coiler are confirmed at quote for your coil.
Coiler sizes: FCL automatic pipe coiling range
The FCL range covers pipe OD 4–63 mm across six models.
| الموديل | الأنابيب OD | لفائف معرف | لفائف OD | عرض لفائف |
|---|---|---|---|---|
| FCL100 | 4 – 12 مم | سماكة 150 ملم | سماكة 300 ملم | سماكة 150 ملم |
| FCL200 | 8 – 28 مم | 200 – 400 مم | سماكة 650 ملم | سماكة 200 ملم |
| FCL400 | 6 – 25 مم | 300 – 500 مم | 680 – 1,200 مم | سماكة 250 ملم |
| FCL600 | 8 – 28 مم | 380 – 600 مم | سماكة 1,050 ملم | سماكة 300 ملم |
| FCL800 | 12 – 32 مم | 490 – 860 مم | سماكة 1,200 ملم | سماكة 350 ملم |
| FCL1000 | 20 – 63 مم | 600 – 1,300 مم | سماكة 1,600 ملم | سماكة 400 ملم |
Wrapper limits: FPH-300N
| العناصر | طراز FPH-300N |
|---|---|
| لفائف معرف | 300 – 700 مم |
| لفائف OD | 500 – 1,000 مم |
| عرض لفائف | 100 – 300 مم |
| الوزن فائف | 10-100 كجم |
| دورة | 23-35 ثانية لكل لفة |
| سرعة الرنين | تصل إلى 120 دورة في الدقيقة |
| الطاقة | 1.9 kW, 380 V 60 Hz 3 ph |
Notice that the larger coilers make coils wider or bigger than 1,000 mm OD and 300 mm width. Those coils need a larger wrapper, confirmed at quote. The FPH-300N takes film rolls 90–100 mm wide on a 50 mm core, with speed, overlap rate and film tension all adjustable.
Worked example: matching coiler and wrapper
Take 100 m of 32 mm PE pipe on an FCL800 with a 600 mm coil ID.
| خطوة | عملية حسابية | نتيجة |
|---|---|---|
| Full FCL800 width | 350 32 ÷ | 10 turns per layer, 320 mm wide |
| Wrapper width check | 320 mm vs FPH-300N 300 mm max | واسع جدًا |
| Set 9 turns per layer | 9 × 32 | 288 مم واسعة |
| Layer 1 (mean 632 mm) | 9 × π × 0.632 | 17.9 م |
| Layers 1–4 | 17.9 + 19.7 + 21.5 + 23.3 | 82.4 م |
| Layer 5 (part) | 100 - 82.4 | 17.6 م |
| لفائف OD | 600 + 2 × 5 × 32 | سماكة 920 ملم |
| Wrapper check | ID 600 ≤ 700; OD 920 ≤ 1,000; width 288 ≤ 300 | نوبات |
تنظيم السرعة. Our coiling and strapping lines are offered with a pay-off and accumulator and run at up to 45 coils per hour, which is 80 s per coil. The FPH-300N needs 23–35 s per coil, so the wrapper keeps up with spare time for transfer.
نتيجة. Run at full width, the coiler makes a 320 mm coil that the FPH-300N cannot take. Setting the coiler to 9 turns per layer gives a 288 mm wide, 920 mm OD coil that both machines handle. Weigh one coil to confirm it is within 100 kg, since pipe weight per metre depends on wall thickness.
قائمة التحقق من الاختيار
- Pipe OD, wall thickness and length per coil.
- Coil ID, OD and width the market expects.
- Coils per hour from the extruder.
- Number of straps and strap material.
- Wrap material, overlap and labelling.
- Transfer between coiler and wrapper: manual or conveyor.
السلامة: EN 415-10 و ISO 12100
Both machines are built to EN 415-10 with interlocked guards, the general safety requirements for packaging machines, with the risk assessment done to ISO 12100. Guard frames cover the wrapping ring and the coiling head, and coils are positioned before each cycle starts.
أسئلة وأجوبة هندسية
Q: Why strap before wrapping? A: Straps hold the coil shape so it cannot open inside the film.
Q: Can one coiler feed one wrapper? A: Yes, if the coil sizes match. The coil width and OD must stay inside the wrapper range.
Q: What strap does the coiler use? A: PP strap is standard on our coiling and strapping lines. The strap size for an FCL pipe coiler is confirmed at quote; on our FPCL-W500 wire coiler it is 8–10 mm PP, 0.8 mm thick.
Q: How long does the FPH-300N take per coil? A: 23–35 s per coil.
الخطوة التالية
- Send your pipe OD, coil length and coil size إلى info@fhopepack.com.
- نحن نطابق the coiler and wrapper as one system.
- نقوم بالرد خلال 24 ساعة مع تصميم وتسعير.
القراءة ذات الصلة
- آلة لف وربط الخراطيم (المنتج)
- Hose wrapping machine FPH-300 (product)
- ماكينة لف وربط الخراطيم ذات الجدار المزدوج
- آلة لف وربط الأنابيب الأوتوماتيكية
مصادر
- FHOPE product pages: hose coiling and strapping machine (FCL); hose wrapping machine FPH-300N; FPCL-W500 coiling and strapping machine
- FCL400 coil ID and OD as confirmed by our engineering team
- EN 415-10؛ ISO 12100:2010
آخر مراجعة: 2026-10-19