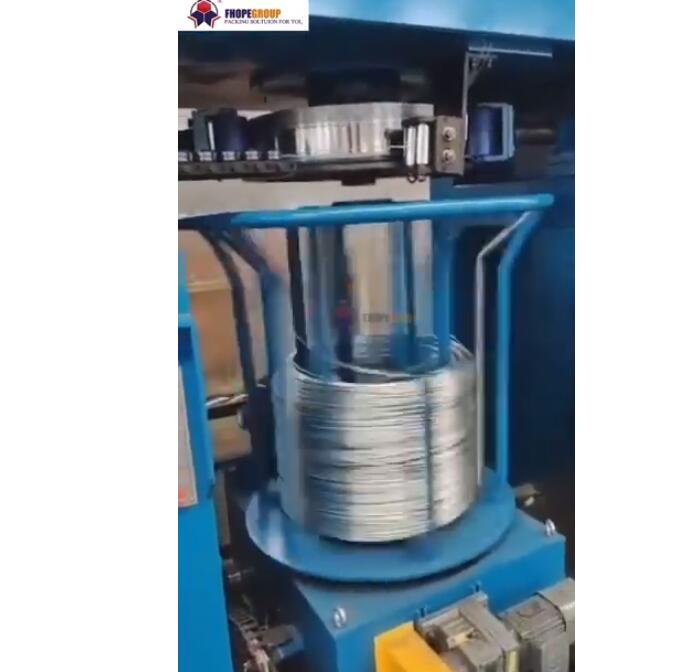
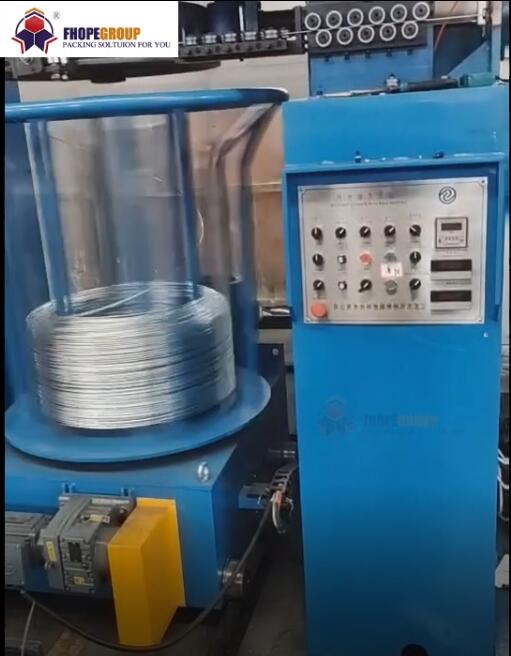
执行摘要 An automated steel wire coil winding and strapping machine winds drawn high- or low-carbon steel wire to a pre-set length, performs precision shear cutting, and secures the finished bundle with automated through-the-eye strapping. The integrated workcell synchronizes a collapsible star-type coiling head with a servo-driven coil transfer unit and an automatic friction-welding strapping head. Operating with 8 to 10 mm PP strapping (2 to 4 strap placements per bundle), the system achieves consistent radial compression, protects wire surface integrity, and eliminates manual handling hazards at continuous line speeds.
目录
- Operational Sequence and Process Breakdown
- 周期时间分析
- System Architecture and Kinematic Workflow
- Wire Coil Strapping Technical Specifications
- Line Takt Synchronization
- 工程选型清单
- 控制架构和安全合规性
- 工程常见问题解答
- 工程咨询及后续步骤
- Related Wire Packaging Systems
- 技术参考
Operational Sequence and Process Breakdown
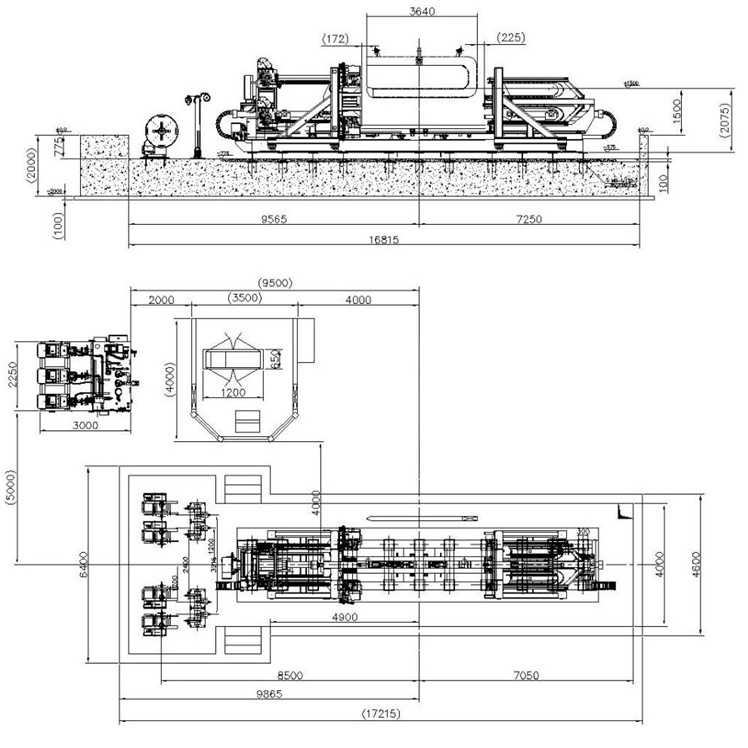
The automated cell is engineered within a perimeter safety enclosure with an interlocked entry gate, housing an automated coiling head driven by a geared motor, dynamic guide arms, a two-axis servo coil transfer manipulator, and a separate through-the-eye strapping module governed by a central PLC panel.
+---------------------------------------------------------------------------------+
|                             Continuous Drawing Line                             |
+---------------------------------------------------------------------------------+
                                         |
                                         v
+---------------------------------------------------------------------------------+
|                    Dual-Roller Length Counter & Wire Clamp                      |
+---------------------------------------------------------------------------------+
                                         |
                                         v
+---------------------------------------------------------------------------------+
|         Collapsible Star Capstan (Winding, Layer Traverse & Flying Shear)        |
+---------------------------------------------------------------------------------+
                                         |
                                         v
+---------------------------------------------------------------------------------+
|               Servo Coil Transfer Manipulator (Lift, Index, Place)              |
+---------------------------------------------------------------------------------+
                                         |
                                         v
+---------------------------------------------------------------------------------+
|                Through-the-Eye Friction-Welding Strapping Station               |
+---------------------------------------------------------------------------------+
                                         |
                                         v
+---------------------------------------------------------------------------------+
|                     Discharge Chute / Unloading Turntable                       |
+---------------------------------------------------------------------------------+- Initial Standby & Verification (0 to ~18 s): The coiled bundle rests securely on the collapsed capstan while downstream interlocks verify the ready state of the strapping module.
- Transfer Manipulator Extraction (24 to ~42 s): The overhead servo gripper lowers onto the finished coil, establishes radial clamping, extracts the bundle from the collapsed core segments, and traverses to the secondary packaging station.
- Leading-End Feeding & Guiding (48 to ~54 s): The wire lead is directed through precision guide rollers onto the expanded capstan clamp, and auxiliary guide arms close to secure the first active turn.
- Controlled Acceleration & Flying Cut (60 to ~78 s): The coiling head accelerates smoothly to set winding speed. Upon reaching target meterage, the integrated hydraulic/pneumatic shear cuts the wire cleanly while the tail wraps flush.
- Station Clearance (approx. 84 s): The finished coil completes index transfer at the offload station, leaving the coiling head cleared for the next continuous cycle.
- Station Dwell & Intermediate Indexing (90 to ~102 s): The intermediate transfer arm holds position, ensuring mechanical stabilization and zero-backlash alignment before gripping.
- High-Speed Continuous Winding (108 to ~174 s): The capstan executes an extended winding profile with synchronized traverse pitch, building regular coil layers from inner diameter to final outer diameter.
- Automated Bundle Extraction (180 to ~198 s): The transfer gripper re-engages, contracts radial jaws to clamp the finished coil eye, and lifts it smoothly from the mandrel.
周期时间分析
| 过程阶段 | 时间线窗口 | Elapsed Duration | Motion & Mechanical Function |
|---|---|---|---|
| Coil Extraction & Transfer | 24 到约 42 秒 | 18〜HK | Servo carriage unloads core; traverses to strapping station |
| Lead Wire Feed & Clamp | 48 到约 54 秒 | 6〜HK | Guide arms engage; leading end locks into capstan clamp |
| Winding & Cut (Coil 1) | 60 到约 78 秒 | 18〜HK | Short-cycle test/sample wind, continuous shear, tail flush |
| Winding Cycle (Coil 2) | 108 到约 174 秒 | 66〜HK | Production winding profile under closed-loop tension control |
| Bundle Lift & Offload | 180 到约 198 秒 | 18〜HK | Capstan collapses radially; transfer clamp secures coil |
Note: Data reflects typical line sequencing observed across video intervals. Operational cycle times scale directly with incoming line speed (m/min), wire gauge, and programmed bundle mass.
How the Winding and Strapping Machine Works
Wire Infeed ---> [ Encoder Wheel ] ---> [ Wire Clamp ] ---> [ Collapsible Capstan ]
                        |                                            |
                  (PLC Counter)                                (Servo Wind)
                        |                                            |
                        +------------> [ Flying Shear ] <------------+
                                             |
                                    [ Transfer Gripper ]
                                             |
                                             v
                             [ Through-the-Eye Strapping Head ]
The wire enters via a precision dual-roller measurement counter. Encoder feedback measures line linear distance to millimetre accuracy, transmitting pulse counts directly to the PLC to trigger coiling ramp-down and flying cut sequences. Integrated anti-reverse bearings prevent spring-back tension loss during pauses.
The collapsible coiling capstan moves through programmed expansion and contraction strokes: expanding to define the coil inner diameter (ID) during winding, and collapsing radially to ensure frictionless bundle release. An AC servo drive regulates rotational speed and winding traverse to produce uniform layers. Once target length is verified, the cutter executes a shear cut.
A servo-driven transfer carriage equipped with expanding inner-eye jaws then extracts the coil and moves it to the automated strapping station. At this point, a reciprocating track feeds PP strap through the coil center (eye), applying adjustable tension and friction-welding the joint in 2 to 4 radial positions.
| 子系统 | 主要工程职能 | 技术机制 |
|---|---|---|
| Precision Meter Counter | Measures linear wire feed with closed-loop precision | Dual hardened alloy encoder rollers + anti-rollback bearing |
| Collapsible Coiling Head | Sets inner diameter, clamps wire lead, and collapses for release | Pneumatically/hydraulically expanded segmented star segments |
| High-Speed Flying Shear | Cuts high-tensile wire cleanly at target count | Hardened alloy tool-steel blade with pneumatic/hydraulic actuator |
| Servo Transfer Gripper | Extracts coil from capstan and indexes to strapper | Two-axis servo positioning frame with multi-point coil ID clamps |
| Through-the-Eye Strapping Head | Secures coils radially through the inner core | Automatic feed sword, tensioning track, and friction-weld head |
| PP Strap De-reeler & Accumulator | Feeds strapping material smoothly without snagging | Dynamic motorized dancer-arm accumulator and tension brake |
Wire Coil Strapping Technical Specifications
| 参数 | 规格 | Notes / Operating Range |
|---|---|---|
| Compatible Strap Material | Polypropylene (PP) / Polyester (PET optional) | Surface-embossed industrial packaging strap |
| 表带宽度 | 8.0 mm至10.0 mm | Standard tool configuration |
| 表带厚度 | 0.8毫米(标称) | ±0.05 毫米公差 |
| 密封方式 | High-frequency friction welding | No metal seals; clean heat-bonded joint |
| Joint Tensile Efficiency | 75% to 80% of parent strap breaking strength | Fully cooled and set under mechanical pressure |
| Strapping Placements | 2, 3, or 4 radial straps per coil | Selected via HMI recipe (90° or 180° indexing) |
| 肩带张力范围 | 200 牛顿至 2,500 牛顿 | Digitally adjustable via servo drive / clutch |
| System Control Platform | 工业PLC(西门子/三菱兼容) | Central touchscreen HMI with recipe memory |
Through the operator HMI, technicians configure acceleration ramps, linear wire cut targets, strap placement sequences, and diagnostic warning limits. Recipe profiles permit fast changeovers between wire diameters, bundle weights, and packaging specs during scheduled product transitions.
Line Takt Synchronization
In a wire drawing and processing facility, downstream packaging cycle time must match or exceed continuous upstream output to prevent accumulator overflow:
Continuous Drawing Line Takt: T_line = Target Cycle Time per Coil (e.g., 120 s)

Total Packaging Cycle Time:
T_total = T_wind + T_shear + T_transfer + T_strap

Downstream Interlock Condition:
T_strap ≤ T_wind (when running parallel buffer stations)
Where the packaging cell operates with independent winding and strapping stations, the transfer manipulator decouples the coiler from the strapping cycle. While Coil N is being strapped (2 to 4 cycles, requiring approximately 8 to 12 seconds per strap placement including rotation), Coil N + 1 is actively winding on the capstan. As long as total strapping and offload time remains below the winding duration, packaging will not bottleneck upstream drawing lines.
工程选型清单
- Wire Gauge & Metallurgy: Exact wire diameter (mm), material grade (low/high carbon, galvanized, stainless), and tensile strength range (MPa).
- 线圈尺寸和重量: Target coil inner diameter (ID), maximum outer diameter (OD), coil width/height, and bundle mass (kg).
- 上游线路速度: Continuous linear speed from the drawing bench or bullblock (m/min or m/s).
- 捆扎要求: Number of radial straps per coil (2, 3, or 4 straps) and material preference (PP vs. PET).
- Downstream Logistics Interface: Offloading destination—gravity discharge chute, walking beam conveyor, C-hook crane pick-up, or automated palletizing cell.
控制架构和安全合规性
The winding and strapping cell involves high rotational inertia, sharp wire leads, high-force shear blades, and automated transfer axes. Operator safety is designed directly into the control hardware:
- Physical Guarding & Interlocking: Industrial perimeter wire-mesh fencing fully encloses moving axes. Access doors are fitted with dual-channel tongue-type interlock switches or RFID safety switches conforming to ISO 12100 和 ZH-415 10的.
- 上锁/挂牌(LOTO)合规性: Dedicated, lockable isolation valves for pneumatic supply and main circuit breaker disconnects are provided for maintenance, re-threading, and strap spool replenishment.
- Fail-Safe Control Architecture: Emergency stop circuits are routed through certified safety relays (Category 3 / Category 4, Performance Level d/e per ISO 13849-1), cutting actuator power and dropping capstan motor brakes instantaneously upon tripped conditions.
工程常见问题解答
Q: How does the cut-off mechanism maintain exact coil lengths? A: A high-resolution dual-wheel rotary encoder rides directly on the infeed wire, sending pulses to a high-speed PLC counter module. Once the target length is met, the system modulates coiling speed, holds tension, and fires the high-speed flying shear, ensuring repeatability within ±0.1% to ±0.3% of total length.
Q: Can the machine handle different coil inner diameters (ID) on the same head? A: Coiling head segments are engineered for a standard expansion range (e.g., standard stroke of 30 mm to 50 mm for coil release). Accommodating radically different coil core diameters requires changing the segmented star capstan plates, which are modular and quick-detachable.
Q: What is the tensile integrity of the friction-welded strap joint? A: The friction-welded overlap retains approximately 75% to 80% of the nominal breaking strength of 8–10 mm industrial PP strap. The process provides reliable bundle retention without the cost, scratch risks, or rust susceptibility of steel crimp seals.
工程咨询及后续步骤
To evaluate an automated coiling and strapping unit for your drawing or finishing line:
- 提交行参数: Send your wire diameters, minimum/maximum coil weights, production line speeds, and factory layout to info@fhopepack.com.
- 48小时内完成技术方案: Our mechanical design team provides a complete line proposal, including general assembly (GA) drawings, cycle time calculations, and strap configuration plans.
- Engineering Site Review & Integration: Work with our project engineers to verify electrical bus tie-ins, safety guarding boundaries, and downstream coil transfer integration.
Related Wire Packaging Systems
- Horizontal Steel Wire Winding and Strapping Machine
- Automatic Wire Coiler & Spooling Systems
- Automatic Wire Coil Compacting and Strapping Solutions
技术参考
- Technical Data & Machine Specifications: FHOPE Steel Wire Winding and Strapping Production Line
- 视频演示: Steel Wire Coil Winding and Strapping Machine in Operation (YouTube)
- 安全与机械标准: ISO 12100:2010 (Safety of Machinery — General Principles for Design), EN 415-10:2014 (Safety of Packaging Machines — Part 10: General Requirements)
上次审核日期: 2026年10月05日
最后更新时间: 2026年10月29日