> **Povzetek**
>
> An automatic nodular cast iron pipe strapping line counts finished pipes, forms them into a tight bundle and steel-straps the bundle at several points along its length. Ductile iron pipe is heavy and its coating and spigot ends are easy to damage, so the bundle must be tight and the pipes must not roll against each other. This page covers the line steps, strap and tension sizing, strap length and what to check before you buy.
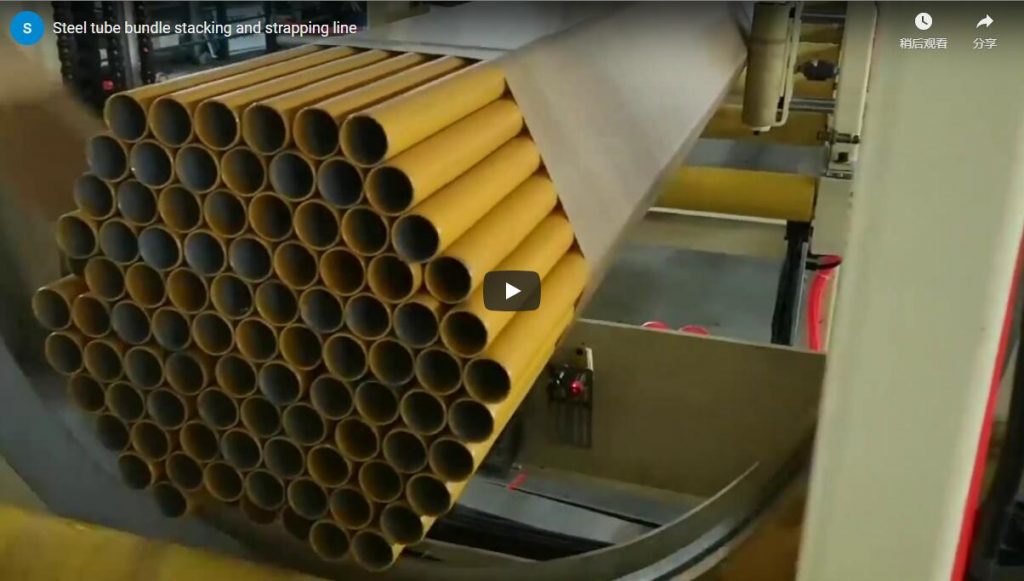
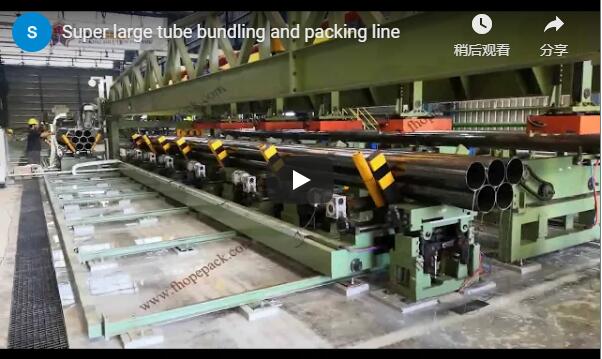
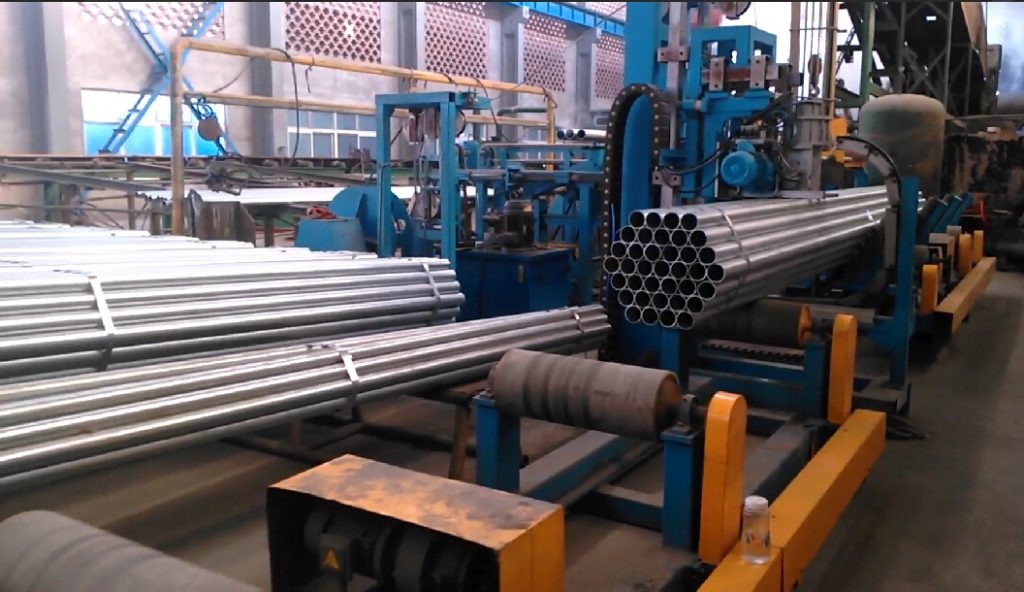
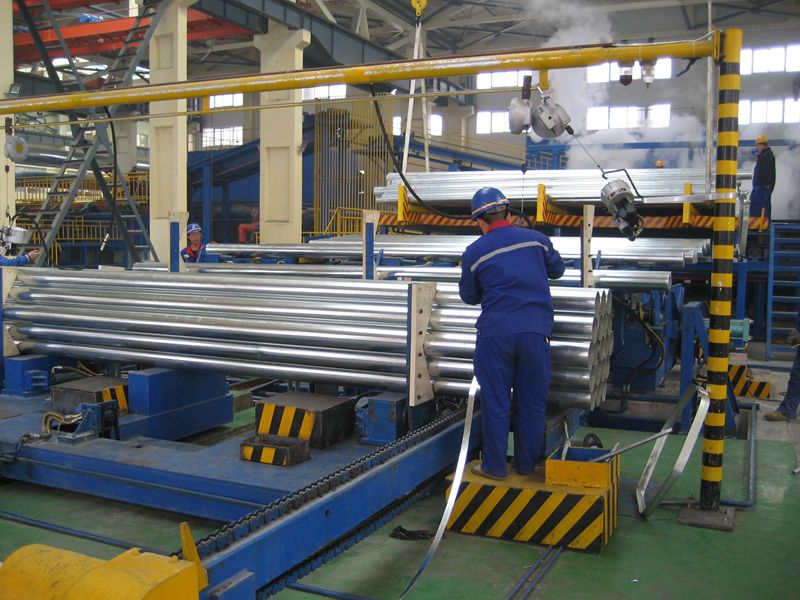
Pipe bundles with red and blue end caps move on blue roller and V-support conveyors into a yellow strapping arch. The head places steel straps around the bundle at each position, while the gantry and guard rails keep people outside the moving zone.
Kazalo
- Why bundle and strap ductile iron pipe
- The line steps
- Strapping machine specifications
- Strap length and feed time
- How many straps per bundle
- Kontrolni seznam za izbiro
- Varnost
- Pogosta vprašanja o inženirstvu
- Naslednji korak
- Sorodno branje
- Viri
Why bundle and strap ductile iron pipe
Smaller-bore ductile iron pipe ships in bundles so cranes and trucks handle one unit, not dozens of loose pipes. Loose pipes roll, chip their coating and dent their spigots. A counted, formed bundle with steel straps stays tight from the mill to the trench. End caps keep dirt and damage away from the pipe bore and joints.
The line steps
1. **Load and align:** single pipes roll into the storage area; a striker plate sets the end position.
2. **Count:** a kick-out device moves pipes one by one to the layer bench, and a photoelectric cell counts each one.
3. **Form:** counted layers drop into a forming bed shaped to the bundle, and stoppers clamp the bundle tight.
4. **Strap:** the strapping machine stays still while the bundle moves to each strap position along its length.
5. **Out:** the strapped bundle goes to the stacking or loading area.
The line runs from a touch-screen station in automatic, semi-automatic or manual mode.
Strapping machine specifications
| Item | Automatic steel strapping machine |
| :--- | :--- |
| Strap | cold-rolled low-carbon steel, blued and waxed |
| Strap width | 25 or 32 mm |
| Strap thickness | 0.8 or 1.0 mm |
| Napetost traku | 7,000–18,000 N |
| Seal | notch type; double seal notch on bundle machines |
| Seal magazine | approx. 180 seals |
| Feed and take-up | 2–3 m/s |
| Tension speed | 6 m/min |
| Hydraulics | 100 bar, working 80–90 bar, water-cooled oil |
| Trakovi na snop | 5 do 7 |
Your bundle sizes and strap pattern are confirmed at quote.
Strap length and feed time
**Strap length around a hexagonal bundle = 6 × (pipes per side − 1) × pipe OD + π × pipe OD.** A 19-pipe bundle has 3 pipes per side. For a 100 mm OD pipe: 6 × 2 × 100 + π × 100 = 1,200 + 314 = 1,514 mm per strap (example only). At 2 m/s feed, that strap is fed in 1.514 ÷ 2 = 0.76 s, so the cycle time is set by tensioning and sealing, not by feeding.
How many straps per bundle
**Straps = bundle length ÷ strap pitch + 1.** A 6 m bundle strapped every 1.2 m needs 6 ÷ 1.2 + 1 = 6 straps, inside the 5 to 7 range of our bundle machines (example only). **Sockets and spigots.** A socket (bell) end is larger than the pipe body, so bundles of socket pipe are usually formed with sockets alternating end to end; the bundle then stays parallel and straps bear on the pipe body, not the bells. The forming bed and strap positions are set per pipe drawing.
**Joint and coating.** On our heavy steel-strap quotations the seal joint holds about 75% of the strap breaking force, so size the strap for the bundle weight with that margin. Where straps bear on coated pipe, cardboard or plastic edge protectors go under the strap; we offer automatic protector applicators on our coil strapping lines, and the option for pipe is confirmed at quote.
Put the first and last straps close to the pipe ends, where bundles spring open first, and keep the bundle centre on the conveyor centre so each strap sits square.
Kontrolni seznam za izbiro
1. Pipe DN, OD and length range?
2. Pipes per bundle and bundle shape?
3. Strap width, thickness and number of straps?
4. Coating type (zinc, bitumen, polyurethane or other), and need for edge protection under straps?
5. Line output in pipes per hour?
6. Crane, stacking or truck loading after strapping?
Varnost
The line is designed to EN ISO 12100:2010 for risk assessment, EN 415-10 for packaging machine safety and EN 60204-1 for electrical equipment. Moving bundles, the strapping arch and hydraulic tensioning are the main hazards, so the line is fenced with guard rails and signs, and access is through interlocked gates with emergency stops.
Pogosta vprašanja o inženirstvu
Q: What strap does the line use?
A: Steel strap, 25 or 32 mm wide and 0.8 or 1.0 mm thick.
Q: How tight is the strap?
A: 7,000–18,000 N, adjustable to the bundle.
Q: How are pipes counted?
A: A photoelectric cell counts each pipe as it is kicked onto the layer bench.
Q: Does the bundle move or the strapper?
A: The strapping machine is stationary; the bundle moves to each strap position. A stationary head keeps the heavy hydraulics fixed and simple; a travelling head suits bundles that should not move, and is confirmed per project.
Naslednji korak
1. **Send your pipe sizes, lengths, bundle pattern and output** to info@fhopepack.com.
2. **We size** the counting, forming and strapping stations.
3. **Odgovorimo vam v 24 urah** s predlogom in ponudbo.
Sorodno branje
- [Automatic steel tube strapping machine (product)](https://www.fhopepack.com/Automatic-Steel-Tube-Packing-Line/Automatic-steel-tube-strapping-machine.html)
- [Automatic steel pipe bundling and strapping machine](https://www.fhopepack.com/videos/automatic-steel-pipe-bundling-and-strapping-machine/)
- [Steel tube bundle strapping machine (product)](https://www.fhopepack.com/Steel-tube-strapping-machine/steel-tube-bundle-strapping-machine.html)
Viri
- FHOPE product pages: automatic steel tube strapping machine; steel tube bundle strapping machine; automatic steel pipe bundle packing line
- EN ISO 12100:2010; EN 415-10; EN 60204-1
- The pipe bundle strapping line shown above
Zadnji pregled: 20. 10. 2026