Rezumat In high-capacity steel wire manufacturing plants, decentralizing the finishing process into multiple parallel strapping lines provides higher operational resilience and lower logistics friction than relying on a single centralized system. Steel wire coils travel along dedicated live roller conveyors through automated strapping stations that compress and radially strap each coil before advancing it to discharge staging. Because modern wire drawing mills operate clusters of high-speed drawing machines, allocating one automated strapping line to serve each production group eliminates plant-wide bottlenecks and maintains continuous uptime.
Cuprins
- How the Lines Run: Layout and Station Sequence
- De ce atâtea linii scurte
- Câte linii
- Ce am stabilit pentru fiecare plantă
- Listă de verificare a selecției
- Siguranţă
- Întrebări frecvente despre inginerie
- Urmatorul pas
- Citire conexă
- Surse
How the Lines Run: Layout and Station Sequence
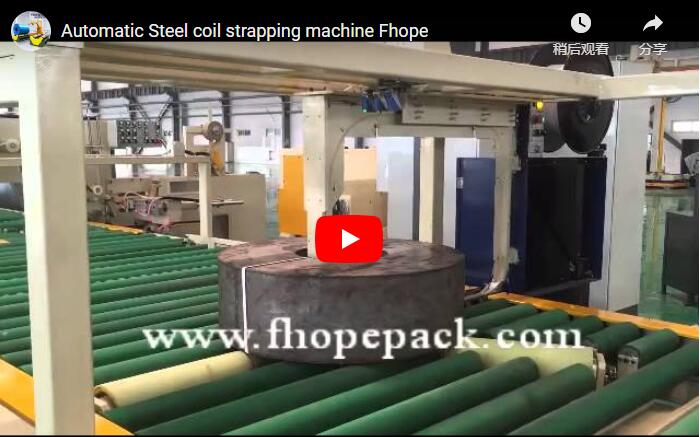
A parallel plant layout distributes heavy wire coils across compact, dedicated handling lanes running adjacent to specific drawing blocks. Each automated line executes a four-stage packaging sequence designed to eliminate manual intervention and protect wire surface integrity:
| Etapa procesului | Equipment & Motion Sequence | Specificații tehnice |
|---|---|---|
| 1. Infeed & Buffer | Wire coils are transferred directly from drawing machine payoff carousels onto the line infeed. | Buffers intermittent mill output; supports coil weights from 30 kg to 6,500 kg+ [manufacturer rating]. |
| 2. Powered Conveying | Motorized live roller conveyors transport coils axially into the strapping envelope. | Contact surfaces feature high-durability polyurethane (PU) coating to prevent scratching on galvanized and bright wire [manufacturer rating]. |
| 3. Legătura automată | Indexing strap chutes pass strap through the coil eye (circumferential/radial banding) under tension. | Individual strapping action completes in ≤35 s/cycle [manufacturer rating]; Siemens S7 PLC controls indexing and multi-strap sequences. |
| 4. Outfeed & Staging | Strapped coils advance to discharge conveyors for automated labeling, weighing, or forklift collection. | Inline integration with high-precision load cells (1/3000 resolution) and automated thermal transfer tag printers [manufacturer rating]. |
De ce atâtea linii scurte
- Trasee scurte. Each line sits directly beside its assigned group of wire drawing machines, minimizing crane transport, internal forklift travel, and floor congestion.
- Niciun punct de sufocare unic. Because lines operate independently, maintenance, strap coil reloading, or mechanical downtime on one strapping station does not interrupt the rest of the plant.
- Design comun. All parallel lines share identical mechanical drives, pneumatic actuators, wear components, and strapping head assemblies, drastically reducing spare parts inventory.
- Creștere pas cu pas. Capital expenditure scales alongside plant expansion; additional modular strapping lines can be installed sequentially as new drawing machines come online.
- High payload handling. Standard modules accommodate industrial wire coils with outer diameters (OD) of 500–1500 mm, inner diameters (ID) of 300/508/610 mm, and axial widths of 20–500 mm [manufacturer rating] (compatible with master coils up to 4,000 kg managed by companion handling systems [manufacturer rating]).
Câte linii
The total number of packaging lines required is determined by matching the collective throughput of the wire drawing facility against the operational cycle rate of an individual strapping line.
Exemplu lucrat (ilustrativ).
| Articol | Valoare |
|---|---|
| Producția instalației (cu titlu ilustrativ) | 600 de bobine pe oră |
| O linie de legare (cu titlu ilustrativ) | 80 de bobine pe oră |
| Linii necesare, 600 ÷ 80 | 7.5, deci 8 linii |
| Bobine pe linie la 8 linii, 600 ÷ 8 | 75 de bobine pe oră |
| Greutatea bobinei (cu titlu ilustrativ) | 1,000 kg |
| Tone pe linie, 75 × 1,000 kg | 75 tone pe oră |
Engineering note on cycle rates: While a single automated strapping head executes a single strapping band cycle in ≤35 seconds [manufacturer rating], full-line operational throughput typically ranges from 20 to 40 coils per hour per line depending on the number of straps applied per coil (e.g., 2, 3, or 4 radial bands), coil rotation time, and upstream feeding automation [manufacturer rating]. The illustrative 80 coils/hour rate above reflects dedicated single-strap configurations or dual-head tandem operations.
Ce am stabilit pentru fiecare plantă
Every line is tailored to plant layout boundaries, metallurgical surface requirements, and logistical handling methods:
| reglaj | Depinde de | Factory Configuration Range |
|---|---|---|
| Curele per bobină | Coil weight, handling dynamics, and export transport | 2, 3, or 4 radial straps through the coil eye; programmed via 12–15″ touchscreen HMI. |
| Material curea | Wire tensile strength and transport shock loads | Heavy-duty PET strap (friction-weld joint efficiency ≈75%–80%) or high-tensile steel strap (notch or sealless joint). |
| Tip transportor | Coil OD, ID, face width, and floor layout | Polyurethane (PU)-lined steel rollers, V-shaped roller beds for horizontal eye coils, or flat slat conveyors. |
| Număr de linii | Total mill tonnage and drawing cell arrangement | Scaled based on plant output and drawing machine clustering to optimize floor pathways. |
Listă de verificare a selecției
Ensure the following operational parameters are specified before finalizing line engineering:
- Coil physical dimensions: Minimum and maximum Outer Diameter (OD), Inner Diameter (ID), and Face Width (mm).
- Coil mass: Net and gross weight range (kg per coil).
- Required straps per coil: 2, 3, or 4 radial bands through the core.
- Peak plant output: Coils per hour and total metric tonnes per shift.
- Machine allocation: Number of drawing machines feeding into each strapping group.
- Floor layout & envelope: Available floor length, ceiling crane clearance, and infeed transfer method.
- Strap specification: Polyester (PET) vs. high-tensile steel strap (strap width and thickness).
- Ambient conditions: Standard plant environment (-10 °C to +45 °C) [manufacturer rating].
Siguranţă
High-tension wire packaging systems incorporate comprehensive risk-reduction measures under international standards:
- Strapping head clearance: Personnel must maintain clear boundaries outside the machine guarding envelope while strapping heads and indexing strap chutes are in motion.
- Live conveyor isolation: Operators must never step onto motorized roller conveyors; walkways and crossovers must be utilized.
- Blocare/Etichetare (LOTO): Energy isolation protocols (electrical and pneumatic discharge) must be fully executed before clearing strap track blockages, servicing strapping heads, or reloading strap coils.
- Conformitate standard: Designed and built for CE compliance in accordance with ISO 12100: 2010 (Siguranța mașinilor — Principii generale de proiectare — Evaluarea riscurilor și reducerea riscurilor) și RO 415-10: 2014 (Siguranța mașinilor de ambalat — Cerințe generale).
Întrebări frecvente despre inginerie
Q: Why many short lines instead of one centralized packaging hub? A: Multiple short lines place the packaging station immediately adjacent to drawing machine cells. This eliminates long-distance coil transport, prevents a single machine stoppage from halting the entire mill, and allows modular expansion as plant capacity grows.
Q: How many strapping lines does our plant need? A: Divide your peak plant hourly output by the net hourly rating of a single strapping line (rounded up to the next integer). In the worked example above, 600 coils/hour divided by 80 coils/hour requires 8 parallel lines handling 75 coils/hour each.
Q: Should we specify PET or steel strapping? A: High-tensile PET is widely used for wire coils due to its constant retained tension, elastic shock absorption during transit, and lower consumable cost. Steel strap is selected for extremely heavy wire coils, sharp cut-edge products, or extreme high-temperature handling off the annealing line.
Q: Can additional strapping lines be added after commissioning? A: Yes. Because each parallel line operates as an independent automation island sharing standard electrical and mechanical architecture, new lines can be integrated without interrupting active lines.
Q: Do all parallel lines share the same spare parts? A: Yes. All lines utilize unified mechanical drives, PU rollers, strap dispenser carts, strapping head components, and Siemens PLC logic, minimizing warehouse inventory costs.
Q: Which machine safety standards govern this equipment? A: For CE and international markets, the design adheres to ISO 12100:2010 for mechanical risk reduction and EN 415-10:2014 for packaging machine safety.
Urmatorul pas
Our application engineering team provides custom layout integration and throughput modeling in three direct steps:
- Trimiteți desenul de machetă including coil dimensions (OD/ID/Width/Weight), peak plant output, and current factory floor drawings to info@fhopepack.com.
- Primiți o propunere tehnică oficială în termen de 48 de ore, complete with cycle time calculations, footprint models, and machine datasheets.
- Programează o inspecție a șantierului with our specialists to review line clearances, drawing mill integration points, and infeed logistics.
Citire conexă
- Linie de înfășurare, răsturnare și stivuire a bobinelor de sârmă de oțel
- Mașină de legat bare de armătură și tijă cu sârmă
- Mașină de înfășurare completă pentru rulouri mici
- Mașină de ambalat bobine
Surse
- Linie automată de ambalare a bobinelor de sârmă — FHOPEpack Engineering Specifications
- Big Wire Coil Wrapping Machine FPW-600 Series — System Integration Data
- Plant Throughput Calculation Model — Illustrative capacity planning example
- ISO 12100: 2010: Siguranța mașinilor — Principii generale de proiectare — Evaluarea riscurilor și reducerea riscului
- RO 415-10: 2014: Securitatea mașinilor de ambalat. Partea 10: Cerințe generale
- Official Turnkey Proposal Protocol (Standard 48-Hour Response SLA)
Ultima recenzie: 21.09.2026
Ultima actualizare: 01.06.2026