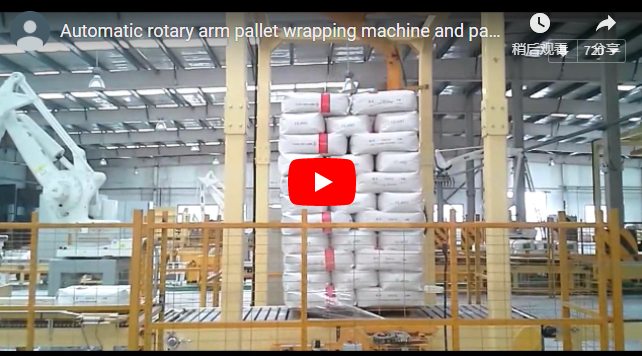
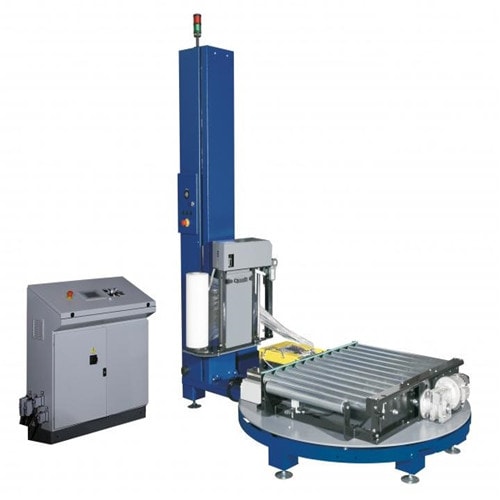
Sintesi Un'avvolgitrice automatica a tavola rotante elimina l'intervento manuale solo se gestisce in modo affidabile la coda del film. La B100 raggiunge un funzionamento completamente automatizzato grazie a un meccanismo pneumatico integrato di bloccaggio, taglio e pulizia: delle forbici meccaniche bloccano la coda del film prima della rotazione della tavola rotante, un filo riscaldante a impulsi taglia il film al termine del ciclo e una spazzola di pulizia elastica sigilla saldamente la coda contro la superficie del pallet. Progettata per un utilizzo industriale continuo, la B100 elabora carichi di pallet fino a 1,800 kg (con un 2,000 kg margine di sicurezza strutturale) a una portata di Oltre 24 carichi all'ora, dotato di un carrello di pre-allungamento motorizzato calibrato al 250% dello standard (regolabile dal 100% al 300%).
Sommario
- La sequenza di serraggio, avvolgimento, taglio e pulizia
- Tension Stability Decides Cut Reliability
- Powered Pre-Stretch Ratio and Film Consumption
- Turntable Dynamics and Line Integration Parameters
- PLC Control System and Program Architecture
- Utilities, Pneumatic Requirements, and Machinery Safety
- Lista di controllo per la selezione degli ingegneri
- FAQ tecnico
- Prossimo passo e protocollo di proposta rapida
- Related Systems and Normative Standards
La sequenza di serraggio, avvolgimento, taglio e pulizia
Il principale punto debole delle avvolgitrici di base è lo svolgimento della pellicola durante il trasporto. La B100 risolve questo problema grazie a un braccio meccanico pneumatico montato sul bordo che esegue quattro fasi coordinate:
| step | Meccanismo | Azione ingegneristica |
|---|---|---|
| Morsetto | Pinza pneumatica a forbice | Fissa il bordo anteriore della pellicola al perimetro del piatto girevole prima dell'inizio della rotazione, eliminando la necessità di fissarla manualmente. |
| Avvolgere | Piattaforma girevole motorizzata | Accelerates smoothly under VFD control, wrapping the unitized load according to programmed layer recipes. |
| taglio | Elemento a filo caldo a impulso | An electrical impulse heats the cutting wire instantly upon cycle completion, cleanly separating the web without blade wear. |
| pulire | Braccio con spazzole ad alta densità | Ruota dinamicamente rispetto alla superficie di carico rotante, lisciando e fissando la coda della pellicola sulla superficie del cartone pallettizzato. |
The clamping assembly retains the primary film tail after the wipe phase, locking the film in position so the system is immediately primed for the subsequent pallet without operator reloading.
Tension Stability Decides Cut Reliability
In fully automated stretch wrapping, the mechanical cutting action is inseparable from film web dynamics. An automated clamp-cut-wipe system fails when tension between the pre-stretch carriage and the load fluctuates out of tolerance.
The chain runs both ways. Pre-stretch surging leaves a loose web at the cut zone, so the thermal severing is incomplete; over-tensioning instead stores elastic energy that snaps back at the cut and pulls the tail out of the clamp, aborting the cycle.
- Snap-Back Prevention: If web tension is excessively high when the impulse wire fires, stored elastic energy causes the severed film tail to retract violently toward the carriage. The tail escapes the clamp jaws, aborting the next automatic cycle.
- Thermal Severing Precision: If the web is slack, the LLDPE film wrinkles across the impulse element, leading to incomplete parting and trailing strings.
- Decoupled Delivery: The B100 integrates a dedicated pre-stretch tension controller that isolates internal roller pre-stretch from external carriage-to-pallet application tension. Maintaining constant web presentation ensures the film lies flat against the cutting wire and wiping brush every cycle.
Powered Pre-Stretch Ratio and Film Consumption
The B100 features a powered pre-stretch film carriage driven by an independent 0.37 kW motor. Routing the film through differential-speed gearing elongates the polymer within the carriage, maximizing yield while eliminating crushing forces on light or crushable cartons.
Standard factory gearing delivers a Rapporto di pre-stiro del 250% (1 m of master film yields 3.5 m applied film). Optional mechanical gear pairs provide adjustments from 100% a% 300 to match specific gauge elongations.
Illustrative Film Consumption Calculation
Per un pallet standard europeo/australiano (1,200 mm × 1,000 mm) avvolto con 15 giri utilizzando lo standard 0.025 mm (25 µm) Pellicola LLDPE:
- Perimetro di carico:
2 × (1.2 m + 1.0 m) = 4.4 m - Lunghezza Web applicata:
4.4 m × 15 wraps = 66 m - Master Roll Consumption (at 250% Pre-Stretch):
66 m ÷ 3.5 ≈ 18.86 m(approx. 217 g of film per pallet, derived from 0.025 mm gauge at 500 mm width) - Master Roll Consumption (at 100% Pre-Stretch):
66 m ÷ 2.0 = 33.0 m(approx. 380 g per pallet)
Master Roll Capacity and Uptime
The carriage accommodates industrial film rolls with a Larghezza dell'anima: 500 mm, uno standard Nucleo da 76 mm, roll lengths from da 500 m a 1,500 m, and weights up to 15 kg.
- At 1,500 m roll capacity and 250% pre-stretch:
1,500 m ÷ 18.86 m ≈ 79 pallets per roll. - In continuous 24 pallets/hour operations, a 1,500 m roll requires replacement only once every ~3.3 operating hours, minimizing scheduled line interruptions.
Turntable Dynamics and Line Integration Parameters
The B100 turns on a ring-gear slew bearing that stays stable with an off-centre load, and a photocell reads the load height so nobody has to reposition a mast limit between SKUs.
What the platform publishes is the film and programme side: 0.025 mm LLDPE, 500 mm wide, 500 to 1,500 m per roll on a 76 mm core at 15 kg; bottom, middle and top layers each set from 0 to 99 turns; separate top and bottom counters plus a resettable cycle counter; and pre-stretch tension control through the HMI. Deck diameter, top-of-roller height, carriage speed and motor ratings are fixed per project, so they come back in the quotation rather than in a table.
For planning, a 24-pallet-per-hour target is a 150 s cycle: roughly 75 s of rotation at 12 r/min plus 75 s for indexing, ramping, homing, cutting, wiping and clamp reset.
PLC Control System and Program Architecture
Control logic is governed by an industrial programmable logic controller housed in a European-standard electrical cabinet, paired with an operator interface and tactile pushbuttons:
- Layer Count Control: Top, middle, and bottom wrap layers are independently programmable from Da 0 a 99 strati, providing reinforced pallet bases and weather-resistant cap overlaps.
- Dual Counters: Integrated non-resettable master production counter alongside resettable batch counters for shift logging.
- Carriage Control: Variable vertical speed regulation controls web overlap pitch during mast ascent and descent.
- Modalità operative: Selectable overwrap cycles, reinforcement mid-wraps, or manual-jog override for maintenance alignment.
Utilities, Pneumatic Requirements, and Machinery Safety
The pneumatic side is the one that has to be right before commissioning: dry, filtered air at 0.6–0.8 MPa, because both the clamp and the impulse cut are air-driven and a wet line will foul the hot wire and slow the jaw.
Misure di salvaguardia
- Isolamento: a lockable main isolator lets the deck and the heating wire be locked off for maintenance.
- Arresto di emergenza: mushroom-head buttons on the console and on external posts.
- base: the EN 415-6 pallet-wrapping framework, an ISO 12100 risk assessment and EN ISO 13849-1 for the safety-related control parts, with the required performance level per guard set by that assessment.
Lista di controllo per la selezione degli ingegneri
- Pallet: maximum load dimensions including the pallet, and minimum and maximum unit weight.
- Throughput: peak pallets per hour and the staging buffer length behind the wrapper.
- Altezza del ponte: the top-of-roller datum against the existing line.
- Film: LLDPE at 25 µm, 500 mm wide, 76 mm core, up to 15 kg per roll.
- Aria: dry, regulated 0.6–0.8 MPa at the machine base.
- Potenza: 380 V three-phase, or whatever the site transformer actually delivers.
FAQ tecnico
Q: Does someone have to tie off or cut the film? A: No. The gripper holds the leading tail, an impulse element parts the film at the end of the cycle and a brush arm smooths the tail onto the load face.
Q: How does bad tension break the cut? A: Slack lets the web wrinkle across the impulse wire, so the cut only goes partway; over-tension stores energy that snaps back and drags the tail out of the clamp, and the next pallet cannot start automatically.
D: Quanta pellicola si risparmia con il pre-tensionamento? A: At 250% one metre of master roll becomes 3.5 m of applied film, so a pallet that takes roughly 380 g at 100% takes about 217 g. That ratio is the saving, not a guarantee.
Q: Can light or fragile loads be wrapped? A: Yes — the elongation happens between the carriage rollers, so the pull on the stack is small and carton corners are not crushed.
Q: What maintenance does the cut-and-wipe group need? A: Check the impulse wire for residue, hold air at 0.6–0.8 MPa, and keep the brush free of adhesive build-up.
Prossimo passo e protocollo di proposta rapida
Accelerate line automation with an OEM engineering proposal delivered within 24 to 48 hours:
- Submit Load Envelope: Send your pallet dimensions (L × W × H), minimum/maximum payload weight, and required shift throughput to info@fhopepack.com.
- Review Layout & Kinematics (24–48 Hours): Our team returns complete drawings showing turntable conveyor integration, top-of-roller elevations, clamp-cut-wipe clearances, and power requirements.
- Control Handshake Finalization: Schedule a technical session to finalize upstream PLC handshakes (interlocking signals, roller run permits, and fault status).
Related Systems and Normative Standards
Attrezzatura correlata
- Avvolgipallet automatico B100
- Semi-Automatic Pallet Stretch Wrapping Machine JL-A200
- Pallet Wrapping Machine A200
- Sistemi di avvolgimento pallet con piattaforma girevole ad alta velocità
Normative Standards
- IT 415-6: 2013: Safety of packaging machines — Part 6: Pallet wrapping machines
- ISO 9001 e ISO 14001Sicurezza dei macchinari — Principi generali di progettazione — Valutazione e riduzione del rischio
- UNI EN ISO 13849-1: Safety of machinery — Safety-related parts of control systems
Ultimo aggiornamento: 05/11/2026