Ամփոփում
A semi-automatic small coil wrapper provides targeted orbital stretch-wrapping for light-to-medium wire, cable, and corrugated hose coils. Engineered for facilities processing hundreds of coils per shift, this compact station replaces manual winding with repeatable mechanical packaging. Packaging integrity depends strictly on roller center distance, core-to-surface tension, and outer diameter overlap calibration. This technical guide outlines machine kinematic setup, drive parameter calculations, and operational safety for the FPCA wrapper platform.
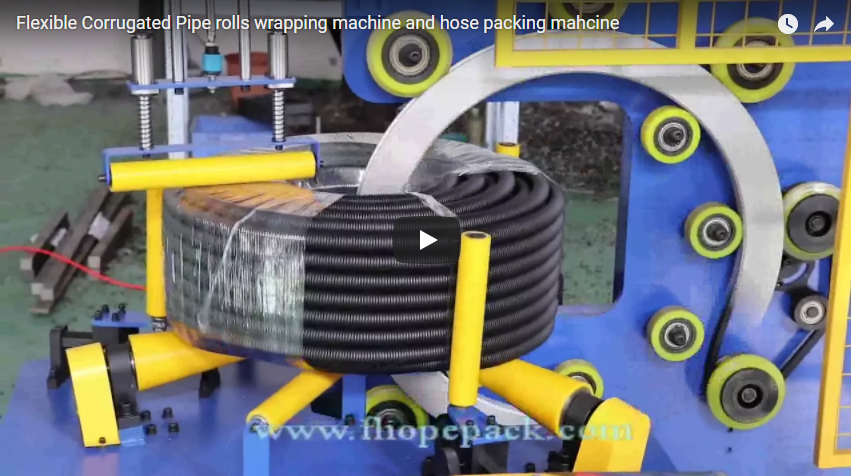
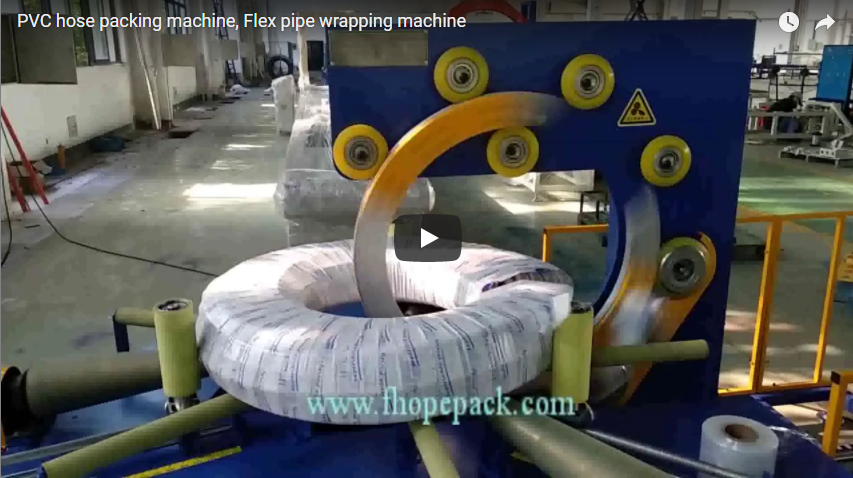
The FPCA series utilizes an orbital wrapping chassis featuring dual polyurethane-coated support rollers, an overhead damping press arm, and an eye-through orbital rotating ring. The coil rests upright on its outer diameter while the support rollers rotate it about its center axis. Simultaneously, the orbital ring shuttles the film roll through the open inner eye, generating a sealed, radial overlap package.
Բառը
- Հիմնական կառուցվածքային բաղադրիչներ
- Setting Up for a New Coil Size
- Ստանդարտ գործառնական ընթացակարգ
- Machine Engineering Specifications
- Overlap Calibration and Kinematic Settings
- Shift Maintenance and Inspection
- Application and Selection Checklist
- Անվտանգության և մեքենաների վերաբերյալ հրահանգներ
- Ինժեներական Հաճախակի տրվող հարցեր
- Engineering Inquiry and Next Steps
- Related Documentation
- Standards and Sources
Հիմնական կառուցվածքային բաղադրիչներ
- Drive and Support Rollers: High-friction, polyurethane-coated (90 Shore A) rollers that support the coil weight and provide peripheral drive rotation without marring soft outer jackets.
- Top Damping Press Roller: Adjustable vertical stabilization roller that counteracts upward tangential pull from the stretch film, preventing coil slippage or axial wandering.
- Ուղեծրային օղակի հավաքում. Precision ring driven by industrial roller chain and sprocket, delivering balanced orbital rotation through the coil eye.
- Film Dispenser Carriage: Features a spring-loaded mechanical core brake or friction clutch to regulate film tension and limit neck-down.
- Drive Unit & Sensors: Powered by heavy-duty Bosch industrial gear motors, coordinated with an inductive proximity sensor for exact zero-position homing and cycle count control.
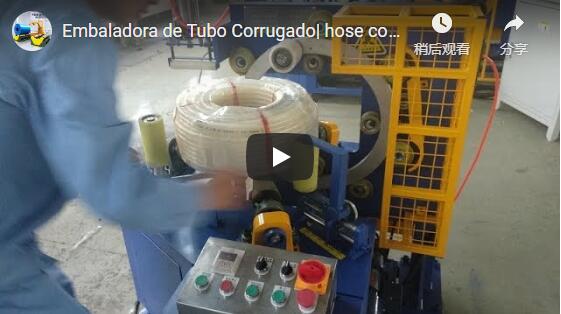
- Ինտեգրված կառավարման վահանակ. Houses system emergency stop, variable frequency drive (VFD) potentiometers for ring speed and roller speed, and manual jog switches.
Setting Up for a New Coil Size
- Adjust Support Roller Spacing: Adjust the horizontal center distance between the bottom support rollers so that the coil eye centers symmetrically over the rotating ring clearance path.
- Engage Top Stabilizer: Lower the top press roller until it firmly contacts the coil top face; lock the height collar to apply steady retaining pressure.
- Load and Thread Film: Mount the designated stretch film roll (LLDPE, PE, or VCI) onto the carriage mandrel. Thread the web through the guide rollers and set the mechanical brake nut.
- Calibrate Web Tension: Pull the film leader manually to confirm constant pull force. Tension must stretch the film sufficiently without collapsing flexible corrugated tubing or tearing.
- Set VFD Speed Ratio: Adjust the ring speed and support roller speed dials to achieve the targeted layer overlap percentage.
- Execute Test Cycle: Wrap one sample coil to verify structural containment and check overlap percentage at both the outer and inner diameters.
Ստանդարտ գործառնական ընթացակարգ
- Coil դիրքավորումը: Place the unwrapped coil squarely between the support rollers; ensure the eye clear path does not interfere with the ring orbit.
- Tuck Film Tail: Draw the film leader from the carriage and secure it securely within the inner core or under the first wire wrap.
- Սկսել ցիկլը. Press the green Start button. The system initiates soft-start acceleration, rotating the coil and the wrapping ring synchronously.
- Ավտոմատ կանգառ՝ Upon completing the preset rotation cycles (detected by the proximity limit switch), the drive decelerates to a controlled home stop.
- Cut and Unload: Cut the film web with a utility cutter, smooth the tail onto the wrapped face, release the top clamp if equipped, and remove the finished coil.
Machine Engineering Specifications
| Technical Parameter | FPCA100 | FPCA-200 |
|---|---|---|
| Կծիկի ներքին տրամագիծը (ID) | 90–250 մմ | 150–400 մմ |
| Կծիկի արտաքին տրամագիծը (OD) | 150–400 մմ | 250–500 մմ |
| Կծիկի լայնությունը / առանցքային բարձրությունը | 50–180 մմ | 80–200 մմ |
| Կծիկի առավելագույն քաշը | 30 կգ | 50 կգ |
| Օղակի պտտման արագությունը | 10–120 պտ/րոպե (VFD կառավարմամբ) | 10–120 պտ/րոպե (VFD կառավարմամբ) |
| Գլանաձև գծային արագություն | 1.5–8.0 մ/ր | 1.5–8.0 մ/ր |
| Net Wrap Cycle Time | 18–30 վրկ | 20–30 վրկ |
| Համընկնման միջակայք | 20%–90% (Continuously variable) | 20%–80% (Continuously variable) |
| Drive Motors- ը | Bosch Industrial DC/AC Geared | Bosch Industrial DC/AC Geared |
| Տեղադրված էլեկտրամատակարարում | 1.8 kW, 220V/380V (50/60 Hz) | 2.0 kW, 220V/380V (50/60 Hz) |
Overlap Calibration and Kinematic Settings
Film overlap is governed by the kinematic speed ratio between the orbital ring angular velocity and the coil peripheral surface speed.
The circumferential advance per wrap at the outer diameter is expressed as:
L_advance = W_film × (1 - Overlap_ratio)
The theoretical total wraps required for single-layer closure across the circumference:
N_wraps = (π × OD_coil) ÷ L_advance
Հաշվարկի օրինակ. Wrapping a coil with 300 mm OD using 60 mm film at a targeted 50% overlap:
L_advance = 60 mm × (1 - 0.50) = 30 mm- Circumference =
π × 300 mm ≈ 942.5 mm - Total wraps required =
942.5 mm ÷ 30 mm ≈ 31.4 wraps - At a ring speed of 120 r/min, the net wrapping time is:
(31.4 ÷ 120) × 60 s ≈ 15.7 s
Note on Radial Differential: Because the inner diameter (ID) circumference is significantly smaller than the outer diameter (OD), film layers naturally accumulate higher overlap along the inner eye. Always calibrate minimum overlap settings based on the coil OD. Net wrapping time accounts only for motor run time; overall cycle time per coil must factor in loading, film fastening, soft-start ramp-up, cutting, and unloading (typically 35–50 seconds floor-to-floor).
Shift Maintenance and Inspection
- Roller Surfaces: Clean polyurethane rollers with isopropyl alcohol; ensure no stretch film adhesive residue or plastic strands are wound around bearing collars.
- Chain and Tensioner: Inspect the primary ring drive chain for proper lubrication and sag (deflection ≤ 10 mm under manual pressure).
- Film Carriage Clutch: Check the friction disc and spring collar for smooth unwind resistance without jerky stick-slip behavior.
- Limit Sensors: Clean the inductive proximity switch faces; confirm LED indicator triggers reliably when the ring reaches home position.
- Անվտանգության սարքեր՝ Test the primary emergency stop pushbutton and perimeter interlock before beginning production.
- Consumable Inventory: Verify that film roll widths, gauge thickness (typically 20–35 µm), and core diameters match recipe requirements.
Application and Selection Checklist
- Խխունջի չափսերի ծրար՝ Confirm minimum and maximum ID, OD, and width match the operational boundaries in the data table.
- Coil Mass and Core Rigidity: Confirm total coil weight is within frame limits (≤ 30 kg for FPCA100; ≤ 50 kg for FPCA-200) and that flexible hoses will not collapse under tension.
- Նպատակային թողունակություն՝ Evaluate duty cycle (e.g., 60–90 coils/hour) to determine if semi-automatic operation or conveyorized feeding is needed.
- Սպառվող տեսակը. Specify LLDPE stretch film, VCI anti-corrosion film for copper/steel wire, or woven PP tape.
- Loading Logistics: Select between manual benchtop loading, infeed gravity chutes, or integration with an upstream coiler.
- Պիտակավորման պահանջներ. Determine whether identification labels are placed beneath the film layers or applied externally post-wrap.
Անվտանգության և մեքենաների վերաբերյալ հրահանգներ
The FPCA series is manufactured in conformance with international industrial safety and electrical codes:
- EN ISO 12100:2010: Risk assessment and risk reduction principles for mechanical assemblies.
- EN 415-10: Safety requirements for packaging machines, wrapping machines, and associated transfer systems.
- EN 60204-1: Electrical equipment of machines, safety earthing, and control circuits.
Գործառնական անվտանգության կանոն. Operators must never place hands inside the rotating ring boundary while the status light indicates live operation. Loading, centering adjustments, and film threading must be conducted strictly with the machine halted and the drive zeroed.
Ինժեներական Հաճախակի տրվող հարցեր
Q: Why does the film layer build up more heavily inside the coil eye? A: Surface advance is proportional to radius. For a given ring cycle, the linear travel along the small inner diameter is shorter than along the outer diameter, causing the film to concentrate more passes per unit area at the ID.
Q: What is the typical floor-to-floor cycle time? A: While net rotational wrap time requires 18–30 seconds depending on outer diameter and overlap, total floor-to-floor time (including manual placement, threading, cutting, and removal) averages 40–55 seconds per coil.
Q: Can the FPCA wrapper run paper, foil, or woven tape? A: Yes. The standard carriage supports LLDPE stretch film. For crêpe paper, VCI tape, or woven polypropylene ribbons, an optional mechanical tension carriage with specialized drag rollers is available.
Q: Can this machine be integrated into an automated coiling line later? A: Yes. The machine base supports downstream installation of powered roller conveyors, automatic pneumatic cutting and clamping units, and coiler signal handshakes via 24V dry contacts.
Engineering Inquiry and Next Steps
- Ներկայացրեք ապրանքի տեխնիկական բնութագրերը՝ Email your coil minimum/maximum ID, OD, width, and package weight to
info@fhopepack.com. - Ճարտարագիտական ակնարկ. Our application engineers review coil stiffness and throughput requirements to match the correct machine frame and carriage.
- Պաշտոնական մեջբերում. Receive a customized machine configuration, layout drawing, and quotation within 24 hours.
Related Documentation
- Cable Coil Wrapping Machine FPCA-200 (Product Overview)
- Small Coil Wrapping Machine Video Library
- Simple Coil Wrapping Machine for Full Size Applications
- How Coil Wrapping Machines Package PET Belt and Hose Coils
Standards and Sources
- FHOPE Technical Documentation: FPCA100 & FPCA-200 Cable & Hose Coil Packaging Machines
- EN ISO 12100` 2010 Մեքենաների անվտանգություն. Նախագծման ընդհանուր սկզբունքներ. Ռիսկի գնահատում և ռիսկի նվազեցում
- EN-415 10 Փաթեթավորման մեքենաների անվտանգություն. Մաս 10. Ընդհանուր պահանջներ
- EN-60204 1 Մեքենաների անվտանգություն. Մեքենաների էլեկտրական սարքավորումներ. Մաս 1. Ընդհանուր պահանջներ
Վերջին անգամ վերանայվել է՝ 2026-10-20