خلاصه اجرایی
یک مرکز خدمات برش، یک کویل اصلی را به کویلهای باریک و متعدد تبدیل میکند و هر کدام باید با برچسب مناسب برای سفارش مناسب خارج شوند. این خط بستهبندی کویل شکافدار، هر کویل را میپیچد، وزن میکند و برچسبگذاری میکند و دادههای سفارش را مستقیماً از ERP شما میگیرد، بنابراین هیچکس برچسب را با دست تایپ نمیکند. در زیر ایستگاههای خط، نحوه تبادل دادهها توسط PLC ما با ERP شما، زمان تاکت در هر کویل و مواردی که قبل از خرید باید بررسی کنید را توضیح میدهیم.
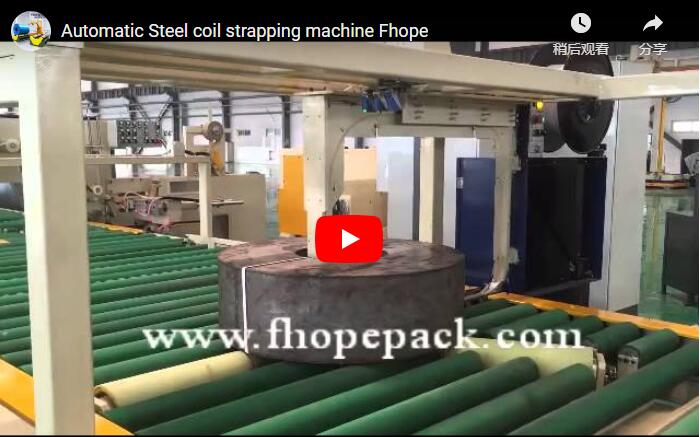
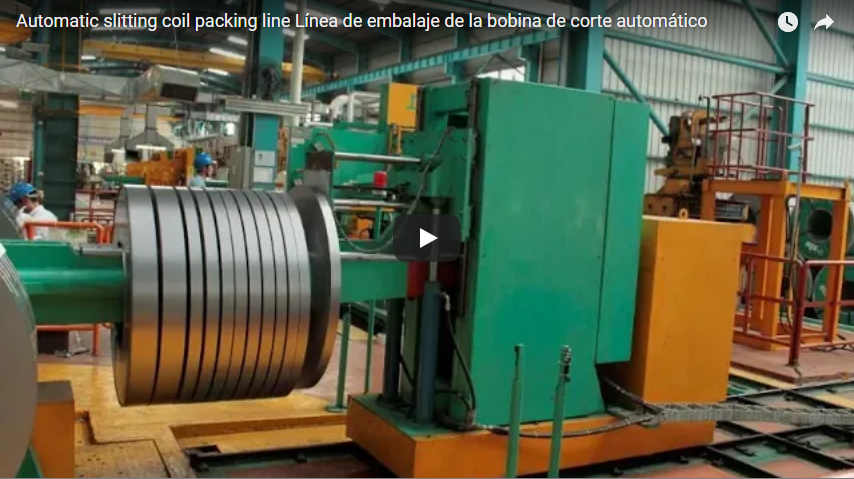
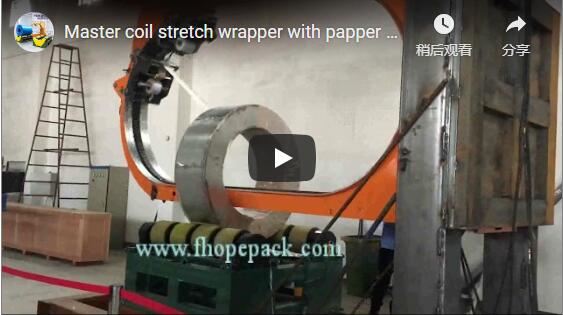
The line is built on a welded steel frame with guarding around the moving stations. Narrow slit coils travel on a motorized roller conveyor into the wrapping station, where an upper clamp holds the coil and a moving arm with a film roll wraps the outer circumference. Wrapped coils exit via a powered roller outfeed and transfer to designated stacking and dispatch zones. A control cabinet with power distribution, safety relays and the operator interface stands beside the line.
فهرست مندرجات
- چرا برچسب زدن گام ضعیفی است
- ایستگاههای خطی
- جریان داده: ERP برای برچسب گذاری و بازگشت
- آنچه روی برچسب نوشته شده است
- محدوده کویل
- زمان تاکت در هر کویل
- چک لیست انتخاب
- ایمنی
- سوالات متداول مهندسی
- مرحله بعدی
- خواندن مرتبط
- منابع
چرا برچسب زدن گام ضعیفی است
One 1,250 mm master coil slit into 125 mm strips produces 10 narrow slit coils, and every coil requires its own label with order, width and verified weight. When labels are handwritten or typed at the packing station, coils get swapped, weights are transcribed wrong, and customers receive material that does not correspond to the delivery note.
This automated packaging line eliminates manual transcription: weight comes directly from an integrated conveyor scale, order data routes automatically from the enterprise resource planning (ERP) system, and an industrial print-and-apply applicator affixes the label at a fixed station in the flow.
ایستگاههای خطی
- پایین رونده یا گیت گردان: takes slit coils from the slitter and turns them to the eye-vertical packing position.
- تسمه بندی: applies radial straps to prevent core telescoping, in PP/steel strap or high-tension PET (15–38 s per strap cycle).
- کاغذ بسته بندی: a moving film arm wraps the coil outer circumference while the upper stabilization clamp holds the coil rigid.
- وزن: an in-line conveyor scale records the gross weight without stopping the flow.
- برچسب زدن: a print-and-apply unit prints and places the identification and barcode label on the wrapped coil.
- پشتهسازی: coils are stacked onto skids or pallets ready for dispatch.
جریان داده: ERP برای برچسب گذاری و بازگشت
| گام | چه اتفاقی می افتد |
|---|---|
| ۱. صدور دستور | The ERP transmits the batch slitting order: master coil ID, individual coil sequence numbers, slit widths, target gauges, and customer order parameters. |
| ۲. کویل میرسد | Optical tracking sensors and line PLC register the physical coil entry and associate it with the active record in the order sequence queue. |
| ۳. وزن کنید | The conveyor scale captures gross weight. Net weight is calculated in the PLC: net weight = gross − tare of strap, film and any pallet, with tare reference values pre-configured in PLC memory. |
| 4. چاپ کنید | The industrial applicator prints the label, synchronizing live ERP production fields with the real-time measured weight. |
| 5. تایید کنید | The automation line writes back the confirmed coil unique identifier, exact weight, and packaging timestamp directly to the ERP system to close the production inventory loop. |
The control system operates on a Siemens S7-1200 or safety-integrated S7-1500F PLC platform. Base configurations use sensor-driven package tracking, while advanced configurations integrate weighing, print-and-apply labelling and direct ERP data exchange. The interface to your ERP (file exchange, database or middleware) and the printer model are confirmed at quote, after your IT team shares the order format.
آنچه روی برچسب نوشته شده است
- Individual coil number and parent master coil heat/lot number
- Customer purchase order, customer name and line-item number
- Material grade, nominal thickness and slit width
- Gross weight from the load cells and calculated net weight
- Production date, line number and shift identifier
- 1D barcode or 2D DataMatrix/QR code for scanning at dispatch
All data fields populate from your defined ERP label template, so they match your outbound delivery note.
محدوده کویل
| مورد | خط کویل باریک شکاف دار |
|---|---|
| وزن کویل | 30،4,000-XNUMX،XNUMX کیلوگرم |
| سیم پیچ OD | ۵۰۰–۱۵۰۰ میلیمتر، قابل افزایش تا ۲۱۰۰ میلیمتر |
| کویل ID | 300، 508 یا 610 میلی متر |
| عرض سیم پیچ | 8-500 میلی متر |
| تولید | 20-40 کویل در ساعت |
| تسمه | PET یا فولاد |
(Note: For higher-throughput master slitting bays requiring centralized palletizing, alternative configurations such as 6-station turntable stacking cells with centering tables and heavy-duty arm handlers are available as distinct engineering variants).
زمان تاکت در هر کویل
Takt time is defined as:
Takt time = 3,600 s ÷ coils per hour
At 40 coils per hour, each station has 90 seconds per coil; at 20 coils per hour, 180 seconds. In-line weighing, print buffer generation and label application must fit inside that window.
To avoid cycle stalls, the ERP reply is never a synchronous coil-by-coil database query while a coil sits on the scale. Order data is pre-loaded to the PLC at order release; when a coil triggers the weighing sensor, tare calculation and label printing execute from local controller memory, and the confirmation is posted back asynchronously once the coil moves on.
چک لیست انتخاب
- Which ERP system do you run, and how does it share order data?
- What are your minimum and maximum coil weights, diameters, widths, and target coils per hour?
- Which label fields and barcode symbologies does your customer mandate?
- What strap material is required (PP, steel or PET), and how many straps per coil?
- Does the surface specification call for stretch film, VCI film, barrier paper or a composite medium?
- How are wrapped coils transferred to dispatch: conveyor offload, crane, or down-stacking onto pallets?
ایمنی
The line is designed to:
- EN ISO 12100: 2010 — machine safety risk assessment and risk reduction.
- EN-415 10، — safety of packaging machines.
- EN-60204 1، — electrical equipment of machines.
The wrapping and clamping area, strapping head and clamp travel are isolated behind perimeter guarding, and access gates are interlocked.
سوالات متداول مهندسی
Q: Does the label weight come from the ERP or the scale? A: Gross weight comes directly from the certified in-line scale load cells. The Siemens line PLC subtracts the calibrated tare weight (strapping, protective wrap, and packaging consumables), and the automation line transmits both gross and verified net values back to the ERP system record.
Q: What if the plant ERP connection drops or goes offline? A: A manual entry fallback on the operator panel is part of the interface design and is agreed at quote.
Q: What is the maximum throughput capability of this line configuration? A: The standard narrow slit coil packaging line processes between 20 and 40 finished coils per hour, depending on the number of straps applied per coil and wrapping film layer overlap.
Q: Can the automated station handle variable slit widths within the same production batch? A: Yes. Because each coil is tracked in the line PLC by order sequence, the line accommodates fluctuating slit widths within the 8–500 mm envelope without manual retooling.
مرحله بعدی
- Send your coil range, required coils per hour, and current label template به آدرس info@fhopepack.com.
- Our packaging engineering team designs the optimized station layout, conveyance sequence, and PLC/ERP communication protocol.
- We deliver a technical proposal and equipment quotation طی ساعت 24.
خواندن مرتبط
- خط بستهبندی کویل شکافدار (محصول)
- دستگاه بسته بندی کلاف (محصول)
- خط بسته بندی کویل با عملکرد چرخش و انباشته
منابع
- FHOPE Technical Specification: Narrow Slit Coil Automated Packaging Line
- EN ISO 12100: 2010 ایمنی ماشین آلات - اصول کلی طراحی - ارزیابی ریسک و کاهش ریسک
- EN-415 10، Safety of packaging machines — General requirements
- EN-60204 1، Safety of machinery — Electrical equipment of machines — General requirements
آخرین بررسی: 2026-10-29