Vertical (eye-to-sky) packaging is the industry standard for securing narrow slit steel coils that lack the mechanical stability to stand safely on edge. By executing an axial through-eye wrap in the eye-horizontal position and subsequently down-ending the bound coil to an eye-vertical orientation, processors eliminate coil tipping, protect vulnerable strip edges, and enable dense pallet stacking. This configuration allows multi-coil stacks to be moved via standard counterbalanced forklifts rather than overhead crane C-hooks, streamlining downstream warehousing while minimizing logistics labor.
بررسی اجمالی
Automated slit coil packaging systems eliminate manual strapping hazards, prevent edge telescoping, and maintain packaging consistency at high line speeds. Modern slit coil packing lines integrate transfer cars, through-the-eye wrapping stations, heavy-duty 90° hydraulic down-enders, pick-and-place stacking arms, and multi-axis strapping units.
The complete sequence protects coils against physical handling shocks and atmospheric oxidation (rust) during road transport, containerized shipping, and long-term staging.
When to Choose Eye-Vertical Over Eye-Horizontal Packaging?
Selecting between an eye-vertical (eye-to-sky) and an eye-horizontal (eye-to-wall) orientation is determined by the coil’s geometric aspect ratio (width-to-outer diameter ratio, W/OD), total mass, and the decoiling configuration of the end user.
- Eye-Horizontal (Eye-to-Wall): The coil axis remains parallel to the plant floor, supported by its outer cylindrical face on curved saddles. Wide master coils and heavy strip coils exhibit a broad ground footprint, giving them inherent gravitational stability. Handling is typically managed via overhead cranes using counterweighted C-hooks or coil grabs.
- Eye-Vertical (Eye-to-Sky): The coil axis stands perpendicular to the floor, resting flat on its side face. Narrow slit coils (slits from 8 mm up to 450 mm wide) feature a very high aspect ratio. When placed on edge, minor vibration causes rapid elastic deflection and lateral tip-over, posing catastrophic safety risks. Stacking coils flat on pallets completely removes the tipping hazard.
       EYE-HORIZONTAL                         EYE-VERTICAL
       (Eye-to-Wall)                         (Eye-to-Sky)

          ┌───────┐                            ┌──────────────┐
          │   ●   │ ◄── Center Eye             │              │
          │ (Axis)│     Horizontal             ├──────────────┤
          └───────┘                            │   ● (Axis)   │ ◄── Axis
      ═════════════════                        │   Vertical   │     Vertical
       Resting on Edge                         └──────────────┘
     (Wide Master Coils)                     ════════════════════
                                                Resting on Face
                                              (Stable Multi-Stack)
Furthermore, stamping plants and roll-forming facilities operating vertical uncoilers require eye-to-sky coils to feed payoffs directly without secondary upending at the uncoiler station.
| نوع سیم پیچ | مشخصات ابعادی | جهت گیری توصیه شده | Mechanical Rationale | Primary Handling Gear |
|---|---|---|---|---|
| کویلهای شکاف باریک | عرض: ۶۰۰–۱۶۰۰ میلیمتر نسبت ابعاد بالا |
Eye-Vertical (Eye-to-Sky) | High lateral instability on edge; stacks safely on pallets | Forklift / Pallet jack |
| Master / Wide Coils | عرض: ۶۰۰–۱۶۰۰ میلیمتر Broad footprint |
Eye-Horizontal (Eye-to-Wall) | Stable on radiused floor saddles; high structural stiffness | Crane with C-hook / Tong |
| Press-Feed Strips | Any width matching vertical payoffs | Eye-Vertical (Eye-to-Sky) | Direct crane/forklift loading directly onto payoff mandrels | Forklift / Stacker |
Automated Packing Flow Architecture
Modern high-speed packaging lines implement a modular five-station sequence designed to isolate the human operator from high-mass movement corridors.
  [ Slitter Exit ]
         │
         ▼
  ┌──────────────┐     Through-the-eye wrapping while axis is horizontal;
  │ 1. Transfer  │ ──► Prevents interlayer telescoping via radial pretension.
  └──────────────┘
         │
         ▼
  ┌──────────────┐     High-speed orbital shuttle drives stretch film, VCI,
  │   2. Wrap    │ ──► or HDPE woven cloth through the center bore.
  └──────────────┘
         │
         ▼
  ┌──────────────┐     Hydraulic tilting cradle rotates coil 90°
  │ 3. Down-End  │ ──► from horizontal bore to vertical eye.
  └──────────────┘
         │
         ▼
  ┌──────────────┐     Mechanical scissor gripper or magnetic head centers
  │   4. Stack   │ ──► and layers coils onto wooden pallets; inserts spacers.
  └──────────────┘
         │
         ▼
  ┌──────────────┐     Radial indexing head tensions 3, 4, or 6 PET/Steel
  │5. Strap/Weigh│ ──► bands through pallet core; automated scale & label print.
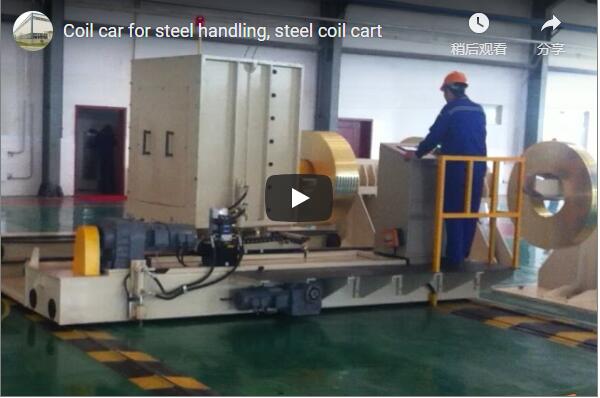
└──────────────┘- Transfer Station: Individual slit coils exit the recoiler turnstile and are collected by an automated coil car or indexing walking beam. Coils transfer sequentially to the packaging roller station without manual riggings.
- Axial Through-Eye Wrapping: The coil is wrapped while still in the eye-horizontal orientation. A split-ring shuttle carries the packaging material through the inner diameter (ID) and across the outer diameter (OD). Wrapping before tilting binds individual strip wraps tightly, eliminating interlayer slippage.
- Controlled 90° Down-Ending: A heavy-duty electro-hydraulic down-ender (tilter) rotates the wrapped coil from horizontal to vertical. Variable-frequency drives (VFD) smoothly decelerate the load through its center-of-gravity shift to prevent edge impact.
- Centering and Stacking: An automated pick-and-place stacking arm equipped with mechanical ID expanding grippers lifts the coil. It transfers and centers the coil onto a waiting pallet, building a multi-tier stack according to target bundle recipes.
- Circumferential Strapping and Labeling: The finished stack indexes to a multi-point strapping head. Polyester (PET) or high-tensile steel straps are applied through the eye and underneath the pallet timber. An inline load cell verifies package net/gross weight, transmitting data to a thermal barcode print-and-apply applicator.
Operators oversee cycle times, recipe setups, and safety diagnostics from a centralized PLC touchscreen console outside perimeter fencing.
Critical Engineering Best Practices Across Stages
- Wrap in Horizontal Orientation Before Down-Ending: Never down-end an unstrapped or unwrapped narrow coil. Performing the through-eye wrap horizontally applies circumferential hoop stress across all layers. This prevents internal telescoping (core shift) during the subsequent 90° tilt. Wrapping first also encapsulates the vulnerable edge corners with multi-layer protective film before gripper contact.
- Material Tailoring by Supply Chain Exposure:
- Domestic short-haul: Cast LLDPE stretch film (25–35 µm) provides containment and basic moisture resistance.
- Ocean container freight: Multi-layer coextruded VCI (Volatile Corrosion Inhibitor) film/paper is required to suppress galvanic corrosion inside condensation zones.
- High-strength export: Extruded HDPE woven fabric outer layers protect against edge-rub friction caused by shipping container vibration.
- Dynamic Center-of-Gravity Stacking: System recipes must stack coils in descending weight order: heaviest slit coil at the base, lightest at the top. The cumulative weight must match pallet load ratings and forklift carriage ratings.
- Interleaving Protective Spacers: Automated disc placement or manual insertion of corrugated cardboard, fiberboard rings, or radial wooden runners between stacked coils prevents edge crimping and absorbs localized vibration during transport.
- Through-Eye Pallet Anchoring: Ensure straps loop directly through the central coil eyes and underneath the pallet’s top deck boards (3, 4, or 6 points at 120°, 90°, or 60° spacing). This binds the coils and pallet into an integral monolithic cargo unit.
- Integrated Data Capture: Integrate digital weighing scales directly into the turntable conveyor. Direct PLC integration prints gross, tare, and net weights alongside ERP slitter run IDs, eliminating human data entry errors.
مشخصات فنی پایه
The following parameters represent standard engineering line configurations for light-to-medium slit steel operations compared against heavy master coil lines.
| پارامتر مهندسی | Narrow Slit Coil Specification | Wide / Master Coil Specification |
|---|---|---|
| Individual Coil Weight Range | 30،4,000-XNUMX،XNUMX کیلوگرم | 3,000،25,000-XNUMX،XNUMX کیلوگرم |
| قطر بیرونی سیم پیچ (OD) | 500–1,500 mm (Optional: up to 2,100 mm) | 800-2,200 میلی متر |
| قطر داخلی سیم پیچ (ID) | Standard: 300 / 508 / 610 mm | 508/610/760 میلی متر |
| محدوده عرض نوار | 8-500 میلی متر | 450-2,000 میلی متر |
| ظرفیت عملیاتی | 20-40 کویل در ساعت | 5-10 کویل در ساعت |
| Cycle Strapping Speed | 15–38 seconds per strap feed/tension/seal | 30–45 seconds per strap |
| رسانههای بستهبندی سازگار | Stretch film, VCI paper, HDPE woven wrap | Stretch film, VCI paper, radial jackets |
| Pallet Strapping Configuration | 3, 4, or 6 radial points (PET or Steel) | Typically 2–4 circumferential body straps |
| معماری درایو | SEW Eurodrive gearmotors / Hydraulic HPU | High-torque heavy hydraulic systems |
Note: Master coils exceeding 5,000 kg typically remain eye-horizontal on protective polymer floor chocks. Eye-vertical stacking configurations are primarily engineered for slit coils under 500 mm in width.
Film Consumption and Throughput Cycle Analysis
1. Film Usage Estimation
Wrap consumption depends on coil cross-section geometry, film roll width, and ring carriage overlap settings. For a representative slit coil:
- قطر خارجی (OD) = 1,400 میلیمتر
- قطر داخلی (ID) = 508 میلیمتر
- عرض (عرض) = ۲۰۰ میلیمتر
- Film Width (Wf) = 120 mm, Film Overlap = 30 mm (Effective advance per pass = 90 mm)
The cross-sectional loop perimeter (Lp) wrapped around the strip wall is:
Lp = 2 × ( (OD – ID) / 2 + W ) = 2 × ( (1400 – 508) / 2 + 300 ) = 2 × (446 + 300) = 1,492 mm (1.492 m)
The mean circumference around the ring path (Cm) است:
Cm = π × (OD + ID) / 2 = 3.1416 × (1400 + 508) / 2 = 2,997 mm (approx. 3.0 m)
Total revolutions required (Nاحیای) with 90 mm effective feed per revolution:
Nاحیای = Cm / 90 mm = 2,997 / 90 ≈ 33.3 revolutions
Accounting for lead-in, tail overlaps, and core transitions (approx. 18–20 extra turns):
Total Film Length = (33.3 + 20) × 1.492 m ≈ 79.5 meters (approx. 80 m per coil)
2. Line Throughput Balance
The following cycle model examines a pallet stack containing six 800 kg slit coils strapped at 4 radial points:
| بررسی چرخه تولید | محاسبات مهندسی | Verified Line Result |
|---|---|---|
| Total Stack Net Weight | 6 coils × 800 kg | کیلوگرم ۷۳۰۰ |
| Automated Strapping Time | 4 straps × 30 seconds | ۳۰۰ ثانیه (۵ دقیقه) |
| Line Stacking Output | 30 coils/hour ÷ 6 coils/stack | 5 finished pallet stacks/hour |
| Available Cycle Window per Stack | 60 minutes ÷ 5 stacks | ۳.۵ دقیقه (۲۰۹ ثانیه) |
Strapping operations occupy 2.0 minutes of the 12.0-minute available pallet cycle window. The downstream strapping unit operates at an approximate 16.7% line utilization rate, preventing bottlenecks at the packaging line discharge.
Industrial Safety Standards and Hazard Mitigation
Automatic packaging machinery must comply with global functional safety and machinery standards:
- انطباق با EN 415-10: Governs specific safety requirements for modular coil packaging machines, covering clamping mechanisms, rotating rings, and high-speed film dispensers.
- ارزیابی ریسک ISO 12100: Applied to systematically identify and mitigate shear points, pinch points, and gravitational fall hazards associated with heavy steel handling.
- OSHA 1910.147 (LOTO) and EN ISO 13849-1: Systems utilize dual-channel safety relays, monitored interlocked perimeter guards, light curtains at pallet infeed/outfeed zones, and automatic mechanical locking pins on hydraulic down-enders for maintenance safety.
- Operator Segregation: All primary control interfaces are situated on external pedestals outside physical safety enclosures, keeping floor workers clear of moving cars and tilting mechanisms.
Line Sizing and Proposal Data Checklist
To receive an engineered layout, cycle simulation, and formal capital equipment quotation, provide the following operating parameters:
- هندسه سیم پیچ: Minimum and maximum Outer Diameter (OD), Inner Diameter (ID), slit width range, and coil weight limits (kg).
- Material Metallurgy: Steel grade, surface finish type (cold-rolled, galvanized, oiled, dry, silicon electrical steel, stainless).
- Upstream Throughput: Nominal and peak slit coils produced per hour from the slitting line.
- Protective Wrap Spec: Selected material combinations (LLDPE film, VCI paper, HDPE woven fabric) and target overlap percentage.
- Stacking Configurations: Coils per stack, target stack height limits, pallet dimensions, and timber runner orientations.
- Securing Configuration: Number of radial strapping points (3, 4, or 6 points), strap type (PET or High-Tensile Steel), and core seal method.
- Plant Interface: Factory floor load capacity, available footprint dimensions, utility supply (compressed air pressure, electrical voltage/frequency), and host ERP communications requirements.
Engineering proposal packages—including 2D/3D plant layout integrations, cycle time analyses, and mechanical component schedules—are delivered within 48 business hours following preliminary data sign-off.
منابع مهندسی مرتبط
- Slit Coil Automatic Packaging Line Solutions
- Technical Analysis: Eliminating Edge Damage in Slit Coil Tilting Operations
- Slit Steel Coil High-Speed Packaging Automation Systems
- Automated Heavy-Duty Steel Coil Transfer Cars and Walking Beams
- Orbital Eye-Through and Horizontal Coil Stretch Wrapping Technology