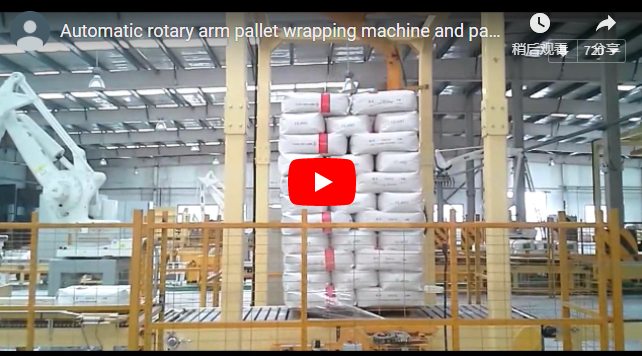
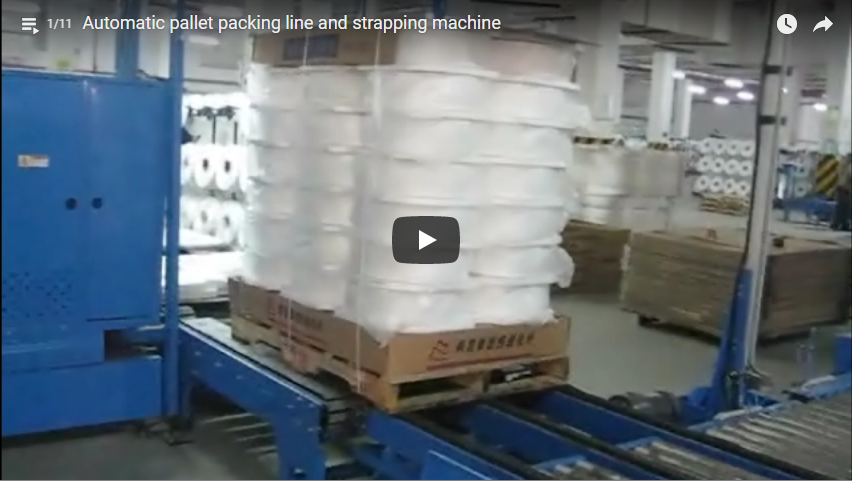
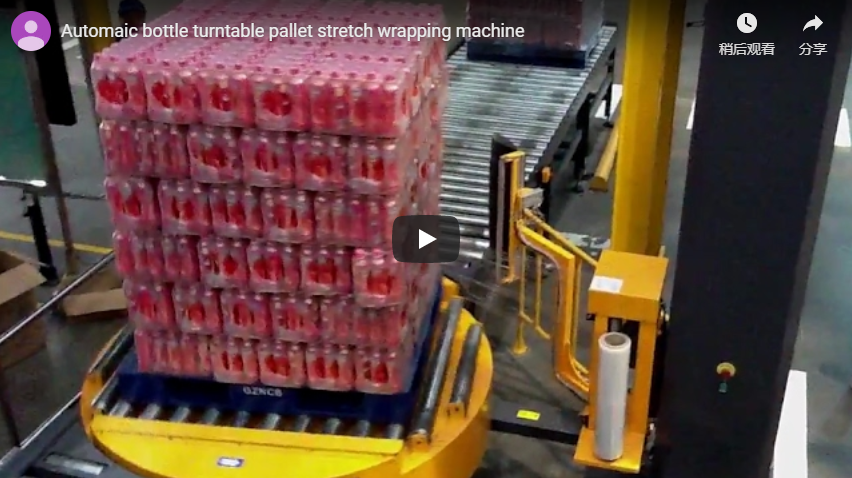
خلاصه اجرایی The B100 is an online turntable pallet wrapper engineered with an integrated powered roller conveyor turntable deck, allowing pallet loads to enter, wrap, and discharge seamlessly within automated conveying lines. Built for duty ratings up to 1,800 kg dynamic payload at line speeds of حداقل ۲۴ بار در ساعت, the machine features a 250% powered pre-stretch film carriage, independent VFD motion profiling, and an automated pneumatic clamp, hot-wire cut, and film tail wipe station. A detailed kinematic and consumables calculation is provided below to verify line cycle times and packaging film yield.
فهرست مندرجات
- What “Online” Means for a Turntable Wrapper
- How a Pallet Moves Through the Wrapper
- Automatic Clamp, Cut, and Wipe Station
- Wrap Programme and Controls
- B100 Engineering Specifications
- Worked Example: Cycle Timing, Line Rate, and Film Yield
- چک لیست انتخاب مهندسی
- Safety Systems and EN 415-6 Compliance
- سوالات متداول مهندسی
- گام بعدی
- خواندن مرتبط
- منابع
What “Online” Means for a Turntable Wrapper
A conventional standalone turntable wrapper acts as an isolated forklift station: pallets are staged, deposited onto the rotary table, wrapped, and retrieved individually. This introduces forklift traffic bottlenecks and variable handling delays.
The B100 online configuration integrates the turntable into the continuous factory conveyor network. The rotating turntable bed is fitted with heavy-duty powered rollers aligned mechanically and electrically with upstream infeed and downstream outfeed conveyor sections. By automating load staging, centering, and discharge via line PLC handshake signals, the wrapper operates as a scheduled process node rather than a manual material-handling stop.
How a Pallet Moves Through the Wrapper
- انتقال از طریق تغذیه: Upstream conveyors advance a palletized load toward the wrapping cell, stopping at the wrapper entry zone until clear-to-send signals handshake.
- Centering and Positioning: The turntable’s motorized roller deck activates, receiving the pallet and bringing it to rest against a designated optical stop position (±5 mm alignment).
- چرخه بسته بندی: Variable-frequency drives (VFD) rotate the turntable up to 12 RPM using controlled acceleration ramps while the motorized film carriage traverses the load height. Bottom, intermediate, and top reinforcement wraps are executed according to preset parameters (0–99 layers).
- Homing and Alignment: The turntable decelerates into an indexing crawl phase, locking into home position via high-precision proximity sensing so its rollers precisely match the outfeed conveyor datum.
- تخلیه خروجی: The turntable rollers energize, moving the stabilized, wrapped pallet onto the outfeed line while signaling upstream equipment that the station is clear.
Infeed and outfeed roller conveyors are configured to match required floor heights, pallet structural types (Euro, block, or perimeter base), and facility layouts.
Automatic Clamp, Cut, and Wipe Station
At the conclusion of the wrapping sequence, an automated pneumatic mechanical assembly takes control of the stretch film:
- Pneumatic Gripper Clamping: Mechanical scissors-style gripper bars capture the web of the film prior to table stop.
- جداسازی حرارتی: An integrated, regulated impulse hot-wire cutter separates the web cleanly without pulling residual tension against the load.
- پایان دم: A pneumatic mechanical wipe brush brushes the trailing film flat against the pallet face, utilizing the natural cling properties of LLDPE to prevent tail unraveling during transport.
- Next-Cycle Threading: The gripper maintains a firm hold on the leading edge of the film roll, ensuring the carriage is pre-threaded and ready to secure the next incoming load without manual operator intervention.
Wrap Programme and Controls
The B100 is controlled via an industrial PLC paired with an intuitive touch-screen HMI and separate emergency controls:
- Zone Wrap Counters: Bottom wraps, middle layer overlaps, and top waterproofing wraps are set independently from 0 to 99 winds.
- Automatic Height Sensing: An integrated retro-reflective photocell automatically registers pallet load top height, even with irregular dark or translucent corrugated cartons.
- Inverter Motion Tuning: Independent frequency inverters allow separate acceleration/deceleration speed adjustments for both the turntable motor and the vertical mast carriage.
- Carriage Threading Profile: The carriage incorporates an ergonomic “W-path” film threading door, maintaining uniform contact across dual pre-stretch rollers.
B100 Engineering Specifications
| پارامتر | مشخصات / رتبه بندی |
|---|---|
| حالت عملیاتی | Fully Automatic (In-line Integrated) |
| ظرفیت عملیاتی | ≥ 24 loads / hour (depending on wrap recipe and line integration) |
| ظرفیت بار نامی | 1,800 kg dynamic payload (2,000 kg static structural rating) |
| Turntable Deck | 2,200 mm diameter; precision chain drive on heavy-duty slewing ring |
| سرعت چرخش صفحه گردان | Up to 12 RPM (VFD-adjustable acceleration and deceleration) |
| Standard Conveyor Top Height | 400 mm (customizable to existing conveyor systems) |
| Film Roll Parameters | LLDPE; width: 500 mm; film thickness: 20–35 µm (standard: 25 µm); core diameter: 76 mm |
| نسبت پیش کشش نیرو یافته | Standard 250% motorized ratio (100% to 300% fixed gear options) |
| سرعت عمودی کالسکه | Up to 2.9 m/min (inverter controlled) |
| معماری کنترل | Industrial PLC, digital HMI display, push buttons, and line interlock I/O |
| Pneumatic Air Supply | 0.6–0.8 MPa (6–8 bar), dry filtered air |
| منبع برق | AC 380 V, 3-Phase, 50/60 Hz (site-configurable) |
| قدرت درایو نصب شده | Turntable: 0.75 kW; Turntable Rollers: 0.75 kW; Mast Drive: 0.37 kW; Pre-Stretch: 0.37 kW |
Engineering note on load ratings: The turntable frame and slewing ring bearing are mechanically rated for 2,000 kg static load support. The maximum operational rating is certified at 1,800 kg dynamic load under continuous 12 RPM rotation to ensure structural fatigue safety over continuous duty cycles.
Worked Example: Cycle Timing, Line Rate, and Film Yield
The following calculation models a standard shipping pallet running through the B100 under typical packaging parameters.
1. Test Load Parameters
- Pallet Base Dimensions: 1,200 mm × 1,000 mm (Perimeter:
2 × (1.2 + 1.0) = 4.4 m). - ارتفاع بار: 1,400 میلی متر
- الگوی بسته بندی: 2 bottom reinforcement wraps, 3 top reinforcement wraps, 20% overlap pitch.
- سرعت چرخان: 12 RPM (0.2 turns/s, or 5.0 s per full rotation).
- سرعت حرکت کالسکه: 2.9 m/min (0.0483 m/s).
2. Wrapping Sequence Execution Time
- Vertical Mast Travel:
Travel distance (up + down) =
2 × 1.4 m = 2.8 m. Travel time =2.8 m ÷ (2.9 m/min) ≈ 0.965 min ≈ 58 s. - Fixed Reinforcement Wraps:
Bottom (2 wraps) + Top (3 wraps) = 5 wraps.
Fixed rotation time =
5 wraps × 5 s/turn = 25 s. - Motion Profiling Overhead: Soft-start ramp (0 to 12 RPM), homing crawl phase, and pneumatic clamp/cut cycle introduce approximately 8 seconds of kinematic dead-time.
- Net In-Station Wrap Time:
58 s (traverse) + 25 s (dwell) + 8 s (profiling) ≈ 91 s.
3. Station Throughput and Conveyor Allocation
- At a target of 24 loads per hour, each load owns a 150-second cycle budget (
3,600 s ÷ 24). - Available Transfer Buffer:
150 s - 91 s = 59 s. - This 59-second window easily accommodates infeed roller transfer (15 s), outfeed discharge (15 s), and interlock communication margins, fully validating the 24 LPH rating.
4. Film Consumption and Yield Analysis
- Table Rotations during Carriage Movement:
58 s × (12 RPM ÷ 60) = 11.6 rotations. - Total Revolutions per Load:
11.6 (traverse) + 5 (reinforcement) = 16.6 rotations. - Applied Web Length:
16.6 rotations × 4.4 m perimeter ≈ 73 m(applied around perimeter). - Linear Machine-Film Drawn from Roll:
With 250% pre-stretch, 1 meter of raw film elongates to 3.5 meters of wrapping web (Stretch Factor = 3.5).
Raw film consumption per pallet =
73 m ÷ 3.5 ≈ 20.9 m. - Pallets per Roll:
A standard 1,500-meter machine roll (
15 kggross package) yields:1,500 m ÷ 20.9 m/pallet ≈ 71 pallets per roll. - At 24 loads per hour, one film roll supports approximately 3 ساعت کار of non-stop production.
(Note: Calculations provide theoretical first-order baselines. Minor variations occur due to tension relaxation and film neckdown behavior).
چک لیست انتخاب مهندسی
Before finalizing machine dimensions and conveyor transitions, determine the following data:
- پاکت ابعادی: Minimum and maximum pallet width, length, and total load height (including wooden skid).
- Dynamic Weight Range: Lightest load (susceptible to shifting during rotation) and heaviest load (approaching the 1,800 kg limit).
- Hourly Line Throughput: Nominal and peak pallets/hour required from the upstream line.
- Conveyor Datum: Existing plant conveyor top-of-roller height, roller diameter, center pitch, and operational conveying speeds.
- Pallet Structural Flow: Direction of pallet bottom boards relative to conveyor roller orientation (ensuring smooth rolling without bottom board drop-in).
- Electrical and Air Infrastructure: Availability of dry industrial compressed air (0.6–0.8 MPa) and plant electrical service specifications.
Safety Systems and EN 415-6 Compliance
The B100 is engineered to meet EN-415 6، (Safety of Packaging Machines: Pallet Wrapping Machines) and adheres to risk assessment principles under ISO 12100.
Because the machine is an online unit operating within an automated conveyor area, physical hazards include the rotary table, moving carriage mast, and mechanical pinch points at conveyor transitions:
- حفاظ گذاری پیرامونی ماشین آلات: Heavy-duty industrial perimeter fencing isolates the machine operating envelope from foot traffic.
- Muting Safety Light Curtains: Optical curtains protecting infeed/outfeed passages are integrated with conveyor mute sensors, distinguishing pallets passing through the opening from personnel crossing the perimeter.
- قفل های ایمنی: Integrated safety interlock switches on maintenance access doors, Category 4 / PLe emergency stop buttons, and OSHA-compliant lockable electrical disconnect switches.
سوالات متداول مهندسی
Q: How does the turntable roller bed maintain alignment with line conveyors? A: An automated homing routine driven by a VFD positioning profile and high-precision inductive proximity switches slows the turntable from 12 RPM to a creep speed, braking it within ±5 mm of roller alignment.
Q: Can lightweight or unstable boxes be wrapped at 12 RPM without shifting? A: Yes, via programmable VFD acceleration control. Additionally, an optional pneumatic overhead top-platen (stabilizing plate) can be installed to apply downward clamping force during rotation.
Q: What is the primary operational maintenance requirement? A: Regular maintenance is confined to roll changes, cleaning film dust from carriage rollers, checking chain tension, and inspecting the pneumatic cutting wire/wipe brush for wear.
Q: What safety classification applies to the wrapping zone? A: Under EN 415-6, turntable wrappers installed in automated lines require perimeter guarding and optical protection at openings that meet Category 3 / PLd or Category 4 / PLe safety architectures.
گام بعدی
To integrate the B100 into your packaging layout:
- مشخصات خط ارسال: Email your pallet dimensions, minimum/maximum load heights, payload weights, and required line throughput to info@fhopepack.com.
- Receive Line Layout Drawings: Our mechanical design team will provide an integration layout drawing showing roller transition points and fencing placement within 24 hours.
- Review Simulation & Proposal: Receive a formal technical proposal with verified cycle calculations, power load specifications, and factory acceptance test (FAT) parameters.
خواندن مرتبط
- Automatic Pallet Wrapping Machine B100 Product Details
- Online Pallet Wrapping Machine for Big-Sized Products
- Turntable Stretch Wrapper B200 Series
- سیستمهای بستهبندی پالت با صفحه گردان درون خطی
منابع
- OEM Equipment Technical Files: FHOPE Packaging Machine B100 Engineering Specifications
- Operational Video Documentation: Online Turntable Pallet Wrapping Machine Video Archive
- International Packaging Safety Standard: EN 415-6 (Safety of Packaging Machines: Pallet Wrapping Machines)
- Risk Reduction Standards: ISO 12100:2010 (ایمنی ماشین آلات - اصول کلی برای طراحی)
آخرین بررسی فنی: 2026-10-24