خلاصه اجرایی A pallet secured solely by manual operator tension inevitably fails under dynamic transport stress: shift-to-shift physical fatigue yields unpredictable containment force and repeated cargo displacement. An industrial automatic turntable pallet stretch wrapper replaces manual variance with rigid, programmable cycle mechanics. As the load rotates on an engineering-grade turntable, a powered pre-stretch carriage travels the vertical mast, applying high-performance stretch film at controlled elongation ratios, precise overlap percentages, and calibrated containment tension. Matched to specific load footprints, payload ratings, and pre-stretch dynamics, this equipment establishes consistent structural load stability across continuous multi-shift distribution cycles.
فهرست مندرجات
- چرا مهار بار اهمیت دارد؟
- بستهبندی دستی در مقابل بستهبندی اتوماتیک
- نحوه اجرای چرخه بسته بندی
- عناصر اصلی
- پیکربندی معمولی
- صرفهجویی در پیشکشش و فیلم
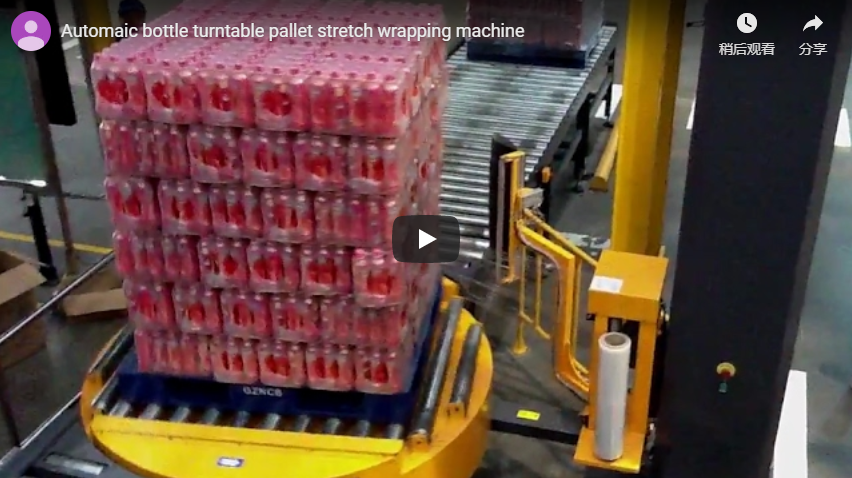
- چیزی که ویدیو نشان می دهد
- چک لیست انتخاب ماشین
- کنترلها و ایمنی
- سوالات متداول مهندسی
- مرحله بعدی
- خواندن مرتبط
- منابع و استانداردها
چرا مهار بار اهمیت دارد؟
Cargo integrity failures in transit generate compounding costs: primary product crushing or interlayer displacement at the vehicle floor, followed by high manual handling fees for emergency restacking at receiving docks. During transit, palletized units encounter continuous three-axis vibration, acceleration, and centrifugal cornering loads. Without sufficient containment force, individual carton layers break friction and walk apart.
True transport load containment does not rely on raw holding pull; it depends on a predictable, engineered envelope. Three mechanical parameters determine success:
- Primary film pre-stretch: The molecular elongation of the film prior to product contact, converting elasticity into working yield strength.
- Applied wrap tension: Dynamic secondary force matching the compressive strength of the cargo walls without corner crush.
- Programmed layer counts and overlap: Continuous mechanical banding locking the bottom cargo layers securely to the timber or plastic pallet base.
Maintaining these parameters precisely constant across every production batch eliminates transit load movement while optimizing resin consumption.
بستهبندی دستی در مقابل بستهبندی اتوماتیک
Manual hand-wrapping leaves tension entirely to operator fatigue and reach angles. Line audits consistently show tension decay from the beginning to the end of a shift: low rolls cause back strain, resulting in insufficient base-lock turns, while high reaches lead to uneven neck-down and loose top layers. Containment consistency drops below 40%, creating high product damage rates in supply chains.
| پارامتر عملیاتی | Manual Hand Wrapping | دستگاه استرچ رپ اتوماتیک چرخشی |
|---|---|---|
| نسبت قبل از کشش | 0% to 15% (unassisted yield) | 200% to 300% (driven dual-roller mechanism) |
| قوام فیلم | Highly variable; degrades with shift fatigue | ±2% repeatability across pre-set PLC programs |
| Pallet Base Locking | Often skipped or loose due to ergonomic strain | Exact mechanical wrap counts directly to the pallet base |
| ایمنی اپراتور | High risk of lumbar fatigue and repetitive strain | Fully hands-off wrapping sequence outside rotating cell |
| Film Waste per Pallet | High (excessive gauge used to compensate tension) | Minimized resin mass per unit with pre-stretched film |
An automatic turntable stretch wrapper executes an exact PLC program for every pallet. Speeds, wrap counts, and film tensions remain perfectly repeatable, eliminating manual variance from the operational budget.
نحوه اجرای چرخه بسته بندی
The operational cycle follows a precise mechanical and electrical sequence:
[Pallet Infeed: Forklift / Conveyor]
               │
               ▼
[Film Tail Anchor & Position Detection via Optical Sensor]
               │
               ▼
[Soft-Start Turntable Rotation & Base Reinforcement Wraps]
               │
               ▼
[Mast Carriage Vertical Ascent with Controlled Film Overlap]
               │
               ▼
[Top Stabilization Wraps + Downward Reinforcement Pass]
               │
               ▼
[Deceleration, Orientation Stop, Auto Film Cut & Wipe-Down]- Infeed & Placement: The pallet load is placed onto the turntable surface by forklift, pallet truck (via ramp), or automated infeed conveyor.
- شروع چرخه: The safety circuit confirms perimeter clearance. The operator triggers start via remote pendant or panel button.
- Controlled Base Lock: The turntable accelerates through a variable frequency drive (VFD) soft-start curve. The powered film carriage rotates at low height to apply 2 to 5 high-tension wraps anchoring the cargo directly to the pallet footing.
- Ascent and Layer Overlap: The mast carriage climbs via heavy-duty chain or belt drive at a fixed vertical velocity, laying film with a 30% to 50% pitch overlap.
- Top Sensing & Reinforcement: An optical sensor detects the top edge of the load. The machine applies programmed top stabilization wraps, then reverses carriage travel down to complete a double-wrap cross pattern.
- Deceleration & Cut-Wipe: The turntable decelerates smoothly, stopping at its original home position (±5 mm). The pneumatic clamp and hot-wire or mechanical knife sever the film, pressing the trailing edge flush against the load wall.
عناصر اصلی
An industrial turntable stretch wrapper integrates structural, mechanical, and electrical sub-assemblies engineered for continuous duty:
- Heavy-Duty Turntable Assembly: Driven by a high-efficiency motor and industrial worm gearbox through heavy-duty roller chain transmission. The top plate is supported by heavy-load nylon tracking castors to absorb dynamic shock loading from forklift placement.
- Powered Pre-Stretch Film Carriage: Houses two precision polyurethane-coated rollers driven by fixed-ratio internal gearing. A separate variable-speed motor stretches the film up to 300% before it exits the carriage. An integrated dancer arm monitors film tension, dynamically compensating for corner speed spikes on rectangular loads.
- Structural Mast & Lift Mechanism: Cold-formed steel mast section housing an enclosed lift chain, counterweight, and drop-prevention safety catch to arrest carriage fall in the event of chain slack.
- Optical Sensing Suite: Carriage-mounted retro-reflective photocell automatically registers load height. Specialized diffuse or polarized sensors are fitted for dark, glossy, or transparent stretch loads.
- Central PLC Control Architecture: Industrial PLC running optimized motion sequences, paired with a user-friendly HMI screen storing recipe profiles for variable cargo configurations.
پیکربندی معمولی
Turntable wrappers are configured to match specific plant line speeds, spatial envelopes, and pallet load matrices.
| Operational Specification | Standard Platform Envelope | گزینه سنگین / توسعهیافته |
|---|---|---|
| قطر چرخان | 1500 میلی متر تا 1650 میلی متر | 1800 میلی متر تا 2000 میلی متر |
| ظرفیت بار نامی | 1500 کیلوگرم تا 2000 کیلوگرم | تا 2500 کیلوگرم |
| حداکثر ارتفاع بار | 2100 میلی متر تا 2400 میلی متر | Up to 2800 mm (extended mast) |
| سرعت چرخش گردان | 3 to 12 RPM (VFD-regulated) | 3 to 15 RPM (high-throughput lines) |
| قابلیت پیش کشش | 200% to 250% standard | Up to 300% high-efficiency gearing |
| Film Carriage Drive | Chain drive with safety catch | Dual-track reinforced mast drive |
| Applicable Film Width | 500 mm (standard cast/blown film) | 500 میلی متر تا 750 میلی متر |
| معماری برق | 220V 1-Phase / 380V 3-Phase (50/60 Hz) | Engineered to facility incoming line |
Kinematic Clearances & Diagonal Sizing Rule
Selecting turntable diameter strictly requires accounting for diagonal sweep and forklift placement offset. The design formula is:
D_turntable ≥ √(Length² + Width²) + 2 × Clearance_margin
- EUR-1 Pallet (1200 × 800 mm): Diagonal =
√(1200² + 800²) ≈ 1442 mm. Adding a minimum2 × 50 mmmargin yields1542 mm، ساختن یک 1650 mm turntable the safe standard to prevent corner overhang hazards. - Industrial Pallet (1200 × 1000 mm): Diagonal =
√(1200² + 1000²) ≈ 1562 mm. افزودن a2 × 50 mmmargin yields1662 mm، نیازمند الف 1650 mm to 1800 mm turntable to accommodate forklift loading tolerances.
صرفهجویی در پیشکشش و فیلم
Powered pre-stretch operates by routing the film around two geared rollers turning at differential surface speeds:
Pre-stretch Ratio (%) = [(Roller_2_Speed - Roller_1_Speed) / Roller_1_Speed] × 100
At a 250% pre-stretch setting, 1 meter of raw film from the supply roll elongates into 3.5 meters of usable film applied onto the load.
[Raw Film Roll: 1.0 m] ──> [Slow Roller 1] ──> [Fast Roller 2 (3.5x)] ──> [Stretched Film: 3.5 m on Pallet]- Resin Mass Reduction: Dramatically lowers consumable film weight per pallet wrapped compared to friction-brake or hand-applied films.
- High Yield & Memory Effect: Extending LLDPE film into its plastic yield point activates its natural elastic recovery, locking product layers tightly together as the film attempts to contract post-wrap.
- Corner Force Mitigation: A calibrated dancer roller adjusts output tension during rectangular rotation, eliminating edge puncture on sharp corrugated carton corners.
- Base Locking Band: Setting 3 to 4 turns of film directly across the interface between the timber skid and bottom layer ensures load-to-pallet unity during high-g truck braking.
چیزی که ویدیو نشان می دهد
The engineering footage displays the shop-floor functional testing and commissioning sequence of a heavy-duty turntable wrapping cell:
- Initial Setup & Threading: Assembly personnel configure the pneumatic supply and verify proper film routing through the dual polyurethane pre-stretch rollers and dancer arm compensator.
- Low-Profile Turntable Rotation: The machine runs a test load on a low-profile turntable plate, demonstrating smooth VFD acceleration and minimal rotational deflection under solid payload blocks.
- Photoelectric Calibration: Engineers test load-height photocell responsiveness, verifying proper optical cutoff at top edges under varying wrap surface reflections.
- Coordinated Axis Travel: The video captures the synchronized relation between mast elevation drive and rotational speed, establishing the constant 40% vertical film overlap essential for dynamic transport containment.
چک لیست انتخاب ماشین
Use this engineering criteria table during initial layout qualification:
| عامل ارزیابی | Engineering Parameter to Confirm | Line Integration Impact |
|---|---|---|
| Max Pallet Footprint | Max diagonal dimension including cargo overhang | Sets minimum turntable diameter and perimeter fence clearance |
| Dead Weight Max | Heaviest pallet gross weight (kg) | Dictates center-bearing rating and drive gear torque selection |
| حداکثر ارتفاع پشته | Highest package elevation + pallet height | Determines mast height and lift chain length |
| پایداری بار | Top-heavy, lightweight, or unstable cartons | Determines need for pneumatic top platen/stabilizer plate |
| Cell Integration | Forklift loading vs. automatic roller conveyor | Dictates stand-alone ramps vs. auto-infeed handshake logic |
| وظیفه زیستمحیطی | Clean warehouse, cold storage (-20°C), or dusty | Selects motor IP rating, low-temp lubricants, and cabinet heating |
کنترلها و ایمنی
Turntable packaging machines operate under strict industrial safety criteria to protect plant personnel from rotating machinery hazards:
- Operational Safety Zone: Safe physical separation must be maintained around the turntable perimeter. Optical light curtains, perimeter pressure mats, or fixed metal interlocked fencing prevent personnel entry during automatic spinning.
- Drive Overload & Slack Chain Arrest: The mast features mechanical limit switches and slack-chain detection. If an obstruction blocks carriage downward travel, the drive motor cuts out instantly to prevent cable bird-nesting or carriage drop.
- یکپارچهسازی توقف اضطراری: Hardwired Category 0 E-stop buttons reside on the main panel and optional remote control pendants, wired to monitored safety relays.
- استانداردهای انطباق:
- EN-415 6،: Specific European Type-C standard governing pallet wrapping equipment design and interlocking.
- ISO 12100: 2010: Comprehensive machinery risk assessment and reduction methodology.
- EN ISO 13849-1: 2023: Safety-related parts of control systems, targeting Performance Level d (PLd) for emergency stop and interlock circuits.
- OSHA 1910.212: General machine guarding requirements for rotating turntables in North American facilities.
سوالات متداول مهندسی
Q: Can this turntable wrapper run lightweight, unstable products without tipping them? A: Yes. By setting variable frequency drive (VFD) acceleration curves to soft-start and pairing them with an optional pneumatic overhead top-clamp platen, the machine holds tall, low-mass cartons stable while initial base locking wraps are established.
Q: How is the correct turntable diameter verified for custom skids?
A: Calculate the true diagonal of the pallet including any box overhang: √(Length² + Width²). Add at least 100 mm to 150 mm to account for off-center forklift placement. If your diagonal exceeds 1550 mm, select an 1800 mm or 2000 mm turntable.
Q: What is the maintenance cycle for the powered pre-stretch carriage? A: The polyurethane-coated pre-stretch rollers require cleaning with isopropyl alcohol every 100 operating hours to remove film tackifier buildup. The mast lift chain requires visual tension inspection monthly and lubrication every 500 operating hours.
Q: Does dark or glossy stretch film cause load-height sensing issues? A: Standard diffuse sensors can misread mirrored surfaces or deep-black packaging. For lines running pigmented black stretch film or glossy printed cartons, we integrate retro-reflective polarized photocells or ultrasonic distance sensors to guarantee edge detection.
Q: Can this machine be integrated into a fully automated unmanned conveyor cell? A: Yes. The turntable can be equipped with an integrated powered roller or chain conveyor deck, pneumatic film clamp-and-cut mechanisms, and dry-contact PLC handshakes to link directly with plant central upstream palletizers and downstream stretch hooders.
مرحله بعدی
- Submit Facility Specifications: Send your pallet footprints (L × W × H), maximum payload weight, and hourly target output to info@fhopepack.com.
- Receive Engineering Analysis: Our engineering department will return a 2D layout drawing, turntable sizing validation, and film pre-stretch ROI calculation within ساعت 48.
- بررسی پروژه: Schedule a video conference with our packaging machine specialists to finalize control specifications, safety guarding envelopes, and factory delivery schedules.
خواندن مرتبط
- خط دستگاه بسته بندی پالت اتوماتیک با صفحه گردان
- Rotary Arm Pallet Stretch Wrapper Machinery
- Fully Automatic Rotary Arm Pallet Wrapping and Packing Cell
- Semi-Automatic Pallet Wrapping Equipment Series
- Industrial Packing Machinery Full Product Catalog
منابع و استانداردها
- Engineering documentation and turntable machine design criteria: FHOPE Technical Machine Index
- Machine platform operational references: FHOPE B200 Automatic Pallet Stretch Wrapper, FHOPE A300 Heavy-Duty Pallet Wrapper, FHOPE B100 Turntable System
- EN-415 6،: Safety of packaging machines — Part 6: Pallet wrapping machines.
- ISO 12100: 2010ایمنی ماشین آلات - اصول کلی طراحی - ارزیابی ریسک و کاهش ریسک.
- EN ISO 13849-1: 2023: Safety of machinery — Safety-related parts of control systems.
- EUMOS 40509 / ASTM D4649: Test methodology for transport packaging and load containment verification.
آخرین بررسی: 2026-10-24