خلاصه اجرایی High-speed coil slitting lines produce narrow steel strips at rates that downstream offline packaging often struggles to match. This engineering guide details the integration of a 90° turnstile downender, an eye-to-sky orbital stretch wrapper, and an automated gantry stacker linked by dynamic powered roller buffer conveyors. By decoupling slitter recoiler cycle times from periodic packaging stoppages—such as stretch film roll changeovers, strapping coil replenishment, and stack offloading—conveyor buffers eliminate slitter downtime. Below, we break down buffer capacity calculations, kinematic transitions across stations, selection rules, and international safety compliance.
Why Buffer Sections Between Stations Matter
In continuous metal processing, the slitter head and recoiler mandrel represent significant capital expenditure. Stopping a slitter due to a bottleneck at downstream packaging introduces heat marks, tension release scratches, and drastic overall equipment effectiveness (OEE) losses. Integrating powered conveyor buffer zones between the upender/downender, orbital wrapper, and gantry stacker directly resolves this mismatch.
- Absorption of Intermittent Stops: Routine maintenance events, film reel changeovers (2–4 minutes), and strapping dispenser reloading are absorbed entirely within the queue without triggering slitter line stops.
- Asynchronous Station Cycling: Each automated cell executes operations based on optical sensor triggers rather than a rigid mechanical cycle. The downender tilts, the wrapper rotates, and the portal stacker picks independently.
- Continuous Slitter Recoiler Discharge: Slit coils vacate the recoil turnstile arm without delay, allowing the crane or coil car to prepare for the subsequent master coil change.
- Reduction of Dynamic Wear: Eliminating constant start-stop operation protects AC motor drives, gearbox reducers, and heavy roller chains from alternating fatigue loads.
Without calculated buffer capacity, any micro-stoppage down the line cascades upstream immediately, forcing slitter operators to idle the knives or cut short coils.
[Slitter Recoil Turnstile]
          │ (Eye-Horizontal Bore)
          ▼
[90° Hydraulic Downender]
          │ (Eye-to-Sky Orientation)
          ▼
┌─────────────────────────────────┐
│ Buffer Zone 1: Infeed Powered   │ <── Absorbs Downender-to-Wrapper Delta
│ Polyurethane Rollers (VFD)      │
└─────────────────────────────────┘
          │
          ▼
[Eye-Through Orbital Ring Wrapper]
          │
          ▼
┌─────────────────────────────────┐
│ Buffer Zone 2: Intermediate     │ <── Absorbs Film Change / Inspection Time
│ Centering Roller Queue          │
└─────────────────────────────────┘
          │
          ▼
[Gantry Stacking & Palletizing]
          │
          ▼
[Discharge Staged Pallet Conveyor]
نحوه کار خط
| ایستگاه | Core Mechanical Subsystem | Function & Kinematics |
|---|---|---|
| Downending / Tilting | 90° hydraulic tilting saddle on slew base | Strips coils from the turnstile arm (eye-horizontal) and tilts them 90° to vertical bore (eye-to-sky) on powered rollers. |
| Infeed Buffer Conveyor | Variable frequency drive (VFD) heavy-duty roller table | Stages multiple coils sequentially; polyurethane-sleeved rollers prevent strip edge deformation. |
| Eye-Through Orbital Wrapping | Vertically guided rotary ring with film carriage | Opens roller gaps; the shuttle ring orbits through the coil center hole, applying helical stretch film under controlled tension. |
| Intermediate Accumulator | Zoned sensor-driven accumulation conveyor | Provides queuing between wrapping and palletizing; matches high wrapping cycle speed to stacker cycle speed. |
| Overhead Gantry Stacking | Portal mechanical scissor clamp or magnetic/vacuum grab | Traverses along X-Z axes, centers above the wrapped coil, picks, and nests coils onto timber pallets up to load height limits. |
The process begins at the turnstile exit. The hydraulic downender engages the coil through its horizontal bore, rotates 90°, and places it onto the powered roller conveyor in an eye-to-sky orientation.
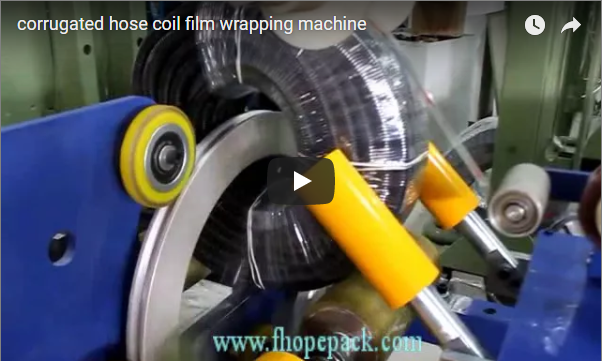
Next, the coil enters the eye-through orbital wrapper. A specialized split roller table supports and rotates the coil about its vertical center while a motorized orbital ring drives the film dispenser through the bore. This encapsulates the outer wall, side faces, and inner eye with overlapping LLDPE/VCI stretch film.
Once wrapped, the coil advances along the secondary buffer to the gantry stacker, which organizes units into neat pallet stacks ready for final strapping, banding, or automated warehousing.
Calculating Buffer Length
Conveyor buffer sizing dictates whether a packaging line succeeds in decoupling downstream stoppages from upstream cutting. The accumulated length must accommodate all incoming coils generated during the maximum single-operator intervention duration.
Core Sizing Formula
N_buffer = ceil( (T_stop / T_slitter) × S_f )
L_buffer = N_buffer × (OD_max + C_gap)- N_buffer: Minimum number of buffer storage positions required.
- T_stop: Longest predicted downstream offline stoppage (minutes).
- T_slitter: Cycle time interval between coils exiting the slitter (minutes/coil).
- S_f: Safety margin factor (typically 1.15 to 1.20 to account for conveyor acceleration/deceleration lags).
- OD_max: Maximum coil outer diameter (mm).
- C_gap: Minimum physical clearance gap maintained between coils by photo-eye sensors (typically 200–300 mm).
مثال مهندسی کاربردی
| پارامتر | نشانه گذاری | ارزش پایه | واحد |
|---|---|---|---|
| Slitter Recoil Output Rate | 1 / T_slitter | 1.0 (1 coil every 60 seconds) | coils/min |
| Maximum Target Downstream Stop (Film Changeover) | T_stop | 5.0 | دقیقه |
| Engineering Safety Factor | S_f | 1.2 | بدون بعد |
| Calculated Holding Capacity | N_buffer | ceil((5.0 / 1.0) × 1.2) = 6 | کویل |
| حداکثر قطر بیرونی کویل | OD_max | 1,250 | mm |
| Sensor Clearance Gap | C_gap | 250 | mm |
| Pitch Length Per Coil Position | L_pitch | OD_max + C_gap = 1,500 | mm |
| Total Effective Buffer Conveyor Length | L_buffer | 6 1,500 9,000 = XNUMX | mm |
When floor layout constraints prevent a linear 9.0-meter conveyor run, engineers implement 90° powered turntable diverters or parallel multi-strand roller accumulator tables to maintain identical coil buffer counts within a compact footprint.
What We Set Per Line
Standard packaging configurations cannot handle all coil gauges and line speeds. Machine parameters are systematically configured according to operational variables:
| Machine Subsystem | Adjustable Setting / Hardware Variable | Engineering Determinant |
|---|---|---|
| Conveyor Buffers | Length, roller pitch, drive power (kW), and VFD speed (6–18 m/min) | Slitter cycle speed, maximum stop allowance, and coil strip width/mass. |
| داوندر | Hydraulic cylinder bore, hydraulic counterbalance valve, saddle geometry | Maximum coil weight (1,000–10,000 kg), strip width (20–500 mm), and coil ID/OD. |
| Rotary Wrapper | Pre-stretch ratio (150%–250%), ring RPM (30–80 RPM), film overlap (20%–70%) | Moisture barrier specifications, sea freight corrosion risks (VCI integration), and throughput requirements. |
| Gantry Stacker | Portal payload, hoist stroke, tooling type (scissor ID grip vs. OD perimeter jaws) | Stack weight ceiling (typically 3,000–5,000 kg per pallet), pallet footprint, and stack height limit. |
| واحد تسمهکشی شعاعی | Number of PET/Steel radial straps through the eye (2, 3, or 4 bands) | Structural integrity against axial telescoping during long-haul transport. |
چک لیست انتخاب
Prior to requesting formal technical engineering drawings, ensure your facility parameters are documented across the following operational criteria:
- پاکت ابعادی کویل: Minimum and maximum Outer Diameter (OD), Inner Diameter (ID), strip width, and individual coil weight range.
- Upstream Output Cycle: Peak coils-per-hour leaving the slitting head recoiler.
- Target Offline Duration: Worst-case downstream stoppage time to absorb (manual film roll swap, strapping restock, label application).
- Available Floor Footprint: Overall building length, width, ceiling hook height, and overhead crane clearances.
- Packaging Material Specs: Stretch film width (100–250 mm), micron thickness (20–35 µm), VCI paper needs, or woven HDPE wrap.
- الزامات تسمه کشی: Determination if coils require bare-metal radial strapping through the eye prior to wrapping.
- Palletizing Configuration: Wood pallet sizes, target stack height (including runner/skid), and manual vs. automatic timber runner placement.
- دستورالعملهای نظارتی: Compliance needs for local plant mandates (CE marking, UL/CSA panel build, OSHA safety guarding).
Safety Architecture & Compliance
Heavy moving steel coils present serious pinch-point and crush hazards. Packaging lines require strict adherence to international safety protocols:
- Separation of Hazards: The hydraulic downender, orbital ring wrapper, and portal gantry stacker must be isolated behind interlocked 2,000 mm steel perimeter fence panels conforming to ISO 14120.
- Optical Guarding: Light curtains (Type 4, Performance Level d/e per ISO 13849-1) monitor buffer infeed and discharge zones. Beam interruption halts powered equipment drives instantly.
- Zero Energy State (LOTO): Individual air dump valves (pneumatics) and mechanical locking pins on hydraulic tilting arms ensure verified Lockout/Tagout capability under OSHA 1910.147 guidelines.
- Applicable Technical Standards:
- ISO 12100: 2010ایمنی ماشین آلات - اصول کلی طراحی - ارزیابی ریسک و کاهش ریسک.
- EN 415-10: 2014: Safety of packaging machines — Part 10: General requirements and integrated packaging lines.
- EN-60204 1،: Electrical equipment of machines.
سوالات متداول مهندسی
Q: Why are buffer roller conveyors positioned before and after the wrapper? A: Positioning buffers on both sides of the orbital wrapper separates the line into three independent operating zones: upending, wrapping, and stacking. If the stacker waits for a pallet exchange, the wrapper keeps running. If the wrapper stops for a film change, the downender continues unloading the slitter.
Q: How does the conveyor avoid scratching the outer strip wraps? A: Rollers are precision-machined steel coated with heavy-wall polyurethane (PU) or high-density vulcanized rubber. Conveyor starts and stops are controlled by VFD S-curve acceleration profiles to eliminate skidding and friction scuffs.
Q: Does the system handle both eye-horizontal and eye-to-sky slit coils? A: Slit coils exit the slitting recoiler with their bore horizontal on an arbor or turnstile. The downender tilts them 90° into an eye-to-sky position, which is the international standard for flat roller transport, eye-through wrapping, and stable pallet stacking.
Q: What tooling does the gantry stacker use to lift wrapped coils without damaging the film? A: The stacker employs smooth polyurethane-lined internal expansion scissor shoes or surface-contact vacuum suction pads. This grips the coil firmly without puncturing the protective plastic film layers.
Q: Can these buffer sections be integrated into existing slitter lines? A: Yes. Provided floor length permits, modular powered roller conveyors can be retrofitted between an existing downender and downstream strapping or palletizing stations using standard fieldbus communications (Profinet, Ethernet/IP).
Q: What ensures the coils remain centered on the roller conveyors? A: Pneumatic self-centering side guide arms or V-shaped roller segments automatically align coils along the conveyor center line before entry into the wrapping and stacking stations.
گام بعدی
Our engineering department develops customized layouts and cycle time analyses for slitting and packaging lines in three straightforward steps:
- Submit Your Layout & Parameters: Email your factory layout drawing, coil dimensions (ID/OD/Width/Weight), and slitter production rates to info@fhopepack.com.
- Receive Engineering Concept within 48 Hours: We deliver a detailed 3D layout proposal, formal buffer capacity calculations, and a complete cycle time chart.
- Site & Interface Review: Our project engineers collaborate directly with your team to align conveyor heights, turnstile centerlines, electrical interfaces, and safety interlocks with your slitter setup.
خواندن مرتبط
- خط بستهبندی و انباشت کویل شکافدار، کج کردن کویل از طریق چشم
- Narrow Steel Coil Packing Line Engineering Strategies
- Automatic Steel Coil Stacking and Palletizing Gantry Systems
- Slit Coil Packing Line Technical Specifications — Product Directory
منابع
- Engineering Documentation: FHOPE Machine Research & Packaging Automation Group.
- مرجع ویدئو: FHOPE Fully Automated Slit Coil Handling, Wrapping, and Stacking Line Demonstration.
- Safety Directives: ISO 12100:2010 (Safety of Machinery Risk Assessment); EN 415-10: 2014 (Packaging Machine Safety Requirements).
- Kinematic Formulas: FHOPE Technical Handbook on Industrial Coil Handling & Continuous Buffer Calculations.
آخرین بررسی: 2026-10-27