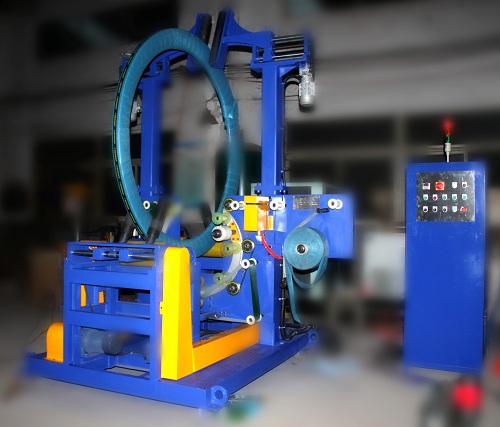
خلاصه اجرایی A two-stage coil packaging line decouples wrapping and stacking into two synchronized automated stations. Stage one applies protective packaging through the eye of the coil using an orbital ring wrapper, while stage two transfers the wrapped coils with an overhead gantry manipulator to form stable eye-to-sky stacks. This separation balances cycle times and prevents downstream handling damage.
فهرست مندرجات
- پاسخ کوتاه
- کاری که دستگاه انجام میدهد
- مرحله اول: حلقه پیچی
- مرحله دوم: دروازه بالای سر
- چه چیزی سرعت خط را تعیین میکند؟
- محدوده کویل برای خطوط تغذیه شده با نوار نقاله
- چک لیست انتخاب برای خط تولید دو مرحله ای
- کنترلها و ایمنی
- سوالات متداول مهندسی
- مرحله بعدی
- خواندن مرتبط
- منابع
پاسخ کوتاه
- A slit coil arrives flat (eye-to-sky) on a powered roller conveyor without requiring an upender.
- An orbital ring wrapper shuttles protective wrap through the coil bore while motorized rollers rotate the coil, sealing the outer diameter, inner bore, and both side faces.
- The wrapped coil indexes downstream via roller conveyor directly into the overhead gantry pick-up station.
- The gantry stacker engages the coil perimeter, lifts it vertically, and deposits it onto a pallet or dedicated stacking station.
- The completed multi-coil stack exits the packaging cell on heavy-duty conveyors for forklift or crane dispatch.
کاری که دستگاه انجام میدهد
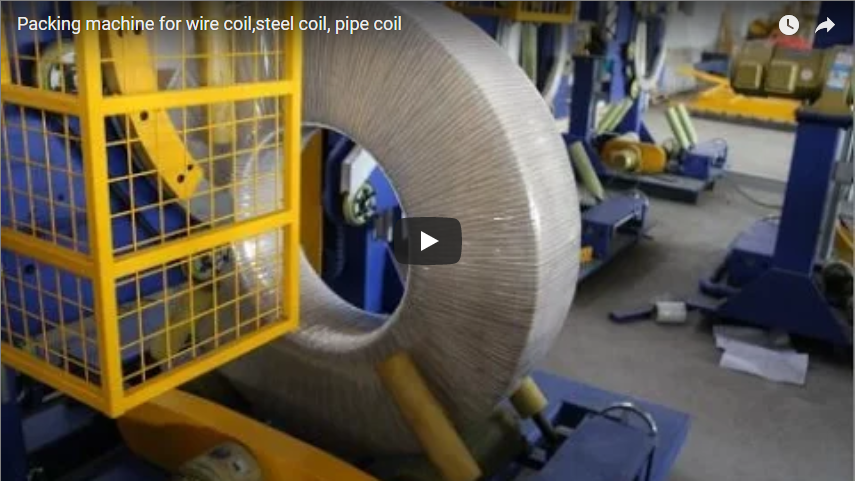
The system processes slit steel coils in an eye-to-sky orientation. Coils travel along a powered roller platform directly into a high-speed orbital ring wrapper, which guides stretch wrap or protective film through the coil center.
Downstream from the wrapping station, a heavy-duty overhead gantry lowers custom mechanical gripper arms over the wrapped unit. The gantry lifts the coil straight up, travels horizontally, and deposits it precisely onto an accumulation stack. By separating eye-through wrapping from vertical pallet stacking, each mechanical station operates independently without cycle-time interference.
مرحله اول: حلقه پیچی
The orbital ring carries the film dispenser shuttle on precision track rollers and traverses through the open coil eye on every rotation. As the ring rotates, support rollers beneath the coil turn it about its vertical axis, creating a uniform helical overlap across successive layers. Once the coil completes a 360° rotation on the rollers, the stretch film fully encapsulates the outer diameter (OD), inner bore (ID), and both flat side faces.
Integrated PLC and touch-screen HMI controls allow operators to adjust centering, film pre-stretch tension, and overlap percentage (typically adjustable between 20% and 90%) according to coil specifications. The station accommodates stretch film, paper wrap, or woven compound tape, and can be integrated with automated radial/circumferential strapping units as well as inline ERP/MES barcode labeling systems.
مرحله دوم: دروازه بالای سر
Once fully wrapped, slit coils require precise transfer without compromising the newly applied protective layers. The overhead gantry stacker automates this handling from above, eliminating the need for manual hoist hooks or forklift interventions inside the automated perimeter.
- بازوهای چنگک در لبه بیرونی بسته میشوند of the coil using regulated mechanical clamping to prevent film tearing or coil edge distortion.
- کالسکه، کویل را مستقیماً بالا میبرد, travels along overhead structural beams, and accurately lowers the unit onto a target pallet or floor position.
- پشته به آسمان نگاه میکند, accommodating up to 6 coils per stack on our automatic coil packing line based on specified coil widths and weight limitations.
Custom gripper heads are tailored to the exact coil dimension envelope and surface finish requirements specified for each plant layout.
چه چیزی سرعت خط را تعیین میکند؟
A two-stage line operates according to the cycle time of its slowest bottleneck station. In typical operations, this is governed either by the ring wrapper (which requires a complete rotational cycle of the coil) or by the overhead gantry (which performs dedicated pick, transfer, deposit, and return strokes).
| اگر کندترین ایستگاه | رفع مشکل معمولی |
|---|---|
| حلقه بسته بندی | Adjust overlap percentage or wrap layers to the minimum required for transport protection. |
| استکر دروازهای | Minimize carriage travel distance by locating stack accumulation positions adjacent to the conveyor. |
| نوار نقاله خروجی | Integrate powered accumulation buffer conveyors to hold finished stacks during forklift transit. |
Target coils-per-hour requirements determine the rotational speed of the wrapping ring, gantry axis acceleration, and intermediate conveyor buffer lengths.
محدوده کویل برای خطوط تغذیه شده با نوار نقاله
Standard conveyor-loaded orbital wrapper specifications:
| مدل | کویل ID | سیم پیچ OD | عرض سیم پیچ | حداکثر وزن کویل |
|---|---|---|---|---|
| FPCA-1000 | 508 / 610 میلی متر | 700-1600 میلی متر | 20-400 میلی متر | کیلوگرم ۷۳۰۰ |
| FPCA-1200 | 508-610 میلی متر | 800-1400 میلی متر | 20-500 میلی متر | کیلوگرم ۷۳۰۰ |
These conveyor-fed models are engineered for horizontal slit coil packaging. All dimensions and capacities represent standard machine frames; custom systems are adapted to specific industrial coil ranges.
چک لیست انتخاب برای خط تولید دو مرحله ای
- Required throughput (coils per hour, accounting for peak production shifts).
- Complete coil dimensional envelope: ID, OD, slit width range, and maximum unit weight.
- Wrapping media selection (stretch film, VCI anti-corrosion film, crepe paper, or woven tape), target overlap percentage, and strapping requirements.
- Maximum stack height, maximum pallet weight, and target stacking configurations.
- Available shop-floor footprint for buffer conveyors, pallet infeed, and stack discharge tables.
- Factory automation protocols: fieldbus networks, ERP/MES production tracking, and automated labeling integration.
کنترلها و ایمنی
System safety depends on regional compliance standards and factory safety classifications. For CE-marked installations, ISO 12100 provides the overarching risk-assessment framework, while EN 415-10 defines the specific safety requirements for automated packaging machinery, dictating perimeter guarding, access interlocks, and emergency-stop circuit architecture.
The high-speed orbital wrapping ring and the linear overhead gantry both constitute dynamic mechanical zones. Machine layouts feature physical perimeter fencing, light curtains at conveyor transfer apertures, and category 4 / PLe safety interlocks evaluated through comprehensive layout risk assessments.
سوالات متداول مهندسی
Q: Why use two stages instead of a single combi-machine? A: Splitting wrapping and stacking into independent stations allows simultaneous processing of adjacent coils. While the gantry stacks a previously wrapped unit, the ring wrapper encapsulates the next inbound coil, maximizing line throughput and keeping mechanical assemblies modular.
Q: How many coils go in a single stack? A: Up to 6 coils per stack on our automatic coil packing lines, depending on coil slit width, total package weight, and downstream warehouse handling limits.
Q: How does the gantry avoid damaging the fresh wrap? A: The custom gripper head applies controlled radial clamping force exclusively to the outer circumference of the coil and performs a true vertical lift. This eliminates internal bore contact, friction chafing, and sling damage.
Q: Which coil widths suit a conveyor-fed line? A: Our standard FPCA-1000 processes widths from 20 to 400 mm, while the FPCA-1200 handles widths from 20 to 500 mm.
Q: Can the line apply automated tracking labels to each coil? A: Yes. Inline ERP/MES automated print-and-apply labeling stations can be integrated along the transfer conveyor between the wrapping and stacking operations.
Q: What decides the overall line cycle time? A: The line speed is governed by the critical path cycle time of either the ring wrapper or the gantry stacker. Target throughput in coils per hour establishes the required ring RPM, conveyor index speed, and gantry motion profiles.
مرحله بعدی
We engineer turnkey two-stage coil packaging lines through a structured process:
- طرح چیدمان خود را ارسال کنید including target coils per hour, coil dimensional parameters, and stack requirements to info@fhopepack.com.
- دریافت پیشنهاد ظرف ۴۸ ساعت, including machine sizing, conveyor footprints, gantry travel spans, and layout drawings.
- رزرو نظرسنجی در سایت to confirm plant floor clearances, foundation requirements, utility supplies, and forklift traffic paths.
خواندن مرتبط
- خط بسته بندی و انباشتگی کشش کویل شکاف دار: حلقه از طریق چشم به دستگاه انباشتگر گانتری
- خط بستهبندی کویل مسی دو مرحلهای: بستهبندی از طریق چشم، سپس چیدن روی ریلهای چوبی
- خط بستهبندی کویل فولاد از تسمهکشی تا انبارداری: پنج معیار بازگشت سرمایه و فرمول بازگشت سرمایه
- خط بسته بندی کویل اتوماتیک
منابع
- Machine operational reference: Automatic Steel Coil Stretch Wrapping Machine and Stacker on YouTube
- Automatic coil packing line specifications (stacking parameters, HMI control of tension and overlap, ERP/MES options): خط بسته بندی کویل اتوماتیک
- FPCA-1000 and FPCA-1200 dimensional tables: دستگاه بسته بندی کلاف فولادی
- Machinery safety directives: ISO 12100:2010 (Safety of machinery — General principles for design); EN 415-10: 2014 (Safety of packaging machines — General requirements)
- Engineering response schedule: OEM standard proposal turnaround (within 48 hours)
آخرین بررسی: 2026-10-29