خلاصه اجرایی A coil that is wrapped and strapped keeps its outer wraps tight, eliminates layer telescoping, and secures internal tail ends during downstream handling and transport. The stretch wrapping and radial strapping units operate as a modular two-station sequence rather than a rigid single-chassis machine. For an operational target of 20 coils per hour, available takt time is 3,600 / 20 = 180 s per coil. The governing station cycle—or the combined wrap-plus-strap cycle if executed on a single shared indexer—must remain comfortably within this takt window. Station layouts and conveyor links are engineered to fit facility footprints.
فهرست مندرجات
- کاری که دستگاه انجام میدهد
- The two stations
- پیچیدن کویل از طریق چشم
- پیچاندن سیم پیچ از طریق چشم
- خروجی، زمان چرخه خط و takt
- کنترلها و ایمنی
- چک لیست انتخاب برای ایستگاه بسته بندی و تسمه کشی کویل
- سوالات متداول مهندسی
- مرحله بعدی
- خواندن مرتبط
- منابع
کاری که دستگاه انجام میدهد
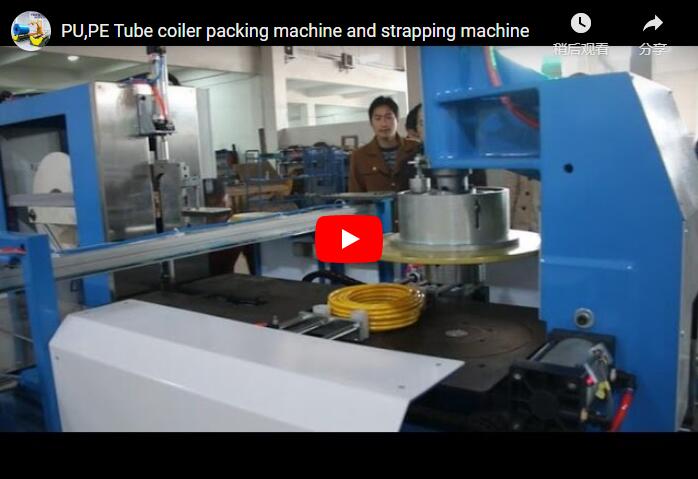
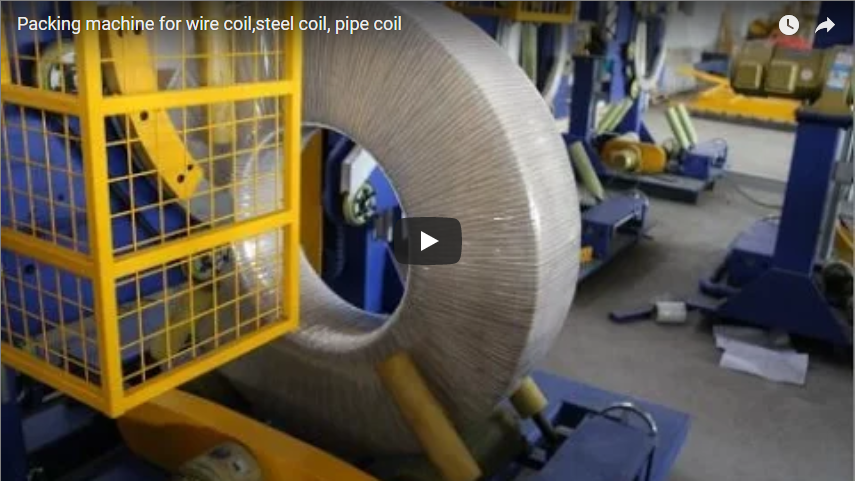
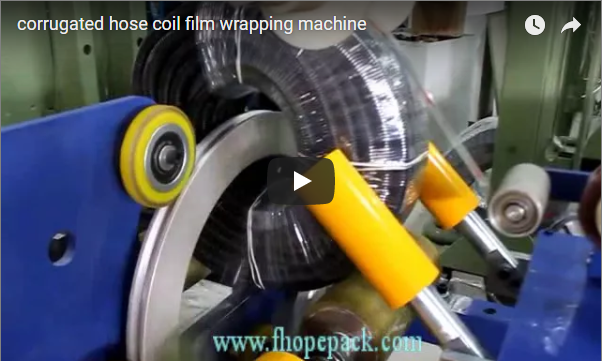
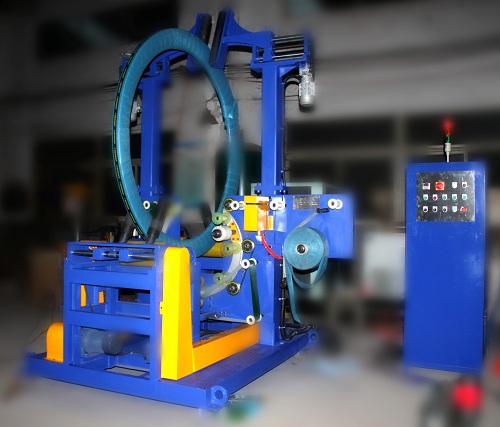
At the wrapping station, the coil rests horizontally on motorized support rollers. A precision rotating ring carries the film carriage directly through the coil eye (inner diameter), applying high-retention stretch film as the support rollers rotate the coil. This process applies continuous, overlapping containment across the coil outer diameter (OD), inner diameter (ID), and both side faces.
At the strapping station, an overhead gantry carrying a heavy-duty strapping head lowers over the coil on the conveyor. A segmented guide track traverses the coil eye, forming an automated loop that tensions, seals, and cuts high-strength PET strapping. An integrated scissor-lift table at the terminal end of the strapping line facilitates transfer and buffering.
The two stations
| ایستگاه | Kinematic & Operational Function |
|---|---|
| Station 1 – Wrap | High-speed orbital ring passes through the coil eye, applying protective stretch wrap around the full cross-section |
| Station 2 – Strap | Gantry-mounted head feeds PET strap through the coil eye, pulling tension and friction-welding the joint |
| جدول بالابر | Hydraulic scissor-lift station positioned at the line discharge for palletization or transfer car indexing |
Applying stretch film first seals the outer wraps, stabilizes loose strip ends, and provides continuous moisture and surface protection. Subsequent radial strapping clamps down over the film, absorbing dynamic shock loads during crane hoist movements, fork truck handling, and transit.
Whether these stations are linked by a continuous powered roller conveyor or configured as decoupled workstations depends on plant layout and buffer requirements. For fully automated slit coil processing lines featuring automated sorting, strapping, through-eye wrapping, and downending, consult our خط بسته بندی کویل شکاف دار برای مراکز خدماتی.
پیچیدن کویل از طریق چشم
An eye-through coil wrapper uses an open/close or C-type/annular rotating ring to orbit stretch film through the center bore, wrapping both faces, the OD, and the ID simultaneously. This configuration shares core drive kinematics with our specialized non-ferrous and copper strip coil packaging equipment. Wrapping speed, film overlap percentage, and pre-stretch rates are adjusted via the PLC interface.
Reference specifications for the standard FPC-200 eye-through wrapper:
| پارامتر | مقدار (مرجع) |
|---|---|
| بسته OD | 600-1,200 میلی متر |
| شناسه بسته | 300-800 میلی متر |
| وزن جسم | 5،500-XNUMX،XNUMX کیلوگرم |
| چرخش سرعت | 10-100 دور در دقیقه |
| سرعت غلتک | 2-4 متر در دقیقه |
| دامنه همپوشانی | 20٪ -90٪ |
| سرعت بسته بندی | ۲۳ تا ۳۵ ثانیه برای هر کویل |
For heavier strip bundles and higher mass capacities, the FPC-300 chassis provides reinforced structural support:
| لفاف بسته بندی | سیم پیچ OD | کویل ID | وزن کویل | سرعت زنگ |
|---|---|---|---|---|
| FPC-200 | 600-1,200 میلی متر | 300-800 میلی متر | 5،500-XNUMX،XNUMX کیلوگرم | 10-100 دور در دقیقه |
| FPC-300 | 700-1,200 میلی متر | 400-900 میلی متر | 10،1,000-XNUMX،XNUMX کیلوگرم | 5-100 دور در دقیقه |
Total wrap cycle time is governed by coil dimensions, selected film width (typically 90–150 mm), and programmed overlap ratio.
پیچاندن سیم پیچ از طریق چشم
Following the wrapping stage, high-tensile PET strapping secures the bundle integrity. Detailed information on this engineering class is available in our دستگاه تسمه شعاعی سیم پیچ فولادی بررسی اجمالی.
The custom-engineered eye-through strapping system applies radial straps through the center bore. As an engineering baseline, reference specifications for our industrial PET eye-through strapping platform include:
| پارامتر | مقدار (مرجع) |
|---|---|
| اندازه تسمه | OD 800–1,350 mm; ID 508–610 mm; width 20–500 mm |
| وزن کویل | 100،2,500-XNUMX،XNUMX کیلوگرم |
| مواد تسمه | PET, width 9–12 mm, thickness 0.4–1.0 mm |
| کشش تسمه | 100-1,000 نیوتن |
| سرعت تسمه | About 12–15 s per strap |
| میز چرخش | چرخش ۳۶۰ درجه برای ۴ تسمه تسمهای |
Actual tension limits, strap counts (e.g., 2, 3, or 4 radial ties), and rotation angles are programmed to match product specifications and shipping standards.
خروجی، زمان چرخه خط و takt
Takt time is dictated by plant production quotas rather than individual machine velocity. The engineering validation below demonstrates an operational target of 20 coils per hour:
| مورد | مقدار |
|---|---|
| هدف خروجی (توضیحی) | 20 کویل در ساعت |
| Takt, 3,600 / 20 | ۹۰ ثانیه در هر کویل |
| زمان بستهبندی، مرجع FPC-200 | 23–50 ثانیه |
| Strap time, 4 straps × 12–15 s | 48–60 ثانیه |
| وضعیت | Slower station (separate) or wrap + strap (combined, 71–110 s) below 180 s |
When wrapping and strapping operate on decoupled conveyor stations, line cycle time is governed strictly by the slower unit (the strapping station at 48–60 s), leaving substantial headroom within the 180 s takt allowance. If both operations are integrated into a single combination station, total process time equals the sum of both sequences (71–110 s), which still operates well inside the required 180 s threshold.
کنترلها و ایمنی
Orbital wrapper rings and gantry strapping heads exhibit high-inertia mechanical motion through open coil cavities. Personnel entry into the ring rotation zone, strapping head descent envelope, or indexing roller conveyors is strictly prohibited during automatic operation. Maintenance, film roll changes, or fault interventions must only occur once the equipment is fully stopped, verified zero-energy, and locked out under established LOTO protocols.
Safety architectures conform to the destination country’s machinery directives. For CE installations, risk assessments comply with ISO 12100, and integrated safeguarding (light curtains, perimeter interlocks, and emergency stop circuits) satisfies EN 415-10 standards for packaging machinery.
چک لیست انتخاب برای ایستگاه بسته بندی و تسمه کشی کویل
- Coil dimensional envelope: minimum and maximum OD, ID, face width, and total mass.
- Required continuous throughput capacity (coils per hour).
- Packaging material specifications: stretch film width, core diameter, film thickness, and target overlap percentage.
- Strapping parameters: strap grade (PET/PP), width, thickness, strap count per coil, and tension requirements.
- Material flow layout: single continuous powered conveyor vs. dual decoupled stations, including discharge elevation changes.
- Plant infrastructure: floor loading limits, pneumatic supply parameters (flow/pressure), and electrical service specifications.
سوالات متداول مهندسی
Q: Why wrap the coil through the eye before strapping it? A: Eye-through wrapping establishes complete environmental containment across the OD, ID, and both side faces while support rollers slowly rotate the coil. This prevents strip edge damage and telescoping, allowing subsequent PET straps to securely bind over the film without scoring metal edges.
Q: Why are the two stations shown as a sequence? A: Presenting the machines as decoupled modules highlights their standalone mechanical functions. It does not dictate a fixed conveyor link; transfer decks, turnstiles, or indexing chains can be engineered to suit specific facility layouts.
Q: How fast is the strapping? A: On our PET eye-through strapping head, strap feeding, tensioning, sealing, and cutting takes approximately 12–15 s per strap. A standard four-strap radial pattern completes in 48–60 s, excluding coil indexing rotation.
Q: Can the wrap and strap share a takt? A: Yes. On separate stations, the governing cycle time is simply that of the slower machine. On a single shared station, cumulative cycle time equals the wrap sequence (23–50 s) plus the strap sequence (48–60 s), yielding 71–110 s total, which easily satisfies a 180 s takt (20 coils/hour).
Q: Which wrapper fits my coil? A: Bundles within 600–1,200 mm OD, 300–800 mm ID, and weights up to 500 kg are handled by the FPC-200. For heavier industrial bundles up to 1,000 kg with IDs of 400–900 mm, the heavy-duty FPC-300 chassis is recommended.
مرحله بعدی
- Submit layout drawings alongside maximum coil dimensions, target strap configurations, and required hourly volume to info@fhopepack.com.
- Receive an engineering evaluation within 48 hours, including equipment footprints, takt time modeling, and film consumption estimates.
- Schedule an engineering review to verify roller conveyor working heights, utility connections, and footprint integration.
خواندن مرتبط
- بسته بندی کویل مسی FPC-200
- دستگاه تسمه کشی PET کویل فولادی
- ویدئو: دستگاه بسته بندی کویل برای نوار مس و فولاد آلیاژی
- ویدئو: خط بستهبندی کویل نوار مسی اتوماتیک با برچسبگذاری، بستهبندی و انباشت
- ویدئو: دستگاه بسته بندی کویل فولادی و کویل مسی برای بسته بندی فیلم از طریق چشم
- ویدئو: دستگاه تسمهکشی کویل فولادی اتوماتیک
منابع
- پارامترهای بستهبندی: بسته بندی کویل مسی FPC-200, بسته بندی کویل مسی FPC-300
- پارامترهای تسمه: دستگاه تسمه کشی PET کویل فولادی
- Takt example: Worked engineering example, standard line values
- دستگاه در حال کار: ویدیوی ما در یوتیوب
- استانداردهای صنعتی: ISO 12100:2010 ایمنی ماشین آلات, EN 415-10:2014 ایمنی ماشین آلات بسته بندی
آخرین بررسی: 2026-10-29