خلاصه اجرایی An automated coil packaging line takes a bare coil from the slitter or mill and discharges it wrapped, strapped and ready to ship, with no manual handling in between. Our line is engineered station by station: an eye-through wrapper covers the coil, transfer and turning stations move it, and a strapping station adds the bands — all automatic, from a 3D plant layout. Strap per coil follows from the اندازه سیم پیچ و طرح باندهر دو برای هر پروژه تنظیم میشوند.
فهرست مندرجات
- کاری که دستگاه انجام میدهد
- ایستگاههای موجود در خط بستهبندی کویل خودکار
- مصرف تسمه به ازای هر کلاف
- برنامه ریزی طرح بندی
- کنترلها و ایمنی
- چک لیست انتخاب برای خط بسته بندی کویل خودکار
- سوالات متداول مهندسی
- مرحله بعدی
- خواندن مرتبط
- منابع
کاری که دستگاه انجام میدهد
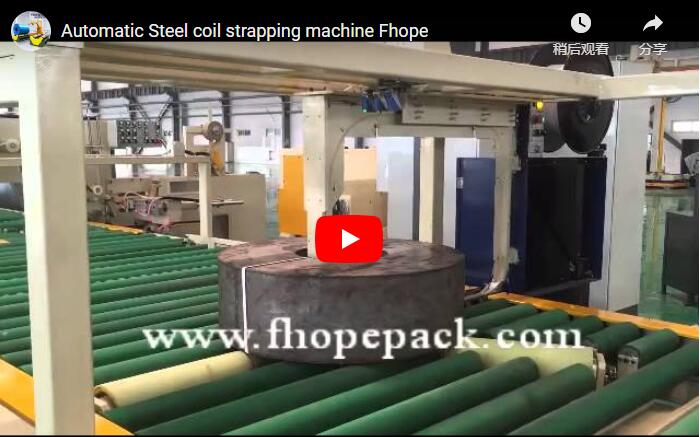
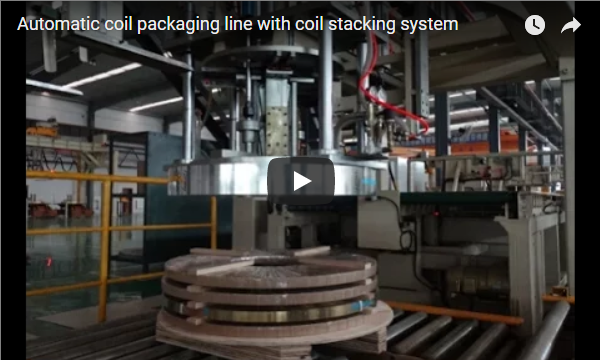
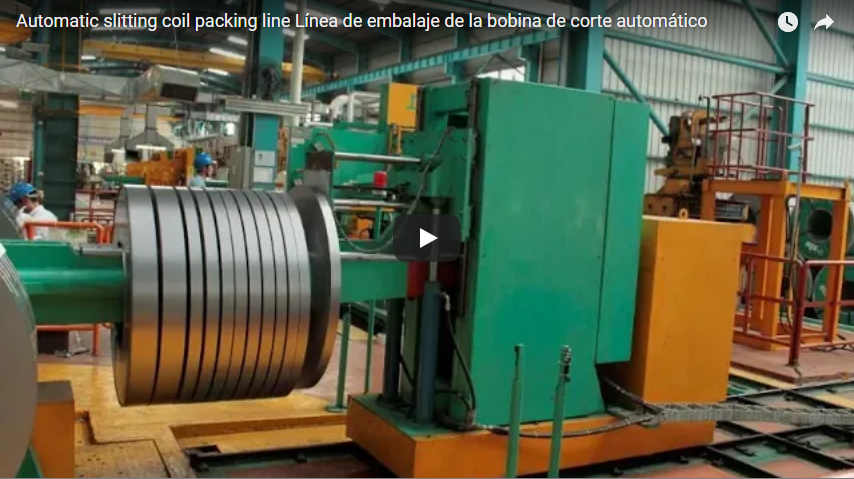
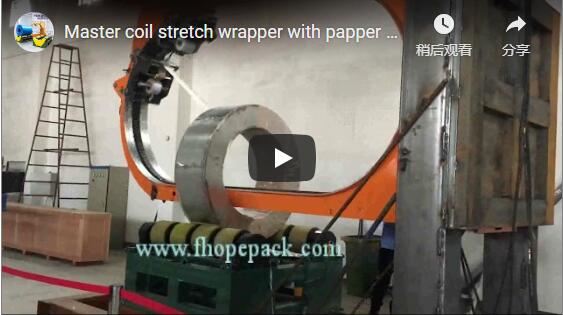
The line is engineered as a continuous, synchronized sequence of stations. A loading station receives the bare coil directly from the slitting line recoiler, crane C-hook, or coil car. An eye-through wrapper covers the metal coil through its center eye and over its cylindrical wall, after which motorized transfer, lifter, or turning stations carry it between active process zones. A dedicated strapping station applies precision radial and circumferential bands, and an automated discharge station transfers the fully wrapped and strapped bundle to downstream downending, stacking, or palletized dispatch.
Every transfer sequence is interlocked and automated. The coil is never manually lifted, pushed, or turned between initial entry and dispatch, eliminating mechanical edge damage and workplace strain. Because every module operates synchronously, the entire line throughput runs at the pace of its slowest station.
Depending on line configuration, the packaging stations handle coil weights from 100 kg to 2,500 kg in standard horizontal formats, or 150 kg up to 6,500 kg on vertical packaging systems (with heavy-duty configurations accommodating 4,000 kg to 11,000 kg) [manufacturer rating]. The eye-through wrapping station supports slitted coils with widths of 20–500 mm, outside diameters of Ø800–1,400 mm, and eye inside diameters of Ø508–610 mm [manufacturer rating]. Conveyor roller speed is maintained at 12 m/min, while the rotating ring delivers 8–80 r/min variable speed, completing an eye-through wrap in 40–70 sec/pcs [manufacturer rating]. For integrated mill systems utilizing automated turnstiles, walking beams, and coil cars, throughput achieves up to 60 coils per hour [manufacturer rating].
ایستگاههای موجود در خط بستهبندی کویل خودکار
| ایستگاه | چقدر می شود؟ |
|---|---|
| بار | کویل لخت را از جرثقیل یا ماشین کویل گیر می گیرد |
| بستهبندی از طریق چشم | سیم پیچ را از طریق چشم و روی دیوار می پوشاند |
| جابجایی و چرخش | سیمپیچ را بین ایستگاهها حرکت میدهد یا میچرخاند |
| تسمه زنی | نوارهای شعاعی و محیطی را اضافه میکند |
| تخلیه | کویل را برای انباشت یا ارسال تحویل میدهد |
هر ایستگاه به طور خودکار کویل را به ایستگاه بعدی منتقل میکند، بنابراین خط با سرعت کندترین ایستگاه خود حرکت میکند.
In our standard integration, the mechanical core comprises a mechanical upender/tilter, an indexing coil transport station, and an orbital wrapping system driven by SEW Eurodrive gearmotors. The wrapping station accommodates multiple packaging media, including PE-coated crepe paper, stretch film, or woven PP tape (with roll specifications of ID 50 mm, OD 200–500 mm, and width 100 mm) to defend coil surfaces against corrosion, condensation, and friction scuffs during transit.
مصرف تسمه به ازای هر کلاف
Strap requirement is calculated directly from coil geometry and the specified binding pattern. Below is an illustrative worked example for a 1,500 mm OD, 508 mm ID, 1,200 mm wide coil configured with 4 radial bands and 2 circumferential bands:
| مورد | مقدار |
|---|---|
| دیوار، (۱۸۰۰ − ۶۱۰) ÷ ۲ | ۶۰ میلیمتر |
| نوار شعاعی، ۲ × (۱۲۰۰ + ۴۹۶) | ۶۰ میلیمتر |
| نوارهای شعاعی، ۴ × ۳.۳۹ متر | در مورد 13.6 m |
| نوار محیطی، π × 1,500 | در مورد 4,712 میلی متر |
| نوارهای محیطی، ۲ × ۴.۷۱ متر | در مورد 9.4 m |
| تسمه در هر کویل، قبل از همپوشانی مهر و موم | در مورد 23 m |
Add the seal overlap to each band when you order strap; the exact joint allowance depends on the strapping head and the strap type, and is confirmed with the strap plan.
برنامه ریزی طرح بندی
| سوال | چرا از آن مهم |
|---|---|
| نحوه رسیدن کویلها | ایستگاه بارگیری را تنظیم میکند: جرثقیل، واگن کویل یا نوار نقاله |
| مواد بسته بندی | کاغذ، فیلم یا هر دو روی بستهبندی |
| تعداد باند در هر کویل | تعداد سرهای تسمهکشی را تنظیم میکند |
| چشم در هنگام اعزام عمودی یا افقی است | تصمیم میگیرد که آیا خط به ایستگاه تبدیل نیاز دارد یا خیر |
| خروجی در ساعت | کندترین ایستگاه و بافر بین ایستگاهها را تنظیم میکند |
For the radial strapping station, our modular strapping system can be configured to apply 2, 3, 4, or 6 radial belts per cycle [manufacturer rating]. The strapping mechanism incorporates a 360° rotating strapping head and arch system that indexes cleanly around the coil eye in both semi-automatic and fully automatic operating modes, with a heavy-duty strapping head engineered for a service life of up to 1,000,000 strapping cycles [manufacturer rating].
برای ایستگاه تسمهکشی به تنهایی، به دستگاه تسمهکشی کویل فولادی خودکار ما مراجعه کنید . برای خطوطی که کویلهای سنگین را میچرخانند و روی هم قرار میدهند، به راهنمای خریدار ما برای بستهبندی کششی و چیدمان رو به پایین مراجعه کنید.
We draw the layout in 3D first, so the plant can check space and flow before building.
کنترلها و ایمنی
کویلها به طور خودکار بین ایستگاهها حرکت میکنند و پوششها و سرهای تسمهکشی درون خط محافظ قرار میگیرند. در حین کار، افراد را از خط محافظ دور نگه دارید و فقط در حالتی که ایستگاه متوقف و ایزوله شده است، وارد شوید.
Main control architecture centers on an industrial Siemens S7-1200 PLC linked to a multi-language touchscreen HMI. Main electrical power runs at 380 VAC (±5%), 50 Hz, 3-phase 4-wire, with 220 VAC single-phase / 24 VDC control circuitry, supported by clean plant air supply at 5–8 kgf/m² [manufacturer rating].
The standards that apply depend on the destination market. For CE markets under Machinery Directive 2006/42/EC, ISO 12100 sets the basic risk-assessment methodology and EN 415-10 sets specific safety requirements for automated packaging machines. Guarded enclosures are protected by safety light curtains, perimeter fencing, door interlocks, and emergency stop pushbuttons at the operator stations [manufacturer rating].
چک لیست انتخاب برای خط بسته بندی کویل خودکار
- محدوده قطر خارجی، قطر داخلی، عرض و وزن کویل.
- کویل در ساعت.
- جنس بستهبندی: کاغذ، فیلم یا هر دو.
- نوارهای شعاعی و محیطی در هر سیمپیچ.
- موقعیت چشم در هنگام اعزام.
- فضای ساختمان، دسترسی به جرثقیل و بارگذاری کف.
سوالات متداول مهندسی
س: یک خط بستهبندی کلاف خودکار چه ایستگاههایی دارد؟ ج: بارگیری، بستهبندی از طریق چشم، جابجایی یا چرخاندن، تسمهکشی و تخلیه.
Q: How much strap does a coil take? A: About 23 m for 4 radial and 2 circumferential bands on a 1,500 mm OD, 508 mm ID, 1,200 mm wide coil in our illustrative example, before adding joint and seal overlap allowances.
Q: What sets the line speed? A: The slowest station; buffers and indexing conveyor sections between stations keep the rest of the line moving smoothly without bottleneck starvation.
Q: What wrap materials can the line run? A: Paper, stretch film, or woven PP tape on the wrapper, configured individually or in combination to suit project requirements.
Q: How does coil delivery affect the line? A: Whether coils arrive by overhead crane C-hook, automated coil car, or roller conveyor determines the mechanical structure of the loading station.
Q: Why start with a 3D layout? A: So the plant engineering team can check foundation boundaries, crane clearances, and logistics flow before any steel is cut or installed.
Q: Do I need a turning station? A: Only if coils must leave eye vertical when they are wrapped eye horizontal, or the other way round. Upenders and downenders bridge the orientation gap between slitters and warehouse stacking.
Q: How many radial bands can the strapping station apply automatically? A: The radial strapping head system can be programmed to index and apply 2, 3, 4, or 6 strapping bands automatically per coil.
مرحله بعدی
ما خط بستهبندی کویل شما را در سه مرحله برنامهریزی میکنیم:
- طرح چیدمان خود را ارسال کنید با اندازه کویل، خروجی و طرح ساختمان به info@fhopepack.com.
- دریافت پیشنهاد ظرف ۴۸ ساعت، به همراه طرح ایستگاه و نقشه تسمه.
- رزرو نظرسنجی در سایت برای بررسی فضای ساختمان و دسترسی به جرثقیل.
خواندن مرتبط
- خط بسته بندی کویل اتوماتیک
- دستگاه های تسمه کویل فولادی
- ویدئو: دستگاه بسته بندی کویل فولادی، کویل مسی برای بسته بندی فیلم از طریق چشم
منابع
- محتوای دستگاه: تیم مهندسی FHOPE، 2026-10-04
- مثال تسمه: مثال عملی ما، مقادیر گویا
- دستگاه در حال کار: ویدیوی ما در یوتیوب
- دامنه استانداردها: ISO 12100: 2010, EN 415-10: 2014
- Equipment engineering specification: FPCA-1200 Horizontal Steel Coil Packing Machine
- Strapping unit technical data: دستگاه تسمه کویل فولادی رادیال
- Line system integration: خط بسته بندی کویل عمودی
آخرین بررسی: 2026-10-28