Kokkuvõte Coil upending and turning moves a steel coil between eye-horizontal and eye-vertical, for storage, packing or the next process. Our mechanical coil upender does it with a gear motor and worm reducer, and the crane only sets the coil on and lifts it off. The FPCT-03 to FPCT-20 take 3 to 20 tons, in 50–100 seconds per turn. A worked example picks the model for a 14.5-ton coil and checks the turns per hour.
Sisukord
- Why coils need turning
- Crane loading onto the upender
- The mechanical drive
- The machine shown
- Mechanical coil upender data
- Worked example: a 14.5-ton coil
- Valiku kontroll-leht: mida meile saata
- Ohutus ja EN 415-10
- Inseneri KKK
- Järgmine samm
- Seotud lugemine
- Allikad
Why coils need turning
Steel and aluminium coils leave the mill with the eye horizontal, which suits roller conveyors and coil cars. Many plants store, pack and ship them eye-vertical, standing on a pallet, because a coil on its face cannot roll and stacks more safely. At the next process, the coil often has to go back to eye-horizontal.
Turning a multi-ton coil on a crane hook alone is a swinging, uncontrolled load. An upender turns it on a fixed path, close to the floor.
Crane loading onto the upender
With crane loading, the crane brings the coil on a C-hook or tongs and sets it in the upender’s V-shaped seat. The crane releases, the operator turns the upender through 90°, and the crane picks the coil off the second face. The crane only lifts; the upender does the turn.
This is the simplest layout: no conveyor or coil car is needed. It suits plants where coils move by crane anyway, and where upending is one step between crane moves.
The mechanical drive
Our mechanical upender is driven by a gear motor through helical gears and a high-quality worm reducer. A heavy-duty four-roll device supports the turning body as it tilts. The turning body is engineered with heavy structural stiffeners and stress-relieved steel plates to withstand dynamic shock loads.
The worm drive holds the load, so the machine can stop at any angle and stays put even when the power is off. An inverter sets the speed, and two displacement limiters with limit sensors end the turn. There is no hydraulic oil to leak or heat.
The machine shown
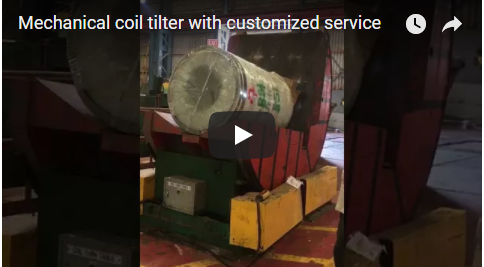
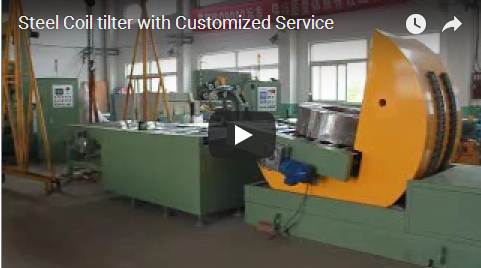
Our orange and green mechanical coil upender, marked FZ25T, turns a large steel coil from eye-horizontal to eye-vertical and back. The coil sits in the orange L-shaped seat on a green base. An operator in a blue work suit and hard hat runs it from a separate control box beside the machine, well clear of the turning seat.
Mechanical coil upender data
| Kirje | FPCT-03 | FPCT-05 | FPCT-10 | FPCT-20 |
|---|---|---|---|---|
| Maksimaalne koormus | 3 t | 5 t | 10 t | 20 t |
| võim | 1.3 kW | 2.0 kW | 4.5 kW | 7.8 kW |
| Pööramisaeg | 50–90 s | 50–90 s | 60–90 s | 60–100 s |
| Varustama | AC 380 V / 50 Hz or to your supply |
Across the range a turn takes 50–100 seconds. Control is by control box or remote control, with the inverter for speed. We make the seat for each product, so the table size follows your coil. Above 20 tons, as with the unit shown, we design the drive to the load.
Worked example: a 14.5-ton coil
A plant upends steel coils of 1,500 mm OD, 610 mm ID and 1,250 mm width, moved by crane. These are illustrative customer figures.
Rulli kaal. Volume = π ÷ 4 × (1.5² − 0.61²) × 1.25 = 1.84 m³. At 7,850 kg/m³ the coil weighs about 14.5 t.
Mudel. That is over the FPCT-10’s 10 tons and inside the FPCT-20’s 20 tons, so the FPCT-20 is the right choice.
Turns per hour. One upending takes t_turn + t_in + t_out, where t_in and t_out are your crane times to set the coil on and lift it off. With the FPCT-20’s 60–100 s turn and 2 minutes of crane time each way, one cycle is 300–340 s. That gives 3,600 ÷ 340 = 10.6 to 3,600 ÷ 300 = 12 coils per hour.
General rule. With crane loading, the crane time usually decides the rate. If you need more coils per hour, a conveyor or coil car at the upender saves the crane moves.
Valiku kontroll-leht: mida meile saata
- Raskeim mähise kaal.
- Coil OD, ID and width range.
- Turn direction: eye-horizontal to eye-vertical, or both.
- Loading: crane, conveyor or coil car.
- Mähised tunnis.
- Supply voltage and control preference.
Ohutus ja EN 415-10
For CE markets we use EN 415-10 as our reference, with a risk assessment to ISO 12100. The main hazards are the turning seat with the coil, the crane load during loading, and crush points between seat and base.
The emergency stop immediately halts drive power, while the self-locking worm gearbox mechanically arrests rotation and secures the cradle in position. The control box keeps the operator away from the turning position. Turn only with the crane hook clear of the coil.
Inseneri KKK
Q: Mechanical or hydraulic upender? A: Our mechanical upender uses a gear motor and worm reducer, holds at any angle without power and needs no hydraulic oil. We also build hydraulic upenders for other layouts.
Q: Can it stop part-way? A: Yes. It can stop at any angle, even with the power off.
Q: Do we need a conveyor? A: Not with crane loading. Add a conveyor or coil car if the crane becomes the bottleneck.
Q: Which standards do you build to? A: For CE we work to EN 415-10, and each machine has an ISO 12100 risk assessment.
Järgmine samm
- Email your coil sizes, heaviest weight and loading method et info@fhopepack.com.
- Vastame 24 tunni jooksul koos ettepanekuga, with the model and seat design.
- Saadame paigutusjoonise with crane access.
Seotud lugemine
- Mechanical coil upender and tilter
- Hüdrauliline mähise ülestõstja
- How does a coil upender work?
- Pooli kallutus ja mähise ülestõstmine
- The 90 degree coil upender with rotary base
Allikad
- Specifications: FHOPE mechanical coil upender and tilter product page (FPCT-03 to FPCT-20)
- Masina video: steel coil tilter with lifting coil loading on YouTube
- Coil weight and turns per hour: our worked example, illustrative coil figures
- Standardid: EN 415-10 (pakkimismasinad, üldine ohutus); ISO 12100:2010
Viimati üle vaadatud: 2026-10-17