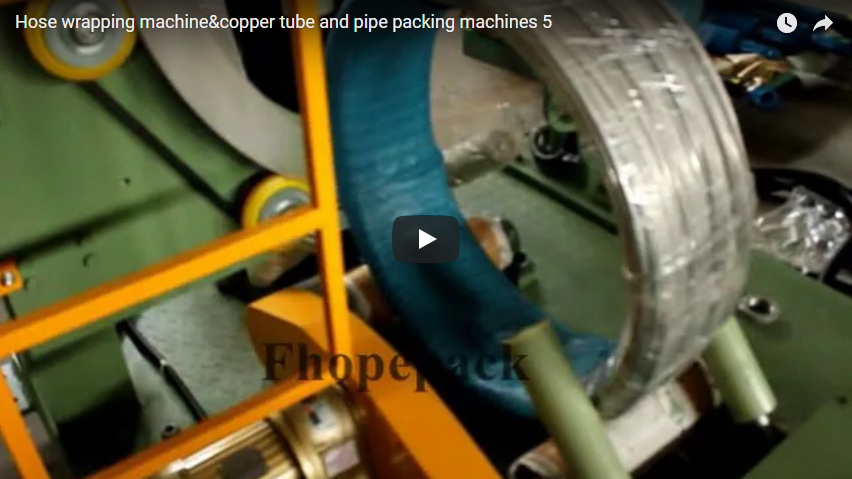
Resumen ejecutivo This automatic wire coil strapping and packing line integrates five inline operations into a continuous packaging sequence for loose or semi-compacted wire coils. Operating on coils loaded eye-to-the-sky on carriers or baskets, the system executes vertical hydraulic compacting, radial strapping through the eye under sustained pressure, peripheral stretch wrapping on an automated turntable, 90° upending, and orbital through-the-eye wrapping. Controlled via a central PLC and HMI terminal, roller conveyors index coils sequentially through each processing station to ensure structural stability, tension retention, and complete moisture protection during transport.
Índice
- Qué hace la máquina
- Estaciones en la línea
- Bobinas por hora
- Lo que configuramos por bobina
- Lista de verificación de selección
- Seguridad
- Preguntas frecuentes sobre ingeniería
- El próximo paso
- Lectura relacionada
- Fuentes
Qué hace la máquina
| Paso | Función |
|---|---|
| Compactación | A heavy-duty vertical hydraulic press clamps the loose coil stack down, eliminating internal voids and establishing target package height. |
| Fornido | Automatic strapping heads feed, tension, seal, and cut high-tensile straps through the coil eye while maintained under hydraulic compression. |
| Envoltura | An automated turntable wrapper applies protective stretch film or paper around the outer cylindrical circumference of the strapped coil. |
| Inclinación | A heavy-duty hydraulic upender tilts the strapped coil 90°, transitioning it safely from vertical eye-to-the-sky to horizontal eye orientation. |
| envoltura de ojo | An orbital wrapping ring passes packaging material directly through the inner eye, completing the protective wrap. |
Estaciones en la línea
| Estación | Trabajos |
|---|---|
| Prensa vertical | Delivers compressive force via guided hydraulic cylinders to compact coil layers and stabilize geometry prior to binding. |
| Envoltura de plato giratorio | Rotates the coil on a heavy-duty platform to apply adjustable-tension protective film to the exterior side walls. |
| Hacia arriba | Executes smooth 90° load reorientation to transfer the coil from the strapping position to the eye-wrapping position. |
| envoltura de ojos | Drives an orbital shuttle ring through the center opening to apply protective wrap along the inner eye surface. |
| Transportador de rodillos | Links all processing modules, indexing coils sequentially without manual intervention. |
Bobinas por hora
Ejemplo resuelto (ilustrativo).
| Parámetro | Valor |
|---|---|
| Ciclo de estación más lento (ilustrativo) | 90 s |
| Bobinas por hora, 3,600 ÷ 90 | 40 |
| Correas por bobina (ilustrativo) | 4 |
| Correas por hora, 40 × 4 | 160 |
Note: The cycle rate above is an illustrative worked example based on balanced conveyor indexing. Actual throughput depends on incoming coil dimensions, required compression dwell time, and chosen wrap overlapping percentages.
Lo que configuramos por bobina
| Configuración | Depende de |
|---|---|
| Golpe de prensa | Pre-compacted coil height, target final height, and wire spring-back properties |
| Número de correas | Outer diameter, total package weight, and structural shipping security guidelines |
| Programa de envoltura | Storage conditions, surface rust susceptibility, and target film layer overlap |
| Velocidad de inclinación | Payload mass, load center of gravity, and coil basket stability during tilting |
Lista de verificación de selección
- Coil outer diameter (OD) and inner diameter (ID).
- Coil stack height (pre-compression and target post-compression) and maximum unit weight.
- Required processing rate (coils per hour under peak operating shifts).
- Number of straps per coil (set per your packing specification).
- Protective packaging specification (OD wrap only, through-the-eye wrapping, or dual-layer composite wrap).
- Line layout constraints (inline straight configuration, 90° transfer layout, and available plant footprint).
Seguridad
- Maintain established exclusion zones and keep personnel clear of hydraulically actuated press platens and rotating rings.
- Perimeter interlocked mesh fencing must remain closed and monitored by safety gate interlocks during automatic cycling.
- Enforce strict Lockout/Tagout (LOTO) protocols before entering the machine envelope for maintenance, clearing strap chute jams, or changing film rolls.
- For CE-regulated markets, line architecture conforms to the safety integration principles of ISO 12100:2010 and the packaging machinery standards of EN 415-10:2014.
Preguntas frecuentes sobre ingeniería
Q: What does the line do? A: It forms an integrated finishing line that accepts loose wire coils, compresses them under hydraulic force, applies perimeter strapping, wraps outer surfaces, reorients the coil 90° via an upender, and applies an orbital through-the-eye film layer for comprehensive environmental protection.
Q: Why compact the coil? A: Compacting forces out loose air gaps between wire convolutions while restraining internal material spring-back. For a comparable FHOPE wire coil compressing and strapping line class handling galvanized wire (wire diameter 2.50–8.0 mm, coil OD 800–1,300 mm, weight up to 2,000 kg), a vertical hydraulic compaction force of 2–3 t typically reduces coil height from 1,200 mm down to 800 mm prior to strap application, preventing strap loosening during transport.
Q: How many coils per hour? A: As demonstrated in our illustrative worked example with a 90 s critical-path station, the calculated theoretical line speed is 40 coils per hour. Plant-specific cycle times vary based on conveyor index distances, strap count, and film rotation speeds.
Q: Why tilt the coil? A: The hydraulic upender rotates the coil 90° to reposition its axis from a vertical orientation (eye-to-the-sky) to a horizontal position, presenting the center eye at the optimal elevation for horizontal orbital wrapping rings.
Q: Can stations be left out? A: Yes. The line architecture is modular: the outer turntable wrapper, through-the-eye wrapper, or upender station can be selected per packing spec, either or both.
Q: Which standards apply? A: Machine design and functional safety follow ISO 12100:2010 for general risk reduction, and comply with EN 415-10:2014 specific to end-of-line packaging and strapping machines in CE-compliant configurations.
El próximo paso
We configure each automated wire coil packaging line to your facility’s exact material parameters in three steps:
- Envíe su plano de distribución along with coil dimensional ranges (OD, ID, height), wire gauge, and throughput requirements to info@fhopepack.com.
- Reciba una propuesta en 48 horas. complete with preliminary engineering layout drawings, technical data sheets, and station cycle time calculations.
- Solicitar una visita al sitio with our engineering team to review line footprints, conveyor loading heights, and electrical interface requirements.
Lectura relacionada
- Máquina automática de rebobinado y atado de bobinas de alambre
- Máquina para envolver y embalar bobinas de alambre de acero
- Máquina flejadora automática de bobinas de acero
- Máquina de embalaje de bobinas
Fuentes
- Contenido de la máquina: Equipo de ingeniería de FHOPE, 4 de octubre de 2026
- Vídeo de la línea: el vídeo en YouTube
- Bobinas por hora: nuestro ejemplo práctico, valores ilustrativos
- Ámbito de aplicación de la norma: ISO 12100:2010; EN 415-10: 2014
- Plazos de presentación de propuestas: solicitud de aprobación de la CTA (propuesta en un plazo de 48 horas)
Última revisión: 29/10/2026