Tóm tắt We pack slit steel coils on an integrated line that wraps each coil through the eye, turns it eye-to-sky, straps it and stacks it on a pallet. The wrap can be stretch film, paper, VCI paper or film, or woven fabric, chosen for how long the coil is stored and how far it travels. Narrow-coil lines pack 20–40 coils an hour. A worked example checks coil weight, strap count against the slitter’s pace, and coils per pallet.
Mục lục
- Where slit coil packing slows a line
- Stations from slitter exit to pallet
- Choosing the strap and wrap combination
- Slit coil line specifications
- Worked example: strap count, pace and pallet load
- Stacking limits and timber separators
- Danh sách kiểm tra lựa chọn: những gì cần gửi cho chúng tôi
- An toàn và tiêu chuẩn EN 415-10
- Câu hỏi thường gặp về kỹ thuật
- Bước tiếp theo
- Đọc liên quan
- nguồn
Where slit coil packing slows a line
A slitter turns one master coil into a set of narrow coils in minutes. Packing them by hand means turning each coil, strapping it, wrapping it and stacking it with a crane. That work quickly falls behind the slitter.
The plant here shows the automated route. Slit coils come off the exit side, coil cars run on floor rails between green machine stations, and orange railings fence off the working area. Packed coils stand in rows waiting to ship.
Stations from slitter exit to pallet
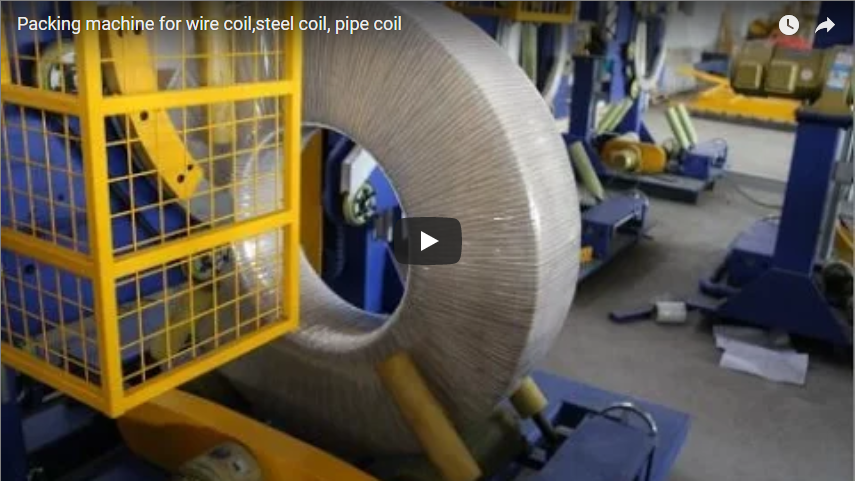
On the line here, the coils are wrapped while they still stand eye-to-wall. The slit coils sit on a mandrel arm and a coil car, and a green orbital wrapper passes film through the eye. Only then does the line turn them eye-to-sky for stacking.
The stations below cover both layouts. Where the wrap goes depends on whether you wrap eye-to-wall, as here, or after down-ending.
- Turnstile and coil car. Slit coils come off the slitter onto the turnstile arm, and a coil car on floor rails carries them between stations.
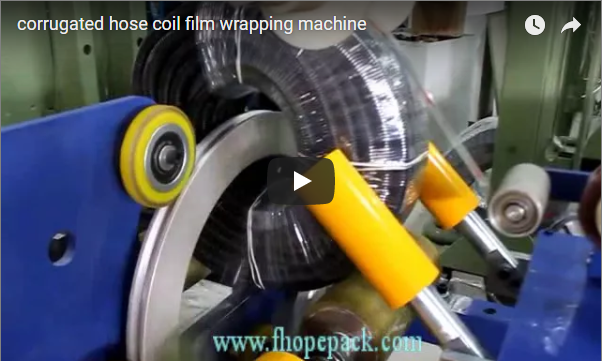
- Orbital wrapping, eye-to-wall. A ring passes paper or film through the eye, with the overlap set by the PLC.
- Down-ender. A hydraulic down-ender turns each coil from eye-to-side to eye-to-sky, in a 60 s cycle.
- Centering and strapping. Sensors and a lifting table centre the coil. A rotating platform then turns it while PET or steel straps go through the eye, at 3, 4 or 6 points.
- Weighing and labelling. The line records net and gross weight and applies a barcode label.
- Xếp chồng. A gantry or a magnetic or vacuum stacker places packed coils on a wooden pallet, and powered rollers carry the pallet out.
Eye-to-wall or eye-to-sky wrap. Wrapping on the mandrel suits a set of coils that leave the slitter together, because the film goes on before anyone handles a bare coil. Wrapping after down-ending puts the wrapper on the conveyor, which suits mixed widths and coils that are strapped first.
For a down-ender, weighing and strapping station, wrapper and outfeed conveyor in a row, we have quoted lengths of 2.5 m, 2 m, 2 m and 2 m. That is about 8.5 m long and 3.0 m wide, before the stacker.
Choosing the strap and wrap combination
The strap holds the coil together. The wrap protects the surface. Choose each one separately.
| Cần | Strap | Quấn |
|---|---|---|
| Short trip, indoor storage | PP hoặc PET | phim kéo dài |
| Dust and handling marks | PET | màng co hoặc giấy |
| Long storage or sea freight | PET hoặc thép | Giấy VCI hoặc màng VCI |
| Heavy coils, rough handling | Thép | woven fabric or composite fabric |
Stretch film and paper suit the standard configuration. VCI film and composite fabrics sit in the advanced configuration, with high-tension PET strapping. Steel strapping suits heavy coils, where a strap that stretches would let the coil loosen.
Slit coil line specifications
| Mục | Narrow coils | Cuộn dây rộng |
|---|---|---|
| trọng lượng thép cuộn | 30–4,000 kg | lên đến 25,000 kg |
| Chiều rộng khe | 8 tầm 500 mm | 450 tầm 1,900 mm |
| Tốc độ đóng gói | 20–40 coils/h | 5–8 coils/h |
| Coil OD | 500–1,500 mm, có thể kéo dài đến 2,100 mm | tương tự |
| Coil ID | 300, 508 hoặc 610 mm | tương tự |
| Chu kỳ đóng đai | 15–38 giây cho mỗi dây đeo | tương tự |
| Kiểm soát | Siemens S7-1200 or S7-1500F PLC | tương tự |
For the stacking section, the stack is up to 1,000 mm high including the pallet. The total load is up to 6,000 kg, with up to 3,000 kg per coil. Conveyors use 100 mm rollers with PU covering, on 380 V, 50 Hz.
Worked example: strap count, pace and pallet load
A service centre slits a master coil into eight strips, each 150 mm wide, with 1,200 mm OD and 508 mm ID. A new master coil comes off the slitter every 20 minutes. These are illustrative customer figures.
Trọng lượng cuộn dây. Each slit coil is π ÷ 4 × (1.2² − 0.508²) × 0.15 = 0.139 m³ of steel. At 7,850 kg/m³ it weighs about 1,090 kg.
Pace needed. Eight coils every 20 minutes is 8 × 3 = 24 coils an hour, inside the 20–40 coils/h narrow range. The 60 s down-ender handles 3,600 ÷ 60 = 60 coils an hour, so it is not the limit.
Strap count. If strapping is the slowest station, its time per coil is straps × strap cycle. At the slow end of 38 s, four straps take 152 s, or 3,600 ÷ 152 = 23.7 coils an hour. That is just short of 24. Three straps take 114 s, or 31.6 coils an hour, which keeps up. At the fast end of 15 s, even six straps take only 90 s.
So check the strap cycle on your strap type before fixing four straps. Three straps at the slow end still clear the slitter.
Stacking limits and timber separators
Coils per pallet. Five coils stack to 5 × 150 = 750 mm. With a 150 mm pallet, that is 900 mm, under the 1,000 mm limit. They weigh 5 × 1,090 = 5,450 kg, under 6,000 kg. A sixth coil would break both limits, so each master coil makes one pallet of five and one of three.
Timber separators can go between layers to stop the coils shifting in transit. On our gantry stacker, four support arms and internal coil protectors keep the coil edges from being damaged.
Danh sách kiểm tra lựa chọn: những gì cần gửi cho chúng tôi
- Coil OD, ID and slit width range.
- Heaviest and lightest coil.
- Coils per master coil and the slitter’s pace.
- Strap type and number of straps.
- Wrap media: film, paper, VCI or woven fabric.
- Pallet size, stack height and weight limit.
An toàn và tiêu chuẩn EN 415-10
We build our coil packing lines to CE requirements, with EN 415-10 as the reference and an ISO 12100 risk assessment. The main hazards are the turning down-ender, the strapping and wrapping heads, coil cars on rails and the stacker’s lifting zone.
Fence the line, as the railings here do, and keep people out of the stacker and rail areas while they move. One technician runs the section from the central PLC and HMI.
Câu hỏi thường gặp về kỹ thuật
Q: Can one line handle both film and VCI paper? A: Yes. The orbital wrapper takes paper or film, and the media is changed for the order.
Q: Do we need steel straps for heavy coils? A: Steel or high-tension PET straps both suit heavy coils. We choose by coil weight and how the coil is handled.
Q: Can the line weigh and label each coil? A: Yes. Weighing and barcode labelling are part of the line, with ERP tracking in the advanced configuration.
Hỏi: Những tiêu chuẩn an toàn nào được áp dụng? Trả lời: Đối với thị trường CE, chúng tôi tuân thủ tiêu chuẩn EN 415-10, kèm theo đánh giá rủi ro theo tiêu chuẩn ISO 12100.
Bước tiếp theo
- Email your coil sizes, slitter pace and packing materials đến info@fhopepack.com.
- Chúng tôi sẽ trả lời trong vòng 24 giờ với một đề xuất., with the stations and strap layout.
- Chúng tôi gửi bản vẽ bố trí for your slitter exit and shipping area.
Đọc liên quan
- Dây chuyền đóng gói và xử lý cuộn dây có rãnh
- Hệ thống đóng gói cuộn xẻ tự động
- Best practices for vertical steel coil packaging
- From eye-to-wall to eye-to-sky in automated steel coil packaging
- Automated slit coil packing line for service centers
nguồn
- Specifications and stations: FHOPE slit coil packing line and automatic slit coil packaging system product pages
- Video trên Line: steel coil wrapping and packing on YouTube
- Coil weight, strap count and pallet load: our worked example, illustrative coil figures
- Tiêu chuẩn: EN 415-10 (máy đóng gói, an toàn chung); ISO 12100:2010
Lần cuối cập nhật: 17/10/2026