Rezumat
Flexible hose, garden tubing, and corrugated pipe emerge continuously from the extrusion line as wound coils. An eye-through orbital packing machine wraps each coil through its central aperture, sealing it against dust, moisture, and layer shifting during transit. Our upright FPH series positions the coil vertically on dual polyurethane-coated support rollers while a high-speed rotating ring conveys stretch film and protective tape through the core. The FPH-200 manages coil weights of 5–50 kg within a 15–35 s cycle, while the heavy-duty FPH-300N handles loads up to 100 kg within 23–35 s.
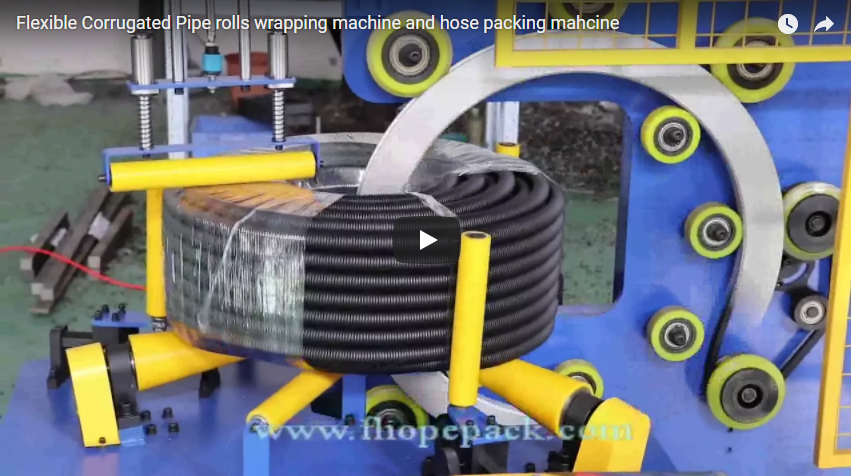
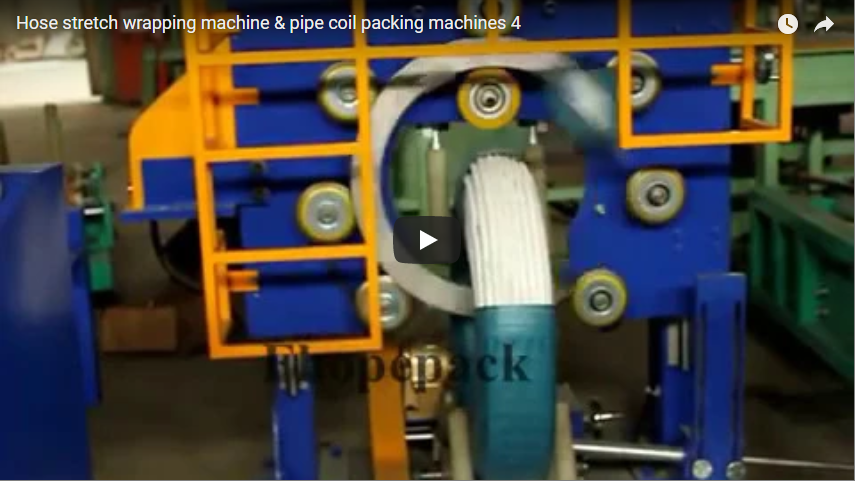
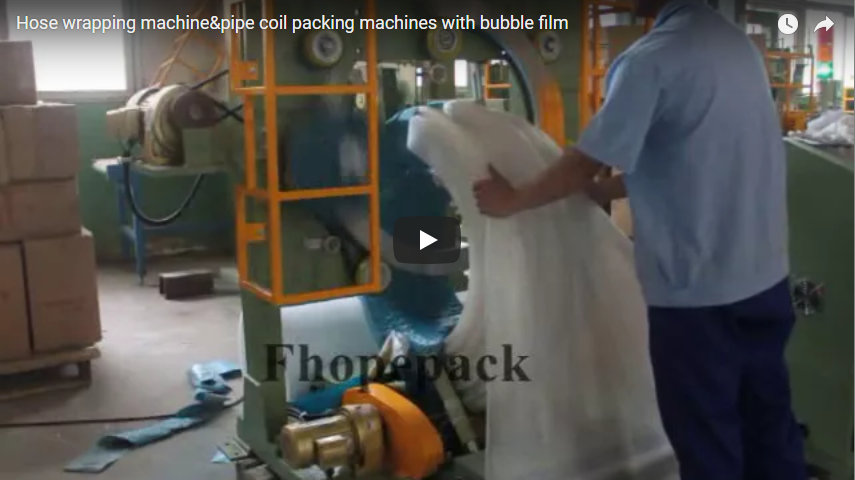
System Overview: Upright coil wrapper in operation. The rotating orbital ring passes through the coil eye while pneumatic side guide rollers stabilize lightweight flexible tubing. Dual material dispensers simultaneously apply clear stretch film and colored PE protective tape behind an interlocked safety perimeter.
Cuprins
- Soluții de etanșare a furtunurilor și țevilor în funcție de produs
- Cum funcționează o mașină de ambalat furtunuri cu ochi vertical
- Datele FPH-200 și FPH-300N
- Exemplu de lucru: o bobină de furtun de grădină de 50 m
- Folie, bandă PE sau hârtie
- Listă de verificare a selecției
- Siguranță: EN 415-10 și ISO 12100
- Întrebări frecvente despre inginerie
- Urmatorul pas
- Citire conexă
- Surse
Soluții de etanșare a furtunurilor și țevilor în funcție de produs
Packaging line integration depends directly on product rigidity, coil diameter, and the discharge state from the cooling trough or extrusion puller.
| Tip produs | Forma produsului | Soluție primară | Caracteristicile mașinii |
|---|---|---|---|
| Garden hose, PVC tubing, small corrugated conduit | Flexible coil, 5–50 kg | FPH-200 Upright Coil Wrapper | Dual dynamic side guides, low-inertia ring |
| Agricultural PE pipe, heavy electrical conduit coils | Semi-rigid coil, 10–100 kg | FPH-300N Upright Coil Wrapper | High-load cradle rollers, reinforced chassis |
| Continuous extrusion requiring winding | Loose unstrapped profile | Automatic Coiler & Strapping Cell | Pneumatic collapsible mandrels with PET strappers |
| Rigid conduit, PVC/PPR straight pipe bundles | 1 m to 6 m straight lengths | Învelitoare de întindere orbitală orizontală | Driven infeed/outfeed V-rollers, top clamps |
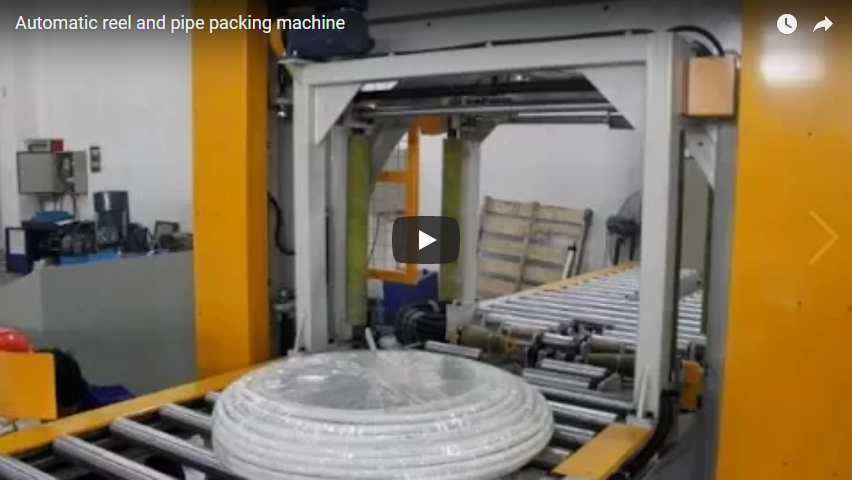
In automated extrusion plants, upstream dual-head automatic coiling units wind and strap the package before transferring it via gravity chute or roller conveyor to the FPH wrapping station. This layout eliminates manual handling at extrusion speeds up to 30 m/min.
Cum funcționează o mașină de ambalat furtunuri cu ochi vertical
The coil rests vertically on two motorized, polyurethane-lined cradle rollers. The orbital ring cuts perpendicularly through the center opening (eye) of the coil. Two pairs of adjustable side guide rollers prevent axial tilting or wobble caused by centrifugal air currents or film tension pull.
       [ Orbital Ring Rotation (ω) ]
                 ╭──────╮
     Side Roller │ ╭──╮ │ Side Roller
     [===]       │ │Co│ │       [===]
                 │ │il│ │
     ============┴─┴──┴─┴============
[Driven Support Rollers (v)]- Loading & Nesting: The operator or push-arm places the coil onto the driven rollers inside the open ring gap.
- Sincronizarea unității: Two independent variable frequency drives (VFD) govern ring rotation (rpm) and roller rotation speed. The ratio between the two sets the exact longitudinal film overlap.
- Eye-Through Helical Application: The film carriage travels circumferentially through the core, applying tensioned stretch wrap along the toroidal surface.
- Externarea: Upon cycle completion, the film tail is cut and wiped pneumatically, and the coil exits to packing or palletizing stations.
Because empty flexible hose coils have low radial stiffness, ring acceleration must follow an S-curve ramp. Excessive immediate film tension (greater than 20 N) can crush or ovalize thin-walled corrugated ducts.
Datele FPH-200 și FPH-300N
| Specificație tehnică | FPH-200 Standard Wrapper | FPH-300N Heavy-Duty Wrapper |
|---|---|---|
| Diametrul interior al bobinei (ID) | 300 – 600 mm | 300 – 700 mm |
| Diametrul exterior al bobinei (OD) | 400 – 900 mm | 500 – 1,000 mm |
| Lățimea bobinei (l) | 50 – 200 mm | 100 – 300 mm |
| Capacitatea de încărcare utilă a bobinei | 5-50 kg | 10-100 kg |
| Packaging Cycle Duration | 15–35 s/bobină | 23–35 s/bobină |
| Viteza de rotație a inelului | 20–90 r/min (controlat de VFD) | 20–120 r/min (controlat de VFD) |
| Roller Conveyance Speed | 2.0–4.0 m/min | 2.0–5.0 m/min |
| Overlap Adjustment Range | 20% la 90% | 20% la 90% |
| Putere instalată | 1.5 kW (380 V, 50 Hz, 3-Phase) | 1.9 kW (380 V / 480 V, 60 Hz, 3-Phase) |
| Standard Consumables | LLDPE Stretch Film, PVC Wrap | LLDPE Film, HDPE Woven, Crepe Paper |
| Specificații rolă de film | Width: 90–100 mm; OD: 100–180 mm; Core ID: 50 mm | Width: 90–150 mm; OD: 100–200 mm; Core ID: 50/76 mm |
Exemplu de lucru: o bobină de furtun de grădină de 50 m
1. Coil Geometry Verification
- Product: Garden hose, Outer Diameter (d_hose) = 25 mm.
- Total Length (L) = 50 m.
- Coil Core (ID) = 350 mm.
- Coil Target Width (W) = 200 mm.
- Turns per layer = 200 mm ÷ 25 mm = 8 turns.
| Layer Index (n) | Layer Mean Diameter (D_n) | Formula (Turn Length × 8) | Layer Hose Length | Cumulative Length |
|---|---|---|---|---|
| Stratul 1 | 350 + 25 = 375 mm | 8 × π × 0.375 m | 9.42 m | 9.42 m |
| Stratul 2 | 375 + 50 = 425 mm | 8 × π × 0.425 m | 10.68 m | 20.10 m |
| Stratul 3 | 425 + 50 = 475 mm | 8 × π × 0.475 m | 11.94 m | 32.04 m |
| Stratul 4 | 475 + 50 = 525 mm | 8 × π × 0.525 m | 13.19 m | 45.23 m |
| Layer 5 (Partial) | 525 + 50 = 575 mm | (50.00 m – 45.23 m) | 4.77 m (approx. 3 turns) | 50.00 m |
- Finished Coil OD = ID + 2 × (Layers × d_hose) = 350 + (2 × 5 × 25) = 600 mm.
- Dimensional Envelope: ID 350 mm, OD 600 mm, Width 200 mm. This falls directly within the FPH-200 operating window (ID 300–600 mm, OD 400–900 mm, Width 50–200 mm).
2. Wrapping Overlap & Cycle Time Kinematics
Wrapping with 100 mm width LLDPE film at a 50% target overlap on the outer perimeter:
- Outer Circumference (C_od) = π × OD = 3.1416 × 600 mm ≈ 1,885 mm.
- Effective advance per ring revolution at 50% overlap = Film Width × (1 – Overlap) = 100 mm × (1 – 0.50) = 50 mm.
- Required Ring Revolutions = C_od ÷ 50 mm = 1,885 ÷ 50 ≈ 38 ring revolutions.
- Note on Core Overlap: Because Inner Circumference (C_id = π × 350 ≈ 1,100 mm) is smaller than C_od, the inner aperture experiences an overlap greater than 70%, creating a water-tight seal through the coil core.
At a ring speed of 80 r/min:
- Pure Wrapping Time = (38 rev ÷ 80 r/min) × 60 s/min = 28.5 s.
- Adding 4.0 s for soft start/stop ramps and pneumatic tail cutting yields a total cycle time of 32.5 s, satisfying the FPH-200 standard operational threshold (15–35 s).
Folie, bandă PE sau hârtie
- Folie extensibilă LLDPE (17–25 µm): Delivers transparent product display, moisture isolation, and elastic bundle retention via controlled elastic memory.
- Colored PE Outer Tape: Applied concurrently via an auxiliary spindle mounted on the rotating ring. Shields UV-sensitive PVC compounds and provides color-coded brand differentiation.
- Reinforced Crepe Paper / VCI / HDPE Woven Tape: Installed on the FPH-300N for heavy industrial gas hoses or corrugated conduits demanding abrasion protection or breathable condensation control during export container shipping.
Listă de verificare a selecției
- Hose Profile: Pipe OD (mm), wall thickness, flexural modulus, and target length per coil (m).
- Coil Geometry Range: Minimum and maximum ID (mm), OD (mm), and axial coil width (mm).
- Limite de greutate: Finished coil mass (kg) to select drive gearbox rating.
- Debit de linie: Extruder line output (meters/minute) and coil production frequency (coils/hour).
- Upstream Equipment: Manual coiling rack vs. integrated automatic twin-spindle winder with strapping head.
- Auxiliary Needs: Integrated labeller, pneumatic coil ejector, or dual-material synchronized wrapping ring.
Siguranță: EN 415-10 și ISO 12100
The FPH platform complies with EN 415-10 (Safety requirements for packaging machines) and has undergone comprehensive risk assessment under ISO 12100: 2010.
- Carcasă mecanică: A heavy-duty, powder-coated steel cage surrounds the upper orbital path.
- Pază interblocată: Access panels utilize dual-channel safety limit switches tied to a safety relay circuit (Performance Level d / Category 3).
- Constrângere operațională: Coil realignment or manual film threading while the ring drive is energized is strictly prohibited. Positioning is executed purely prior to automated cycle initiation.
Întrebări frecvente despre inginerie
Q: Can a single FPH machine package both soft PVC hoses and rigid PE pipe coils? A: Yes, provided coil dimensions and weights fall within machine parameters. Softer hoses require low film tension (8–15 N) and slower acceleration ramps, while rigid coils can utilize maximum ring speeds (90–120 r/min) with higher tension settings.
Q: What is the true throughput of the FPH-200 packaging unit? A: Practical output ranges between 60 to 90 coils per hour under automatic continuous operation, governed by coil circumference, overlap setting, and material handling speeds.
Q: Can the wrapper interface with an automated upstream winder? A: Yes. The control cabinet includes standard I/O and optional Ethernet/IP or Profinet fieldbus architectures to handshake with upstream coilers and downstream transfer conveyors.
Q: How is wrap overlap adjusted on the shop floor? A: Overlap percentage (20% to 90%) is entered on the industrial HMI touchscreen. The PLC automatically modulates the frequency ratio between the ring drive inverter and the roller drive inverter.
Urmatorul pas
- Trimiteți specificațiile produsului: Forward your hose OD, coil ID/OD dimensions, and line throughput to info@fhopepack.com.
- Kinematic Matching: Our packaging engineering team calculates ring speeds and structural clearances to match your extrusion rate within 24 hours.
- Full System Quotation: Receive an equipment proposal with layout drawings, safety interlocking details, and consumption estimates.
Citire conexă
- Hose coil wrapper FPH-200 (product specifications)
- Hose wrapping machine FPH-300N (product specifications)
- Vertical hose coil wrapping machine video library
- Hose coil wrapping machine film tension demonstration
Surse
- FHOPEPACK Engineering Documentation: FPH Series Operating and Service Manual (FPH-200 / FPH-300N).
- Organizația Internațională de Standardizare: ISO 12100:2010 – Safety of machinery — General principles for design — Risk assessment and risk reduction.
- Comitetul European de Standardizare: EN 415-10:2014 – Safety of packaging machines — Part 10: General requirements.
Ultima recenzie: 21.09.2026