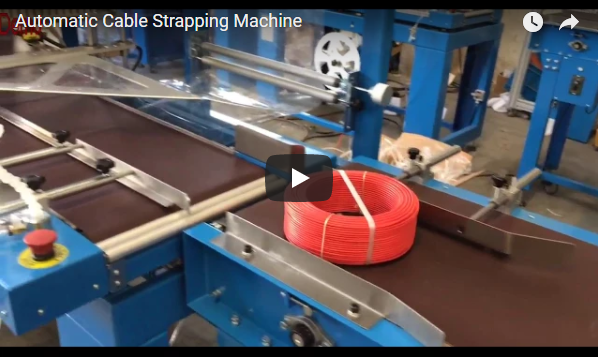
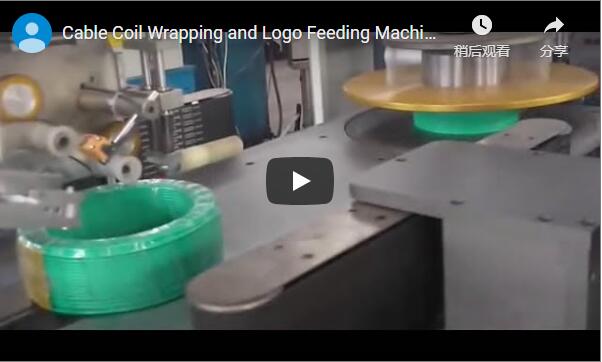
Streszczenie High-speed extrusion and coiling lines generate finished wire coils every few seconds, making manual handling a severe bottleneck that risks surface damage and line stoppages. This fully automatic packaging solution synchronizes a dual-head coiling unit, a toroidal eye-through orbital stretch wrapper, an automatic tape/label applicator, and a pneumatic discharge ramp feeding directly into shipping cartons. Guaranteeing zero line stoppage depends on matching the overall packing cycle time to the extrusion takt time across your shortest coil run. We calculate and configure ring rotational speed, roller indexing, and pneumatic dwell times to achieve continuous, hands-off output.
Spis treści
- System Overview & Motion Sequence
- How the Online Packaging Cycle Works
- Matching Wrap Cycle to Line Speed (Takt Time Calculation)
- Configuration Options for Cable Coil Packing
- Machine Controls and Functional Safety
- Selection Checklist for an Online Cable Coil Wrapper
- Często zadawane pytania dotyczące inżynierii
- Następny krok
- Powiązane artykuły
- Źródła
System Overview & Motion Sequence
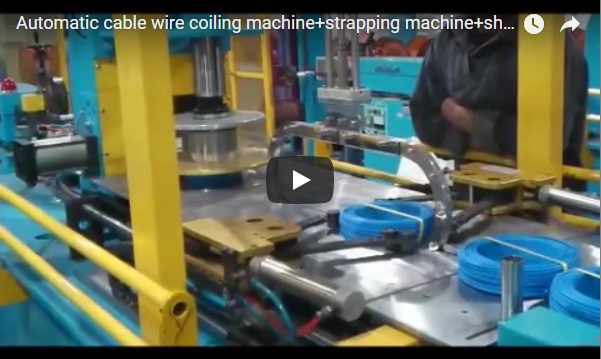
The online packaging system integrates three primary mechanical sub-assemblies: an automatic coiling and indexing feeder, a high-speed orbital wrapping ring, and a pneumatic drop-gate carton packing station.
During continuous operation, the finished cable coil is indexed from the coiler reel onto motorized polyurethane cradle rollers. An overhead pneumatic stabilizer cylinder secures the coil vertically, preventing core collapse or loose wraps.
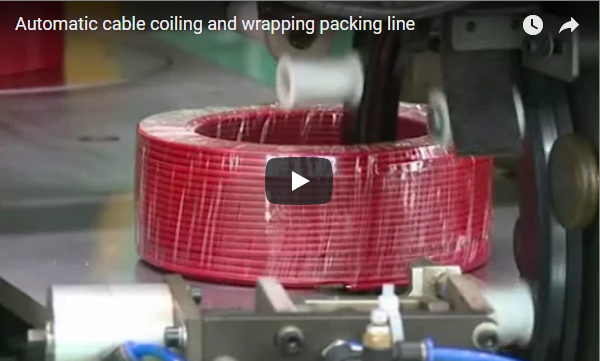
The orbital wrapping ring passes stretch film through the center eye of the coil while the cradle rollers rotate the coil along its toroidal axis. Concurrently, an integrated taping arm dispenses a protective label band across the outer diameter. Once wrapped and taped, a pneumatic horizontal pusher indexes the coil onto a low-friction roller conveyor, allowing it to slide smoothly down a guided chute into waiting corrugated cartons without manual intervention.
How the Online Packaging Cycle Works
The entire packing sequence is managed by a centralized PLC, sequencing five distinct mechanical phases:
| Faza | Sub-Assembly Action | Dynamic Function |
|---|---|---|
| 1. Infeed & Positioning | Pneumatic transfer guide & cradle rollers | Positions the loose-wound coil axially into the center eye-path of the wrapping ring. |
| 2. Clamping & Stabilization | Overhead pneumatic press roll | Delivers 0.2–0.4 MPa damping pressure to clamp the coil crown, eliminating vibration and ovality. |
| 3. Eye-Through Wrapping | High-speed aluminum cast rotating ring | Rotates the film dispenser shuttle through the coil center at 120–250 RPM; cradle rollers rotate the coil for 30%–70% film overlap. |
| 4. Cut, Clamp & Tape | Pneumatic shear blade & adhesive label dispenser | Cuts and heat-tacks/holds film tail while applying the perimeter paper/film branding band. |
| 5. Ejection & Boxing | Linear rodless cylinder pusher & gravity roller bed | Releases top clamp, advances the unit onto the rolling chute, and drops it into the staging carton below. |
This automated cycle ensures that finished electrical building wire (e.g., THHN, BV, RVV) moves from the capstan coiler directly into shipping cartons without cosmetic scuffs or human handling.
Matching Wrap Cycle to Line Speed (Takt Time Calculation)
To prevent extrusion line throttling, the total automated packaging cycle time (T_total) must be strictly less than the coiling time of a single reel (T_coiling).
The allowable takt time is calculated by:
T_coiling (s) = [Coil Length (m) ÷ Line Speed (m/min)] × 60
The wrapper cycle consists of mechanical movements plus active wrapping:
T_total = T_transfer + T_wrap + T_tape_cut + T_discharge
Przykład obliczeń inżynierskich
| Parametr | Specyfikacja ilustracyjna | Engineering Formula / Condition |
|---|---|---|
Line Speed (V_line) |
60 m / min | Extrusion line pull-off speed |
Coil Length (L_coil) |
100 m | Minimum run length per product cycle |
Allowable Coiling Takt Time (T_coiling) |
100.0 s | (100 m ÷ 60 m/min) × 60 s/min |
Coil Transfer & Clamp (T_transfer) |
4.5 s | Pneumatic arm indexing and top press stroke |
Active Wrapping Cycle (T_wrap) |
8.0 s | Ring speed: 180 RPM; 24 revolutions per coil |
Tape Dispensing & Film Cut (T_tape_cut) |
3.5 s | Pneumatic shear stroke and adhesive wipe |
Ejection to Carton (T_discharge) |
4.0 s | Pusher forward stroke and reset |
Total Packaging Cycle (T_total) |
20.0 s | Margin: 80.0 s (Line buffer: 80%) |
Shorter coil runs (e.g., 25 m or 50 m) reduce available coiling takt to 25–50 seconds. As long as T_total stays under the coiling takt time, zero bottleneck occurs.
For larger hose, conduit, or corrugated pipe bundles requiring heavy-duty horizontal rotary tables, consult our Maszyna do owijania rur HDPE i węży i nasz maszyna do pakowania rur i przewodów w zwoje.
Configuration Options for Cable Coil Packing
| Wymagania produkcyjne | Mechanical Engineering Solution | Korzyść operacyjna |
|---|---|---|
| Integrated Product Branding | Automatic radial tape / label band applicator | Applies company logo and barcode before final film cut. |
| Direct-to-Carton Packing | 45° adjustable roller chute with counter sensor | Automatically indexes cartons once preset coil count is met. |
| Wide Outer Diameter (OD) Variance | Servo-driven adjustable cradle roller center distance | Accommodates coil ODs from 150 mm up to 500 mm on one line. |
| High Extrusion Line Speeds (> 120 m/min) | Dual-ring shuttle wrapper or dual-station transfer bed | Cuts wrap cycle time down to 10–12 seconds per coil. |
| Moisture / Dust Corrosion Protection | Synchronized film-feeding shuttle (PVC + PE film / VCI) | Delivers 100% moisture-tight seal for maritime shipping. |
Machine Controls and Functional Safety
High-speed orbital rings operate with high rotational inertia. Equipment safety systems comply with international machinery directives:
- Safety Architecture & Risk Reduction: Zgodny z ISO 12100: 2010 (Risk assessment and risk reduction).
- Packaging Machinery SafeguardingZbudowany do EN 415-10: 2014 safety standards for packaging lines, incorporating interlocked perimeter perimeter mesh guarding and Category 4 / PL e safety light curtains across the coil infeed and discharge zone.
- Pneumatyczne zawory bezpieczeństwa: Main air manifold incorporates soft-start and dump valves compliant with ISO-13849 1 to exhaust trapped pneumatic energy upon Emergency Stop (E-Stop) activation.
- Blokada/Tagout (LOTO): OSHA 29 CFR 1910.147 compliant ball-valve lockouts for pneumatic supply and lockable electrical main disconnect switches.
Selection Checklist for an Online Cable Coil Wrapper
- Specyfikacje kabli: Conductor cross-section (mm²), overall outer diameter (OD), and sheath material (PVC, XLPE, LSZH, TPU).
- Geometria cewki: Minimum and maximum inner diameter (ID), outer diameter (OD), and core height (H).
- Line Speed & Length: Maximum line speed (m/min), minimum coil cut length (m), and target takt time (seconds).
- Consumables Specification: Stretch film width (50–100 mm), film thickness (15–35 µm), and paper/PVC label band widths.
- Logistyka downstream: Carton dimensions, stacking array (single vs. stacked), and roller conveyor height.
- Utility Interfaces: Compressed air supply (0.5–0.7 MPa clean, dry air) and power feed (380V/480V 3-phase 50/60 Hz).
Często zadawane pytania dotyczące inżynierii
Q: Can the orbital wrapping system keep up with high-speed extrusion lines? A: Yes. Because active wrapping takes only 8–15 seconds, a single packaging unit easily services extrusion speeds up to 100 m/min on 100-meter coils. For ultra-short coils (e.g., 25–30 meters) at high line speeds, an accumulator or dual-station transfer cradle is integrated.
Q: Does the coil clamp deform soft or flexible low-smoke zero-halogen (LSZH) cables? A: No. Clamping is performed by pneumatic cylinders fitted with precision proportional pressure regulators. Polyurethane contact pads distribute load evenly across the coil crown, maintaining structural roundness without indenting the sheath.
Q: Which production parameter dictates line capacity?
A: The shortest cut length at peak extrusion speed. This scenario yields the minimum coiling takt time (T_coiling), dictating the required orbital ring RPM and transfer speed.
Q: How does the system secure the tail of the stretch film? A: A pneumatic grip-and-cut mechanical unit holds the film leading edge at startup, releases it during rotation, and hot-melts or wraps the trailing end under tension during the final revolution.
Q: Can this wrapper handle both PVC and stretch films? A: Yes. The mechanical tension brake on the rotating shuttle can be adjusted manually or via dynamic electromagnetic braking to handle PE stretch film, PVC film, or woven PP tape.
Następny krok
Accelerate your line automation with our engineering team:
- Prześlij specyfikacje linii: Email your coil dimensions (OD/ID/Height), minimum cut length, and line speed to info@fhopepack.com.
- Receive 3D Layout & Takt Analysis within 48 Hours: Our application engineers will calculate your machine cycle times, line buffer requirements, and utility schematics.
- Conduct Final Design Review: Finalize electrical fieldbus protocols (Profinet, Ethernet/IP), mechanical hand-off conveyors, and delivery schedules.
Powiązane artykuły
- Automatyczna linia do pakowania cewek
- Automatic Horizontal Cable Coil Wrapping and Packaging Machines
- Economic Cable Coil Packing Machine & Wire Coil Strapping System
Źródła
- Technical Specifications & Machine Kinematics: FHOPE Engineering Technical Documentation, 2026-10-04.
- Takt Time & Kinematic Calculations: Internal packaging machinery engineering validation models.
- Demonstracja maszyny: Cable Packaging Systems on YouTube.
- Normy bezpieczeństwa i maszyn: ISO 12100:2010 Bezpieczeństwo maszyn, EN 415-10:2014 Wymagania bezpieczeństwa dla maszyn pakujących.
Ostatnia aktualizacja: 2026-10-04