Samenvatting
A film taping machine for sheet and panel, also called a protective film application machine or sheet film laminator, lays a full-width protective film on the face of boards, sheets and panels as they run along a conveyor. A film roll unwinds above the panel, a pressure roller pressed down by air cylinders bonds it flat, and the film is cut between panels. Our equivalent solution is sized to your panel width and line speed. This guide explains the parts, the common defects and how to avoid them, and how to work out film use and output.
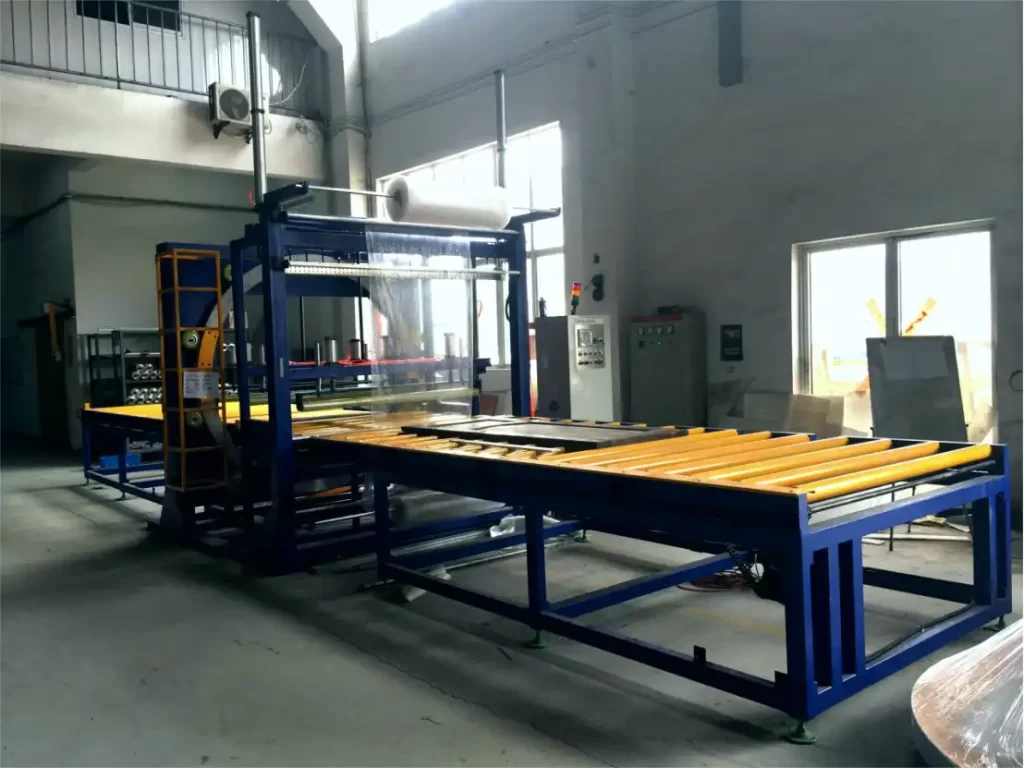
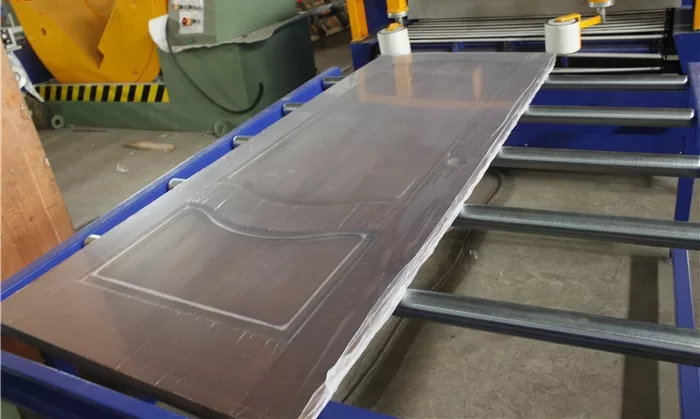
On this machine, white panels run on a roller conveyor between blue steel side frames. A full-width roll of green protective film sits across the line, and a pressure roller beam is lowered by pneumatic cylinders, fed by red air hoses, to bond the film to the panel face. The operator loads panels at the infeed, and the covered panels move on to the outfeed.
Inhoudsopgave
- Wat de machine doet
- Hoofd onderdelen
- Veel voorkomende defecten en hun oorzaken
- Film use per panel
- Panelen per uur
- De film kiezen
- Selectie checklist
- Veiligheid
- Veelgestelde vragen over techniek
- Volgende stap
- Gerelateerd lezen
- Bronnen
Wat de machine doet
Protective film keeps scratches, dust and handling marks off a finished face: coated metal sheet, aluminium composite panel, plastic sheet, laminate board or glass-like surfaces. Applied by hand, a full-width film wrinkles, traps air and goes on crooked. The machine applies it at an even tension and pressure, in line with your production or as a separate station before packing.
Hoofd onderdelen
| Deel | Job |
|---|---|
| Invoerrolband | carries and guides the panel, with side frames for alignment |
| Film ontspannen | holds the film roll; a brake or tension control keeps the film flat |
| Drukrol | rubber-covered roller lowered by air cylinders, bonds film to the panel |
| Afsnijden | cuts the film between panels, by hand or automatically |
| Drive | sets the line speed |
| Uitvoer | takes covered panels to stacking |
One-side or two-side versions are possible: a second unwind and roller under the panel cover the back face.
Veel voorkomende defecten en hun oorzaken
- Rimpels: film tension too low or uneven across the width. Fix the unwind brake and check roll alignment.
- Luchtbellen: pressure too low, or the panel is dusty. Raise cylinder pressure and clean the panel before the nip.
- Film running off to one side: panel not guided straight, or roller not parallel. Set the side guides and level the roller.
- Film lifting later: wrong film adhesion for the surface. Choose the film with your film supplier for the finish.
- Stretched film: tension too high. The film shrinks back later and curls panel edges.
Film use per panel
Film per panel = panel length + gap. Panels per roll = roll length ÷ film per panel. For a 2.44 m panel with a 0.1 m gap (example only):
| Check | Berekening | Resultaat |
|---|---|---|
| Film per panel | 2.44 + 0.1 | 2.54 m |
| Film area on a 1.22 m wide panel | 2.44 × 1.22 | ongeveer 3.0 m² |
| Panels per 500 m roll | 500 2.54 ÷ | over 196 |
Cutting the film at panel ends instead of leaving a gap saves the 0.1 m per panel, but needs an automatic cut-off.
Panelen per uur
Panels per hour = line speed × 60 ÷ panel pitch. At 10 m/min and a 2.54 m pitch (example): 10 × 60 ÷ 2.54 = about 236 panels per hour. In practice manual loading usually sets the rate, so match the speed to how fast your crew can load and unload. Maximum speed, width and power for your build are confirmed at quote.
De film kiezen
- hechting: low tack for polished or coated faces, higher for rough faces.
- Thickness and colour: thicker film for heavy handling; coloured or printed film shows clearly that the face is covered.
- Breedte: a little narrower or wider than the panel, depending on whether edges must be covered.
- Verwijdering: check the film peels off clean after storage and sunlight exposure.
Selectie checklist
- What are the panel widths, lengths and thicknesses?
- One side or both sides?
- Which surfaces and films will you run?
- What line speed or panels per hour?
- Manual or automatic film cut-off?
- Standalone, or in line with your production?
Veiligheid
The machine is designed to EN ISO 12100:2010 for risk assessment, EN 415-10 for packaging machine safety and EN 60204-1 for electrical equipment. The nip between pressure roller and panel is the main hazard, so it is guarded, with an emergency stop at the infeed.
Veelgestelde vragen over techniek
Q: Why does my film get bubbles? A: Usually low roller pressure or dust on the panel. Clean the panel and raise the cylinder pressure.
Q: Can it cover both sides? A: Yes, with a second unwind and roller under the panel.
Q: How many panels per hour? A: Line speed × 60 ÷ panel pitch. Loading speed often sets the real limit.
Q: Does it cut the film? A: By hand or automatically, as you choose.
Volgende stap
- Send your panel sizes, surfaces and film type naar info@fhopepack.com.
- Wij hebben een bepaalde maat. the width, rollers and cut-off.
- We reageren binnen 24 uur met een voorstel en een offerte.
Gerelateerd lezen
- Automatic profile tapping machine (product)
- Semi-automatische folie-aanbrenger op aluminiumprofiel
- Deurpaneel afdicht- en krimpmachine
Bronnen
- EN ISO 12100:2010; EN 415-10; EN 60204-1
- The sheet and panel film machine shown above
Laatst beoordeeld: 19-10-2026