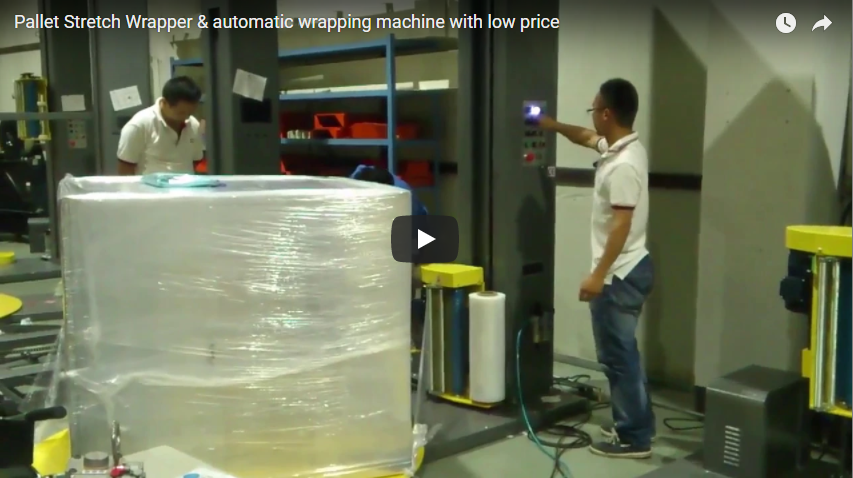
Kopsavilkums Designed for high-speed beverage packaging lines, this inline automatic turntable stretch wrapper integrates directly with factory roller conveyors to deliver unmanned end-of-line pallet unitization. The system utilizes a powered variable-ratio pre-stretch carriage with closed-loop tension regulation, critical for stabilizing light, unstable, and deformable shrink-wrapped bottle packs without causing load crushing. Overlap is mechanically governed by turntable angular velocity and vertical carriage travel: at 12 RPM and a 2.9 m/min carriage rise, the film advances 242 mm per revolution. While nominal 500 mm film yields a theoretical 51.6% overlap, factory-calibrated pre-stretch neck-in provides an effective overlap of approximately 42.4% (178 mm), ensuring structural integrity under rigorous dynamic transit conditions.
Why Bottle Pallets Are Different
Palletized beverage containers—particularly PET bottles and aluminum cans bundled in polyethylene shrink wrap—present unique engineering challenges compared to rigid corrugated cartoning.
In this inline installation, the automatic turntable wrapper interfaces directly with upstream accumulation lines and downstream pallet transfer conveyors. The infeed motorized roller conveyor transfers the unstable pallet onto the turntable deck. Once wrapping is complete and verified, the turntable aligns with the discharge vector and conveys the unitized pallet onto the outfeed line.
+------------------------+      +-------------------------------+      +-------------------------+
|  Upstream Accumulation | ---> | Turntable Wrapper with Power  | ---> |   Discharge Conveyor    |
|   Roller Conveyor Line |      | Rollers (Pneumatic Lock Pin)  |      |   to Warehouse/Shipping |
+------------------------+      +-------------------------------+      +-------------------------+
Bottle packs are inherently top-heavy and yield low interlayer friction coefficients. Multi-pack bundles rest entirely on the crown caps and rounded neck profiles of the layer below, resulting in minimal surface contact. Under improper film tension or abrupt rotary acceleration:
- Centrifugal shear displacement: Excessive angular acceleration (dω/dt) exerts lateral forces that can cause unconstrained upper tiers to slide off the layer interface.
- Package crushing vs. loose unwrapping: High tension without pre-stretch crushes corner bottles and deforms shrink packs. Insufficient containment force allows pallet loads to telescope during transit.
- Decoupling from the wooden base: If the bottom layers are not positively anchored to the pallet runners, the entire payload can shear off the pallet skid during warehouse braking or cornering.
To counteract these kinematic risks, the turntable drive is engineered with variable-frequency drive (VFD) S-curve soft start and soft stop control, preventing sudden torque spikes while maintaining high throughput.
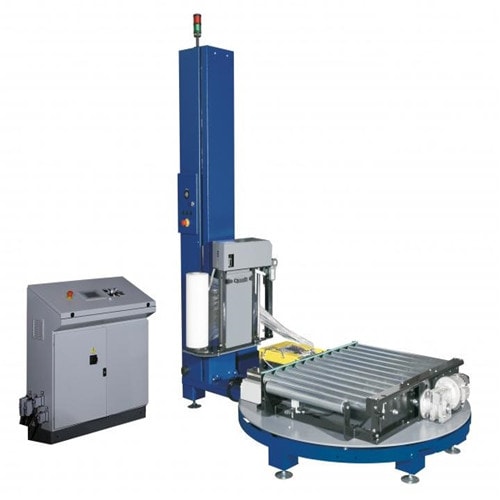
Automatic turntable stretch wrapper. The integrated roller deck transitions pallets in and out within inline conveyor circuits.
specifikācija
| Parametrs | Inženiertehniskā specifikācija | Practical Packaging Impact |
|---|---|---|
| Ražošanas jauda | Up to 25–35 loads/hour (load height dependent) | Matches standard medium-speed bottling line output |
| Maksimālais kravas svars | 1,800 kg | Handles dense water, soft drink, and beer pallets |
| Plates atskaņotāja sistēma | 2,200 mm diameter; chain-driven roller conveyor | Accommodates standard 1,000 × 1,200 mm and 1,200 × 1,200 mm skids |
| Rotācijas ātrums | 0–12 RPM (VFD adjustable via PLC) | Optimizes cycle duration against centrifugal stability limits |
| Turntable Acceleration | Inverter-controlled S-curve profile (3–6 s ramp) | Eliminates inertia shocks to delicate bottle towers |
| Stretch Film Spec | LLDPE machine grade; 500 mm web width; 20–25 µm | Balances high tensile yield with puncture resistance |
| Iepriekšējas stiepes attiecība | 250% standard (100%–300% electronically geared) | Converts 1 m of raw film into 3.5 m of wrapping web |
| Vagona vertikālais ātrums | 1.0–2.9 m/min (frequency controlled) | Determines vertical spiral pitch and layer overlap |
| Reinforcement Winds | Bottom, middle, top: 0–99 programmable cycles | Secures base-to-pallet anchor and top unconstrained layer |
| Pallet Height Sensing | Optical diffuse-reflection sensor with auto-delay | Accurately detects transparent PET film and shrink tops |
Overlap Calculation: Turntable Velocity vs. Carriage Feed
During continuous spiral wrapping, the film overlap ratio governs moisture resistance, structural containment, and film consumption per load. Vertical carriage pitch per turntable rotation dictates layer coverage.
1. Motion Calculation at Full Operating Velocity (12 RPM)
- Rotation Period per Turn:
T = 60 s ÷ 12 RPM = 5.0 s - Vertical Rise per Turn:
At the maximum carriage travel speed of 2.9 m/min (48.33 mm/s):
Rise = 48.33 mm/s × 5.0 s = 241.7 mm (≈ 242 mm per revolution) - Nominal Theoretical Overlap (Nominal 500 mm Web):
Nominal Overlap = 500 mm - 242 mm = 258 mm (51.6%)
2. Physical Pre-Stretch Neck-in Compensation
Raw nominal dimensions do not represent dynamic reality. When cast or blown LLDPE film passes through 250% motorized pre-stretch rollers, longitudinal elongation triggers transverse Poisson contraction (neck-in). By the time the film bridges the free air gap and contacts the load corners, effective web width (W_eff) reduces from 500 mm to approximately 420 mm (a 16% reduction).
- True Dynamic Overlap on Product Corners:
Dynamic Overlap = 420 mm - 242 mm = 178 mmDynamic Overlap Ratio = (178 mm ÷ 420 mm) × 100% ≈ 42.4%
Nominal Film Width:   |==================== 500 mm ====================|
Dynamic Neck-in Web:  |-------------- 420 mm --------------|
Carriage Rise:                             |=== 242 mm ===|
Effective Overlap:    |---- 178 mm (42.4%) -|
3. Reduced Speed Comparison Table (Carriage Rise Held at 2.9 m/min)
| Pagrieziena galda ātrums | Turn Period (s) | Vertical Rise / Turn (mm) | Nominal Overlap (500 mm) | Dynamic Overlap (420 mm Neck-in) | Ieteicamais pielietojums |
|---|---|---|---|---|---|
| 12 RPM | 5.0 s | 242 mm | 258 mm (51.6%) | 178 mm (42.4%) | High-throughput, stable bottom-trayed packs |
| 10 RPM | 6.0 s | 290 mm | 210 mm (42.0%) | 130 mm (31.0%) | Medium height, interlocked shrink packages |
| 8 RPM | 7.5 s | 362 mm | 138 mm (27.6%) | 58 mm (13.8%) | Low-tension dust-cover wraps (single pass) |
Inženiertehniskie noteikumi: If packaging unstable, trayless PET bottles, carriage ascent speed should be programmed down to 1.8–2.2 m/min when operating at lower rotational speeds to maintain at least 40% true dynamic overlap across the stack.
Wind Pattern Optimization for Unstable Bottle Packs
Uncontained cylindrical bottle columns demand a segmented tension and layer strategy executed via the control HMI:
[ Top Winds: 3-4 Wraps ] ---> High containment, tension balanced (Prevents crown cap slip)
         |
[ Spiral Body: 40%+ Overlap ] ---> Elastic membrane web (Absorbs road transit vibration)
         |
[ Base Anchor: 4-5 Wraps ] ---> Ties bottom bundle to wooden pallet (Prevents deck shearing)- Base Pallet Reinforcement (Bottom Winds: 4–5 turns): The film carriage dwells at its lowest mechanical boundary, wrapping both the lowest layer of bottles and the top 50–75 mm of the wooden pallet deck simultaneously. This forms a structural composite anchor that prevents horizontal load shift under emergency vehicle braking (0.8 g force standard).
- Column Body Wrapping (Middle Layers): Continuous spiral wraps overlap uniformly down and up the load height. Powered pre-stretch rollers isolate tension spikes from the load: film is elongated by 250% between dual rollers inside the carriage, allowing relaxed, low-tension film delivery onto the load. A responsive analog load-cell dancer roller continuously meters delivery speed to maintain contact tension within an ultra-precise 15–25 N band.
- Top Tier Stabilization (Top Winds: 3–4 turns): Bottles on the top layer have zero downward deadweight. If wrapped under high film contraction, perimeter bottles tilt inward. The PLC shifts the pre-stretch delivery to high feed matching while completing extra non-crushing reinforcement wraps to unitize the top plane.
Automated Film Handling for Unmanned Operation
Inline conveyor integration requires 100% hands-free cycle initiation, termination, and clean tail management:
- Pneumatic Scissor Clamp: At load arrival, a heavy-duty pneumatic clamp holds the leading edge of the stretch film securely above conveyor deck level. The turntable commences soft-start rotation; once the initial base wrap locks the film to the load, the clamp releases the tail automatically.
- Impulse Hot-Wire Cut-Off: Upon wrap completion, the turntable stops precisely at its zero-index alignment lock. A pneumatic arm advances an electrically heated impulse nichrome wire to slice through the film web cleanly with no frayed threads or film tearing.
- Pneumatic Wipe-Down Arm: Simultaneously, a trailing soft brush arm and pneumatic roller press the severed film tail firmly against the side of the pallet. The film’s natural cling properties fuse the tail flush with the wrapped surface, preventing trailing film edges from tripping warehouse automated storage and retrieval system (ASRS) photo eyes.
Utilities, Mechanical Alignment, and Safety Architecture
| Utility / Mechanism | Inženiertehniskais parametrs | Funkcionālā prasība |
|---|---|---|
| Elektropakalpojumi | 380–415 V AC, 3-Phase, 50/60 Hz | Hardwired to industrial main bus with lockable disconnect |
| Savienotā piedziņas jauda | Turntable: 0.75 kW; Deck Rollers: 0.75 kW; Carriage: 0.37 kW; Pre-stretch: 0.37 kW | Total power envelope: ~2.5 kW with continuous duty cycles |
| Kompresēts gaiss | 0.6–0.8 MPa (6–8 bar), clean, dry, non-lubricated | Powers clamping cylinders, cutting arm, and deck lock indexer |
| Mechanical Positioning | Heavy-duty pneumatic cone locator / lock pin | Locks turntable deck rigidly inline with factory rollers during pallet transfer |
| Conveyor Deck Height | 450–650 mm (adjustable via leveling feet) | Matches existing upstream/downstream roller conveyor lines |
Atbilstība normatīvajiem aktiem un drošība
- Machinery Risk Assessment: atbilst ISO 12100: 2010 principles for basic safety and lifecycle risk mitigation.
- Packaging Machinery Safety Standards: Engineered to satisfy LV 415-6: 2013 (specific safety criteria for pallet wrapping machinery) and LV 415-10: 2014 (general safety requirements for packaging equipment).
- Hazard Containment: Perimeter fencing with interlocked safety access doors (Category 4, PL d/e), integrated mute-capable light curtains at pallet infeed/outfeed portals, and dual-channel mushroom-head E-stop circuits.
Plant Engineering Selection Checklist
Evaluate the following technical constraints prior to project sizing:
- Palešu profils: Maximum load dimensions (Length × Width × Height), gross payload mass, and skid bottom deck configuration.
- Pack Packaging Style: Shrink wrap only (loose bundles), corrugated base trays with film, or open PET bottle cases.
- Line Cycle Rate: Peak hourly pallet volume output from upstream packaging machines (determines RPM and conveyor transfer speeds).
- Target Containment Force: Required containment retention (daN) to meet EUMOS 40509 or ASTM D4169 transport stability standards.
- Material Handling Handshake: Conveyor roller diameter, drive pitch, roller motor horsepower, and PLC interlocking protocol (Profibus, PROFINET, Ethernet/IP, or clean 24 V DC dry contacts).
- Pneumatic / Electric Availability: Clean air line delivery at minimum 0.6 MPa continuous pressure and plant voltage tolerance.
Biežāk uzdotie jautājumi
Q: Why must overlap be confirmed on actual product rather than calculated solely on paper?
A: Paper formulas assume an undeformed 500 mm flat film plane. In practice, mechanical pre-stretch ratios of 200%–300% induce 15%–20% transverse neck-in. Furthermore, rectangular pallets cause linear film velocity to surge and decelerate four times per revolution around corner radiuses. An on-site trial run confirms true minimum overlap across corner profiles.
Q: How does the system prevent thin-walled PET bottles from crushing?
A: Conventional friction-brake wrappers pull against the load to extract film, which instantly deforms loose bottle bundles. Our system uses a motorized pre-stretch carriage with an analog dancer arm: the film is elongated 250% between internal gearing rollers before it exits the carriage. The load only experiences the ultra-low payout tension (15–25 N) required to position the film against the pack.
Q: Can carriage lift speed and turntable rotation speed be adjusted independently?
A: Yes. The turntable and vertical carriage are driven by independent inverter-duty SEW/Nord gearmotors controlled by the PLC. Operators can fine-tune both parameters via the touchscreen HMI to achieve tailor-made overlap configurations ranging from 20% dust wrap up to 60%+ heavy-duty marine freight reinforcement.
Next Steps for Project Integration
Integrate automated turntable stretch wrapping into your packaging hall:
- Data Sheet Submission: Send your facility layout drawings, pallet dimension limits (L × W × H), container formats, and line speed targets to info@fhopepack.com.
- Proposal & Cycle Simulation: Our packaging engineering group will return a formal layout drawing, motion cycle analysis, and 3D integration scheme within 48 hours.
- Līniju integrācijas validācija: Schedule a factory acceptance review or virtual technical meeting with our engineering team to verify conveyor height alignment, network handshakes, and field commissioning logistics.
Related Systems & Resources
- Automatic Pallet Wrapping Machine B100 Series
- Video: Turntable Pallet Wrapper for the Beverage Industry
- Video: Automatic Pallet Wrapping Machine with Inline Conveyors
- Video: Inline Turntable Pallet Wrapper with Automatic Top Sheet Dispenser
- Video: High-Speed Rotary Arm Stretch Wrapping Machine A200
Reference Engineering Standards
- ISO 12100: 2010: Mašīnu drošība. Vispārīgie projektēšanas principi. Riska novērtēšana un riska samazināšana.
- LV 415-6: 2013: Iepakošanas mašīnu drošība. 6. daļa: Palešu ietīšanas mašīnas.
- LV 415-10: 2014: Iepakošanas mašīnu drošība. 10. daļa: Vispārīgās prasības.
- EUMOS 40509:2020: Test method for load unit rigidity and transport stability validation.
Technical review completed: October 2024 | Principal Systems Engineer, Packaging Automation Group