개요
An automated aluminum profile packing line integrates sub-bundle strapping, high-speed orbital spiral wrapping, automated collation, and master bundle master-wrapping into a continuous flow. The inline sub-bundle wrapping station handles cross-sections from 외경 100mm ~ 300mm and lengths exceeding 1,000 mm at line speeds up to 12m/분. Because the orbital wrapper acts as the primary pacing bottleneck between upstream extrusion outputs and downstream master bundling, overall line throughput is sized directly around this station’s cycle and cycle-reset envelope.
차례
- 포장 라인의 스테이션
- 서브 번들 래퍼의 작동 방식
- Bundle Window: Physical and Dimensional Envelope
- Which Station Sets the Line Pace?
- End Taping and Material Management
- Utilities, Safety, and Compliance Standards
- 엔지니어링 선정 체크리스트
- 자주 묻는 질문 (FAQ)
- System Sizing and Proposal Next Steps
- 관련 기술 문서
- 표준 및 기술 참조
포장 라인의 스테이션
Plant layout, extrusion press capacity and profile specifications dictate the line topology. A standard automated packaging line integrates seven core stations:
| 역 계단 | 시스템 기능 | Station Description |
|---|---|---|
| 01 | Sub-bundle binding | 4 binding stations securing loose extrusions |
| 02 | Sub-bundle transfer | Transfer arms bridging binding tables to the wrapper |
| 03 | Sub-bundle orbital wrapping | High-speed continuous stretch/paper wrapper |
| 04 | 서브번들 수집 및 정렬 | Buffer table aligning wrapped sub-bundles |
| 05 | Master bundle assembly | Multi-fork gantry assembling final bundle matrices |
| 06 | Master bundle wrapping | Orbital wrapper for shipment-ready master packs |
| 07 | Bundle outfeed | Motorized discharge roller tables |
The line wraps with kraft paper or LLDPE stretch film. A 6-fork transfer mechanism lifts an entire layer of sub-bundles onto a staging roller bed, repeating the cycle until the planned bundle matrix is complete.
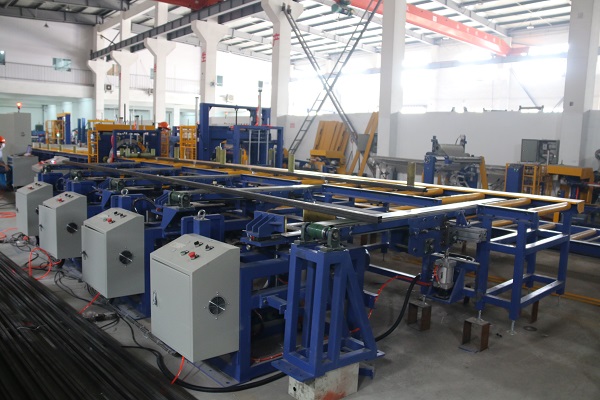 Figure 1: Fully automated aluminum profile packaging line showing motorized polyurethane-coated roller conveyors and integrated master control panels.
서브 번들 래퍼의 작동 방식
The sub-bundle advances on powered infeed rollers into the rotating orbital ring. The reel of paper or film rides a circular track and applies a helical wrap while the conveyor moves the bundle forward.
[Infeed Conveyor] ---> [Centering Rollers] ---> [Hold-Down Unit] ---> [Orbital Ring] ---> [Outfeed Conveyor]
                                                        │                     │
                                                        ▼                     ▼
(Anti-Torsion) (Continuous Spiral)- 중심: Conical vertical rollers centre incoming profiles on the pass-line.
- 누르고 있기: Pneumatic rollers clamp the extrusions to the bed, preventing twist, splay and vibration at high ring speed.
- 사이클 제어: Photocells detect the bundle ends and trigger film feed, wrapping, clamping and cutting via the PLC.
Bundle Window: Physical and Dimensional Envelope
The sub-bundle wrapper handles standard mill-finish, powder-coated and anodized extrusions:
| 매개 변수 | Specification Window | 엔지니어링 노트 |
|---|---|---|
| Bundle Cross-Section (OD) | 100mm에서 300mm | Diagonal must clear the inner ring |
| 번들 길이 | 1,000mm ~ 6,000mm 이상 | Extension conveyors sized per layout |
| Sub-Bundle Weight | 15kg에서 100kg | Within standard conveyor loading |
| Wrapper Conveyors | 2,000 mm infeed / 2,000 mm outfeed | 기본 면적 |
| 선형 컨베이어 속도 | 6m/분 ~ 12m/분 | VFD 제어 |
| 링 회전 속도 | 20RPM ~ 90RPM | Inverter driven |
| Nominal Wrap Output | 5m/분 ~ 15m/분 | Governed by overlap and travel |
| Spiral Overlap Range | 10의 % 90 %로 | Adjustable via VFD and ring speed |
예시: six profiles at 1.5 kg/m and 6 m long weigh 54 kg, within the 15–100 kg rating. Conveyor speed is limited to 12m/분 to prevent profile slippage on the roller surfaces.
Which Station Sets the Line Pace?
With four upstream binding positions feeding one sub-bundle wrapper, the wrapper is the line’s critical path.
The pure wrapping cycle time per 6-meter bundle scales with conveyor feed rate:
| 선형 래핑 속도 | Pure Wrap Cycle (6 m bundle) | 이론적인 최대 처리량 |
|---|---|---|
| 12m/분 | 30 초 | 120개 묶음/시간 |
| 5m/분 | 72 초 | 50개 묶음/시간 |
Cycle time allowances: these figures cover continuous wrapping travel only. Transfer, film cutting and roll changeover add time.
For a master bundle of 12 sub-bundles, wrapping travel is 12 × 30 s = 360 s (6 min). This window lets the downstream master bundling station gather, stack and wrap without halting extrusion outfeed.
End Taping and Material Management
An integrated taping unit secures trailing ends so paper edges do not unravel during handling and transfer.
Taping runs while the bundle moves, synchronized with the wrap so tail fastening stays off the critical path.
| Material Handling Item | 기술 사양 |
|---|---|
| Supported Packaging Media | Paper or stretch film |
| Supply Roll Core Diameter | 50mm 내경 |
| Supply Roll Width & Outer Diameter | 100 mm to 200 mm width; 100 mm to 200 mm OD |
| 장력 조절 | Adjustable, mechanical or pneumatic |
| Cut-and-Feed Mechanism | Automatic cutter and mechanical arm feed |
Utilities, Safety, and Compliance Standards
| 유틸리티 요구 사항 | Specification (Sub-Bundle Wrapper Base Unit) |
|---|---|
| 전력 공급 | 380 V ±10%, 3-Phase, 50/60 Hz (Configurable to 480 V / 220 V) |
| 연결된 드라이브 전원 | Approximately 2.5 kW (Wrapper drive and base roller motors) |
| 공압 공급 | 0.5 MPa to 0.7 MPa (clean, dry, filtered air) |
산업 안전 표준
- ISO 12100:2010: Risk assessment and risk-reduction integration.
- EN 415-10 : 2014: General packaging machine design and safeguarding requirements.
- 구역 보호: Interlocked fencing around the ring, light curtains at the apertures, and redundant E-stop circuits on safety relays.
엔지니어링 선정 체크리스트
Prior to finalized mechanical layout and quotation, our engineering department reviews the following key operational parameters:
- Cross-Section Profile Geometry: Solid, hollow, architectural or structural profiles, including wall thickness and weight per metre.
- Bundle Assembly Configuration: Profiles per sub-bundle (e.g., 4, 6, 8) and the collation matrix for master bundles.
- Surface Protection Standards: Anodized, powder-coated, electrophoretic or mill-finish requirements.
- Wrapping Media Strategy: Kraft paper vs. stretch film, plus tape-banding requirements.
- 용량 목표: Required output in metric tons per shift or master bundles per hour.
- 시설 면적: Layout drawings showing discharge orientation, columns and crane clear-height.
- Site Power and Air Supply: Facility voltage, frequency and compressed-air capacity.
자주 묻는 질문 (FAQ)
What is the maximum package envelope the sub-bundle wrapper accepts?
The unit accepts cross-sectional package diagonals between 100 mm and 300 mm, lengths from 1,000 mm upward, and total weights between 15 kg and 100 kg.
What is the net packaging time for a standard 6-meter bundle?
At 12 m/min, pure wrapping travel takes 30 seconds; with feed-in, film cut and discharge, floor cycle time is about 40–45 seconds per sub-bundle.
Can the system wrap single extrusions without bundle grouping?
Yes, provided the profile diagonal exceeds the 100 mm OD limit. Smaller profiles need custom guides or grouped sub-bundling.
Why is end taping recommended for paper wrapping applications?
Unlike stretch film, kraft paper lacks natural cling. End taping stops trailing seams from tearing during transfer to the master stacking bed.
Can the wrapper switch between paper and stretch film on the same ring?
Yes. The tension carriage accepts standard 50 mm core rolls of crepe paper, woven tape or LLDPE film with adjustable tension.
System Sizing and Proposal Next Steps
Our engineering team dimensions turn-key aluminum extrusion packing lines via a structured 3-stage process:
- Submit Facility Drawings and Specifications: Send layout drawings, profile sections, bundle recipes and target capacity to info@fhopepack.com.
- Receive Proposal Within 48 Hours: We deliver a proposal with cycle-time balancing, layout drawings and station-by-station motor schedules.
- Engineering Site Review: On-site validation to finalize foundations, electrical tie-ins and outfeed logic.
관련 기술 문서
- 자동 알루미늄 프로파일 포장 라인 시스템
- High-Speed Aluminum Profile Sub-Bundle Wrapping Machine
- Automatic Aluminum Wrapping and Tape-Banding Unit
- Technical Video: Horizontal Aluminum Profile Stretch Wrapping Station
- Technical Video: Automated Solid Aluminum Rod and Extrusion Wrapper
표준 및 기술 참조
- ISO 12100:2010: 기계의 안전 — 설계의 일반 원칙 — 위험 평가 및 위험 감소. ISO Standards Portal.
- EN 415-10 : 2014: 포장기계의 안전 — 제10부: 일반 요구사항. NEN Standards Portal.
- FHOPE Internal Engineering Archive: Extrusion Packaging Technical Specifications and Pacing Manuals (Rev. 2026-10-11).
Last reviewed by Principal Packaging Systems Engineer on October 25, 2026.





