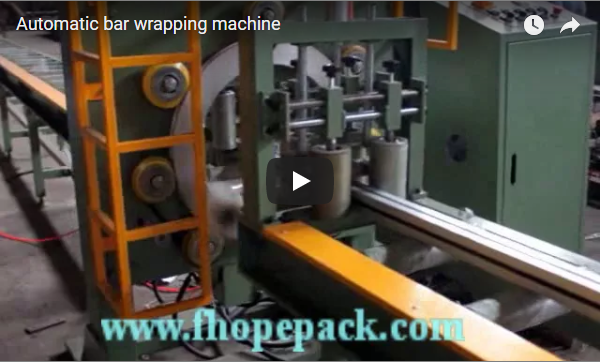
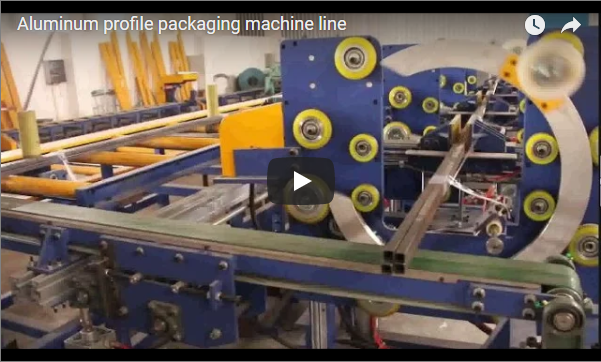
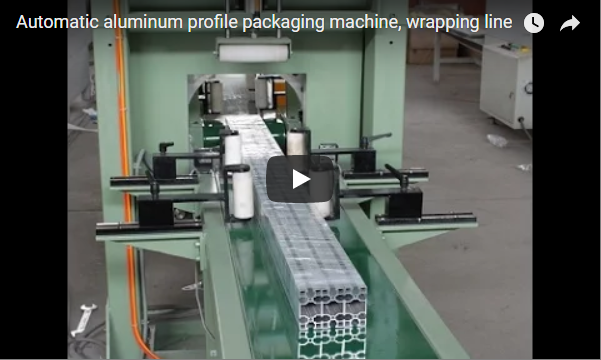
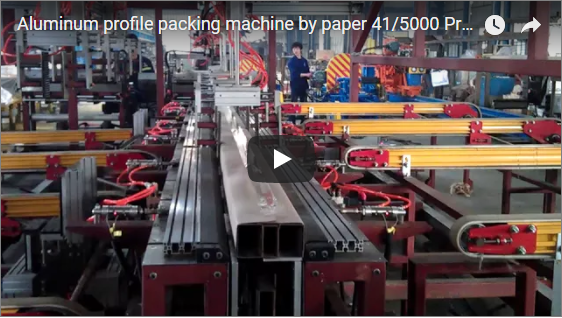
خلاصه اجرایی A horizontal orbital stretch wrapping machine turns an orbital film carriage along a rigid circular ring while motorized conveyors advance long bundles horizontally through the ring, applying a continuous, tightly overlapped spiral wrap. The technical sequence demonstrates the dynamic process: a counterbalanced carriage dispenses film around an E1000 rotating ring frame over heavy-duty support rollers, while pneumatic top press-down units stabilize the product profile against displacement. Engineered for profiles, wood battens, plastic extrusions, and metal bundles, the E1000 orbital wrapper accommodates cross-sections from 400 mm to 1000 mm outer envelope (or equivalent diagonal) and unit weights from 50 kg to 400 kg, operating at variable ring speeds between 10 r/min and 60 r/min.
فهرست مندرجات
- آنچه کلیپ نشان میدهد، به ترتیب
- زمان چرخه روی کلیپ
- نحوه عملکرد دستگاه استرچ رپ اوربیتال افقی
- مشخصات بستهبندی مداری E1000
- چک تاکت
- چک لیست انتخاب برای دستگاه استرچ رپ مداری
- کنترلها و ایمنی
- سوالات متداول مهندسی
- مرحله بعدی
- خواندن مرتبط
- منابع
آنچه کلیپ نشان میدهد، به ترتیب
The E1000 horizontal orbital stretch wrapper operates within an integrated structural steel frame featuring an enclosed cast-aluminum alloy rotating ring, shielded on top by safety-interlocked perimeter wire mesh guards. A heavy-duty roller conveyor system traverses the ring bore, managed through a standalone NEMA/IP-rated PLC operator console positioned safely clear of the rotating orbit.
- 0 to about 3 s (Initial Clamp & Lead-End Reinforcement): The load enters the wrap station on driven rollers. As the leading edge triggers the optical alignment zone, pneumatic vertical press-down rollers descend to anchor the profile. The yellow dynamic film carriage rotates smoothly from the top quadrant, applying anchor wraps around the leading edge while the conveyor remains stationary.
- About 3 to 6 s (Primary Spiral Pitch Progression): The variable-frequency drive synchronizes ring rotation with the roller conveyor infeed speed. The film carriage orbits continuously at constant tension, spanning the gap between conveyor beds and laying overlapping stretch film across the moving load.
- About 6 to 10 s (Continuous Wrapping & Trailing Edge Prep): High-speed rotation stabilizes as multiple protective film layers build up along the load length. Pneumatic guide assemblies maintain bundle alignment, eliminating lateral shifting and vibration throughout the orbital cycle.
زمان چرخه روی کلیپ
| روی کلیپس قدم بگذارید | پنجره زمانی | مدت زمان | Motion & Mechanical Function |
|---|---|---|---|
| اولین چرخشهای کالسکه | ۰ تا حدود ۴ ثانیه | حدود ۱۱ ثانیه | Ring acceleration and lead-end reinforce wrapping under stationary hold |
| فیلم روی بار گذاشته شده است | حدود ۱۲ تا ۳۰ ثانیه | حدود ۱۱ ثانیه | Synchronized axial conveyor advance with controlled overlap wrapping |
| ساخت لایهها | حدود ۱۲ تا ۳۰ ثانیه | حدود ۱۱ ثانیه | High-speed spiral wrapping with overhead pneumatic stabilization |
Note: The recorded clip captures a representative 10-second process phase of steady-state wrapping. Full production cycles incorporate automated head clamping, indexed advance, tail-end reinforced wrapping, and automated cut-and-wipe routines.
نحوه عملکرد دستگاه استرچ رپ اوربیتال افقی
The horizontal orbital packaging process synchronizes product transit with continuous rotary web dispensing:
- Infeed & In-Position Detection: Powered infeed rollers convey long components toward the ring center. An adjustable diffuse photocell sensor detects the front edge, initiating conveyor deceleration and commanding overhead pneumatic clamp cylinders to apply targeted vertical holding force.
- Rotary Orbital Wrapping: The high-strength structural ring, guided by durable polyurethane support rollers, accelerates via inverter control. The dynamic carriage releases film under mechanical or power-pre-stretch roller tension. The spiral overlap ratio is governed by the kinematic relationship between conveyor linear velocity (
V_conv), ring rotational speed (ω_ring), and effective film roll width (W_film):Overlap Ratio (%) = [1 - V_conv / (W_film × ω_ring)] × 100%Standard operational overlap settings range from 10% for dust protection to 90% for high-rigidity structural bundling. - End Reinforcement & Cut-Off: Tail-edge wrap reinforcement is programmable via the HMI touchscreen (1 to 5 turns). Upon completion, a heavy-duty pneumatic mechanical scissor arm and clamping hand grip the film web, execute a clean mechanical blade or impulse hot-wire cut, and park the film tail securely for seamless start of the subsequent bundle.
| بخش | چقدر می شود؟ | مشخصات مهندسی |
|---|---|---|
| Reinforced cast-aluminum ring (width ≤ 60 mm) | Carries the film carriage at high speeds | Dynamically balanced alloy, low inertia |
| Infeed and outfeed roller conveyors | Advance products through the wrapping zone | Polyurethane-sleeved or galvanized steel rollers |
| High-precision photocell sensor | Senses load boundaries and triggers cycles | Infrared diffuse reflection, adjustable gain |
| Pneumatic press-down & side devices | Restrain loads and suppress cantilever bounce | Dual-action cylinders with pressure regulators |
| Automated cut & clamp mechanism | Grips, cuts, and buffers film web | Pneumatic mechanical clamp with industrial knife |
| Control architecture (PLC, HMI, VFDs) | Governs cycle speeds, interlocks, and overlaps | Siemens/Delta PLC with multi-recipe memory |
مشخصات بستهبندی مداری E1000
| دستگاه استرچ رپ مداری E1000 | Standard Technical Specification |
|---|---|
| Object length capability | 1000 mm to continuous maximum |
| Cross-section / Bundle envelope | 400 mm to 1000 mm outer diameter (Diagonal ≤ 1000 mm) |
| ظرفیت وزن بسته نرم افزاری | 50 kg to 400 kg (Higher on engineered frames) |
| Infeed conveyor dimensions | 2000 mm length × 1200 mm effective roller width |
| Outfeed conveyor dimensions | 2000 mm length × 800 mm effective roller width |
| سرعت خطی نوار نقاله | 3 m/min to 12 m/min (Inverter controlled) |
| سرعت چرخش حلقه | 10 r/min to 60 r/min (Soft-start / soft-stop VFD) |
| مواد بستهبندی سازگار | Cast LLDPE stretch film, PE woven strip, VCI rust-inhibiting paper |
| Overall machine footprint | تقریباً طول ۵۲۰۰ میلیمتر × عرض ۱۶۰۰ میلیمتر × ارتفاع ۱۸۰۰ میلیمتر |
| Connected utility load | 4.5 kW, 380 V AC, 50/60 Hz, 3-Phase + PE, 0.5–0.7 MPa air |
چک تاکت
Packaging cycle calculations depend on bundle geometry, required overlap, and reinforce wraps:
- Passage Duration: For an illustrative 3000 mm long extrusion package running at an infeed rate of 6 m/min (0.1 m/s), linear transit time through the ring is:
T_travel = 3000 mm / (100 mm/s) = 30 seconds - Indexing & Cut Cycles: Adding 10 seconds for initial lead-end wrapping (3 turns), trailing reinforcement, and automated pneumatic cut-clamp action yields a total floor-to-floor cycle time of approximately 40 seconds per bundle.
- Line Output: This configuration delivers a gross packaging throughput of up to ۴۵ بسته در ساعت.
Adjusting conveyor advance speed allows operators to balance tighter film consumption with maximum line productivity according to upstream manufacturing takt.
چک لیست انتخاب برای دستگاه استرچ رپ مداری
- پاکت مقطعی: Verify maximum load width (
W) و ارتفاع (H) against ring clearance:D_ring ≥ √(W² + H²) + Margin (≥ 150 mm). - Takt & Throughput Target: Confirm bundles-per-hour requirement against transit speed and multi-wrap reinforcement settings.
- سازگاری مواد بسته بندی: Specify LLDPE stretch film (17–35 µm), anti-corrosion VCI film, reinforced kraft paper, or woven tape.
- الزامات حفاظت از سطح: Check necessity for rubber-coated/polyurethane conveyor rollers and non-marking press-down wheels.
- End-Seal Mechanism: Select pneumatic mechanical knife cutting or thermal wire severing based on film thickness and composition.
- رابطهای یکپارچهسازی: Determine whether stand-alone manual push-button controls or upstream line integration (dry contacts / Profinet) are required.
کنترلها و ایمنی
Orbital stretch wrappers feature rotational inertia hazards that necessitate rigorous machine guarding and control integration:
- Perimeter Guarding & Exclusion Zones: The E1000 incorporates rigid structural guarding around the rotating assembly. Interlocked safety switches remove drive power whenever maintenance panels are opened.
- Operator Decoupling: The control console is physically isolated from the rotating plane, keeping line operators entirely outside the hazard zone during automatic operation.
- LOTO Protocols: Standard operating procedures mandate formal Lockout/Tagout (OSHA 1910.147 / EN ISO 14118) isolation of both electrical supply and pneumatic pressure prior to film reel replacement, threading, or clearing load jams.
- Inching & Setup Modes: Low-speed jog routines enable safe carriage threading and setup without compromising structural guarding integrity.
- دامنه انطباق: Equipment safety designs align with ISO 12100: 2010 (Risk Assessment and Risk Reduction) and EN 415-10: 2014 (Safety Requirements for Modular Packaging Machines).
سوالات متداول مهندسی
Q: What package profiles are suitable for the E1000 horizontal wrapper? A: The system handles rigid and semi-rigid long profiles exceeding 1000 mm in length, with outer cross-sectional envelopes between 400 mm and 1000 mm (or maximum diagonal ≤ 1000 mm), and unit weights between 50 kg and 400 kg.
Q: How does the automatic cutoff mechanism secure film tails? A: A pneumatic mechanical clamp captures the film against the finished bundle while an integrated heavy-duty blade cuts the web cleanly. The clamp retains the tail, positioning it ready for immediate application to the next incoming bundle without manual re-threading.
Q: How is the overlap percentage configured and maintained? A: Film overlap is dialed in via the HMI touchscreen by varying ring rotational velocity (10 to 60 r/min) relative to conveyor speed (3 to 12 m/min). The onboard PLC recalculates inverter output frequencies to hold constant overlap across varying profile lengths.
مرحله بعدی
To size an optimal orbital wrapping layout for your production line, our engineering team follows a systematic three-stage evaluation:
- Submit Layout & Bundle Data: Forward your bundle dimensions (length, cross-section drawings), material types, line height, and output targets to info@fhopepack.com.
- دریافت پیشنهاد مهندسی ظرف ۴۸ ساعت: Obtain a complete package detailing recommended wrapper frame size, conveyor layout, cycle time calculations, and layout CAD drawings.
- Technical Verification & Alignment: Schedule an engineering consultation to confirm line integration points, infeed/outfeed transfers, and safety boundary interlocks.
خواندن مرتبط
- E1000 horizontal stretch wrapper technical parameters
- Profile orbital wrapping machine with 90 degree transfer system
- Horizontal wrapping machine for wood battens and metal extrusions
منابع
- مشخصات دستگاه: صفحه محصول دستگاه استرچ لفاف افقی E1000
- Video demonstration & engineering footage: FHOPE Orbital Packaging Systems on YouTube
- استانداردهای ایمنی بینالمللی: ISO 12100:2010 ایمنی ماشین آلات, EN 415-10:2014 ایمنی ماشین آلات بسته بندی
آخرین بررسی: 2026-10-05