خلاصه اجرایی
Steel coil wrapping and strapping starts at the hot mill: the coil is strapped first to prevent spring-back and catastrophic burst, then wrapped downstream once cooled to protect against moisture and rust. Our automatic radial strapping machine runs high-tensile steel straps through the coil eye while the coil sits securely on the conveyor line. This guide details the radial strapping sequence, strap sizing and tension safety thresholds, calculation formulas, and downstream packaging line integration.
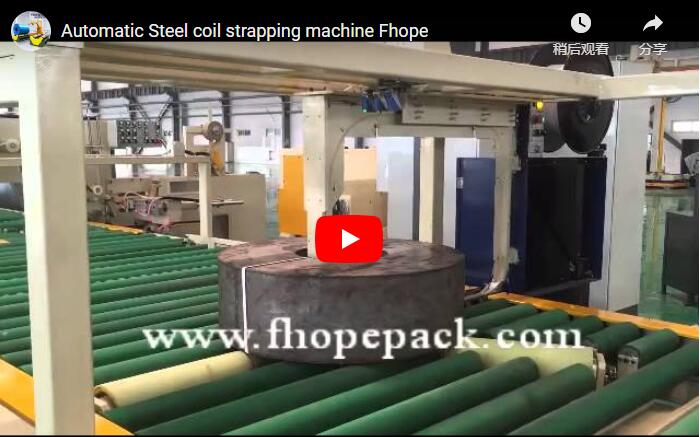
Automatic coil processing line: hot-rolled steel coils rest in an eye-horizontal orientation on a heavy-duty slat conveyor. A heavy-duty gantry strapping station straddles the coil transfer line, indexing its high-temperature telescoping track through the bore to apply high-tension radial binding before line handoff.
فهرست مندرجات
- چرا اول تسمه، بعد پیچیدن
- چرخه تسمهکشی شعاعی
- محدوده کویل و تسمه
- اندازه و کشش تسمه
- طول تسمه در هر کویل
- جایی که بسته بندی مناسب است
- بهترین شیوه
- چک لیست انتخاب
- ایمنی
- سوالات متداول مهندسی
- مرحله بعدی
- خواندن مرتبط
- منابع
چرا اول تسمه، بعد پیچیدن
A freshly coiled strip straight from the hot strip mill coiler retains severe elastic recovery strain (coil spring-back). Without immediate containment, outer laps relax and burst open during cooling or crane transfer.
- Strapping (Mill Exit): High-tensile steel strapping applies direct radial holding force through the coil eye, stabilizing laps immediately for rough crane handling, coil yard buffer transfer, and pickling input. In high-temperature hot-rolled projects, our heavy-duty strapping machines operate directly behind the downcoiler at coil temperatures up to 800 °C.
- Wrapping (Post-Cooling): Stretch film and VCI barriers are polymer-based and degrade at rolling temperatures. Film wrapping must only be performed after coil temperatures drop to ambient levels, sealing the cold-rolled, pickled, or slit coil against ambient humidity, airborne contaminants, and road splash during transport.
چرخه تسمهکشی شعاعی
- ورودی کویل: The walking beam or heavy-duty coil car indexes the eye-horizontal coil onto the strapping cradle/slat conveyor and retracts to safe clearance height.
- دستگاه خاموش: The gantry descends to the coil surface while the segmented inner strap track traverses through the coil ID (eye) and locks to complete a rigid circulating arch.
- خوراک: The motorized strap feed group drives the 19–32 mm steel strap through the hardened track guides until the optical and mechanical limit sensors verify full return at the strapping head.
- مهر: The floating tensioning head engages the coil OD, draws strap slack, pulls the programmed tension, crimps the double-notched seal (or 50 × 32 mm buckle from 0.9 mm sheet), and shears the strap end.
- برگشت: The arch track uncouples and retracts from the bore, the strapping head returns to home position, the gantry raises, and the strapped coil transfers downstream.
With dual strapping head configurations, two radial straps are indexed and crimped simultaneously without rotating the coil. For single-head systems with integrated 360° slew rings, 2, 3, 4, or 6 radial straps are placed symmetrically around the circumference.
محدوده کویل و تسمه
| پارامتر مهندسی | Hot-Rolled Heavy Project Benchmark | General Production Range |
|---|---|---|
| عرض سیم پیچ | 450-620 میلی متر | 300-2,000 میلی متر |
| قطر خارجی/شناسه کویل | ۵–۱۰ میلیمتر / ۱۵۰ میلیمتر | OD 800–2,200 mm / ID 508–762 mm |
| کویل وزن | حداکثر ۲.۵ تن | تا ۴۰ تن |
| دمای سطح | Below 800 °C (heat-shielded head) | محیط تا 800 درجه سانتیگراد |
| Steel Strap Gauge | 32 mm width, 0.8–1.0 mm thickness | 19 mm, 25 mm, 32 mm width |
| Applied Strap Tension | 2,000–20,000 N (PLC adjustable) | 2,000–20,000 N continuously variable |
| Take-Up Speed | ~105 میلیمتر بر ثانیه | Variable speed take-up |
| Pneumatic / Hydraulic Utility | 5–7 bar, clean, dry, lubricated air | 5–7 bar compressed air / hydraulic assist |
| PLC System Interface | Siemens S7 / Industrial Ethernet | Profinet, Ethernet/IP, Profibus DP |
Specific coil envelopes, takt times, and binding counts are validated during project layout engineering.
اندازه و کشش تسمه
The sealed joint efficiency, not raw strap tensile strength, dictates safe working tension.
Consider a standard 32 × 0.9 mm high-tensile steel strapping band:
- مقطع اسمی:
32 mm × 0.9 mm = 28.8 mm² - Raw Breaking Load: At a tensile strength of 950 N/mm², breaking force reaches:
F_break = 28.8 mm² × 950 N/mm² = 27,360 N - Seal Joint Limit: A double-notch crimp or buckle joint delivers roughly 75%–80% joint efficiency:
F_joint = 27,360 N × 0.75 = 20,520 N
While the servo/hydraulic tensioning head can pull up to 20,000 N, operating at machine peak will stress the joint close to failure and risk edge damage on thin-gauge strip.
- Working Setting: Maintain working tension within 40%–60% of joint yield strength (typically 8,000–12,000 N) to provide an adequate safety buffer against dynamic shock during transit.
- حفاظت لبه: On soft-grade or thin-gauge strip, programmed tension is derated, and automated cardboard edge corner protectors are placed under the strap path to prevent edge buckling.
طول تسمه در هر کویل
To calculate raw steel strap consumption per radial binding:
Radial Strap Length ≈ 2 × Coil Width + (OD - ID) + Overlap & Seal AllowanceCalculation Example (620 mm width, 1,400 mm OD, 550 mm ID):
- Perimeter Loop:
(2 × 620 mm) + (1,400 mm - 550 mm) = 1,240 mm + 850 mm = 2,090 mm - Joint & Cut Allowance:
+ 150 mm - Total Strap per Tie:
2,240 mm (2.24 m)
For a 4-strap pattern on a 60-coil-per-shift line:
Total Shift Consumption = 2.24 m × 4 straps × 60 coils = 537.6 m
This calculated length dictates required strap dispenser jumbo coil stock and shift changeover frequency.
جایی که بسته بندی مناسب است
| پارامتر تولید | Hot-Rolled Coils (Mill Exit) | Cold-Rolled, Coated & Slit Coils |
|---|---|---|
| پیکربندی تسمه | Radial (through eye) for burst restraint | Radial + circumferential for package integrity |
| بسته بندی محافظ | Unwrapped or post-cooling perimeter hood | Orbital eye-through stretch film / VCI wrap |
| Edge Guard Application | Heavy-duty corner clips if required | Inner/outer cardboard angles & edge donuts |
| ریسک خرابی اولیه | Elastic spring-back burst & lap telescoping | Moisture intrusion, oxidation rust & cosmetic scratching |
For finished products, an automated eye-through steel coil wrapping machine positions directly in-line downstream of the cooling yard. See چگونه کویلهای فولادی با کاغذ و فیلم کششی بستهبندی میشوند for integrated line synchronization. Required cooling buffers prior to wrapping depend on coil tonnage and ambient yard ventilation.
بهترین شیوه
- مدیریت دستور غذا: Archive coil width, OD, ID, and tension profiles directly in the PLC recipe manager to enable single-touch changeover and automatic track-stroke matching.
- Guide Track Maintenance: Purge the strap track and tensioning jaws daily; hot-mill oxide scale and steel slivers create misfeeds and jaw slippage if uncleaned.
- Shift Joint Inspection: Verify notch crimp depth and joint pull resistance on a test loop at the start of each production shift.
- Pneumatic Conditioning: Ensure clean, dried compressed air at 5–7 bar; drain coalescing water filters at regular intervals to prevent cylinder stick-slip.
چک لیست انتخاب
- Coil physical dimensions: minimum/maximum Width, OD, ID, and weight?
- Strip surface temperature at the strapping station (ambient, <400 °C, or up to 800 °C)?
- Strapping scheme: radial-only, circumferential-only, or combined cross-strapping?
- Target strap count per coil (e.g., 2, 3, 4, or 6 radial straps)?
- Strap specification preferred (19 mm, 25 mm, or 32 mm high-tensile steel)?
- Required line cycle time (takt time in seconds per coil)?
- Upstream/downstream handling interface (coil car, walking beam, slat conveyor, C-hook crane)?
ایمنی
The machine design and cell integration comply strictly with international safety directives:
- EN ISO 12100:2010: Risk assessment and risk reduction for industrial plant equipment.
- EN 415-10: Specific safety standards for modular strapping machines and packaging cells.
- EN 60204-1: Electrical safety, grounding, and control circuit reliability.
The primary operational hazards involve high-speed track closure, pinch points at the tensioning jaws, and burn hazards from radiant hot coils. The complete strapping zone is isolated by perimeter safety fencing with dual-channel category-4 interlocked service gates, light curtains at conveyor entry/exit, and emergency stop circuits integrated with upstream mill controls.
سوالات متداول مهندسی
Q: Can this radial strapping machine handle red-hot coils direct from the coiler? A: Yes. For hot-mill projects up to 800 °C, the machine integrates water-cooled heat shields, radiant thermal insulation, high-temperature pneumatic seals, and specialized strap track guides.
Q: How many radial straps can be applied in a single cycle? A: Dual-head machines apply two straps at once. When paired with an integrated 360° slew indexing base, the head automatically indexes to apply 2, 3, 4, or 6 radial straps per package sequence.
Q: What strap materials and dimensions are supported? A: High-tensile steel strap from 19 mm to 32 mm in width (0.8 mm to 1.0 mm thickness), using notched seal joints or crimped buckle closures depending on strap tension specifications.
Q: How does the station interface with existing mill automation? A: The onboard Siemens or Allen-Bradley PLC exchanges handshakes via Profinet, Industrial Ethernet, or discrete hardwired I/O for coil positioning, interlock clearing, and recipe handshakes.
مرحله بعدی
- Submit Engineering Data: Send your coil dimensional envelope, temperatures, shift tonnage, and cycle time targets to info@fhopepack.com.
- اندازه سیستم: Our engineering team confirms strap cross-section, head configuration (single vs. dual), gantry layout, and downstream wrapping integration.
- Formal Proposal: Receive an engineering proposal including 2D/3D footprint drawings and a commercial quotation within 24 to 48 hours.
خواندن مرتبط
- دستگاه تسمهکشی کلاف فولادی شعاعی (محصول)
- دستگاه تسمهکشی کویل فولادی محیطی (محصول)
- دستگاه بسته بندی کویل فولادی (محصول)
- دستگاه تسمه شعاعی کویل فولادی
- خط بسته بندی کویل اتوماتیک (محصول)
منابع
- FHOPE Radial and Circumference Coil Strapping Machine Technical Specifications (2025)
- Industrial Engineering Standards: EN ISO 12100:2010, EN 415-10, EN 60204-1
- Packaging Machinery Operations Field Benchmark: Hot-Rolled Strip Coiling & Strapping Plants
آخرین بهروزرسانی: 2026-10-29