> **Kokkuvõte**
> La maquina de línea automática de envasado de bobinas is our automatic coil packing line with a coil stacking system, for strip coils coming off a slitting line. A turnstile with 2 or 4 arms takes up to 60 t of coils, a down ender lays each coil onto the conveyor, an eye-through wrapper wraps it and a gantry stacker sets it on the pallet. A worked example checks the turnstile load, the packing pace and the pallet stack.
Sisukord
- Why pack slit coils in one line
- Turnstile: the buffer after the slitter
- Down ender: from eye horizontal to the conveyor
- Läbipaistev ümbris
- Portaalvirnastaja
- Controls and safety parts
- Worked example: slit set, pace and pallet
- Valiku kontroll-leht: mida meile saata
- Ohutus ja EN 415-10
- Inseneri KKK
- Järgmine samm
- Seotud lugemine
- Allikad
Why pack slit coils in one line
A slitter turns one master coil into a set of narrow coils at once. If they are then turned, wrapped and stacked by crane one by one, packing becomes the slowest part of the shop. Every crane lift is also a chance to damage an edge.
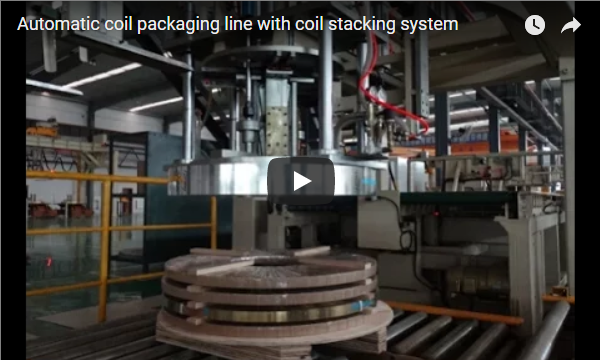
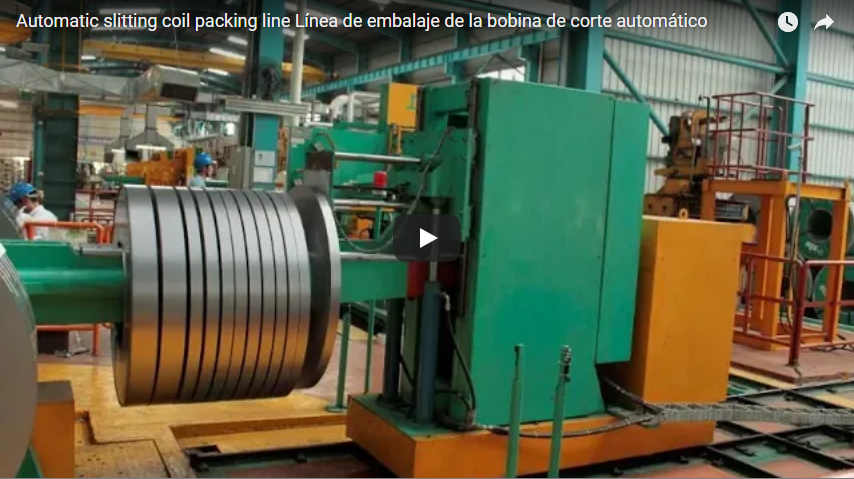
Our line takes the whole set from the slitter and passes each coil from station to station automatically. Our demonstration line shows the sequence: the coil is turned on a rotating stand, wrapped in white film on a yellow roller line, carried down a long roller conveyor and stacked by a yellow-armed stacker. Yellow railings fence the machines.
Turnstile: the buffer after the slitter
The turnstile is a heavy rotating stand with 2 or 4 arms. The slit set is pushed onto one arm while the coils on another arm are being packed. That decouples the slitter from the packing pace.
We choose 2 or 4 arms to suit the slitting line speed. Each turnstile takes up to 60 t, with arms up to 2,000 mm long.
Down ender: from eye horizontal to the conveyor
The down ender picks one coil at a time off the turnstile arm, separating it from its neighbours. A hydraulic lifting nose adjusts to different coil widths. It then lays the coil on its roller conveyor table, with a falling-protection device holding the coil during the turn.
Läbipaistev ümbris
The wrapper has its own conveyor table, so it connects straight into the line. The ring passes the film through the coil eye while rollers turn the coil. Ring speed and roller speed each run on an inverter, and the wrapping material tension is adjustable. So overlap and tightness can be set for each coil size.
Portaalvirnastaja
The stacker is a gantry-type mechanical coil lifter. It picks each wrapped coil off the conveyor and sets it on the pallet, one by one. Our stacking system builds stacks up to 1,000 mm high including the pallet, with up to 3,000 kg per coil and 6,000 kg per stack.
| Station | Key data |
| :— | :— |
| Turnstile | 2 or 4 arms, up to 60 t, arms up to 2,000 mm |
| Down ender | hydraulic lifting nose, falling protection, roller conveyor table |
| Wrapper | eye-through, ring and roller speed on inverters, adjustable material tension |
| Stacker | gantry type, stack up to 1,000 mm with pallet |
| Stack load | up to 3,000 kg per coil, 6,000 kg per stack |
| HMI | 10 or 12 inch touch screen |
Controls and safety parts
One PLC runs the whole line, with a 10 or 12 inch HMI for parameters, recipes, status and alarms. Inverters control the conveyor, turnstile, ring, roller and stacker speeds. Sensors confirm coil position and machine interlocks at each station.
The safety system uses safety relays or an optional safety PLC for the emergency stops and guard switches. Light curtains or area scanners are optional, typically round the stacker and turnstile. Emergency stop buttons sit along the whole line.
Worked example: slit set, pace and pallet
A service centre slits a master coil of 1,500 mm OD, 508 mm ID and 1,250 mm width into 10 strips of 120 mm, with 50 mm of trim. One master coil takes 15 minutes to slit. These are illustrative customer figures.
**Turnstile load.** The master coil’s cross-section is π ÷ 4 × (1.5² − 0.508²) = 1.564 m². Times 1.25 m and 7,850 kg/m³, the slit set weighs 1.564 × 1.25 × 7,850 = 15,350 kg, or 15.4 t. That is far below 60 t, and 1,250 mm sits on a 2,000 mm arm.
**One slit coil.** Each 120 mm strip weighs 1.564 × 0.12 × 7,850 = 1,473 kg.
**Packing pace.** Ten coils every 15 minutes means one coil every 900 ÷ 10 = 90 s. So down-ending, wrapping, transfer and stacking must each finish within 90 s per coil. Otherwise the turnstile fills up and the slitter waits. Our slit coil system’s down-ending cycle of 60 s fits inside that budget; time the other stations the same way.
**Pallet stack.** At 1,473 kg, four coils weigh 5,892 kg, inside the 6,000 kg stack limit. They stand 4 × 120 = 480 mm high, well under 1,000 mm with the pallet. So each slit set fills two pallets of four and one of two.
**General rule.** The slowest station sets the line. Its time per coil must be at most T_slit ÷ n, where T_slit is the slitting time for one master coil and n the number of strips.
Valiku kontroll-leht: mida meile saata
1. Master coil OD, ID, width and weight.
2. Number and width of strips.
3. Slitting time per master coil.
4. Wrapping material: film, paper or both.
5. Pallet size and stack limits.
6. Floor space and how pallets leave the line.
Ohutus ja EN 415-10
For CE markets we follow EN 415-10 as the reference, with a risk assessment to ISO 12100. The main hazards are the turning turnstile, the down ender, the wrapping ring and the moving stacker.
Fence the line, as on our demonstration line, and interlock the access gates to the perimeter fence. Keep the stacker and turnstile zones clear while they move, and add light curtains or area scanners where people need open access.
Inseneri KKK
Q: Two arms or four on the turnstile?
A: It depends on your slitting line speed. More arms give more buffer between slitting and packing.
Q: Can the line handle different coil widths?
A: Yes. The down ender’s hydraulic lifting nose adjusts to different widths, and the wrapper settings change per coil.
Q: Can we choose the PLC brand?
A: Yes. We build with Siemens, Rockwell, Mitsubishi or Omron PLCs.
Q: Which standards do you build to?
A: EN 415-10 as our CE reference, with an ISO 12100 risk assessment.
Järgmine samm
1. **Email your master coil size, strip layout and slitting time** to **info@fhopepack.com**.
2. **We reply within 24 hours with a proposal**, with the turnstile, wrapper and stacker.
3. **We send a layout drawing** for the exit of your slitting line.
Seotud lugemine
– [Automatic steel coil packing system with strapping and stacking](https://www.fhopepack.com/Steel-coil-wrapping-machine/Automatic-coil-packaging-line.html)
– [Coil packing line with tilter and stacking function](https://www.fhopepack.com/videos/coil-packing-line-with-tilter-and-stacking-function/)
– [What is the best packing material combination for steel coil packing?](https://www.fhopepack.com/videos/what-is-the-best-packing-material-bombination-for-the-steel-coil-packing/)
– [What kind of stretch film fits coil packing](https://www.fhopepack.com/videos/what-kind-of-stretch-film-fit-for-coil-packing/)
– [Automated slit coil packing line for service centers](https://www.fhopepack.com/videos/automated-slit-coil-packing-line-for-service-center-boost-your-productivity/)
Allikad
– Specifications: FHOPE automatic steel coil packing system and automatic slit coil packaging system product pages
– Machine video: [coil packing line with stacking on YouTube](https://www.youtube.com/watch?v=MEVAMtNxh34)
– Slit set, pace and pallet: our worked example, illustrative coil figures
– Standards: EN 415-10 (packaging machines, general safety); ISO 12100:2010
Viimati üle vaadatud: 2026-10-17