Kokkuvõte
An automatic steel wire coil strapping and rewinding machine takes wire from a large coil or reel, rewinds it into smaller coils of a set length, cuts it and ties each coil. Ours winds on a servo-driven, expanding coiling head, counts length to the centimetre, and straps 2–4 places through the coil eye with 8–10 mm PP strap. Our coiling and strapping versions are matched to line speeds of up to 45 coils per hour. A worked example builds the time budget for that rate.
Sisukord
- Why wire is rewound into smaller coils
- The rewinding line
- Masinamoodulid
- Pakkimisandmed
- Worked example: a 45 coil/h time budget
- Valiku kontroll-leht
- Ohutus: EN 415-10 ja ISO 12100
- Inseneri KKK
- Järgmine samm
- Seotud lugemine
- Allikad
Why wire is rewound into smaller coils
Wire drawing and galvanizing lines make large coils or fill big reels. Many buyers want smaller coils of an exact length that one person can handle and that sell by the metre. Rewinding by hand is slow, the length is guessed and the coil shape is loose.
A rewinding and strapping machine does all of it in one cycle. It measures the length, winds a regular coil, cuts the wire and ties the coil, so every coil leaves the same.
The rewinding line
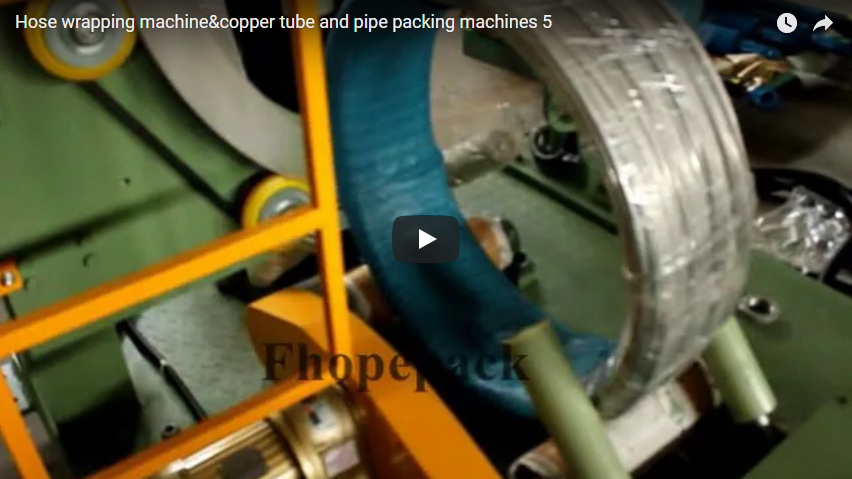
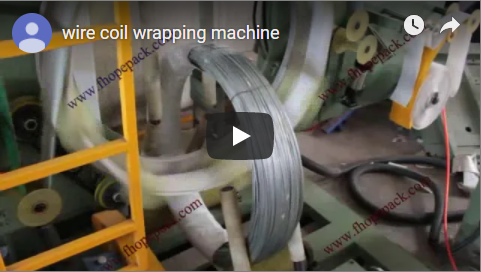
Wire comes off the supply coil at the back of the line and runs forward through the guide and length counter. At the front, it winds onto a large segmented coiling head that turns on a horizontal axis; the head opens and closes automatically to wind and then release the coil. Next to it, a second, smaller head works on the following coil. The strapping unit sits above the coil at the transfer point.
Masinamoodulid
- Meter counter. Measures the wire length, accurate to the centimetre, and signals the cutter and coiling head. The upper wheel is aluminium alloy with a hardened ceramic coating; the lower wheel has a rubber cover to protect the wire. A one-way bearing stops the wire running back.
- Coiling head. Moves up and down to take off the coil and fix the wire end at the start. It opens and closes automatically, and a servo drive keeps the coil shape regular.
- Omanik. A servo-driven holder clamps the finished coil and moves it to the strapping station.
- Lõikur. Cuts the wire when the set length is reached. The blade is special alloy steel, vacuum heat-treated for hardness.
- Kontroll. PLC, servo and touch screen. Winding speed, coil length, alarms and reset are handled on the screen. Coil length and wire diameter settings can be changed while the line runs; the new values take effect on the next coil, not mid-wind.
- Rihmade kinnitamine. Eye-through strapping at 2–4 places, positioned by program, with adjustable tension and automatic strap feed. A strap dispenser with an accumulator feeds the head, and moving wheels signal the feed speed.
Pakkimisandmed
| Kirje | Väärtus |
|---|---|
| Rihm | PP, 8–10 mm wide, 0.8 mm thick |
| Ühine | friction (vibration) weld |
| Ühine seisukoht | front of the wire coil |
| Liigese efektiivsus | approx. 75–80% of the strap breaking load |
| Rihmade kohad | 2–4, through the coil eye |
| Rihmade varustus | pay-off with accumulator; moving wheels signal feed speed |
Worked example: a 45 coil/h time budget
Illustrative coil: 1,000 m of 5 mm steel wire, wound to 600 mm OD, 400 mm ID and 200 mm width, tied in 4 places.
| Samm | Arvutus | Tulemus |
|---|---|---|
| Time per coil at 45 coils/h | 3,600 ÷ 45 | 80 s |
| Coil mass | 7,850 × π/4 × 0.005² × 1,000 | ≈ 154 kg |
| Strap per tie, around the section | 2 × (200 + 100) mm | 0.6 m |
| Strap per coil, 4 ties | 4 × 0.6 m | 2.4 m plus joints |
| Joint holding force | 0.75–0.80 × strap breaking load F_b | 75–80% of F_b |
| Winding time | t_w = L ÷ v_wind | from your line speed |
| Time left for transfer and strapping | 80 − t_w | must cover all 4 ties |
Tulemus. At 45 coils per hour each coil has 80 s. With one coiling head, winding (L ÷ v) plus transfer plus four ties must all fit in 80 s. With two heads working in turn, one coil winds while the other is transferred and strapped, so each task only has to fit inside 80 s on its own. The tie cycle and index time are measured on your coil at the factory acceptance test. The strap is sized on the joint, not the strap alone: a joint holds about 75–80% of the strap’s breaking load.
Valiku kontroll-leht
Before we quote, we ask which reel or supply coil feeds the line and for the coil data:
- Wire diameter and grade; coated or bare.
- Supply: reel type or coil, and its weight.
- Finished coil: length or weight, OD, ID, width.
- Coils per hour and line speed.
- Ties per coil: 2, 3 or 4.
- Next step: film wrap, compacting, stacking.
Ohutus: EN 415-10 ja ISO 12100
We design the machine to EN 415-10 and assess its risks to ISO 12100. The hazards are the turning coiling head, the moving wire, the cutter and the strapping head. The wire path and the coiling head are guarded. Emergency stops are hardwired mushroom-head pushbuttons on the control stations, to EN ISO 13850; the touch screen shows status and handles reset only. Guarding scope and CE paperwork are fixed in the contract for each line.
Inseneri KKK
Q: How accurate is the coil length? A: The counter measures to the centimetre and signals the cutter at the set length.
Q: Can the coil size be changed while the line runs? A: The settings can be changed on the screen while running; they apply from the next coil.
Q: Does the number of ties affect output? A: Yes. Each extra tie adds one index and one tie cycle, so 4 ties take longer than 2. Where output is tight, we use 2 or 3 ties or a second coiling head.
Q: How many straps per coil? A: 2–4 places, set by program; the tension is adjusted for each coil size.
K: Milline standard kehtib? V: Masina puhul on tegemist standardiga EN 415-10 ja riskihindamise puhul standardiga ISO 12100.
Järgmine samm
- Send wire size, supply reel and finished coil data aadressile info@fhopepack.com.
- Me valime a horizontal or vertical coiling and strapping version.
- Vastame 24 tunni jooksul küljenduse ja tsitaadiga.
Seotud lugemine
- Automatic steel wire coiling and strapping machine (product)
- Full automatic steel wire rope coiler for winding and strapping
- Automatic steel wire coiler for winding and strapping
- Steel wire coil rewinding and automatic packing
- Automatic steel wire coil packing machine (product)
Allikad
- FHOPE product page: automatic steel wire coiling and strapping machine
- FHOPE project notes on coiling and strapping versions and line speed
- Our wire rewinding and strapping line shown above
- Worked example: illustrative figures; steel density 7,850 kg/m³
- Standardid: EN 415-10; ISO 12100:2010
Viimati üle vaadatud: 2026-10-18