Ülevaade
Coil packaging ties three decisions together: how much labor each wrap needs, how consistently the film holds the load, and whether the wrapping step keeps pace with the coiler that feeds it. FHOPE supplies both manual stations and automated coil lines, and the right choice depends on your volumes and coil sizes. This guide covers how each option operates, what an automated line does to a coil, and what to specify, and is written for coil mill engineers and coil-line buyers.
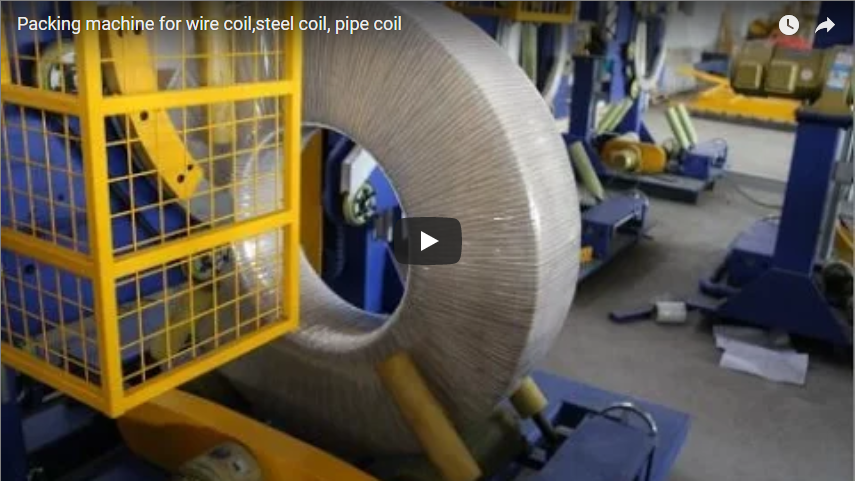
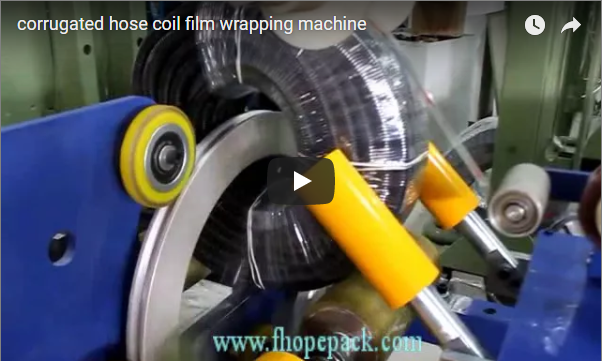
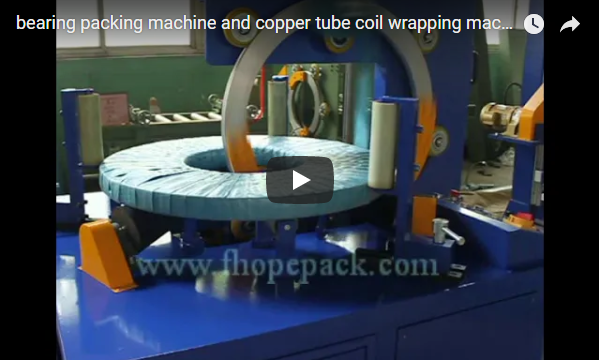
The video below shows the automated line wrapping a coil on the conveyor and moving it through to strapping:
Manual Station vs Automated Line
| Aspekt | Manual station | Automatiseeritud liin |
|---|---|---|
| Tööjõud mähise kohta | Operators position, apply film and strap by hand; most minutes per coil | Operator supervises; the machine wraps and straps |
| Film consistency | Hand-applied tension varies from wrap to wrap | Ring applies pre-stretch film at controlled overlap, coil to coil |
| Pace with the coiler | The station waits on hand labor | Cycle is set to the upstream coiling rate |
| Investment and footprint | Low entry, simple services | Higher entry; needs floor space and a control panel |
A manual station works at low volume and low variety. The trade is consistency: hand-applied tension varies, and it takes the most minutes per coil at the point where the line is waiting on it.
How the Automated Line Wraps and Straps
| Samm | Mis juhtub |
|---|---|
| Sissetoomine | The coil enters on a heavy-duty roller or chain conveyor sized to the coil width, with the bed surface (for example rubber-coated rollers) selected for surface protection per project. |
| positsioneerimine | A sensing station picks up coil position; centering arms square the inner-diameter axis with the wrapping ring center. |
| Ring wrap | The coil stays still while the film ring orbits it; pre-stretch rollers draw the film before it is applied. |
| kopsakas | The banding unit applies tensioned steel or PET bands at set positions. |
| Edge and closing | An automatic sealer or shrink edge completes the cover where the spec calls for it. |
| Väljavool | The wrapped coil advances to storage or shipping. |
Positioning is what automated wrapping does first: an off-center wrap shifts in transit no matter how fast it was made, and nothing after positioning can fix a drifted start. The result is a cover with even compression and consistent overlap from coil to coil.
Mida täpsustada
| Sisend | Miks see on oluline |
|---|---|
| Coil OD/ID, width and weight | Sets the conveyor and ring envelope |
| Coils per day and line rate | Manual station vs automated line |
| Ühistranspordi režiim | Film and strapping needed per load |
| Upstream coiling rate | Line output matching the coiler |
| Floor space and services | Layout and available air and power |
| Elektrivarustus | Voltage, phase and frequency on site |
The whole selection is set per project from your coil sizes and the line rate you need.
Tehase testimine ja vastuvõtmine
- Täistsükli tõendid. Ask for a test log of complete wrap and strap cycles on a representative coil.
- Pikendatud jooks. The vendor’s stated practice on this machine family includes near-continuous pre-delivery testing (up to about 24 hours where stated).
- Kontroll ja ohutus. Confirm smooth, responsive control and a verified emergency stop; interlocks keep operators clear of conveyors and the strap head, and the ring is enclosed where the cycle is automatic.
- Load stability. Evidence that the wrapped coil holds under strap tension during testing.
- Kasutuselevõtt. Kirjalik paigaldus-, kasutuselevõtu- ja kohapealse teenuse ulatus.
- Wire Coil Packing Machine with Wrapping Station Movement – Coil wrapping station mechanics in the same family.
- Terasest spiraalkallur kohandatud teenusega – Coil tilting and handling around the line.
- Mähise ümberpööramise ja tööstusliku ümberpööramise lahendused – Coil and pallet handlers used with wrapping lines.
On arrival repeat: empty cycle, loaded cycle, emergency stop.
KKK
Q: Manual station or automated line?
A: Low volumes suit a manual or semi-automatic station; as coils per day climb, an automated line pays on consistency and output. The choice is sized from your volumes per project.
Q: Why is coil centering the first thing that matters?
A: An off-center wrap shifts in transit and costs repositioning time; alignment before wrapping is the difference between a stable load and a reworked one.
Q: What film and strap does it use?
A: Stretch film with pre-stretch control, and steel or PET strapping tensioned to the load. Confirmed per project.
Q: Can the line keep pace with the coiler?
A: Yes — output is set to match the upstream coiling rate, so wrapping does not become the bottleneck.
K: Millised standardid kehtivad?
A: The machine family is designed with EN 415-10 as the packaging-machinery safety reference and an ISO 12100 risk assessment for the ring and banding stations.
Järgmine samm
Send coil OD/ID/width/weight, coils per day, transit mode and upstream coiling rate, for a station-versus-line comparison and a layout drawing.