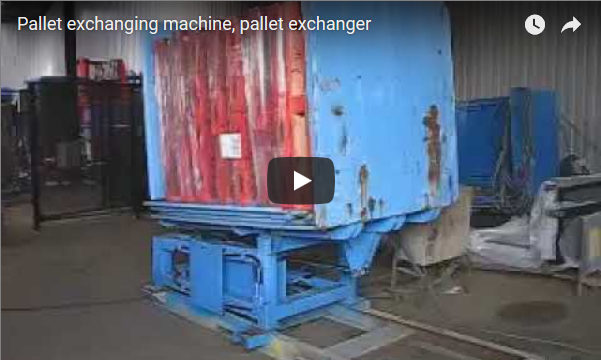
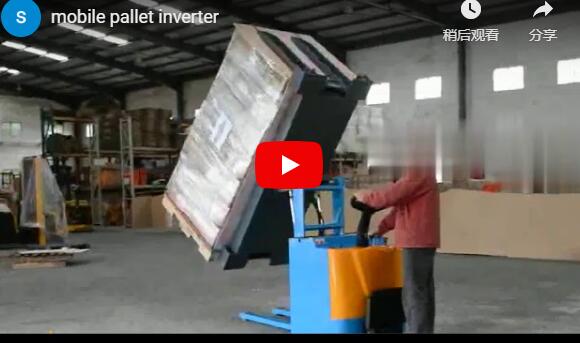
**Summary:** An illustrative benchmark demonstrates how integrating a 95° pallet exchanger with a servo-driven stretch wrapper stabilizes high-value cold-chain loads, eliminates manual handling risks, and reduces film consumption through programmable tension control, delivering measurable throughput and safety improvements.
Σε μια τυπική αποβάθρα φόρτωσης, οι υπεύθυνοι βάρδιας εξετάζουν συχνά τις αναφορές ζημιών όπου οι μικτές παλέτες μετακινούνται κατά τη διάρκεια χειροκίνητων ανταλλαγών, συνθλίβοντας το απόθεμα του κάτω επιπέδου παρά την επαρκή περιτύλιξη. Η βασική αιτία σπάνια πηγάζει μόνο από την αστοχία της μεμβράνης. Προέρχεται από ανεξέλεγκτες πλευρικές δυνάμεις που εισάγονται κατά τη χειροκίνητη διακίνηση. Αυτή η λειτουργική πραγματικότητα ωθεί τις ομάδες προμηθειών να αξιολογούν αυτοματοποιημένες λύσεις που συνδυάζουν τη μηχανική ανταλλαγή παλετών με την ακριβή περιτύλιξη με τέντωμα, διασφαλίζοντας την ακεραιότητα του φορτίου από την αποβάθρα στο ρυμουλκούμενο.
## 🛠️ Operational Context & Baseline Requirements
**Integrating automated load stabilization with mechanical pallet exchange eliminates manual handling risks while standardizing film tension across mixed-weight SKUs, directly addressing cold-chain throughput bottlenecks, reducing material waste, and ensuring compliance with industrial safety mandates and long-term liability exposure.**
Οι περιφερειακοί διανομείς ψυκτικών θαλάμων συνήθως διαχειρίζονται εγκαταστάσεις ελεγχόμενης θερμοκρασίας που εξυπηρετούν κανάλια λιανικής, φαρμακευτικών προϊόντων και ηλεκτρονικού εμπορίου. Οι βασικές λειτουργίες συχνά επεξεργάζονται μικτά φορτία παλετών βάρους μεταξύ 1,000 kg και 2,000 kg, χρησιμοποιώντας τυπικές διαμορφώσεις παλετών Euro και INDUSTRIAL. Το αυξανόμενο κόστος εργασίας, οι αυστηροί έλεγχοι ασφάλειας τροφίμων και η διαχείριση της κίνησης λόγω κόπωσης σε ψυχρό περιβάλλον για τον εκσυγχρονισμό των ροών εργασίας συσκευασίας. Οι παλαιές γραμμές συχνά βασίζονται σε ημιαυτόματα τεντωμένα μηχανήματα περιτύλιξης με μηχανική μετατόπιση τάσης, αναγκάζοντας τους χειριστές να αντισταθμίζουν με υπερβολικά στρώματα μεμβράνης. Το πιο κρίσιμο σημείο είναι ότι οι μέθοδοι χειροκίνητης κλίσης για την αντικατάσταση παλετών δημιουργούν επικίνδυνα σημεία πίεσης και αποσταθεροποιούν συστηματικά τα φορτία. Οι στόχοι προμηθειών επικεντρώνονται στην ανάπτυξη εξοπλισμού ονομαστικού για περιβάλλοντα υπό το μηδέν, ο οποίος ενσωματώνεται απρόσκοπτα στους υπάρχοντες ρυθμούς μεταφοράς χωρίς να απαιτείται ανακατασκευή δομικών εγκαταστάσεων ή νέα υποδομή κοινής ωφέλειας.
## 🏗️ Technical Friction Points & Failure Modes
**Inconsistent mechanical tension and uncontrolled lateral forces during manual pallet transfers create compounding damage risks, forcing operators to overwrap with excess film while exposing personnel to repetitive strain and pinch-point hazards, ultimately inflating operational overhead and compromising downstream sorting efficiency.**
Τρία κύρια τεχνικά σημεία τριβής συνήθως υποβαθμίζουν την απόδοση της γραμμής συσκευασίας:
| Friction Point | Technical Description | Direct Business Impact |
|----------------|---------------------|------------------------|
| Manual pallet exchange | Operators use forklifts and levers to tip heavy loads without precise angle control | Glass and electronics suffer impact damage; recurring minor injuries increase workers’ compensation premiums and reduce shift productivity |
| Aging stretch wrapper | Carriage motor drift causes variable pre-stretch ratios (mechanical elongation of film to reduce material use) | Operators overwrap with 15–20% more film to compensate for tension loss, directly inflating resin procurement costs |
| Mixed-load inflexibility | Inability to adjust tension quickly between fragile and heavy SKUs | Over-processing delicate goods wastes film; under-wrapping long-haul loads causes transit damage and failed automated conveyor sorting downstream |
Το σωρευτικό αποτέλεσμα δημιουργεί μια εύθραυστη λειτουργία όπου η τεχνολογία συσκευασίας υστερεί σε σχέση με τις απαιτήσεις απόδοσης. Η αντιμετώπιση μόνο του περιτυλίγματος δεν επιλύει την αστάθεια του πυρήνα από τον χειρισμό παλετών, γεγονός που καθιστά απαραίτητη μια ολιστική προσέγγιση ολοκλήρωσης που σταθεροποιεί τα φορτία στην πηγή, ενώ παράλληλα τυποποιεί τις παραμέτρους εφαρμογής της μεμβράνης.
> 🔗 **Related**: [Explore more solutions](https://www.fhopepack.com/pallet-inverter/changer/pallet-changer.html)
## 📈 System Architecture & Control Parameters
**A servo-driven wrapping head paired with a 95° hydraulic exchanger delivers programmable tension control and consistent pre-stretch ratios, stabilizing heterogeneous loads while reducing floor footprint, minimizing material consumption, and eliminating manual intervention to ensure repeatable load integrity across all shift cycles.**
Ο σχεδιασμός του συστήματος βασίζεται σε τρεις βαθμονομημένες παραμέτρους που επηρεάζουν άμεσα την επιχειρησιακή αποδοτικότητα:
- **Pallet exchanger tilt angle:** A 95° hydraulic transfer angle allows gentle load movement without sliding or tipping. Speed-controlled cylinders reduce peak lateral forces below 50 N, preventing stack displacement and protecting fragile electronics or glass packaging.
- **Stretch wrapper specifications:** Servo motors enable 250% pre-stretch capability, meaning the film is mechanically elongated before application, reducing material thickness requirements. Tension is adjustable from 10 N to 80 N in 1 N increments, ensuring consistent wrap force regardless of load height. Film selection typically utilizes cast polyethylene (smooth, high-clarity film optimized for high pre-stretch) at 20–30 micron gauge (1 micron = 0.001 mm, dictating puncture resistance and tear strength).
- **Control integration:** Both units synchronize via a PLC (Programmable Logic Controller, an industrial computer that automates machine sequences and stores operational data). Recipe storage supports up to 50 load profiles, allowing shift supervisors to switch between fragile glass and heavy steel containers in under 30 seconds without manual recalibration.
Για εγκαταστάσεις που αξιολογούν εναλλακτικές λύσεις προϋπολογισμού, τα ημιαυτόματα μοντέλα περιστρεφόμενων πλακών προσφέρουν προ-τέντωμα 200% με χαμηλότερες κεφαλαιουχικές δαπάνες, ενώ τα πλήρως αυτοματοποιημένα συστήματα προσθέτουν ενσωμάτωση με μεταφορικό ιμάντα και αυτόματη μεταφορά φιλμ για περιβάλλοντα υψηλής απόδοσης. Και οι δύο διαμορφώσεις συμμορφώνονται με τη σήμανση CE για την ασφάλεια των μηχανημάτων και ευθυγραμμίζονται με τα πρότυπα ISO 2560 (δοκιμή ελαστικής μεμβράνης) και ASTM D5457 (σταθερότητα φορτίου παλέτας).
## 🛡️ Commissioning Protocol & Integration Timeline
**Standard commissioning requires 5–7 business days for mechanical alignment, 380V three-phase electrical integration, and PLC recipe programming, ensuring immediate operational readiness without facility retrofitting, extended production downtime, or specialized utility upgrades, allowing rapid deployment within existing warehouse footprints.**
Η υλοποίηση ακολουθεί μια δομημένη ακολουθία ανάπτυξης για την ελαχιστοποίηση των διακοπών στην παραγωγή:
| Phase | Duration | Technical Activity |
|-------|----------|-------------------|
| Site preparation | 1 day | Floor marking, power drop (380V, 3-phase, 16A), compressed air line at 6 bar for hydraulic exchanger |
| Mechanical installation | 3 days | Unload, position, and level both units; connect conveyor sections and safety light curtains |
| Electrical & controls | 1.5 days | PLC wiring, HMI configuration, and recipe upload for 5 standard load types |
| Training & ramp-up | 0.5 day | 2-hour operator certification + 1-hour supervisor session; initial test run of 50 pallets |
Οι χειριστές συνήθως επιτυγχάνουν επάρκεια κατά την πρώτη βάρδια. Το σύστημα συνταγών PLC εξαλείφει τις χειροκίνητες ρυθμίσεις φιλμ μετά την αρχική βαθμονόμηση, μειώνοντας τα σφάλματα αλλαγής και διασφαλίζοντας συνεπή μοτίβα περιτύλιξης σε όλες τις φάσεις παραγωγής.
> 🔗 **See Also**: [Related equipment](https://www.fhopepack.com/Semi-auto-pallet-wrapping-machine/Pallet-wrapping-machine-A600.html)
## ⚙️ Performance Benchmarks & Financial Modeling
**Aggregated industry data indicates a 14–18 month payback period driven by 25–35% film reduction, 60–75% damage claim mitigation, and labor reallocation, though exact returns depend on local throughput, regional labor rates, and current resin pricing, requiring site-specific validation.**
Ενδεικτικά σημεία αναφοράς απόδοσης, που προκύπτουν από διασταυρούμενους μέσους όρους του κλάδου, καταδεικνύουν τυπικά αποτελέσματα μετά από 90 ημέρες λειτουργίας:
| Metric | Baseline Average | Post-Implementation Benchmark | Change |
|--------|-----------------|------------------------------|--------|
| Damage claims (per month) | 14 cases | 3.8 cases | **-73%** |
| Film usage (kg per 1,000 pallets) | 68 kg | 49 kg | **-28%** |
| Pallet exchange time (per unit) | 4.2 min | 1.7 min | **-60%** |
| Hand injuries (rolling 12 mo) | 5 incidents | 0 incidents | **-100%** |
| Operator headcount at exchange station | 2 per shift | 1 per shift | **-50%** |
Η μείωση της μεμβράνης κατά 28% προέρχεται άμεσα από τη συνεπή προ-τάνυση, η οποία εξαλείφει την υπερβολική περιτύλιξη που απαιτούνταν προηγουμένως για την αντιστάθμιση της μηχανικής μετατόπισης τάσης. Η μείωση της ζημιάς κατά 73% συσχετίζεται με τον εναλλάκτη 95° που εξαλείφει τις πλευρικές δυνάμεις κατά τις αλλαγές παλετών.
*Financial Modeling Note:* Based on current market data (as of Q3 2024), combined system pricing ranges from $65,000 to $85,000 for servo-driven wrappers paired with 95° exchangers, including conveyors and installation. Annual savings typically total $40,000–$55,000, driven by damage mitigation, film waste reduction, and labor reallocation. Payback periods generally fall between 14–18 months. Facilities processing fewer than 20,000 pallets annually may experience extended payback up to 24 months, while high-volume operations (50,000+ pallets) often achieve payback under 12 months. ROI and savings are model-based estimates derived from industry averages and are not guaranteed results; actual performance will vary based on local labor rates, film resin pricing, and specific throughput volumes.
## 🛠️ Procurement Evaluation Matrix
| Item | Recommended Criteria | Direct Business Impact | Pass / Fail |
|------|---------------------|------------------------|-------------|
| Load weight & size | Confirm machine capacity ≥ max pallet weight + 20% margin | Prevents motor overload and structural fatigue during peak shifts | ☐ |
| Film type | **Cast PE** for general use; **blown PE** for sharp-edged loads | Cast film maximizes pre-stretch efficiency; blown film provides puncture resistance for irregular edges | ☐ |
| Pre-stretch ratio | Minimum **200%** suggested; **250%** for film cost reduction | Higher pre-stretch directly lowers resin consumption and reduces material procurement costs | ☐ |
| Pallet exchange angle | **90–95°** for gentle transfer; avoid steeper angles | Reduces lateral forces on stacked goods, minimizing transit damage and insurance claims | ☐ |
| Cold-chain rating | Ensure motors, seals, and lubricants rated for **-10 °C** or lower | Prevents hydraulic fluid thickening and motor failure in sub-zero environments | ☐ |
| Recipe profiles | At least **10 profiles** for mixed-load flexibility | Eliminates manual recalibration time, reducing changeover downtime and operator error | ☐ |
| Safety compliance | CE marking required for EU; verify ANSI/PMMI for North America | Ensures regulatory compliance and reduces liability exposure during audits | ☐ |
| Budget (semi-auto) | $3,000–$15,000 for standalone wrapper; add $10,000–$20,000 for exchanger (as of 2024) | Aligns capital expenditure with throughput requirements and facility constraints | ☐ |
| Budget (full auto) | $20,000–$150,000+ depending on throughput and conveyor integration (as of 2024) | Scales with high-volume operations and automated downstream sorting requirements | ☐ |
## 🏗️ Technical FAQ
**Q: Can I add a pallet exchanger to an existing stretch wrapper?**
Α: Ναι, υπό την προϋπόθεση ότι το περιτύλιγμα έχει επαρκή χώρο στο δάπεδο και το ύψος του μεταφορικού ιμάντα ταιριάζει με το επίπεδο εκκένωσης του εναλλάκτη. Αναμένεται πρόσθετο κόστος ενσωμάτωσης ύψους 8,000–15,000 $ για συγχρονισμό PLC και αναβαθμίσεις κυκλωμάτων ασφαλείας.
**Q: What film thickness should I use for cold storage?**
A: **23–27 micron cast PE** performs optimally for most frozen goods due to its smooth surface and high pre-stretch compatibility. For loads with sharp corners or protruding edges, switch to **blown PE** in the same gauge range to improve puncture resistance. Verify temperature ratings with your resin supplier.
**Q: How long does training take for a new system?**
A: Most operators achieve proficiency within **2–4 hours**. Recipe-based PLCs significantly reduce the learning curve by automating tension and wrap-count adjustments, minimizing manual intervention and calibration errors.
**Q: Is the 95° exchanger safe for fragile electronics?**
Α: Ναι, όταν είναι εξοπλισμένο με υδραυλικό σύστημα ελεγχόμενης ταχύτητας και επενδεδυμένα στηρίγματα φορτίου. Η πλευρική δύναμη συνήθως παραμένει κάτω από 50 N, συγκρίσιμη με την ήπια συγχώνευση μεταφορικών ταινιών. Να επικυρώνετε πάντα με δείγματα φορτίων πριν από την πλήρη ανάπτυξη για να διασφαλίζετε τη συμβατότητα με τη συγκεκριμένη διαμόρφωση συσκευασίας σας.