Shrnutí
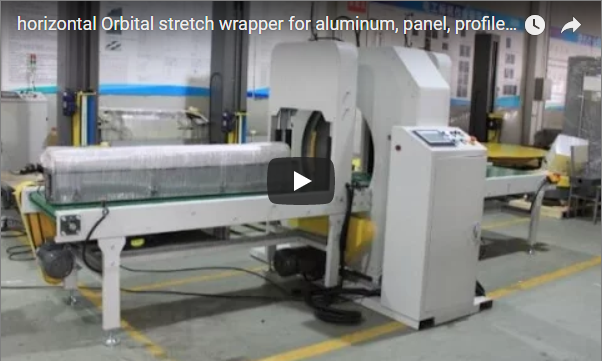
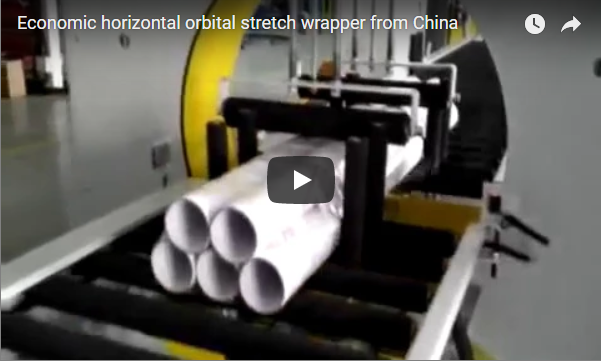
Eliminujte ruční manipulaci a zabraňte přesouvání nákladu u nepraktických, stlačitelných nebo dlouhých produktů díky automatickému horizontálnímu balicímu stroji v kroužcích. Horizontální orbitální baličky FHOPE pracující při rychlostech otáčení kroužků až 100 ot./min s dobou cyklu 20 až 35 s zajišťují stacionární náklad pod rovnoměrným napětím fólie na dopravníkové lince. Doprovodné video demonstruje kompletní automatizovaný cyklus.
Obsah
- Automatizovaný cyklus horizontálního balení a propustnost
- Proč omotat velké předměty kroužky
- Jak funguje horizontální obalovací systém
- Obálka a rozpočet filmu
- TECHNICKÉ ÚDAJE
- Kontrolní seznam pro výběr
- Ovládací prvky a bezpečnost
- Často kladené otázky k inženýrství
- Další krok
- Související čtení
- Zdroje
Automatizovaný cyklus horizontálního balení a propustnost
Horizontal ring wrapping secures products vulnerable to shifting or unwieldy to rotate—including compressible hose coils, cable bundles, extrusions, and boxed goods—by orbiting stretch film around a stationary load traveling through the ring axis.
The automated cycle follows a coordinated mechanical sequence:
- Přísun: The powered conveyor advances the load into the wrapping centerline.
- Stationary Clamping & Orbiting: Top-press or side-guide rollers secure compressible products while the orbital ring accelerates up to 100 rpm, applying pre-stretched film under closed-loop tension.
- Cut and Wipe Sequence: An automated pneumatic clamp-and-cut unit grips the film, cuts it cleanly, and secures the trailing tail at cycle completion before outfeed indexing.
Proč omotat velké předměty kroužky
Orbital wrapping eliminates centrifugal forces acting on the cargo. By keeping the load stationary on the horizontal conveyor while rotating the lightweight film carriage around it, even unstable or compressible goods (such as flexible corrugated pipe coils or light bundles) are wrapped without distortion or falling over.
For cylindrical coils wrapped horizontally (eye-horizontal / through-the-bore configuration), the equipment clears internal core dimensions while enclosing the outer perimeter. For rigid boxes, panels, and linear profiles, sizing is governed by the total cross-sectional diagonal clearance relative to the ring diameter.
Because every FHOPE system is custom built, machinery envelopes are tailored to customer product matrices. Standard coil configurations span an inner diameter (ID) of 250 to 650 mm, an outer diameter (OD) of 450 to 800 mm, and widths from 120 to 280 mm, accommodating unit loads from 5 to 30 kg.
Jak funguje horizontální obalovací systém
The wrapper mounts over the conveyor gap. The structural steel ring supports a balanced pre-stretch film carriage driven by heavy-duty polyurethane friction drive wheels or timing belts.
- Dodávka filmu: A motorized pre-stretch unit elongates the film prior to product contact, minimizing core compression on delicate goods while maximizing holding force.
- Řízení napětí: The carriage dispenses film smoothly at speeds up to 200 m/min to maintain throughput matching high ring RPM.
- Cycle Coordination: A central PLC synchronizes ring rotational speed (RPM) with conveyor linear speed (m/min) to achieve exact film overlap percentages (typically 30% to 60%). The cycle completes within 20 to 35 seconds per bundle.
Obálka a rozpočet filmu
Three baseline engineering checks verify throughput and material consumption prior to line commissioning:
1. Full-Cover Pass Calculation
For a stationary radial wrap or coil perimeter wrapping:
- Coil outer diameter (OD) = 0.8 m
- Effective band width (W_film) = 0.5 m
- Overlap target = 50% (effective step advance = 0.25 m)
- Perimeter coverage length = π × OD = 3.1416 × 0.8 m = 2.513 m
- Required passes = 2.513 m / 0.25 m = 10.05 passes The PLC rounds this up to 11 ring revolutions to guarantee complete outer overlap.
2. Film Stock Mass Budget
Stretch film inventory is budgeted by polymer areal density:
- Roll length = 1,000 m
- Roll width = 0.5 m
- Film thickness = 25 µm (0.000025 m)
- LLDPE resin density = 920 kg/m³
- Film mass = 1,000 m × 0.5 m × 0.000025 m × 920 kg/m³ = 11.5 kg (Note: This represents raw net film mass before pre-stretch elongation).
3. Cycle Time vs. Line Takt
- Target output = 144 units/hour
- Available cycle budget = 3,600 s / 144 = 25.0 s per piece This budget easily accommodates 5 s infeed, 15 s orbital wrapping (at 50–60 rpm), and 5 s clamp/cut/outfeed sequence.
TECHNICKÉ ÚDAJE
The values below represent standard engineering envelopes for coil and bundle ring wrapping models. Dimensions for extended linear profiles or boxed loads are engineered against your cross-sectional drawing.
| Parametr | Standardní rozsah | Engineering Remarks |
|---|---|---|
| Vnitřní průměr cívky (ID) | 250 až 650 mm | Sized for orbital ring wall clearance |
| Vnější průměr cívky (OD) | 450 až 800 mm | Must fit inside maximum ring opening circle |
| Coil Width / Package Height | 120 až 280 mm | Conveyor gap width clearance |
| Kapacita zatížení | 5 až 30 kg | Standard roller conveyor load rating |
| Celkový čas cyklu | 20 až 35 s na kus | Dependent on package size and pass count |
| Maximální rychlost vyzvánění | Až 100 ot./min | Frequency inverter (VFD) controlled |
| Film Carriage Delivery Speed | Až 200 m/min | High-speed powered pre-stretch option |
| Film Gauge Compatibility | 17 až 35 um | Cast or blown LLDPE stretch film |
Kontrolní seznam pro výběr
- Cross-Section Diagonal: Confirm maximum product cross-section (√(Width² + Height²)) to ensure a minimum 100 mm radial clearance inside the ring.
- Load Rigidity: Determine if top vertical hold-down rollers are needed for compressible coils or lightweight boxes.
- Takt Time Alignment: Match ring acceleration, wrap cycle time, and indexing conveyor speed to the upstream packing rate.
- Specifikace filmu: Define stretch film width (typically 250 mm or 500 mm), gauge, and required pre-stretch ratio (150% to 250%).
- Safety Guarding Integration: Confirm perimeter interlocks, light curtains, and Lockout/Tagout (LOTO) interface locations.
Ovládací prvky a bezpečnost
The machine operates in an automated continuous cycle under strict safety interlocks. High-inertia rotating assemblies require defined safeguarding protocols:
- Zone Interlocking: Infeed and outfeed portals feature Category 4 / PLe light curtains or perimeter safety fencing with monitored door interlocks. Opening any access gate triggers an immediate Category 0 controlled stop.
- Bezpečnost údržby: Power isolation points must be locked out per OSHA / EN standards before servicing film carriages, adjusting clamp blades, or entering the ring envelope. Reaching into the rotating ring during operation is strictly interdicted.
- Harmonizované standardyVyrobeno v souladu s ISO 12100 (Bezpečnost strojních zařízení – Obecné zásady pro konstrukci – Hodnocení rizik a snižování rizik) a EN-415 10 (Bezpečnost balicích strojů – Obecné požadavky).
Často kladené otázky k inženýrství
Q: What products are best suited for horizontal ring wrapping? A: Long extrusions, pipe and hose coils, wire bundles, lumber, and boxed goods. It is especially beneficial for products that deform or tip over if turned on conventional turntable wrappers.
Q: How does the system achieve 20 to 35 second cycle times? A: By combining ring rotation speeds up to 100 rpm with rapid automated pneumatic clamp-and-cut units. Film is captured immediately at the wrap position without manual tying.
Q: How is full film coverage determined? A: The onboard HMI calculates passes from the product dimensions and user-selected overlap percentage. For example, a 0.8 m OD coil wrapped with a 0.5 m band at 50% overlap requires 10.05 theoretical passes, which the PLC rounds up to 11 full revolutions.
Q: What international safety standards govern the machine? A: Machines destined for CE markets follow ISO 12100 for comprehensive risk reduction and EN 415-10 for packaging machinery mechanical and electrical safety integration.
Q: Can this wrapper integrate directly into an automated production line? A: Yes. The orbital unit features dry contacts and industrial Ethernet (Profinet/EtherNet/IP) protocols to handshake with upstream coiling/stacking stations and downstream sorting conveyors.
Další krok
- Odeslat výkresy: Provide product cross-section dimensions, weight range, and target hourly takt time.
- Obdržet technický návrh: Obtain a custom ring layout, cycle simulation, and formal quotation within 48 hours.
- Site & Line Integration Survey: Schedule an engineering review with our project team for mechanical and controls tie-in.
Contact our packaging engineering group: info@fhopepack.com
Související čtení
- Stroj na navíjení a vázání kabelů
- Stroj na navíjení a balicí stroj hadic: Nejprve cívka, poté fólie
- Ekonomický balicí stroj na kabelové cívky: Specifikace FPCA, doba balení a nastavení překrytí
- Stroj na balení trubek a hadic z HDPE: Vysvětlení balení kroužkem s průchodkou
- Balicí stroj kabelových cívek pro cívky s malým vnitřním průměrem
- Automatický stroj na navíjení a balení trubek pro hadice a plastové trubky
Zdroje
- Stroj na balení hadicových cívek FPH-200
- Automatický stroj na navíjení a balení kabelů
- ISO 12100: Safety of machinery — General principles for design — Risk assessment and risk reduction
- EN 415-10: Safety of packaging machines — Part 10: General requirements
- FHOPE Engineering Technical Documentation
Poslední aktualizace: 28. 10. 2026