ملخص تنفيذي
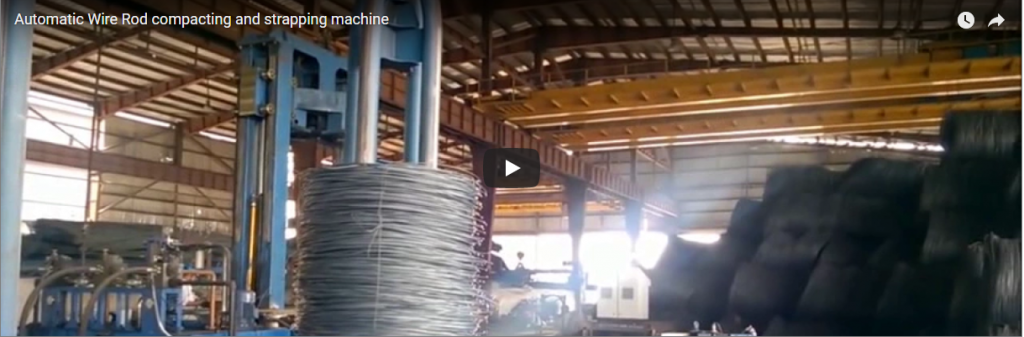
An automated steel wire rope coiling and strapping line transforms continuous wire or rope extrusion and drawing feeds into precisely measured, cut, and radial-strapped coils without manual handling. Operating at line speeds from 200 to 800 m/min, the system utilizes a high-precision dual-head turntable arrangement to eliminate production downtime: while one head coils at full line velocity, the idle head completes radial strapping through the eye and initiates pneumatic discharge for up to 40 coils per hour. The integrated tension accumulator and servo traverse eliminate wire overlapping, coil slack, and surface scuffing across severe industrial packaging cycles.
جدول المحتويات
- ما يفعله جهاز لف الملفات
- التوتر ومجمع الأسلاك
- رأس واحد أو رأسين
- بيانات الملف
- مثال عملي: هل يستطيع رأسان مواكبة بعضهما البعض؟
- قائمة التحقق من الاختيار
- السلامة: EN 415-10 و ISO 12100
- أسئلة وأجوبة هندسية
- الخطوة التالية
- القراءة ذات الصلة
- مصادر
ما يفعله جهاز لف الملفات
The continuous steel wire rope enters the machine through a dual-wheel optical/rotary encoder length meter. To prevent marring, indenting, or stripping surface coatings on galvanized, stainless, or polymer-sheathed wire rope, the bottom traction encoder is lined with high-density polyurethane (PU 95 Shore A). This metering assembly records lineal length to 0.01 m precision, feeding high-speed interrupt pulses directly to the central PLC to manage multi-stage deceleration and trigger the flying shear mechanism.
Downstream of the meter, the wire rope feeds to a horizontal turntable head configured in an eye-to-sky (eye-vertical) orientation. A dedicated digital servo traverse drive syncs axially with turntable rotation speed:
Traverse Pitch (mm/rev) = Wire Diameter (mm) × Pitch Factor (1.02–1.08)
This coordinated feed eliminates interlocking strands, wire crossover, and perimeter collapse, ensuring geometrically square coils with flat outer boundaries.
Once the targeted winding recipe is completed:
- The spindle slows dynamically to zero at a designated circumferential shear home position.
- A high-hardness hydraulic or pneumatic shear blade cuts the rope.
- The expandable inner core pins collapse pneumatically, releasing coil core tension.
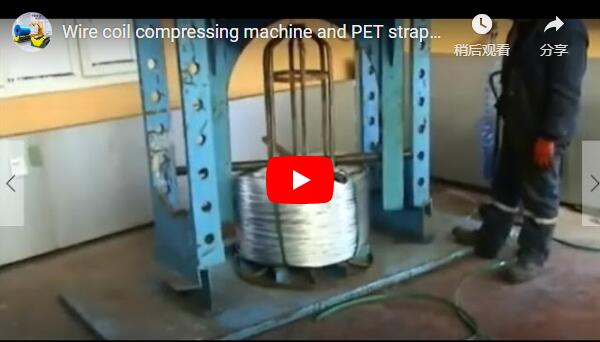
- An automated strapping arm rotates through the open coil eye, feeding, tensioning, and friction-welding poly strapping bands.
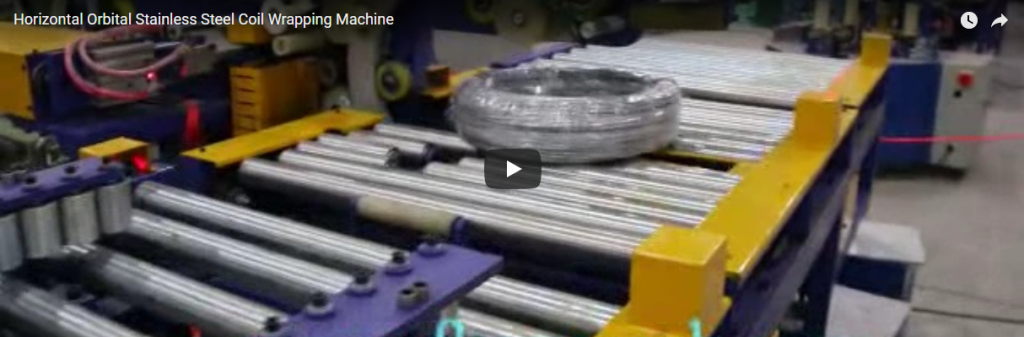
- The strapped package is pushed laterally onto an exit roller bench beneath the structural blue main frame for downstream robotic palletizing or wrapping.
All cycle parameters—including target length, outer diameter (OD), inner diameter (ID), core width, traverse speed profile, and active fault diagnostics—are configured via a multi-lingual industrial HMI. Operators can trim winding line speeds and cut lengths on-the-fly without stopping the line, while switching between wire rope diameters is handled by calling pre-calibrated product recipes from PLC memory.
التوتر ومجمع الأسلاك
A vertical dancer/accumulator assembly is stationed between upstream payoff/drawing operations and the coiler. Holding a buffer volume of 5 to 20 m of wire rope, it maintains continuous loop tension regardless of momentary speed differentials during coiling spindle ramp-up or cut cycles.
Tension is calibrated via a closed-loop 24 V DC electropneumatic regulator coupled to precision load cells or dancer angle potentiometers. A synchronization algorithm automatically modulates coiler take-up inverter frequency to track upstream line velocity, isolating the incoming rope from shock loading, plastic elongation, or structural untwisting:
Buffer Time (s) = Accumulator Active Storage (m) ÷ Production Line Velocity (m/s)
Precision inductive limit switches track the high and low mechanical boundaries of dancer travel. If upstream wire feed stops abruptly or line tension drops due to a strand fracture, the system executes an immediate emergency stop (Category 0 / Category 1 per IEC 60204-1) to avoid machine jamming and protect the operator.
رأس واحد أو رأسين
Choosing between single-head and dual-head configurations depends on continuous upstream process limits:
- Single-Head Configuration: The drawing, stranding, or extrusion line must ramp down or pause while the coil is sheared, bound through the eye, and cleared from the drum. This layout suits batch production or slow line outputs, rated up to 20 coils per hour.
- Dual-Head Configuration: Employs an indexing rotary chassis or alternating feed carriage. As Head 1 reaches its target length and shears, the wire lead is instantly transferred to Head 2 to commence winding without dropping upstream line velocity. Simultaneously, Head 1 indexes into the strapping and ejection station.
Dual-head architecture delivers 100% duty-cycle operation, doubling practical plant throughput to 40 coils per hour.
بيانات الملف
| معلمة الفنية | Specification / Metric Unit | ملاحظات هندسية |
|---|---|---|
| Winding Linear Speed | 200-800 م / دقيقة | Inverter/servo-driven vector control |
| قدرة الإنتاج | 20 coils/h (Single Head) / 40 coils/h (Dual Head) | Dependent on strap count and coil length |
| Wire / Rope Diameter Range | 1.0–16.0 mm (Customizable upon order) | Tailored feed guides, rollers, and shears |
| Length Metering Precision | ±0.01 m (Encoder pulse tracking) | Dynamic two-stage deceleration curve |
| Accumulator Buffer Capacity | 5–20 m effective take-up | 24 V DC proportional pneumatic regulator |
| Working Pass-line Height | 1,000 mm nominal (±50 mm) | Ergonomic conveyor and line matching |
| معيار إمداد الطاقة | 380 V / 440 V, 3-Phase, 50/60 Hz | Control circuit: 24 V DC safety bus |
| Radial Strapping Format | Through-the-eye; 2, 3, or 4 radial bands | Automatic coil indexing on turntable |
| Strapping Material Spec | High-tensile PP or PET (8–10 mm width, 0.8 mm thickness) | Smooth feed track with jam detection |
| Strap Joint Execution | High-frequency friction weld | 75%–80% base strap tensile strength retention |
مثال عملي: هل يستطيع رأسان مواكبة بعضهما البعض؟
To confirm whether dual coiling heads can maintain continuous 100% capacity without throttling upstream lines, consider the following reference specification:
- المنتج: 500 m wire rope coil
- خط السرعة: 300 م/دقيقة
- متطلبات التعبئة والتغليف: 4 radial PP straps through the coil eye (empirical strapping cycle: 15 s per strap = 60 s total)
| Production Step & Balance Metric | Mathematical Evaluation | Resulting Time Allocation |
|---|---|---|
| Winding cycle per coil (T_wind) | (500 m ÷ 300 m/min) × 60 s/min | 100.0 ق |
| Maximum theoretical output (Dual Head) | 3,600 s/h ÷ 100 s | 36.0 coils/h (Within 40/h machine ceiling) |
| Available idle window for secondary head | Equivalent to winding time (T_wind) | 100.0 ق |
| Strapping cycle (4 radial straps) | 4 straps × 15 s/strap | 60.0 ق |
| Margin for shear, indexing, and coil push-off | 100.0 ثوانٍ - 60.0 ثوانٍ | 40.0 s (Sufficient safety margin) |
| Accumulator storage buffer at 300 m/min | (20 m ÷ 5.0 m/s) | 4.0 s (For flying cut transition) |
التحليل الهندسي: At 300 m/min, winding 500 m requires exactly 100 s. Because strapping takes 60 s, the idle station retains a comfortable 40 s buffer to collapse the core pins, rotate the indexing arm, and push the coil to the discharge table. The line runs continuously at 36 coils/h without back-pressure.
Critical Limit Check: If coil length is cut to 250 m at the same 300 m/min speed:
- Winding cycle drops to: 250 ÷ 5.0 = 50 s
- Strapping 4 bands requires 60 s.
- The winding station finishes 10 s before strapping is complete. In this scenario, the line must either adjust to 2 or 3 straps per coil, or the upstream line must slow down to 250 m/min to maintain process synchronization.
قائمة التحقق من الاختيار
When preparing technical specifications for a customized coiler proposal, compile the following operational parameters:
- Rope Construction & Grade: Outer wire diameter, rope structure (e.g., 6×19, 7×7), tensile strength (N/mm²), and surface finish (dry, galvanized, lightly oiled, or coated).
- Target Coil Geometry: Minimum and maximum Outer Diameter (OD), required core Inner Diameter (ID), and coil stack height/width range.
- Upstream Velocity Profile: Constant extrusion/drawing speed, acceleration/deceleration rates (m/s²), and maximum line capacity (m/min).
- هندسة الآلة: Single-head (batch/intermittent) versus dual-head (continuous zero-downtime) selection.
- متطلبات التأمين: Number of radial strap positions (2, 3, or 4 straps), strapping material (PP vs. PET), and strap tension limits.
- التكامل النهائي: Inline automated checkweighing, barcode/RFID labeling, shrink film wrapping, or palletizer handshakes.
السلامة: EN 415-10 و ISO 12100
Every coiler is engineered in accordance with EN-415 10 (Safety of packaging machines – General requirements) and validated via risk assessments based on ISO 12100: 2010:
- Entanglement & Whiplash Containment: The perimeter of the rotating coiling heads is secured by electro-galvanized safety fencing painted in RAL 1021 safety yellow. Access doors feature dual-channel Category 3 / PL d interlock safety switches (ISO 13849-1).
- Shear Blade Guarding: The high-speed cutting unit is housed within an interlocking poly-carbonate barrier, preventing manual reaching while armed.
- Accumulator Runaway Protection: Dual mechanical stops with spring-loaded shock absorbers prevent dancer carriage derailment, backed by monitored inductive over-travel limits that disconnect motor power via safe-torque-off (STO) drives.
- هندسة التحكم: Dual-channel emergency-stop pushbuttons are placed at the primary operator panel, discharge conveyor, and coiler loading stations, linked to a certified 24 V safety relay.
أسئلة وأجوبة هندسية
Q: How does the system achieve ±0.01 m cut accuracy at 800 m/min? A: The PU-coated tracking wheel communicates with a dedicated PLC high-speed counter card. When approaching the target length, the variable frequency drive executes a controlled S-curve deceleration down to a creeping velocity, ensuring precise blade synchronization without rope slip.
Q: Can we adjust package width and core ID for different contracts? A: Coil traverse width is adjusted directly through recipe management on the HMI. Core ID changes utilize modular, rapid-exchange pin segments or segmented core mandrels that expand and collapse over a designated size window.
Q: How does the machine respond to unexpected wire breaks? A: If the wire snaps upstream, the vertical accumulator carriage drops instantaneously toward its low limit, triggering optical sensors. The PLC initiates an emergency ramp-down across the traverse and spindle, isolates the strapping head, and flashes an alert stack light.
Q: What safety standards dictate export compliance? A: The machine is built to EN 415-10 and ISO 12100 for CE certification, with electrical enclosures adhering to IEC/EN 60204-1 and NFPA 79 for North American installations.
الخطوة التالية
- Submit Your Production Data: Forward wire rope outer diameters, maximum drawing speeds (m/min), and required coil dimensions (ID/OD/Width) to info@fhopepack.com.
- Line Cycle Review: Our mechanical engineering team will calculate your cycle balance table, verifying strap count against winding velocity.
- عرض هندسي خلال 24 ساعة: Receive a comprehensive layout drawing, equipment quote, and cycle time confirmation.
القراءة ذات الصلة
- آلة لف الأسلاك الأوتوماتيكية (المنتج)
- آلة لف وربط الأسلاك الفولاذية الأوتوماتيكية (المنتج)
- آلة لف وإعادة لف الأسلاك الفولاذية الأوتوماتيكية
- آلة لف الأسلاك الفولاذية الأوتوماتيكية للف الأسلاك وربطها
- آلة لف وتغليف الأسلاك والكابلات، تعمل على مدار 24 ساعة
مصادر
- FHOPE Technical Documentation: High-Speed Wire & Cable Coiling Systems
- Factory Acceptance Test (FAT) Empirical Data: Radial Strapping Station Cycle Logs
- International Standard EN 415-10: سلامة آلات التعبئة والتغليف - الجزء 10: المتطلبات العامة
- المعيار الدولي ISO 12100:2010: سلامة الآلات - مبادئ عامة للتصميم - تقييم المخاطر وتقليل المخاطر
- International Standard ISO 13849-1: سلامة الآلات – الأجزاء المتعلقة بالسلامة في أنظمة التحكم
آخر مراجعة: 2026-10-19