执行摘要
Automated tire wrapping equipment replaces slow, inconsistent manual packing by applying orbital and toroidal stretch wrapping to passenger, truck, and heavy-duty OTR tires. Selecting the correct machine requires balancing the tire’s dimensional envelope—Outer Diameter (OD), Inner Diameter (ID), cross-sectional width, and weight—against line cycle times (18 to 50 seconds per unit). Equipment pricing reflects physical ring clearance, structural load capacity, installed drive power, and upstream automation integration, with investment payback achieved through direct labor reduction and high-ratio film pre-stretch savings.
在生产和物流设施中,轮胎、软管卷盘、盘绕管材和圆形弹性体产品的搬运和包装面临着独特的工程挑战。传统的手工包装方法速度慢、存在人体工程学风险且效果不稳定,经常导致运输过程中出现磨损、受潮污染和材料浪费。专用的轮胎包装机——也称为轨道式轮胎包装机或环形包装机——正是为了解决这些物理瓶颈而设计的。
在现代包装生产线中,从人工缠绕过渡到自动化环状包装,可以立即显著提高生产效率、货物密封性和树脂消耗量。本工程指南详细介绍了机械原理、操作优势、尺寸参数和成本驱动因素,这些对于工厂经理和包装工程师选择设备至关重要。
(术语说明:本指南在技术分析中通篇使用美式拼写“tire”,但在直接引用、正式型号名称和链接的参考文档中保留国际和OEM目录中的拼写“tyre”。)
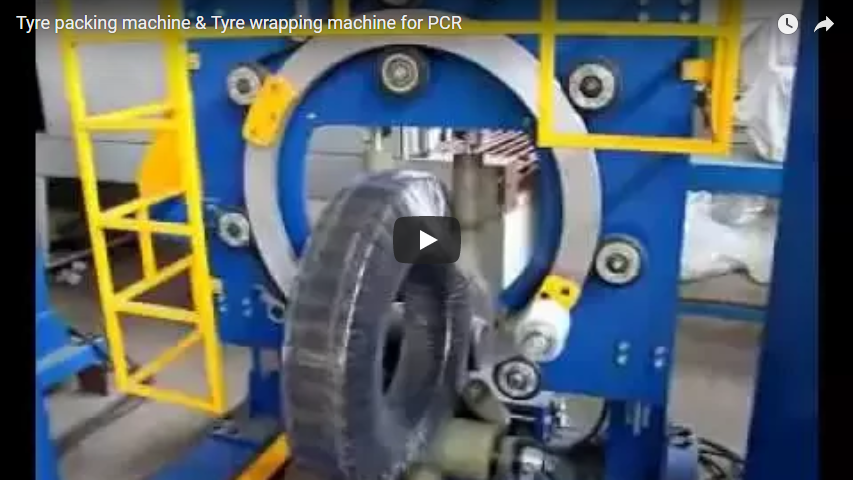
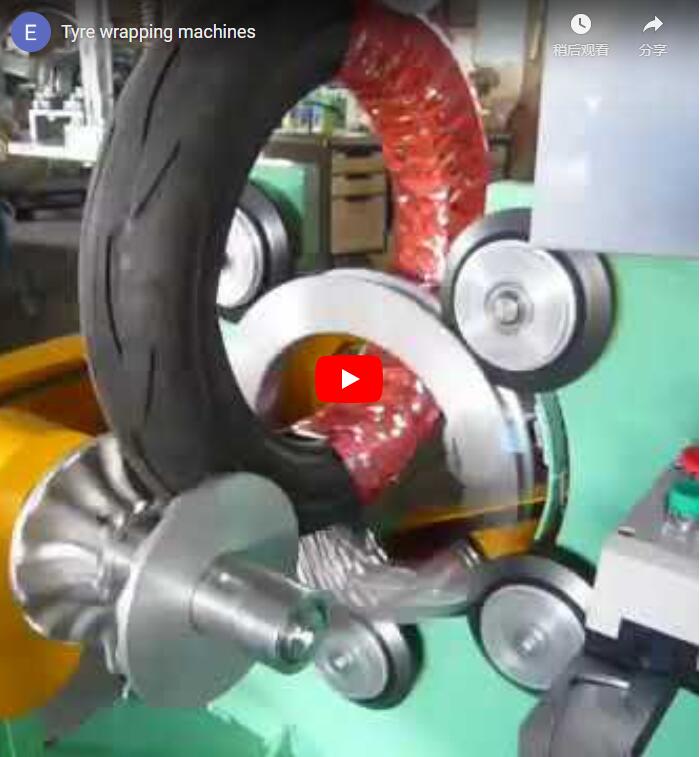
[ Rotating Toroidal Ring ] / \ +—-/———————–+ | | Tire Cross- | | Film carriage orbits through | | Section Envelope | | the tire bore (Rim ID) while | +———-+———-+ | polyurethane trunnion rollers | | | rotate the carcass on its axis. +————–|————–+ [Driven Rollers]
1. 核心问题:为何手动轮胎包装不足
轮胎制造厂、翻新厂和配送中心在依赖人工或半人工托盘转盘缠绕时,会面临反复出现的物流故障模式:
- 几何不一致性: 人工覆膜无法保持均匀的径向预拉伸或一致的层间重叠(通常在15%到70%之间波动)。这种不一致性会导致水分渗入、薄膜散开以及存储堆垛不稳定。
- High Ergonomic and Labor Burden: Handling passenger tires (8–15 kg) repeatedly causes strain injuries, while commercial truck tires (30–80 kg) and heavy OTR units present severe occupational hazards under plant safety guidelines.
- 电影过度消费: Hand application cannot achieve mechanical neck-down control or dynamic pre-stretch, consuming up to 3× more Linear Low-Density Polyethylene (LLDPE) than automated powered-carriage systems.
- 表面和珠粒降解: 薄膜密封不严会导致多式联运过程中出现紫外线降解、臭氧开裂、油脂污染和珠座磨损。
- 线路吞吐量不平衡: 手动缠绕工位每条轮胎需要 90 到 180 秒,这会在高速硫化机或自动化精加工单元后面造成操作瓶颈。
2.
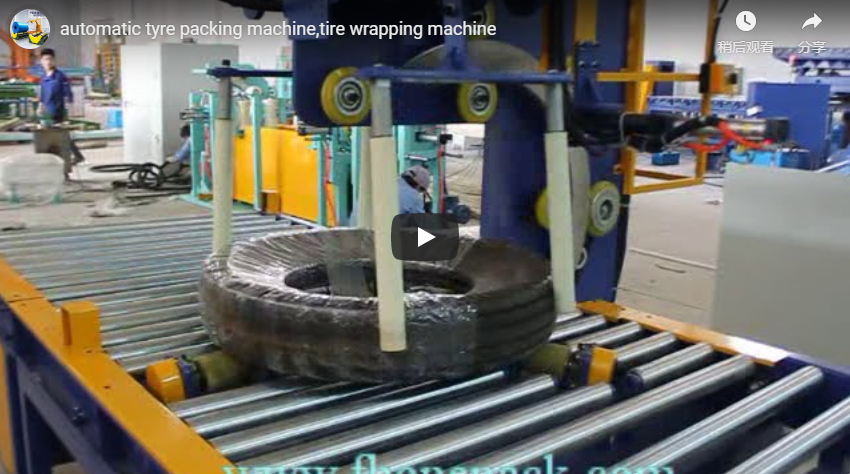
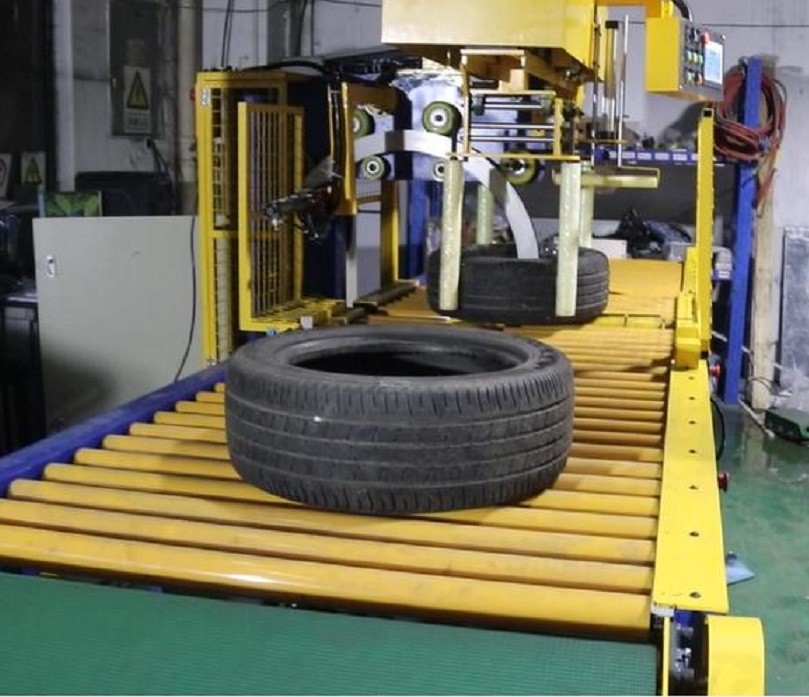
- 进给和对齐: 轮胎通过重力输送、动力滚筒或高架落入式输送机进入,落入两个聚氨酯涂层支撑滚筒中,使胎体相对于环形径向平面居中。
- 环形穿梭机交战: The rotating ring accelerates to set operational speed, guiding the film dispensing head through the tire’s inner bore and across the outer tread circumference.
- 协调双轴运动: 驱动支撑辊的表面速度与环形辊的旋转速度相匹配,从而产生电子同步的搭接比:
Overlap Ratio (%) = [1 - (V_tire_surface / (Film_Width × ω_ring))] × 100 - 张力控制预拉伸: A motorized roller system prestretches the film prior to exit. Constant load regulation stabilizes winding tension, preventing bead deformation on unmounted casings.
- 气动切割密封/胶带粘贴: 循环完成后,自动气动臂夹住薄膜,热线或锯齿刀片切断薄膜,自动擦拭或胶带固定机构将薄膜尾部牢固地固定在轮胎胎面外径 (OD) 上。
- 弹射: 动力气动升降臂或倾斜轴承将包装好的产品踢到出料收集输送机上。
3. 主要技术规格和工程特点
When assessing machinery specifications against plant requirements, focus on kinematic configuration, ring clearances, and structural ratings. FHOPE manufactures dedicated standalone wrapping units tailored to specific product dimensions:
| 参数 | FPT-200 | FPT-300 | FPT-400 |
|---|---|---|---|
| Compatible Tyre ID | 300–700毫米 | 500–900毫米 | 750–1200毫米 |
| Compatible Tyre OD | 510–800毫米 | 800–1200毫米 | 1000–1400毫米 |
| Max Tyre Width | 40–250毫米 | 80–300毫米 | 80–400毫米 |
| Tire Weight Capacity | 10-30 kg | 10-100 kg | 20-120 kg |
| 环旋转速度 | 0–120 转/分钟 | 30–110 转/分钟 | 30–80 转/分钟 |
| Cycle Packing Speed | 18–30 秒/件 | 25–40 秒/件 | 35–50 秒/件 |
| 薄膜重叠范围 | 10-80% | 20-80% | 20-80% |
| 已安装驱动功率 | 1.5 kW | 2.0 kW | 2.5 kW |
| 电源 | AC 380V / 50Hz | AC 380V / 50Hz | AC 380V / 50Hz |
- 净空尺寸范围: 包覆环的内径(
D_ring必须能够轻松避开轮胎横截面和旋转车架的占地面积:D_ring ≥ Carcass_Height + Carriage_Radial_Projection + Clearance_Margin至关重要的是,轮胎内径(轮辋内径)必须与梭子架的轮廓相适应:Tire_ID_min ≥ Shuttle_Thickness + Film_Spool_Width + clearance(clearance confirmed against the carriage drawing) - 控制集成: PLCs tied to a touch-panel HMI enable operators to store custom wrap recipes (ring r/min, roller drive speed, overlap percentage, reinforcement wraps) by SKU.
- 材料通用性: Standard carriages accept blown or cast LLDPE stretch film, HDPE, PP tape or VCI anti-corrosion film; film thickness and roll size are specified per project.
4. 型号选择:使设备与生产线几何形状相匹配
Equipment selection depends strictly on dimensional envelope boundaries, production cadence, and whether standalone operation or continuous inline packaging is required.
Standalone Machine vs. Continuous Automated Line Selection Rule
To determine whether an application requires an individual toroidal wrapping station or an inline continuous packaging system, apply the following operational envelope thresholds:
- 指定一个 Automatic Tire Packing Line: Select the complete automated line if production fits the standardized operational window:
- Tire Weight: 5–100 kg
- Tire Height (Width): 150–300 mm
- Tire Outer Diameter (OD): 600–1000 mm
- Tire Inner Diameter (ID): 150–500 mm
- Continuous Line Target: 30–35 s/pcs cycle rate
- Plant Infrastructure: Inline powered roller conveyors operating at 2–4 m/min, compressed air supply of 5–7 bar, and electrical connection of approximately 2.2 kW (380V / 50Hz / 3ph). The line carriage utilizes standard stretch film rolls with ID 50 mm, OD 80–120 mm, and width 60–70 mm.
- Specify a Standalone Wrapper (FPT Series): If products fall outside this envelope—such as narrow tires below 150 mm width, large casings with OD up to 1400 mm, internal bores requiring clearances up to 1200 mm ID, or high-mix lines with frequent manual staging—select a dedicated standalone machine:
- Small passenger and motorcycle tires (OD 510–800 mm, weight 10–30 kg): Choose FPT-200.
- Standard passenger, commercial, and light van tires (OD 800–1200 mm, weight 10–100 kg): Choose FPT-300.
- Heavy commercial, bus radial (TBR), and small agricultural tires (OD 1000–1400 mm, weight 20–120 kg): Choose FPT-400.
5. 轮胎包装机的价格受哪些因素影响?
轮胎包装设备的购置成本取决于机器的结构刚性、机械尺寸和自动化程度。主要定价因素包括:
- Ring Diameter and Structural Frame Rigidity: Larger structural rings designed to wrap casings up to 1400 mm OD require wider fabricated ring gearings, oversized guide wheels, and heavier structural frames to dissipate dynamic centrifugal forces.
- 驱动系统和动态有效载荷: Moving a 30 kg tire requires moderate torque, whereas rotating a 120 kg commercial tire at high speed demands heavy-duty gearboxes and upgraded variable frequency drives. This drive progression scales directly with installed motor capacity: 1.5 kW on the FPT-200, 2.0 kW on the FPT-300, and 2.5 kW on the heavy-duty FPT-400.
- 自动化和物料搬运升级: Standalone operator-loaded stations represent the most economical capital outlay. Upgrading to a continuous automated packaging line (rated at approximately 2.2 kW base drive power) introduces integrated powered conveying systems, 5–7 bar pneumatic centering arms, automated film cutting and clamping mechanisms, and optical sensor positioning.
- 预拉伸托架工程: Basic mechanical friction-brake carriages have a lower initial cost but lack pre-stretch control. Motorized dual-roller powered pre-stretch carriages maximize film yield (delivering up to 200%–300% stretch), cutting long-term resin expenditure.
- Specialized Material and Multi-Dispenser Systems: Carriages engineered to run alternative substrates—such as woven PP tape, reinforced paper, or VCI rust-inhibiting material alongside stretch film—require multi-reel shuttles and dedicated constant-tension brake assemblies.
6. 实用工程采购清单
在批准轮胎包装机的资本支出(CapEx)之前,请审查以下技术标准清单:
- 定义产品边界尺寸: 记录所有生产 SKU 的最小和最大轮胎外径、内径、横截面宽度以及湿/干胎体重量。
- 检查孔径径向间隙: 确认它
Tire_ID_min - Shuttle_Profile_Width ≥ 50 mm防止环旋转过程中发生机械干涉。 - 计算线路节拍时间: Verify that machine cycle times (18–30 s on FPT-200, 25–40 s on FPT-300, 35–50 s on FPT-400, or 30–35 s on automated lines) match target hourly cell outputs with a 15% operational buffer.
- Evaluate System Architecture: Match facility layout to either a self-contained standalone wrapping unit or a fully conveyorized automated packing line.
- Verify Pneumatic and Electrical Supplies: Ensure utility feeds support 380V 50Hz 3-phase power and 5–7 bar clean compressed air for automatic cut-and-clamp circuits.
- Audit Film Specifications: Confirm core and roll compatibility (e.g., standard LLDPE or 50 mm ID core, 80–120 mm OD roll for compact shuttles).
7. 结论:应按产品线参数而非产品目录标准进行规范
Selecting the proper tire packaging system requires balancing key physical variables: outer and inner clearance envelopes, casing weights, and line automation levels. Specifying an undersized wrapper causes physical shuttle collisions inside the tire bore, while selecting an oversized machine for small production volumes introduces unnecessary floor space allocation and capital cost.
Review product dimensional limits, verify that the wrapping shuttle clears the minimum tire rim bore, and compare standalone units against integrated packaging lines. FHOPE provides complete mechanical layout drawings, cycle time assessments, and equipment proposals delivered within 24 to 48 hours to match specific plant throughput and dimensional constraints.
上次审核日期: 2026年11月05日