> **Executive Summary**
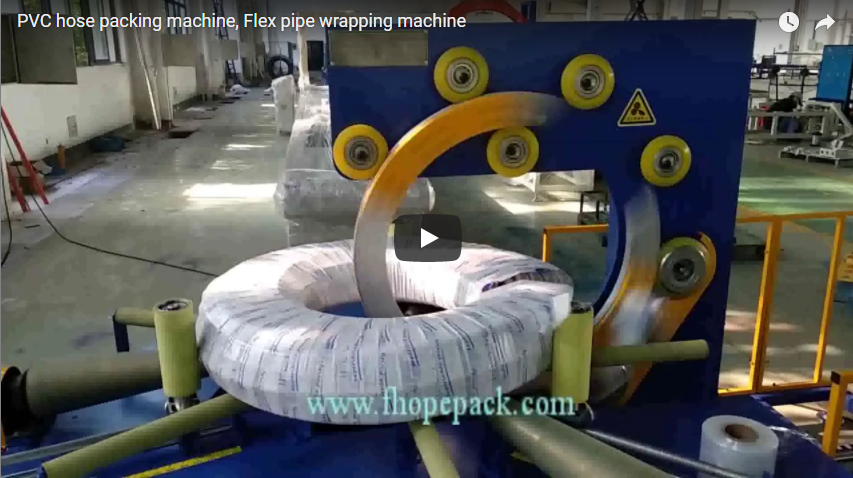
> The FPH-300N hose coil stretch wrapping machine is an orbital eye-through packaging system engineered for flexible garden hoses, corrugated conduits, and extruded plastic tubes. Supporting coils from 10 to 100 kg on dual motor-driven polyurethane rollers (eye-vertical orientation), the system drives an orbital wrapping ring at infinitely adjustable speeds up to 120 r/min via VFD control. It completes a tight, dust-tight, and moisture-resistant wrap cycle in 23 to 35 seconds. Below is the technical specification, an empirical cycle-time calculation model, and compliance guidelines under EN 415-10.

<iframe width="940" height="535" src="https://www.youtube.com/embed/oQQJtuG4lrU" frameborder="0" allow="accelerometer; autoplay; clipboard-write; encrypted-media; gyroscope; picture-in-picture; web-share" referrerpolicy="strict-origin-when-cross-origin" allowfullscreen></iframe>

---

<h2 id="table-of-contents">Table of Contents</h2>

<ul>
<li><a href="#why">Why Hose Coils Require Eye-Through Orbital Film Wrapping</a></li>
<li><a href="#how">Kinematic Working Principle of the FPH-300N</a></li>
<li><a href="#specs">FPH-300N Technical Specifications</a></li>
<li><a href="#example">Worked Example: Ring Revolutions, Cycle Times, and Output Model</a></li>
<li><a href="#options">Modular Options for High-Throughput Automation</a></li>
<li><a href="#selection-checklist">Engineering Selection Checklist: Parameters to Provide</a></li>
<li><a href="#safety">Safety Architecture and EN 415-10 Compliance</a></li>
<li><a href="#engineering-faq">Engineering FAQ</a></li>
<li><a href="#next-step">Project Next Steps and Engineering Inquiries</a></li>
<li><a href="#related-reading">Related Reading</a></li>
<li><a href="#sources">Reference Standards and Technical Sources</a></li>
</ul>

<h2 id="why">Why Hose Coils Require Eye-Through Orbital Film Wrapping</h2>

Extruded garden hoses, corrugated electrical conduits, and industrial pneumatic tubes retain high elastic memory after coiling. Conventional strapping or manual tape banding concentrates radial stress on single points, causing outer-layer deformation, coil unwrapping, and transit scuffing inside corrugated boxes.

Orbital eye-through stretch wrapping solves this structural issue by applying continuous helical wraps through the coil core (eye) and around the outer circumference. This creates uniform, multi-directional containment that preserves circular geometry, prevents turn dislocation, and seals the product against ambient dust and moisture. Clear LLDPE stretch film maintains full brand and color visibility on retail display racks while reducing manual packaging labor on high-output extrusion lines.

<h2 id="how">Kinematic Working Principle of the FPH-300N</h2>

The FPH-300N operates on a two-axis coordinated kinematic system:

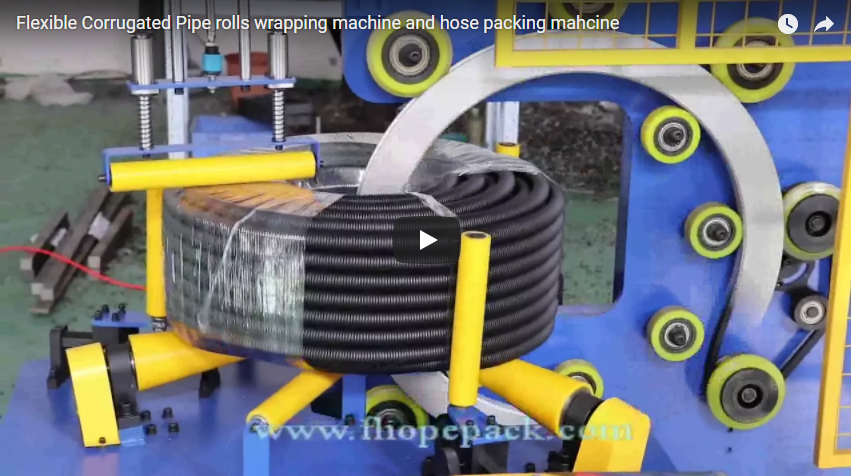
1. **Part Positioning and Loading:** The operator loads the strapped coil onto dual polyurethane-coated drive rollers. The coil is positioned in an eye-vertical orientation with its core aligned through the center opening of the stationary cast-aluminum ring frame.
2. **Cycle Initiation and Safety Interlock:** Closing the perimeter yellow interlocked safety mesh guard arms the system. The operator initiates the cycle via the remote console or pedal switch.
3. **Synchronized Helical Wrapping:** The orbital ring rotates the film dispenser through the open center of the coil and around its cross-section. Simultaneously, the bottom support rollers rotate the coil around its horizontal centerline. The coordinated velocity ratio between ring rotation (RPM) and roller surface speed (m/min) establishes the precise helical film pitch and overlap percentage.
4. **Ring Home-Position Reset:** Upon reaching the preset wrap count or limit switch target, the VFD brings the orbital ring to a smooth deceleration stop at the designated 12-o'clock loading position. The operator unlatches the guard and offloads the fully encapsulated coil.

<h2 id="specs">FPH-300N Technical Specifications</h2>

| Technical Parameter | Specification / Tolerance Range |
| :--- | :--- |
| Inner Diameter (ID) Range | Φ300–700 mm |
| Outer Diameter (OD) Range | Φ500–1,000 mm |
| Coil Axial Width | 100–300 mm |
| Maximum Weight Capacity | 10–100 kg |
| Packaging Cycle Duration | 23–35 s per coil (parameter dependent) |
| Maximum Ring Speed | Up to 120 r/min (inverter controlled via VFD) |
| Film Overlap Adjustment | 10% to 90% (programmable via speed ratio) |
| Film Material Specifications | LLDPE Stretch Film: OD 100–180 mm, ID 50 mm, Width 90–100 mm |
| Alternative Material Compatibility | Crepe paper, woven HDPE tape, or VCI film |
| Total Drive Power | 1.9 kW |
| Electrical Configuration | 380 V / 60 Hz / 3-Phase (Custom voltages available) |

A friction brake assembly on the high-speed film carriage ensures uniform unwinding tension without ballooning or web tearing.

<h2 id="example">Worked Example: Ring Revolutions, Cycle Times, and Output Model</h2>

Consider a standard industrial hose coil with the following dimensions: **OD = 800 mm**, **ID = 400 mm**, and **Width (W) = 200 mm**. The packaging recipe specifies a **100 mm film roll width** with a **50% overlap at the outer circumference**.

### 1. Ring Revolutions per Cycle
- Outer circumference = π × OD = 3.1416 × 800 mm = 2,513 mm.
- At 50% overlap, the effective film advance per ring revolution is:
  `Advance = 100 mm × (1 − 0.50) = 50 mm/rev`.
- Total revolutions required = `2,513 mm ÷ 50 mm/rev = 50.3 revolutions`.
  Rounding up to ensure complete closure yields **51 ring turns**.

### 2. Pure Wrapping Cycle Time
- At a conservative VFD production speed of **120 r/min** (2.0 rev/s):
  `Cycle Time = 51 rev ÷ 120 r/min = 0.425 minutes ≈ 25.5 seconds`.
  This aligns with the 23–35 second specification window.

### 3. Film Overlap Distribution at the Core
Because the inner circumference is smaller (`π × 400 mm = 1,257 mm`), the effective advance per turn across the coil eye is:
`Advance_eye = 50 mm × (400 ÷ 800) = 25 mm/rev`.
The resulting overlap at the eye is:
`Overlap_eye = (1 − 25 mm ÷ 100 mm) × 100% = 75%`.
This structural variance creates a naturally reinforced core that prevents coil collapse during stacking.

### 4. Unstretched Film Consumption
- Cross-sectional perimeter = `2 × (Width + Radial Thickness) = 2 × [200 + (800 − 400) ÷ 2] = 800 mm (0.8 m)`.
- Total film linear consumption per coil = `51 turns × 0.8 m = 40.8 meters` (prior to pre-stretch elongation).

### 5. Practical Throughput per Hour
Assuming an average manual loading, tail-tacking, and unloading time of **15 seconds** per coil:
`Total Cycle Duration = 25.5 s (wrap) + 15 s (handling) = 40.5 seconds`.
`Theoretical Capacity = 3,600 s/h ÷ 40.5 s/coil ≈ 88 coils/hour`.

<h2 id="options">Modular Options for High-Throughput Automation</h2>

To eliminate handling bottlenecks on continuous extrusion lines, the FPH-300N can be equipped with modular field upgrades:

- **Pneumatic Cut-and-Clamp System:** Automatically grips and hot-cuts the film tail at cycle completion, keeping the operator away from the rotating ring.
- **Synchronized Logo Tape Applicator:** Feeds printed identification tape under the outer stretch film layer for branding and anti-counterfeiting.
- **Category 4 Safety Light Curtains:** Replaces manual mesh swing doors with optical safety barriers for unhindered overhead crane loading.
- **In-Line Driven Conveyor Integration:** Replaces manual offloading with motorized indexing rollers for fully automated coiler-to-palletizer transfer.

<h2 id="selection-checklist">Engineering Selection Checklist: Parameters to Provide</h2>

To confirm machine sizing and ring clearance, provide our engineering department with:

1. **Dimensional Envelope:** Minimum and maximum Coil ID, OD, and Width (axial height).
2. **Payload Specifications:** Minimum and maximum coil weights (kg).
3. **Product Surface Characteristics:** Smooth wall, corrugated spiral, or braided rubber.
4. **Packaging Substrate:** LLDPE stretch film, VCI anti-corrosion film, or reinforced crepe paper.
5. **Target Line Rate:** Coils per hour produced by upstream coilers or winders.
6. **Electrical Standards:** Plant line voltage, frequency, and local control voltage requirements.

<h2 id="safety">Safety Architecture and EN 415-10 Compliance</h2>

The FPH-300N is engineered in compliance with **EN 415-10** (Safety of Packaging Machines) and risk assessed to **ISO 12100**:

- **Physical Guarding:** Heavy-gauge yellow wire-mesh guard enclosures eliminate accidental operator contact with the high-speed orbital ring and roller pinch points.
- **Interlocked Access:** Guard doors feature positive-break safety interlock switches that enforce machine stopping if the enclosure is breached during operation.
- **Deceleration Profile:** VFD braking units prevent free-wheeling ring run-out in the event of emergency stop (E-stop) activation or power interruption.
- **Workpiece Stability:** Dual polyurethane side guide rollers prevent tall, narrow coils from tilting or dislodging during high-speed rotation.

<h2 id="engineering-faq">Engineering FAQ</h2>

**Q: Can the FPH-300N accommodate heavy wire coils or rigid steel pipes?**
A: The standard FPH-300N chassis is optimized for coils up to 100 kg. For heavy copper tubing, steel wire, or large HDPE pipe bundles, refer to our heavy-duty FPH-400 and FPH-500 series featuring structural channel frames and dual-chain ring drives.

**Q: Why does film buildup occur primarily inside the coil eye?**
A: Because the inner circumference is smaller than the outer circumference, the orbital ring deposits an identical number of film layers across a shorter perimeter. This creates a higher overlap ratio (e.g., 75% ID vs. 50% OD), reinforcing the core.

**Q: Is the machine compatible with non-stretch paper wrapping?**
A: Yes. By replacing the stretch film carriage with our constant-tension paper unwinding spindle, the machine operates with crepe paper, HDPE woven wrap, or micro-perforated VCI rust-inhibiting paper.

**Q: Which harmonized standards govern CE certification for this system?**
A: The equipment complies with Machinery Directive 2006/42/EC, utilizing EN 415-10 for packaging machinery mechanical safety and EN 60204-1 for electrical equipment.

<h2 id="next-step">Project Next Steps and Engineering Inquiries</h2>

1. **Submit Application Data:** Forward your maximum and minimum coil dimensions, coil weights, and required line speeds to **info@fhopepack.com**.
2. **Technical Feasibility Proposal:** Our engineering team returns a formal technical quotation with ring diameter clearances within 24 hours.
3. **Integration Drawing:** We supply certified 2D/3D CAD layout drawings to integrate the wrapping station directly into your extrusion or coiling line.

<h2 id="related-reading">Related Reading</h2>

- [FPH-300 Hose Coil Wrapping Machine Overview](https://www.fhopepack.com/Hose-packaging-machine/Hose-wrapping-machine-FPH-300.html)
- [Automatic Hose Coiling and Strapping Integration Line](https://www.fhopepack.com/Hose-packaging-machine/Hose-coiling-and-strapping-machine.html)
- [Hose Coil, Cable Coil Wrapping Machine and Pallet Wrapper Systems](https://www.fhopepack.com/videos/hose-coilcable-coil-wrapping-machine-and-pallet-wrapper/)
- [Heavy Steel Wire Coil Orbital Wrapping Solutions](https://www.fhopepack.com/videos/steel-wire-coil-wrapping-machine-wire-coil-packing-solution/)
- [Hose Wrapping Machine Solutions for HDPE Pipe Coils](https://www.fhopepack.com/videos/hose-wrapping-machine-hdpe-pipe-coil-packing-machines/)
- [Orbital Tube Packing Solutions for Copper Tube and Extrusions](https://www.fhopepack.com/videos/hose-wrapping-machinecopper-tube-and-pipe-packing-machines-for-steel/)

<h2 id="sources">Reference Standards and Technical Sources</h2>

- Technical Specifications: FHOPEpack FPH-300 Industrial Series Hose Wrapping Systems
- Machine Demonstration Video: [FHOPE Hose Coil Orbital Wrapping Machine Demonstration](https://www.fhopepack.com/videos/)
- Kinematics and Film Calculations: FHOPE Mechanical Design Whitepaper (Coil Packaging Division)
- Safety Harmonized Standards: EN 415-10:2014 (Packaging Machines Safety); ISO 12100:2010 (Safety of Machinery - General Principles for Design); EN 60204-1 (Electrical Safety)

<p><strong>Last reviewed:</strong> 2026-10-17</p>