Yönetici Özeti — Packaging industrial tube bundles requires balancing ring throat bore clearance, material load rating, and bundle length. Loose or strapped tube clusters in steel, copper, and rigid polymer must traverse an orbital wrapper without profile sag, center-line shift, or throat collision. The E500 accommodates bundle outer diameters (OD) from 200 to 500 mm under heavy loads up to 500 kg. The E600 expands ring throat access to 600 mm OD for lighter bundles up to 200 kg down to 800 mm in length. For large multi-tube master bundles, the E1000 handles cross-sections up to 1000 mm OD and 400 kg. Sizing an orbital cell requires synchronizing ring rotational speed with infeed/outfeed conveyor velocity and engineering external mid-span supports for long bundles exceeding standard 2000 mm conveyor decks.
What the ring does to a tube bundle
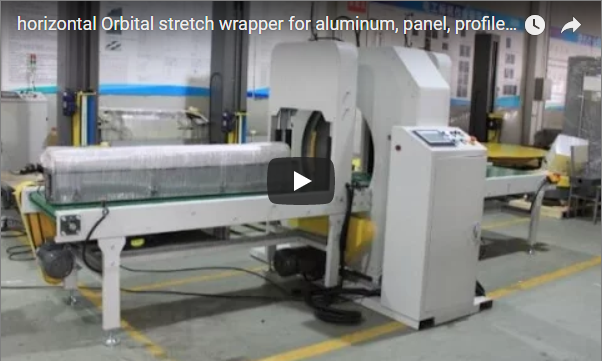
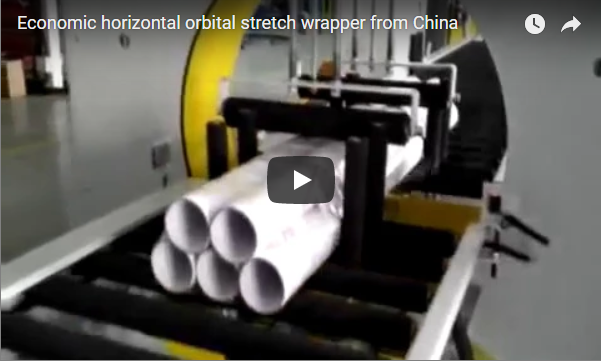
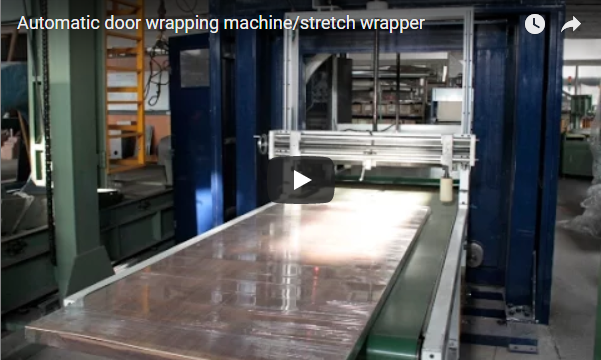
An orbital stretch wrapper passes elongated tube bundles axially through a rotating structural ring. Dual drive friction wheels rotate the ring within a vertical housing while motorized conveyor beds propel the bundle through the center bore.
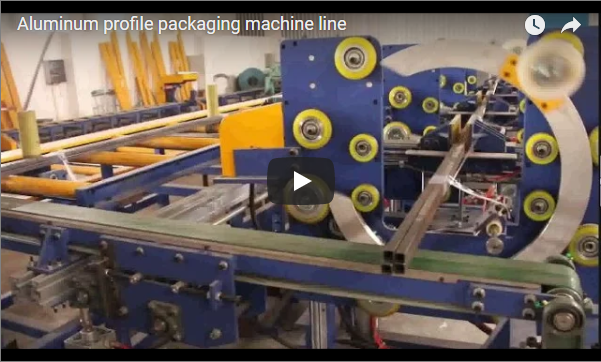
During passage, film rolls mounted to the ring orbit the product, dispensing stretch film, protective paper, or composite woven tape in a continuous helical spiral. Pneumatic side guide rollers and top press wheels stabilize loose individual tubes into a rigid, non-shifting geometric cluster.
Once the trailing end reaches the wrapping perimeter, the ring applies programmable reinforcement wraps. An automated pneumatic clamp-and-cut arm grips the film web, slices it clean, and retains the leading tail for the next tube sequence without manual operator threading.
Pencere boyutu: E500, E600, E1000
Selecting the correct orbital wrapper requires matching bundle diameter, single-bundle weight, and bundle length to machine capabilities.
| Makine modeli | Bundle OD Window | Maksimum Yük | Minimum Paket Uzunluğu | Halka Dönme Hızı | Conveyor Platform (L × W) | Motor gücü |
|---|---|---|---|---|---|---|
| E500 Yatay Sarma Makinesi | 200 – 500 mm | 500 kg | > 1500 mm | 10–60 dev/dak | 2000 × 700 mm | ~4.5 kW |
| E600 Yatay Sarma Makinesi | 200 – 600 mm | 200 kg | > 800 mm | 10–60 dev/dak | 2000 × 800 mm | ~4.5 kW |
| E1000 Yatay Sarma Makinesi | 400 – 1000 mm | 400 kg | > 1000 mm | 10–60 dev/dak | 2000 × 1200 mm | ~4.5 kW |
Model Selection Rules
- Select E500 for heavy bundles: When bundle OD is within 200–500 mm and total bundle mass reaches 200–500 kg (typical for solid copper rods or thick-wall carbon steel conduit).
- Select E600 for large, lightweight bundles: When bundle OD expands up to 600 mm but bundle mass stays below 200 kg, especially when packaging shorter cuts (>800 mm).
- Select E1000 for large industrial bundles: When bundle OD spans 400–1000 mm with loads up to 400 kg.
Boundary Conflict Case: OD 550 mm with 300 kg Load
If your product bundle measures 550 mm OD with a total mass of 300 kg, it falls outside standard envelopes. Although 550 mm fits inside the E600 ring bore, the 300 kg weight exceeds the E600 roller bed limit of 200 kg. This application must step up to the E1000 (handling up to 400 kg across a 1200 mm wide conveyor) or specify an engineered chassis upgrade on the E500/E600 frame.
Bundle OD, load and the throat
A bundle outer diameter (OD) represents the circumscribed circle enclosing the tube pack. For standard hexagonal nested tubes (such as a 7-tube bundle consisting of 1 center tube enclosed by 6 outer tubes):
Bundle OD = 3 × Tube OD
For rectangular or irregular tube racks, calculate the maximum cross-sectional diagonal:
Cross-Section Diagonal = √(Width² + Height²)
The internal ring clearance throat must allow clearance for both the bundle profile and the revolving film roll carriage. Operating a 500 mm OD bundle inside an E500 frame leaves an envelope buffer that prevents structural collisions if bundle strapping loosens during transit.
Furthermore, total payload governs bearing fatigue. When processing dense alloy bundles, high static point loads require structural V-rollers rather than flat cylindrical sleeves to keep the center of gravity aligned with the ring center line.
Conveyor length for long bundles
Standard machine configurations provide 2000 mm motorized infeed and 2000 mm motorized outfeed conveyors. Standard factory bundles frequently run 6 m (6 m) in length.
When a 6 m bundle rests on a 2000 mm conveyor, 4000 mm extends unsupported across the plant floor. As the bundle advances into the orbital throat, excessive overhang induces cantilever sag. If vertical deflection exceeds 15 mm, the lead end will scrape the ring frame or jam against the pneumatic cut-and-clamp carriage.
To prevent bundle tilt and throat collision on long bundles:
Required Intermediate Supports = (Bundle Length - Infeed Conveyor Length - Outfeed Conveyor Length) / Maximum Allowable Span
For a 6000 mm bundle with standard 2000 mm infeed and outfeed beds:
- Free unsupported overhang length = 2000 mm.
- Maintain an intermediate support span
S_max ≤ 1500 mm. - Add external idle or driven V-roller extension stands to ensure at least two contact support zones are engaged beneath the bundle at all times throughout the wrapping sequence.
Cycle time from conveyor and ring speed
Total bundle cycle duration is calculated by combining linear conveyor transit time, dwell time for stationary head and tail reinforcement wraps, and mechanical handling pauses:
Total Cycle Time (seconds) = (Bundle Length / Conveyor Speed) × 60 + (Reinforcement Wraps / Ring Speed) × 60 + Dwell Overhead
Sample Calculation: 6-Meter Bundle
- Bundle length: 6.0 m
- Conveyor speed: 8.0 m/min (within the standard 3–12 m/min variable range)
- Ring speed: 30 r/min (inverter controlled, 10–60 r/min range)
- Reinforcement wraps: 10 total wraps (5 stationary wraps at head, 5 at tail)
- Mechanical clamp, cut, and indexing dwell: 6 seconds
- Linear Transit Time:
(6.0 m / 8.0 m/min) × 60 = 45 seconds - Reinforcement Rotation Time:
(10 wraps / 30 r/min) × 60 = 20 seconds - Mechanical Dwell Overhead:
6 seconds - Calculated Production Time:
45 + 20 + 6 = 71 seconds per bundle(yielding approximately 50 completed bundles per hour).
Why Short Bundles on the E600 Run Faster
Short bundles (e.g., 1000 mm on an E600) clear the ring faster: linear transit is 1000 mm ÷ 8 m/min ≈ 7.5 s, plus the turns. With lower bundle inertia, acceleration ramps are faster, reducing overall handling pauses between successive cycles.
Film width and overlap
Helical wrapping overlap is governed by film spool width, linear conveyor speed, and ring rotational frequency.
Pitch Advance per Ring Revolution (mm/rev) = (Conveyor Speed in m/min / Ring Rotational Speed in r/min) × 1000
Overlap Percentage = [1 - (Pitch Advance / Film Width)] × 100%
Media Specifications Across Models
- E500 ve E600: Accommodates roll widths of 150–300 mm, outer roll diameters of 100–250 mm, on standard 50 mm core IDs.
- E1000: Expands roll width capacity from 100 mm up to 500 mm (outer roll diameter 100–250 mm, 50 mm core ID) to provide wide surface coverage over large-envelope tube groupings.
Adjusting the mechanical core brake regulates stretch tension. For thin-walled plastic or polished brass tubing, apply low tension with 50% overlap. For rigid carbon steel, increase film carriage tension to secure bundles without external steel banding.
Güvenlik ve altyapı hizmetleri
Every orbital wrapper installation must integrate verified utility drops and safety interlocks prior to production release.
Yardımcı Program Gereksinimleri
- Elektrik Beslemesi: 380V AC, 3-Phase, 50 Hz.
- Bağlı Yük: Approximately 4.5 kW across main ring drives and dual conveyor gearmotors.
- Pnömatik: Clean, dry compressed air at 5–8 kgf/cm² (0.5–0.8 MPa) to operate vertical clamp stabilizers, top hold-down rolls, and the pneumatic cut-and-clamp jaw.
- vakıf: Flat, vibration-isolated industrial reinforced concrete slab rated to bear dynamic machine weight (overall dimensions up to L5200 × W1800 × H1800 mm).
Operasyonel Güvenlik
Integrated safety enclosures comply with international wrapping machinery directives:
- Guarded emergency stop pushbuttons positioned at operator control panels and conveyor loading stations.
Seçim kontrol listesi
Use this checklist to confirm your application parameters prior to final wrapper procurement:
- Tube Parameters: Outer diameter, wall thickness, material (steel, copper, PVC, aluminum).
- Paket Profili: Total outer diameter (200–500 mm for E500; 200–600 mm for E600; 400–1000 mm for E1000).
- Paket Ağırlığı: Total mass per bundle (confirm against 500 kg max for E500, 200 kg for E600, 400 kg for E1000).
- Paket Uzunluğu: Minimum length (>800 mm for E600, >1000 mm for E1000, >1500 mm for E500) and maximum length.
- Conveyor Extensions: Number of external V-roller support stands required for long bundles (>3000 mm).
- Ambalaj Medyası: Stretch film, anti-corrosion VCI paper, or woven composite tape (film width 100–500 mm, roll OD 100–250 mm, 50 mm core).
- Tesis Yardımcı Hizmetleri: 380V 50Hz electrical supply and 5–8 kgf/cm² compressed air drop at installation site.
Mühendislik SSS
Q: Can the E600 wrap a 500 kg bundle if the diameter is only 450 mm? A: No. Although a 450 mm OD bundle clears the E600 ring throat (200–600 mm range), the E600 conveyor and roller bed are rated for a maximum of 200 kg. A 500 kg load will overload conveyor drive rollers and bearings. You must specify the E500, which is built to support up to 500 kg.
Q: What happens if a 6-meter flexible plastic tube bundle sags inside the wrapper? A: Excessive sag (deflection greater than 15 mm) causes the bundle leading edge to strike the bottom of the revolving ring throat or catch on the lower film clamp assembly. Flexible or long bundles require external support roller stands and pneumatic hold-down rollers to maintain horizontal alignment along the pass-line.
Q: Why do short tube bundles run on an E600 achieve higher hourly throughput than 6-meter bundles? A: Short bundles (such as 1000 mm) traverse the wrapping zone in under 8 seconds at an 8 m/min line speed. Because short bundles present less mass inertia, the conveyor starts, indexes, and clears faster, reducing overall cycle dwell and yielding higher hourly unit volumes.
Q: How do we prevent bundle telescoping or shifting during continuous wrapping? A: Pneumatically actuated vertical side-guide rollers align the bundle laterally on the infeed bed, while adjustable overhead pressure wheels clamp the tubes downward. This mechanical constraint holds loose tubes in a fixed array while rotational film tension is applied.
Sonraki adım
Submit your production bundle requirements to receive an engineered wrapping system proposal:
- Provide Your Application Parameters: Send your minimum/maximum bundle OD, bundle length range, single-bundle weight, and tube material to our packaging application engineers.
- Receive Engineered Layout: Within 24 to 48 hours, our technical team will return a formal proposal containing 3D layout drawings, conveyor extension engineering, ring clearance calculations, and guaranteed cycle-time projections.
- Factory Acceptance Trials: Ship sample tube profiles to our facility for wrapping test runs, film overlap verification, and cycle optimization prior to final delivery.
Son gözden geçirme tarihi: 21.09.2026