Zhrnutie
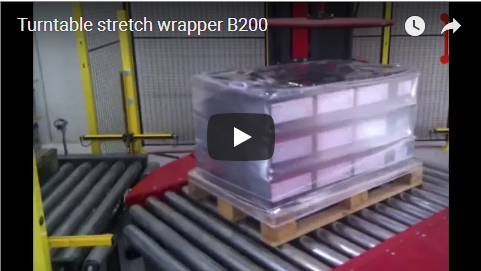
The B series is a heavy-duty, fully automatic turntable stretch wrapper engineered for continuous roller conveyor lines. An integrated overhead gantry automatically measures and dispenses a protective top poly sheet over the pallet load before the rotary turntable applies high-tension LLDPE stretch film up the sides, securing a 5-sided weatherproof barrier. Built for pallet loads up to 1,800 kg on a 2,200 mm structural turntable running up to 12 rpm, the system features a 250% powered pre-stretch carriage delivering throughputs of at least 24 to 26 loads per hour. Below is the structural technical specification, film overlap calculation, cycle time budget, and consumption analysis.
This integrated packaging cell combines an overhead PE film dispenser with a powered roller turntable wrapper to achieve IP54-equivalent dust and splash containment. By locking the draped waterproof top cap beneath the final upper wraps of power-stretched film, the system eliminates water pooling and pallet load shifting during intermodal transport.
Obsah
- Trať, stanica za stanicou
- Údaje série B
- Prekrytie z rýchlosti otočného taniera a vozíka
- Rozpočet času cyklu
- Fólia na jedno nabitie pri 250 % predbežnom natiahnutí
- Kontrolný zoznam výberu
- bezpečnosť
- Často kladené otázky týkajúce sa inžinierstva
- Ďalši krok
- Súvisiace čítanie
- Zdroje
Trať, stanica za stanicou
- Infeed Entry. A forklift or upstream automated guided vehicle (AGV) positions the pallet on the powered infeed roller conveyor. Optical proximity sensors confirm pallet orientation and square alignment.
- Top Sheet Application. As the conveyor indexes the load into position, the overhead gantry film dispenser unrolls, cuts, and drapes a low-density polyethylene (LDPE) cover sheet symmetrically across the top of the cargo.
- Primary Stretch Wrapping. The load enters the motorized turntable station. Variable frequency drives (VFD) ramp rotation up to 12 rpm. The powered pre-stretch carriage tracks vertically, securing reinforcement winds at the pallet base, spiraling up the load face, and locking down the top sheet edges with dedicated top layers (0–99 programmable wraps).
- Automatic Cut, Clamp, and Wipe. At cycle completion, an electro-pneumatic scissor gripper captures the film web. An impulse hot-wire mechanism cleanly severs the film, while an integrated trailing brush wipes the tail securely against the pallet. The pneumatic clamp holds the leading edge in standby for the subsequent pallet.
- Výpustný otvor. The conveyor drives the unitized pallet to the outfeed buffer accumulation line for forklift removal or direct transfer to automated high-bay racking.
The conveyor line integration is fully modular. All operational cycles execute without operator intervention via a centralized programmable logic controller (PLC) network. Conveyor pass-line height, roller pitch, roll width, and film thickness are calibrated to client specifications during design validation.
Údaje série B
| Technické parametre | Specification / Tolerance |
|---|---|
| Automation Rating | Fully automatic, continuous inline operation |
| Rated Line Throughput | ≥ 24–26 pallet loads per hour (load-dependent) |
| Maximálna nosnosť | 1,800 kg (balanced dynamic rating) |
| Turntable Assembly | 2,200 mm diameter, ~400 mm top-of-roller height, slew-bearing ring gear & dual heavy-duty chain drive |
| Rýchlosť gramofónu | 0–12 rpm (adjustable via VFD), soft start / controlled decel, home-position auto-alignment |
| Špecifikácia filmu | LLDPE stretch film, 25 µm (0.025 mm), 500 mm web width, 76 mm core, 500–1,500 m roll |
| Film Delivery Pre-Stretch | 250% standard (1 m yield = 3.5 m applied); field-adjustable 100% to 300% via gear sets |
| Pohon filmového vozíka | VFD inverter-controlled lift mechanism; vertical linear travel speed at 2.9 m/min |
| Detekcia výšky nákladu | High-accuracy diffuse reflection retro-reflective photoelectric sensor |
| Reinforcement Wind Settings | Independent base, middle, and top parameters: 0–99 wraps; multi-cycle re-wrap enabled |
| Architektúra riadenia systému | Industrial PLC with touchscreen HMI; lockable main disconnect; mushroom E-stop pushbuttons |
| Inštalovaný výkon pohonu | Turntable: 0.75 kW; Roller conveyor: 0.75 kW; Carriage lift: 0.37 kW; Pre-stretch drive: 0.37 kW |
| Pneumatic & Electrical Supply | 3-Phase 380 V ±10%, 50 Hz; clean compressed air at 0.6–0.8 MPa (6–8 bar) |
Prekrytie z rýchlosti otočného taniera a vozíka
Turntable rotational speed and carriage elevation speed govern the effective film pitch. At a continuous 12 rpm, each table rotation consumes:
t_rev = 60 s ÷ 12 rpm = 5.0 s
The carriage vertical elevator operates at 2.9 m/min (48.3 mm/s):
v_carriage = 2,900 mm ÷ 60 s ≈ 48 mm/s
| Mechanická kontrola | Inžiniersky výpočet | Kvantitatívny výsledok |
|---|---|---|
| Carriage Rise per Rotation | 48 mm/s × 5.0 s | rozstup 240 mm |
| Nominal Film Width | Industrial cast/blown LLDPE | 500 mm |
| Effective Vertical Overlap | (500 mm − 240 mm) ÷ 500 mm | 52% prekrytie |
Operational Rule: Reducing carriage hoist frequency increases overlap percentage and containment force at the expense of cycle time; raising turntable speed increases wrap density. To maintain package integrity under ASTM D4169 vibration profiles, set the vertical overlap to ≥ 50%, then program dedicated reinforcement bands at the pallet-to-load shear junction.
Rozpočet času cyklu
Evaluation parameters based on an ISO standard pallet: 1,200 mm (L) × 1,000 mm (W), height 1,650 mm (inclusive of timber skid), corner diagonal = √(1,200² + 1,000²) ≈ 1,562 mm (well within the 2,200 mm turntable boundary). Configuration: 3 base wraps, 3 top wraps.
| Fáza cyklu | Kinematic Formula & Parameters | Čas vykonania |
|---|---|---|
| Carriage Ascent | 1,650 mm ÷ 48 mm/s | ≈ 34 s |
| Carriage Descent | 1,650 mm ÷ 48 mm/s | ≈ 34 s |
| Base Reinforcement Wraps | 3 revolutions × 5.0 s | 15 s |
| Top Cap Anchoring Wraps | 3 revolutions × 5.0 s | 15 s |
| Total Active Wrapping Time | 34 s + 34 s + 15 s + 15 s | 98 s |
| Conveyor Index, Top Cap Drape, Cut/Wipe | Sequenced conveyor positioning & cycle reset | 40 s |
| Total Gross Cycle Time per Unit | 98 s + 40 s | 138 s |
| Line Capacity (Hourly Output) | 3 600 s ÷ 138 s | ≈ 26.1 loads/hour |
Inžinierske posúdenie: The realized throughput of 26 pallets per hour exceeds the baseline rating of 24 LPH. Because top-sheet roll dispensing and cutting occur concurrently while the pallet indexes forward onto the turntable, top-capping contributes minimal overhead to the cycle. On applications requiring higher throughput, setting the PLC to a single-ascent wrap program saves approximately 34 seconds, boosting line yield beyond 34 LPH.
Fólia na jedno nabitie pri 250 % predbežnom natiahnutí
| metrický | Výpočet | Hodnota |
|---|---|---|
| Total Table Revolutions per Load | (34 s ÷ 5.0 s) + (34 s ÷ 5.0 s) + 3 + 3 | ≈ 19.6 otáčok |
| Pallet Perimeter Profile | 2 × (1.2 m + 1.0 m) | 4.4 m |
| Total Stretched Film Applied | 19.6 zákrut × 4.4 m | ≈ 86.2 m |
| Unstretched Film Feed at 250% Yield | 86.2 m ÷ (1 + 2.5) = 86.2 m ÷ 3.5 | ≈ 24.6 m |
| Applied Film Mass (Density: 920 kg/m³) | 24.6 m × 0.5 m × 0.000025 m × 920 kg/m³ | ≈ 0.283 kg (283 g) |
| Production Capacity per 1,500 m Master Roll | 1,500 m ÷ 24.6 m | ≈ 61 loads |
At 250% powered pre-stretch, 1.0 meter of roll stock yields 3.5 meters of tensioned film around the cargo. Utilizing low-end friction-brake carriages (100% pre-stretch) increases raw material consumption by up to 75%, requiring 43.1 m of roll stock per pallet (approx. 0.495 kg), underscoring the ROI delivered by precision powered pre-stretch heads.
Kontrolný zoznam výberu
- Load Parameters: Minimum/maximum footprint (L × W), overall height, payload mass, and load overhang/underhang.
- Ciele priepustnosti: Required pallets per hour during peak shift demand.
- Environmental Sealing Requirements: Top sheet gauge (e.g., 30–60 µm LDPE) and weatherproofing specification (dust-proof vs. splash-resistant).
- Plant Conveyor Interfacing: Conveyor top-of-roller (TOR) elevation, line velocity, roller pitch, and upstream/downstream handshake logic.
- Consumable Specs: Gauge, core diameter, and elongation properties of local machine-grade LLDPE film.
- Dimenzovanie úžitkových vozidiel: Facility input voltage, total connected electrical load, and regulated dry compressed air supply.
bezpečnosť
The B series is manufactured in compliance with EN-415 6 (Safety of Packaging Machines: Pallet Wrapping Machines), EN ISO 12100: 2010 (Risk Assessment), and EN-60204 1 (Electrical Equipment of Machines).
Primary hazard zones include rotating turntable machinery, the vertical hoist carriage, and the pneumatic overhead sheet cutting mechanism. Full system installations include:
- Perimeter mesh safety guarding (height ≥ 2,000 mm) with ISO 14119 interlocked maintenance access doors.
- Category 4 / PL e optical safety light curtains positioned at conveyor infeed and discharge stations, configured with selective hardware muting sensors to allow pallet passage while arresting motion if personnel enter.
- Dual-channel safety E-stop circuits, motor circuit breakers with lockable disconnects (OSHA LOTO compliant), and pneumatic dump valves to vent residual stored air pressure during an emergency stop.
Často kladené otázky týkajúce sa inžinierstva
Q: Why integrate a top sheet dispenser instead of manual top sheeting? A: Manual top draping introduces line stoppages, inconsistent edge coverage, and workplace safety risks. The automated dispenser guarantees precise sheet placement and continuous conveyor operation, ensuring an IP54 moisture-tight wrap when sealed by the upper stretch wraps.
Q: Can the dispenser handle protective PE foam or bubble roll stock? A: Yes. The powered roll-unwind carriage and pneumatic guillotine cutter handle LDPE poly sheeting, anti-static foam, or thin air-bubble film without mechanical modifications.
Q: What guarantees that the top sheet will not lift off during high-wind outdoor storage? A: The PLC is programmed to overlap the top sheet with at least 2–4 full revolutions of machine stretch film across the uppermost 150 mm of the load corners, locking the cap securely against the carton stack.
Q: Is operator oversight required during automatic operation? A: No. The line operates fully unmanned. Automated photocell sensing, powered film clamping, impulse cutting, and pneumatic wipe-down handle the full wrap cycle. Forklifts or AGVs interact exclusively with the infeed and discharge accumulation zones.
Q: Can the system be deployed without infeed/outfeed conveyors? A: Yes. Standalone configurations allow direct forklift or hand-truck loading. In this configuration, the turntable roller bed is replaced with a heavy-duty checker-plate steel deck, or fitted with a roller pneumatic locking brake to prevent pallet displacement during loading.
Ďalši krok
- Parametre odoslanej žiadosti: Forward your maximum load dimensions, gross weights, and line target rates to info@fhopepack.com.
- Engineering Simulation: Our packaging engineers model your cycle time, overlap percentage, and pre-stretch yield ratios.
- Formal Proposal Delivery: Receive an integration drawing, layout footprint, and formal quote within 24 hours.
Súvisiace čítanie
- Automatický baliaci stroj na palety B300 (produkt)
- Paletový baliaci stroj s dávkovačom vrchného listu
- Dávkovač PE fólií na automatické zakrývanie paliet
- Inline otočný baliaci stôl paliet
- Rotačné rameno na balenie paliet s krycou vrchnou plachtou
- Otočná zavinovačka B200
- Baliaci stroj s rozťahovacím ramenom a dávkovačom vrchného listu
Zdroje
- FHOPE Technical Data Sheets: Automatic Pallet Wrapping Machine B300 Series
- European Standard EN 415-6: Packaging Machines Safety — Part 6: Pallet Wrapping Machines
- International Standard EN ISO 12100:2010: Safety of Machinery — General Principles for Design
- European Standard EN 60204-1: Safety of Machinery — Electrical Equipment of Machines
Naposledy skontrolované: 19. 10. 2026
<iframe width="940" height="535" src="https://www.youtube.com/embed/gow0GlDQ-Js" frameborder="0" allow="accelerometer; autoplay; clipboard-write; encrypted-media; gyroscope; picture-in-picture; web-share" referrerpolicy="strict-origin-when-cross-origin" allowfullscreen></iframe>