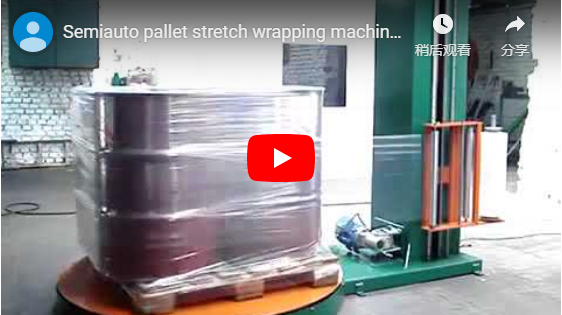
Резюме The B200 inline turntable stretch wrapper integrates directly into automated conveying lines, eliminating manual forklift staging by automatically receiving, wrapping, and discharging palletized goods. Engineered with a heavy-duty roller turntable, it supports standard payloads of 2,000 kg (expandable to 3,000 kg) with variable-frequency rotational speeds of 3–12 rpm. An integrated pneumatic top plate stabilizes lightweight, loose, or tall loads during the rotation cycle, while infeed, turntable, and outfeed roller conveyors operate on a single coplanar level for smooth transfer.
Содержание
- Как работает встроенный цикл B200
- Технические характеристики поворотного стола B200 для стретч-упаковки
- Когда необходима пневматическая верхняя пластина
- Cycle time and throughput dynamics at 3–12 rpm
- Film carriage and power pre-stretch system
- B200 engineered options
- Controls, safety logic, and compliance
- Контрольный список для выбора упаковочной машины для стретч-пленки с поворотным столом.
- Часто задаваемые вопросы по инженерным вопросам
- Следующий шаг
- Связанное чтение
- Источники
Как работает встроенный цикл B200
The B200 integrates upstream packaging, stretch wrapping, and downstream logistics into a single continuous handling cycle. By eliminating forklift transport at the wrapping station, it minimizes product handling damages and maintains consistent line velocity.
[Infeed Roller Conveyor] ---> [Coplanar Roller Turntable] ---> [Outfeed Roller Conveyor]
                                        │
                         [Pneumatic Top Plate Clamp]
                         [Rotational Stretch Cycle]
                         [Auto Film Clamp & Cut]
A standard automated wrapping sequence proceeds as follows:
- Infeed Transfer: The pallet moves from the plant infeed roller conveyor onto the motorized roller turntable. Both systems are aligned coplanar at identical pass-line heights (typically 450 mm to 550 mm above finished floor level) to prevent pallet tipping or roller impact shocks.
- Стабилизация нагрузки: For unstable or lightweight stacks, the overhead pneumatic platen lowers, applying controlled vertical pressure (0.2–0.6 MPa adjustable) to secure the upper tiers.
- Automated Height Detection & Wrapping: A retroreflective photoelectric sensor detects the top edge of the load. The variable-frequency drive (VFD) accelerates the turntable smoothly up to target speed (3–12 rpm), while the power pre-stretch carriage ascends and descends along the mast to apply programmed bottom, body, and top wrap counts.
- Pneumatic Clamping & Cutting: Upon cycle completion, the pneumatic clamp captures the film tail, an impulse hot-wire or serrated blade severs the web, and a wipe-down brush secures the trailing film edge flush against the load.
- Выпуск готовой продукции: The top platen retracts upward, and the synchronized double-strand chain-driven turntable rollers discharge the wrapped unit load onto the outfeed accumulation conveyor.
The turntable roller bed utilizes a continuous double-strand drive chain mechanism, ensuring zero roller slippage under concentrated 2,000–3,000 kg downward loads.

Технические характеристики поворотного стола B200 для стретч-упаковки
| Технические параметры | Standard Engineering Configuration | Вариант повышенной прочности / удлиненный вариант |
|---|---|---|
| Максимальная грузоподъемность | 2,000 kg (dynamic rated) | От 2,500 кг до 3,000 кг |
| Скорость вращения поворотного стола | 3–12 rpm (VFD controlled acceleration/deceleration) | Custom low-speed profile (1–8 rpm) |
| Roller Conveyor Pass-Line Height | 450 мм - 550 мм (регулируется) | Engineered to plant specification |
| Power Pre-Stretch Ratio | Up to 200% fixed gearing (1 m roll yields 3.0 m) | Custom 250% to 300% gear ratios |
| Диаметр поворотного стола | 1,800 мм | 2,000 мм до 2,200 мм |
| Maximum Load Wrapping Height | 2,100 мм | 2,400 мм до 2,800 мм |
| Аппаратное обеспечение контроллера | OMRON Sysmac PLC with digital operator interface | Siemens S7-1200 / Allen-Bradley PLC |
| Требования к подаче воздуха | 0.6–0.8 МПа сухой, фильтрованный сжатый воздух | Air prep unit included with auto-drain |
Film changeover downtime is optimized: the pre-stretch carriage features an easy-access open-door threading design, reducing roll replacement time to approximately 10 seconds.
Когда необходима пневматическая верхняя пластина
The pneumatic top stabilizing plate applies constant downward clamping force to the upper load face during turntable rotation. This device is required under the following operating conditions:
- Low-Density or Empty Cartons: Lightweight corrugated packaging tends to drift or deform when subjected to high film web tension at perimeter corners.
- Unbonded Top Tiers: Unbanded, unglued, or column-stacked boxes and bags can dislodge due to centrifugal forces before containment film wraps the upper edge.
- High Aspect Ratio Stacks: Pallet units with a high center of gravity (stack height greater than 1.8 × pallet width) experience pronounced overturning moments during the rotational start phase.
For dense, high-friction, interlocked loads (e.g., rigid wooden crates or filled liquid drums), the cycle operates in bypass mode with the top platen locked in the upper home position.
Cycle time and throughput dynamics at 3–12 rpm
Total cycle time per pallet (T_cycle) consists of turntable rotational wrapping time plus mechanical conveyor handling and auxiliary sequence steps:
T_cycle = T_acc/dec + (N_winds ÷ RPM × 60) + T_infeed + T_outfeed + T_aux
Где:
N_winds: Total carriage turns applied across base reinforcement, upward traverse, top overlap, downward traverse, and base tie-off.RPM: Programmed steady-state turntable speed (3–12 rpm).T_aux: Cumulative time for top platen motion, photoelectric load sensing, and automated cut/wipe sequences (typically 12–18 seconds).
Representative Cycle Time Calculations (Assuming 15 Total Rotational Winds)
- High-Throughput Configuration (12 rpm, Stable Loads):
- Rotational Phase: 15 winds ÷ 12 rpm = 1.25 minutes (75 seconds)
- Infeed, Outfeed, Soft Start/Stop, and Cut: ~25 seconds
- Общее время цикла: ~100 seconds per pallet (~36 pallets per hour)
- High-Care Configuration (3 rpm, Fragile or Unstable Stacks):
- Rotational Phase: 15 winds ÷ 3 rpm = 5.00 minutes (300 seconds)
- Infeed, Outfeed, and Top Plate Settling: ~30 seconds
- Общее время цикла: ~330 seconds per pallet (~10–11 pallets per hour)
Turntable acceleration and deceleration ramp rates are tuned in the OMRON PLC to prevent load shifting during speed transitions.
Film carriage and power pre-stretch system
The B200 utilizes a powered dual-roller pre-stretch film delivery carriage:
- Механическое преимущество: Standard 200% pre-stretch ratio mechanically elongates 1 meter of stretch film into 3 meters on the product. This reduces consumable film mass per pallet by up to 55% compared to friction-brake carriages.
- Drive Separation: A dedicated DC motor powers the pre-stretch rollers, isolating film elongation tension from the load-wrapping tension.
- Контроль натяжения: Web tension applied to the pallet corners is modulated via an analog dancer-arm potentiometer or load-cell feedback, preventing corner crushing on soft corrugated cartons.
- PLC Wrap Recipes: Bottom wrap counts, top reinforcement wraps, carriage elevation traverse speed, and intermediate reinforcement bands are independently configurable through the HMI screen.
B200 engineered options
The standard B200 chassis accommodates various operational requirements:
| Engineered Module | Техническое назначение | Target Operational Scenario |
|---|---|---|
| Floor-Mounted Approach Ramp | Bridges factory floor to turntable level | Pallet truck entry during off-conveyor servicing |
| Pneumatic Top Stabilizing Platen | Overhead clamping force (150–500 N adjustable) | Lightweight, loose, or tall carton stacks |
| Auto Film Clamping, Cutting & Wiping | Pneumatic tail gripper with thermal/shear cut | Fully automated, zero-operator inline cells |
| Extended Mast Assembly (2,800 mm) | Extends vertical carriage travel envelope | High-cube warehouse storage loads |
| Heavy-Duty Turntable (2,000 mm / 3,000 kg) | Structural reinforcement, high-capacity slewing ring | Heavy cast parts, ceramics, paper rolls |
| Washdown/Corrosion Protection | Custom epoxy, zinc primer, or stainless steel skin | High-humidity or cold-chain warehousing |
Controls, safety logic, and compliance
The B200 operates under an OMRON Sysmac control architecture. The operator panel includes manual cycle jog overrides, variable carriage speed potentiometers, and automatic emergency stop sequences.
Integrated inline cells include mandatory perimeter safety barriers compliant with international standards:
- Оценка рисков: Evaluated and designed in compliance with ISO 12100: 2010 (Безопасность машин и механизмов — Общие принципы проектирования).
- Packaging Machinery Safety: Соответствует EN 415-10: 2014 safety requirements for automated pallet wrappers.
- Защита ячейки: Interlocked safety fencing surrounds the turntable turning perimeter. Infeed and outfeed roller portals feature muting safety light curtains (Category 4 / PLe compliant) configured to distinguish pallet passages from personnel intrusion.
Контрольный список для выбора упаковочной машины для стретч-пленки с поворотным столом.
Before finalizing the packaging line layout, verify these operating parameters:
- Профиль поддона: Footprint dimensions (L × W), maximum load height, and maximum dynamic payload weight (kg).
- Throughput Demand: Target output capacity in pallets per hour (PPH) under peak line conditions.
- Геометрия конвейера: Infeed and outfeed roller heights, roller diameters, roller centers, and operational conveying speeds.
- Stack Integrity: Presence of loose top layers, light cartons, or high centers of gravity requiring a pneumatic top plate.
- Уровень автоматизации: Requirement for fully automated pneumatic film clamping, cutting, and heat-wiping mechanisms.
- Footprint & Access: Layout clearance for safety perimeter fences, maintenance access gates, and LOTO (Lockout/Tagout) power disconnects.
Часто задаваемые вопросы по инженерным вопросам
What is the maximum load capacity of the B200 turntable?
The standard B200 roller turntable is structurally rated for dynamic payloads up to 2,000 kg. For heavy industrial goods such as metal ingots, chemicals, or refractory blocks, an optional reinforced slewing bearing carriage upgrades total load capacity to 2,500–3,000 kg.
How does the pneumatic top plate prevent pallet damage?
The top plate uses a regulated pneumatic cylinder that exerts a controlled vertical clamping force downward onto the load. This prevents shifting or corner lift on light, unbanded cartons while allowing variable pressure adjustment (0.2–0.6 MPa) to avoid crushing fragile product boxes.
What rotational speeds does the turntable support?
The turntable is driven by an industrial gearmotor governed by an adjustable variable-frequency drive, operating smoothly between 3 rpm and 12 rpm. Acceleration and deceleration profiles are set within the PLC to prevent rotational load tipping.
Can the B200 operate as a fully unmanned packaging station?
Yes. When paired with powered infeed/outfeed roller conveyors and the automated pneumatic film clamping and cutting mechanism, the wrapper runs without an operator. Pallets index automatically into position, wrap according to stored recipe parameters, and discharge without manual intervention.
How long does a stretch film changeover take?
Film roll threading requires approximately 10 seconds. The power pre-stretch carriage incorporates a wide-opening latch door, allowing operators to drop in standard 500 mm (20 in) film rolls and thread the web across pre-stretch rollers without tools.
Следующий шаг
Integrate the B200 into your packaging line in three structured stages:
- Submit Factory Layout & Payload Specs: Send pallet dimensions, maximum unit weights, target pallets per hour, and conveyor pass-line heights to info@fhopepack.com.
- Review Detailed 48-Hour Technical Proposal: Our mechanical applications team will deliver a 2D/3D layout footprint, cycle-time simulation, and system quotation within 48 hours.
- Engineering Layout Verification: Schedule an engineering site review to coordinate floor anchoring, electrical bus routing, and conveyor interlocks.
Связанное чтение
- Automatic pallet stretch wrapping machine B200 product specifications
- Industrial turntable stretch wrapper family overview
- Video: automatic turntable pallet wrapping machine line in operation
- Video: online turntable pallet wrapping machine cell integration
- Video: automated palletizer and turntable stretch wrapper line
Источники
- Equipment specifications, carriage ratios, options: Fhopepack B200 Automatic Pallet Stretch Wrapping Machine
- Machine operational demonstration: B200 Turntable Stretch Wrapper Video Documentation
- Международные стандарты безопасности: ISO 12100:2010 Оценка рисков, связанных с оборудованием и EN 415-10:2014 Требования безопасности упаковочных машин
Последнее обновление: 21.09.2026