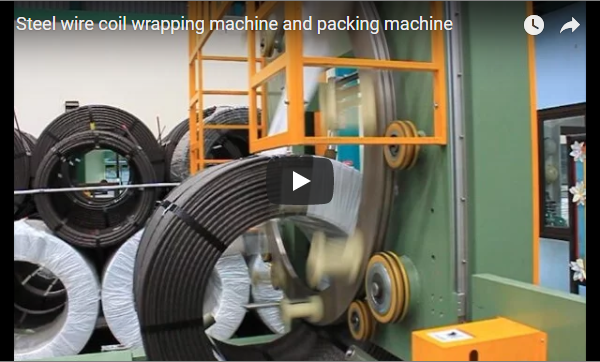
Резюме Big export coils are often too large or produced in too low a volume to justify a fully automated packaging line. A heavy-duty coil roller station supports and rotates the coil on two motor-driven, parallel turning rollers, allowing a compact two-person crew to inspect, wrap, apply metal outer protective sheets, and strap the entire pack in one dedicated workstation. By replacing crane-assisted turning between operations, the station eliminates crane wait times, prevents rigging shock loads on coil edges, and lowers handling cycle times by over 40%.
Содержание
- Чем занимается вальцовочная станция.
- Последовательность упаковки
- Зачем нужна крышка из стального листа?
- Нарезка листового материала и ремней по длине.
- Вальцовочная станция или упаковочная линия
- Безопасность на вальцовом участке
- Контрольный список выбора
- Часто задаваемые вопросы по инженерным вопросам
- Следующий шаг
- Связанное чтение
- Источники
Чем занимается вальцовочная станция.
A coil packing roller station consists of a heavy-duty fabricated structural steel bed equipped with two parallel, horizontal cylindrical rollers. The metal coil rests directly across these rollers with its central core axis oriented horizontally (eye-horizontal / cradle orientation). Both rollers are mechanically coupled and driven by a variable frequency drive (VFD) gearmotor system, ensuring steady, synchronized rotation without slippage.
When the operator activates the station, the rollers rotate the coil in controlled jog steps (typically at a peripheral speed of 1.5 to 3.0 m/min). This brings every segment of the outer circumference, internal eye bore, and lateral sidewalls directly within reach of the packing personnel stationed along the platform.
This localized rotation replaces repetitive crane repositioning. Under traditional manual floor packing, an overhead crane must lift, tilt, or turn the coil multiple times so workers can reach the underside to wrap paper, fit outer jackets, and thread strapping bands. By keeping the coil continuously cradled on the powered rollers from initial loading to final strapping, the station eliminates crane-hook handling damage, reduces crane hoist fatigue, and keeps packing operations within a safe, fixed ergonomic envelope.
Последовательность упаковки
The step-by-step coil packaging process on the driven roller station proceeds in a single continuous setup:
| Шаг | Эксплуатация | Engineering Function & Purpose |
|---|---|---|
| 1 | Coil placement on turning rollers | Single loading motion via overhead crane (C-hook/nylon sling) or coil car; zero mid-process crane dependency |
| 2 | Inner & outer barrier wrap application | VCI film or creped PE-laminated paper wrapped around circumference; side folds tucked into the internal eye bore |
| 3 | Side discs & edge protector fitting | Internal/external metallic edge angles protect coil rims; radial fiberboard or galvanized discs protect side faces |
| 4 | Outer steel sheet application | Cold-rolled or galvanized steel wrapper curled around outer diameter (OD) to resist puncture and impact |
| 5 | Radial & circumferential strapping | Heavy-duty steel or PET straps tensioned pneumatically through the eye and around the circumference |
| 6 | Coil offloading | Fully strapped, weather-tight, and impact-shielded pack discharged directly to warehouse or shipping bay |
Because the rollers turn the coil precisely between steps 2 and 5, operators complete wrapping, tucking, sheet alignment, and pneumatic tool tensioning from a single operating side without reaching underneath heavy suspended steel.
Зачем нужна крышка из стального листа?
Flexible packaging films, VCI papers, and woven fabric wrappers defend metal surfaces against relative humidity, salt spray, and particulate contamination, but they offer virtually zero resistance to dynamic mechanical forces.
Heavy master export coils (ranging from 5 to 35 metric tons) encounter severe point contacts throughout multimodal transit. Wire rope slings, C-hooks, forklift tines, container wedge dunnage, and ship-hold lashing chains exert concentrated shear stresses on the outer wraps. A localized impact or dent on the outer layers will propagate inward, damaging dozens of steel coil wraps and turning thousands of dollars of prime gauge metal into scrap.
A sacrificial sheet of galvanized or cold-rolled mild steel (typically 0.5 mm to 0.8 mm thick) curled around the outer diameter distributes concentrated external loads across a broad surface area. When secured with circumferential high-tensile steel strapping, the outer steel jacket forms a rigid, self-supporting cylindrical armor that prevents outer lap gouging and maintains structural coil integrity during marine shipping.
Нарезка листового материала и ремней по длине.
To minimize station cycle time, protective covers and strapping bands should be pre-sheared to calculated lengths prior to coil staging.
Below is an engineering worked example for an export master coil with dimensions: Внешний диаметр = 1,800 мм, внутренний диаметр = 610 мм, ширина = 1,500 мм.
| Компонент упаковки | Governing Formula | Calculated Value (Nominal) | Practical Cut Length (with Allowances) |
|---|---|---|---|
| Внешняя окружность | π × OD | 3.1416 × 1,800 мм = 5,655 мм | Эталонная геометрия |
| Steel Outer Sheet | (π × OD) + Overlap Allowance | 5,655 мм + 150 мм | 5,800 мм (5.80 м) |
| Circumferential Strap | (π × OD) + Seal/Tensioner Joint | 5,655 мм + 200 мм | 5,855 мм (5.85 м) |
| Radial Eye Strap | 2 × Width + (OD − ID) + Joint Allowance | (2 × 1,500) + (1,800 − 610) + 250 mm | 4,440 мм (4.44 м) |
Engineering notes on allowances:
- Sheet Overlap (100–150 mm): Prevents seam separation under circumferential strap pressure.
- Radial Strap Geometry: Traverses through the inner bore (1× width), across the outer sheet (1× width), and along both radial side walls (2 × [(OD − ID) / 2] = OD − ID).
- Seal & Tool Joint Allowance (200–250 mm): Compensates for strapping feed-wheel take-up, pneumatic tensioner foot placement, and double-notch/crimp seal overlaps.
Вальцовочная станция или упаковочная линия
Selecting between a semi-manual roller turning station and a fully automated through-the-eye wrapping line depends on production throughput, pack specification mix, and capital expenditure:
| Production Criterion | Driven Roller Station | Автоматическая линия упаковки рулонов |
|---|---|---|
| Типичный результат | 3 to 8 coils per hour (shift dependent) | 12 to 25+ coils per hour |
| Разнообразие продуктов | High variation in OD, ID, width, and packaging specs | Standardized coil runs with uniform packaging specs |
| Pack Specification | Multi-material packs (VCI + paper + side discs + steel shell) | Stretch film / woven tape wrapping with auto-strapping |
| Начальные инвестиции | Low to moderate capital expenditure | High capital investment and civil foundation requirements |
| Метод обращения | Stationary rotation; batch crane or coil car loading | Continuous indexing; walking beams, shuttles, or turnstiles |
A powered roller station provides an immediate, low-risk upgrade for processing facilities that produce custom export coils. It removes hazardous crane balancing steps without requiring major shop floor reconfiguration. As volume scales, the station remains valuable as an offline rework and special-pack bay alongside automated lines.
Безопасность на вальцовом участке
Because heavy cylindrical loads are turned on an open horizontal cradle, safeguarding against in-running nips and mechanical instability is essential:
- In-Running Nip Points: The contact zones where the turning rollers meet the coil outer diameter present pinch hazards. Operators must maintain minimum clearance distances during rotation, and the control system must use momentary “deadman” hold-to-run foot switches or dual pushbuttons.
- Roll-Off Stability: The center-to-center distance between the two turning rollers must be engineered so that the center of gravity of the smallest and largest coils remains seated below the roller apex line, preventing accidental ejection.
- Поверхностное трение: Rollers should be encased in thick, high-durometer vulcanized polyurethane (PU, 85–95 Shore A) or high-friction neoprene. This provides traction against oiled steel sheets and eliminates surface galling.
- Применимые стандарты: Equipment design must comply with ISO 12100: 2010 (Risk assessment and risk reduction), EN 415-10: 2014 (Safety requirements for general packaging machines), and local OSHA / CE mechanical and electrical safety directives.
Контрольный список для выбора станции для прокатки рулонов
- Maximum & Minimum Coil Weight: Nominal and maximum tonnage ratings (e.g., 5 to 30 tons).
- Dimensional Boundaries: Maximum/minimum OD, minimum ID, and face width range.
- Roller Surface Finish: Heavy-wall steel tube bare vs. vulcanized polyurethane lining for sensitive surfaces.
- Требования к приводу: Dual-roller drive vs. single-roller drive; VFD variable rotation speeds with dynamic braking.
- Strap Feeding Aids: Pneumatic strap feeding tracks or roller gap slots for through-the-eye threading.
- Технические характеристики упаковочных материалов: Pre-cut steel outer sheets, plastic fluted edge angles, and inner bore tuck depths.
- Интеграция с заводом: Crane bay clear hook height, coil car floor tracks, and operator safety fencing layout.
Часто задаваемые вопросы по инженерным вопросам
Q: What is the primary purpose of a coil roller packing station? A: It rotates heavy master coils on driven rollers around their horizontal axis, allowing operators to complete wrapping, protective metal sheeting, and strapping in one position without using overhead cranes to reposition the coil.
Q: Why is an outer steel sheet cover necessary for export coils? A: Plastic stretch films and VCI papers only protect against moisture and corrosion. A steel outer sheet acts as a puncture- and dent-resistant shield against slings, hooks, forklift tines, and dynamic transit shifts.
Q: How is the outer steel sheet length calculated?
A: Calculate the coil circumference using π × OD, then add a 100 mm to 150 mm overlap allowance at the joint. For an 1,800 mm OD coil, the nominal length is 3.1416 × 1.8 m = 5.65 m, requiring a sheet cut to approximately 5.80 m.
Q: What straps are required for sea freight coil packaging? A: Heavy export packaging uses both radial straps (threaded through the inner eye to lock laps and side edge protectors) and circumferential straps (encircling the outer diameter to clamp the steel jacket tight).
Q: When is it justified to transition from a roller station to an automated packaging line? A: A full packaging line is justified when consistent output exceeds 10 to 12 coils per hour with uniform dimensions, allowing capital recovery through high throughput and automated cycle times.
Следующий шаг
To configure an optimized coil roller station or complete packing line layout:
- Предоставьте технические характеристики вашей катушки. (minimum/maximum OD, ID, face width, weight, and target output per shift) along with your plant layout to info@fhopepack.com.
- Receive an engineering concept within 48 hours, including roller center geometry calculations, drive power ratings, and 2D footprint layouts.
- Schedule an engineering consultation to evaluate strap feeding tracks, ergonomic tooling balancers, and safety perimeter requirements.
Связанное чтение
- Стальной спиральный турникет
- Видео: мастер-упаковщик стальных рулонов в стретч-пленку.
- Видео: упаковочная машина для рулонов, упаковка и погрузка/разгрузка.
Источники
- Field packing process and machine specifications: Technical verification by FHOPE Engineering Team, documentation update 2026-10-04.
- Dimensional calculation formulas: Standard industrial packaging geometry models for flat-rolled coiled products.
- Safety and mechanical design conformity: ISO 12100: 2010 (Безопасность машин и механизмов — Общие принципы проектирования), EN 415-10: 2014 (Безопасность упаковочных машин — Общие требования).
Последнее обновление: 21.09.2026