Резюме Flexible corrugated pipe and conduit rolls present unique packaging challenges: they are physically bulky, lightweight, and prone to springy radial deformation during rotation. In orbital eye-through stretch wrapping, the coil’s inner diameter (ID) and outer diameter (OD)—not its weight—primarily determine machine frame sizing and ring clearance. Three standardized machine platforms accommodate typical production profiles: the compact ФПКА-100 (OD 300–500 mm) for electrical conduit coils, the mid-range ФПХ-300Н (OD 500–1,000 mm) for commercial flexible hose, and the heavy-duty ФПХ-400Вт (OD 700–1,500 mm) for corrugated agricultural and civil drainage pipe rolls.
Содержание
- Как работает обертка для гофрированных труб
- Три модели в зависимости от размера рулона
- Почему гофрированным рулонам необходима опора для роликов?
- Перекрытие на ребристой поверхности
- Время цикла
- Коммунальные услуги и безопасность
- Контрольный список выбора
- Часто задаваемые вопросы по инженерным вопросам
- Следующий шаг
- Связанное чтение
- Источники
Как работает обертка для гофрированных труб
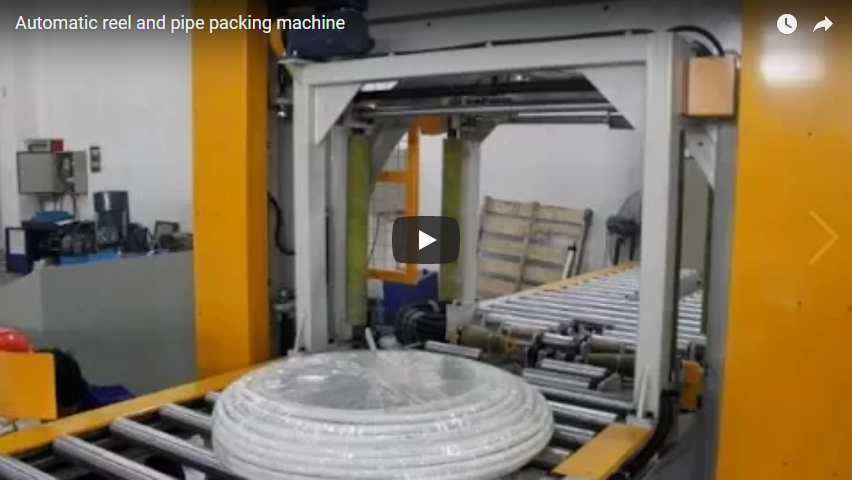
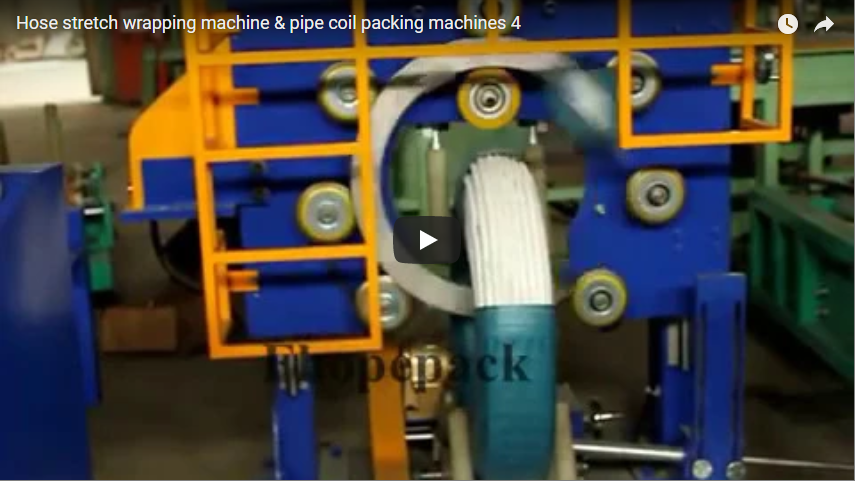
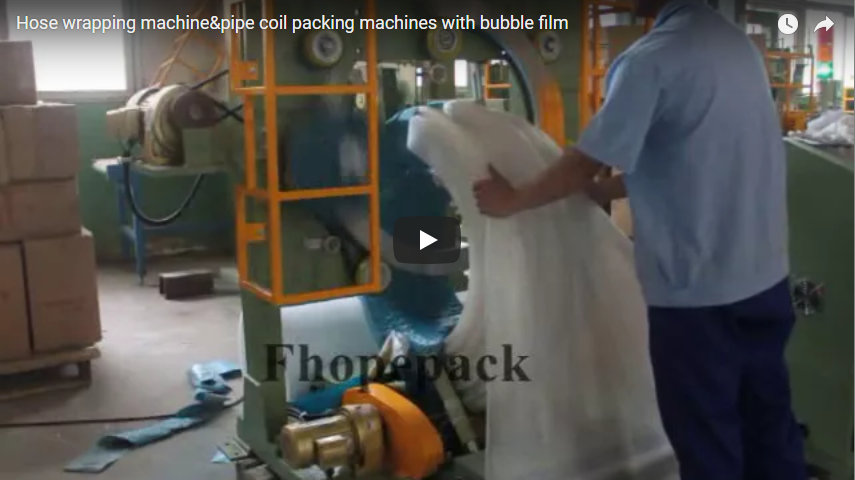
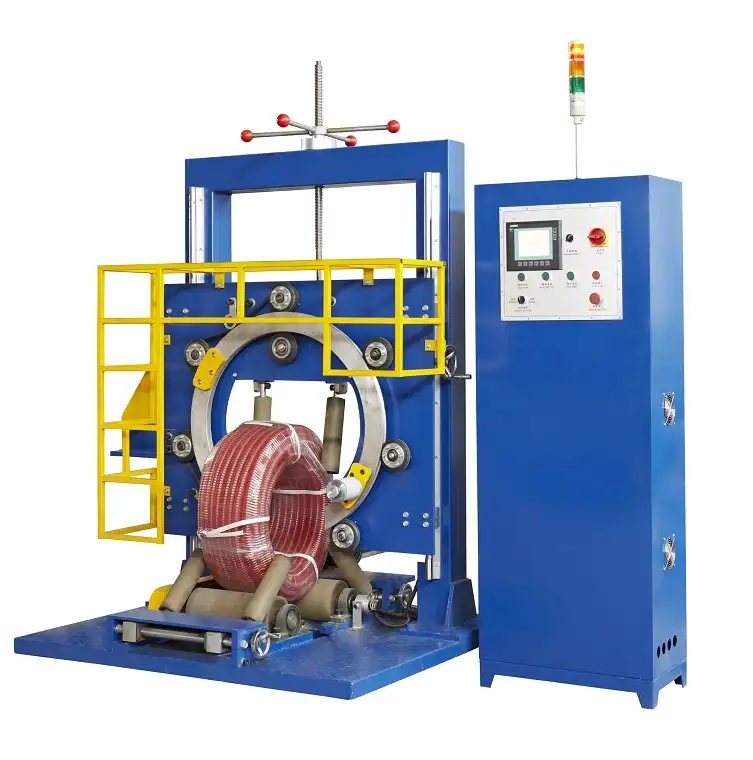
The horizontal-axis orbital coil wrapper secures the corrugated pipe roll between polyurethane-coated base support rollers and adjustable vertical side-guide rollers. An aluminum rotating ring carries the film carriage through the roll’s central eye, while the motorized support rollers rotate the roll 360 degrees around its own axis.
This synchronized dual-axis rotation deposits stretch film circumferentially around the entire cross-section of the roll. Variable Frequency Drives (VFDs) control the speed ratio between the rotating ring and the support rollers, allowing operators to dial in the exact film overlap percentage required.
   [ Rotating Ring (Eye-Through Orbit) ]
                 │
           ┌─────▼─────┐
           │ Stretch   │ ──> Dispenses film through coil core
           │ Carriage  │
           └───────────┘
                 │
       ╔═════════╪═════════╗
       ║   ┌─────┴─────┐   ║
       ║   │ Corrugated│   ║ <── Held by side-guide rollers
       ║   │ Pipe Coil │   ║
       ║   └─────┬─────┘   ║
       ╚═════════╪═════════╝
                 │
      [ PU Support Rollers ] ──> Index coil 360° circumferentially
Engineered for ergonomic manual loading, crane loading, or inline conveyor integration, the ring incorporates an automatic soft-start and soft-stop acceleration ramp. At the end of the wrap cycle, an integrated sensor and timing relay trigger the automatic home-position ring park mechanism for rapid unloading.
Три модели в зависимости от размера рулона
Coil geometry (ID, OD, and axial width) defines the required ring opening and roller spacing. Payload weight is rarely the primary sizing constraint for corrugated products.
| Инженерный параметр | ФПКА-100 | ФПХ-300Н | ФПХ-400Вт |
|---|---|---|---|
| Внутренний диаметр катушки (ID) | 150 – 350 мм | 300 – 700 мм | 300 – 1,250 мм |
| Внешний диаметр катушки (OD) | 300 – 500 мм | 500 – 1,000 мм | 700 – 1,500 мм |
| Ширина катушки / Осевая высота | 50 – 200 мм | 100 – 300 мм | 150 – 400 мм |
| Максимальный вес катушки | 5-50 кг | 10-100 кг | 10-100 кг |
| Время цикла упаковки | 25–35 с | 23–35 с | 30–55 с |
| Максимальная скорость кольца | 100 г / мин | 120 г / мин | 100 г / мин |
| Ширина упаковочной пленки | 50 – 70 мм | 90 – 100 мм | 90 – 120 мм |
| Подключенная мощность привода | 1.5 кВт | 1.9 кВт | 1.5 кВт |
- Selection scenario A: A corrugated electrical conduit roll with 250 mm ID, 450 mm OD, 120 mm width, and 12 kg weight fits directly on the ФПКА-100.
- Selection scenario B: A corrugated agricultural sub-drainage coil measuring 600 mm ID, 1,200 mm OD, 350 mm width, and 65 kg requires the expanded ring clearance of the ФПХ-400Вт.
Почему гофрированным рулонам необходима опора для роликов?
Unlike rigid steel or copper coils, a corrugated pipe coil behaves like an open-wound spring. When rotating on its belly, the roll experiences dynamic radial deflection and axial buckling. Uncontrolled, this flexibility causes lateral walking, rotational vibration, and uneven film application.
Our wrapping systems stabilize corrugated rolls using three coordinated mechanical mechanisms:
- Twin PU-Coated Driving Rollers: Support the coil belly, dampening rotational vibrations while delivering consistent non-slip friction drive to ribbed plastic surfaces.
- Adjustable Lateral Guide Rollers: Straddle the roll flanks to prevent the package from shifting axially as tensioned film exerts lateral pull forces.
- Mechanical Friction Tension Brake: Maintains constant web tension from full film reel to core depletion, ensuring light corrugated walls do not crush under excessive film neck-down.
On heavy-duty units like the FPH-400W, roller drive friction and side-roller distance are independently adjustable to handle varying profile stiffness across HDPE, PP, and PVC materials.
Перекрытие на ребристой поверхности
Stretch film bridges across the outer ridges of corrugated pipe rather than conforming down into the annular valleys. Because air and moisture ingress occur primarily along these bridged gaps, maintaining an airtight package requires precise overlap control.
The FPH-300N offers programmable overlap from 10% to 90%, while the FPH-400W operates between 20% and 90%.
Because orbital wrapping creates a fan-like film distribution—tightly bunched at the inner core and spread widest at the outer perimeter—we calculate the required wrap count strictly at the outer diameter (OD), where gaps are most likely to open.
       Film Overlap Distribution on Annular Profile:

            [ Outer Diameter (OD) ] ── Wider spacing (Target: 30%–50% overlap)
                   \        /
                    \      /
                     \    /
                      \  /
             [ Inner Diameter (ID) ] ── Heavy film accumulation (Denser seal)
Calculation Example: 250 mm ID × 450 mm OD Coil with 60 mm Film
- Outer Circumference Calculation:
C_OD = π × OD = 3.1416 × 450 mm = 1,414 mm - Effective Pitch at 30% Overlap:
With a 60 mm film roll, 30% overlap means 70% effective advance per ring revolution:
Advance = 60 mm × (1 - 0.30) = 42 mm/rev - Total Ring Wraps Required:
Wraps = 1,414 mm ÷ 42 mm/rev ≈ 34 wraps - Resulting Overlap at Inner Circumference (ID):
C_ID = π × ID = 3.1416 × 250 mm = 785 mmThe same 34 wraps over 785 mm advance only:Advance_ID = 785 mm ÷ 34 wraps ≈ 23.1 mm/revThis yields an overlap of:[ (60 mm - 23.1 mm) ÷ 60 mm ] × 100% ≈ 61.5%
The film naturally forms a multi-layer protective barrier at the coil eye. The carriage’s mechanical brake prevents film twisting or neck-down creasing throughout the cycle.
Время цикла
Net packaging throughput depends on ring rotation speed, programmed overlap percentage, and operator handling speed:
| Модель машины | Pure Wrapping Cycle | Theoretical Output (Excluding Handling)* |
|---|---|---|
| ФПКА-100 | 25–35 s / roll | 102–144 rolls / hour |
| ФПХ-300Н | 23–35 s / roll | 102–156 rolls / hour |
| ФПХ-400Вт | 30–55 s / roll | 65–120 rolls / hour |
*Note: Actual floor capacity depends on whether loading is performed manually, with an overhead balancer, or via powered indexing conveyors. Loading and unloading typically add 15 to 30 seconds per cycle for standalone operations.
Коммунальные услуги и безопасность
| Technical Utility | Спецификация / Параметр |
|---|---|
| Подключенная мощность | 1.5 kW (FPCA-100, FPH-400W) / 1.9 kW (FPH-300N) |
| Стандартное напряжение питания | 380 V AC, 50/60 Hz, 3-Phase (Optional 220 V / 480 V configurations) |
| Film Core Internal Diameter | 50 mm ID core (standard orbital film roll) |
| Цепь управления | 24 V DC safe control voltage |
Системы безопасности и соблюдение нормативных требований
- Физическая охрана: Integrated perimeter mesh guard enclosures isolate the orbital ring rotation path from the operator loading station.
- Защита диска: Motor overcurrent detection, thermal overload protection, and dynamic braking prevent ring overrun.
- Jog & Setup Modes: Auxiliary foot-switch control allows controlled, low-speed jogging during film loading and roll positioning.
- Международные стандарты: Built to comply with ISO 12100: 2010 (Безопасность машин и механизмов — основные понятия, общие принципы проектирования) и EN 415-10: 2014 (Безопасность упаковочных машин — Общие требования).
Контрольный список выбора
Confirm the following engineering parameters prior to requesting a formal proposal:
- Размеры катушки: Minimum and maximum ID, OD, and width (axial face thickness).
- Весовой диапазон: Minimum and maximum gross roll weight (kg).
- Спецификация материала: Corrugated material type (PE, PP, PVC, PA) and single-wall vs. double-wall rib profile.
- Целевая пропускная способность: Required continuous production output (rolls per hour).
- Упаковочный материал: Stretch film (PE), crepe paper, woven polypropylene tape, or knit-mesh stretch film.
- и перевалки сыпучих материалов : Manual operator loading, pneumatic ejector ramp, or automated infeed/outfeed integration.
- Коммунальные услуги на участке: Exact plant voltage, frequency, and local safety disconnect requirements.
Часто задаваемые вопросы по инженерным вопросам
Q: Which wrapping model is recommended for small electrical corrugated conduit?
A: ФПКА-100 is specifically proportioned for small conduit coils with inner diameters between 150–350 mm, outer diameters between 300–500 mm, and coil weights up to 50 kg.
Q: Which model handles large agricultural and stormwater drainage coils?
A: ФПХ-400Вт accommodates large pipe bundles up to 1,500 mm OD and 1,250 mm ID, featuring heavy-duty guide assemblies designed for wide-face coils.
Q: How does the system prevent flexible pipe rolls from uncoiling during wrapping?
A: The machine combines adjustable polyurethane base rollers with vertical side-guide rollers to constrain the coil radially and laterally. In addition, the tension-controlled film carriage applies balanced hoop stress, pulling the ribs tightly into an integral bundle.
Q: What is the realistic continuous output for a single machine?
A: For a standard model such as the FPCA-100 or FPH-300N, the automated wrapping cycle runs in 25–35 seconds. With manual staging and removal, average production yields between 60 and 90 wrapped rolls per hour.
Q: How is film overlap adjusted for different transport environments?
A: Overlap is controlled directly from the control console via independent inverter frequency presets. Increasing ring speed relative to roller rotation increases overlap (up to 90%) for complete weather protection and moisture sealing.
Следующий шаг
To size your pipe coil wrapping equipment:
- Submit your dimensional matrix (minimum/maximum ID, OD, width, weight, and hourly target) to info@fhopepack.com.
- Получите инженерное предложение в течение 48 часов., including recommended ring sizing, roller configuration, film consumption estimates, and overlap calculations.
- Запланируйте рассмотрение заявки with our engineering team to finalize layout drawings and conveyor interfaces.
Связанное чтение
- Corrugated hose packing machine FPCA-100 technical details
- Hose wrapping machine FPH-300N specifications
- Hose coil wrapping machinery FPH-400W configuration
- Full range of horizontal & orbital hose packaging systems
- Video library: automatic hose and coil wrapping equipment
Источники
- FPCA-100 Technical Specifications & Operating Guidelines: FHOPE Corrugated Hose Packing Series
- FPH-300N Engineering Data & Speed Ratings: FHOPE FPH-300N Product Page
- FPH-400W Heavy-Duty Dimensional Ranges: FHOPE FPH-400W Overview
- Machine Operation Video Demonstration: FHOPE Corrugated Pipe Rolls Wrapping Demonstration
- Machinery Safety Directives: ISO 12100:2010 Безопасность машин и механизмов, EN 415-10:2014 Безопасность упаковочных машин
Последнее обновление: 21.09.2026