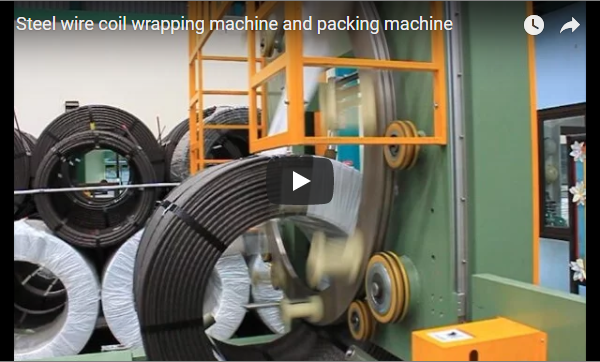
Резюме An inline steel strip coil packing machine automates the orbital eye-through protective wrapping process directly on an integrated powered roller conveyor, eliminating intermediate crane lifts and preserving strip edge integrity after slitting. In our operational clip, a bare slit steel coil enters the packaging station, an eye-through orbital wrapping ring descends to engage the coil ID/OD profile at 10 to 12 s, applies an overlap barrier wrap, and discharges the sealed coil by 28 s. Rated for medium-to-heavy industrial strip handling, our FPS-400 platform accommodates coils with inner diameters (ID) of 508 or 610 mm, outer diameters (OD) of 800 to 1,400 mm, axial widths of 100 to 400 mm, and payloads from 100 to 2,000 kg.
Содержание
- Technical Breakdown: Station Sequence and Motion Cycle
- Cycle Time and Phase Analysis
- Why Wrap Slit Strip Coils Inline
- FPS-400 Technical Specifications
- Takt Time and Capacity Verification
- Selection Checklist for an Inline Strip Coil Wrapping Line
- System Controls, Interlocks, and Operational Safety
- Часто задаваемые вопросы по инженерным вопросам
- Next Step: RFQ and Line Sizing
- Связанные Чтение
- Sources and Standards
Technical Breakdown: Station Sequence and Motion Cycle
The machine structure utilizes a heavy-duty structural steel cantilever frame finished in industrial blue, housing a vertical linear guide column that drives the orbital wrapping carriage above a heavy-duty motorized roller conveyor. Integrated polyurethane-coated side guide rollers center the coil along the conveyor axis. A machine-mounted operator interface panel with hardwired safety circuits is positioned on the service side, complemented by a tri-color LED stack light (red/amber/green) mounted on the main frame post.
- 0 to 8 s (Infeed & Center Verification). A bare, slit carbon steel coil rests in an eye-to-sky orientation (horizontal eye axis perpendicular to transport) on the powered conveyor bed. The orbital shuttle ring remains parked in its elevated home position, providing full radial clearance above the line while wrapped coils advance downstream.
- 10 to 12 s (Descent & Clamping Sequence). Pneumatic/mechanical roller drives index the coil into the wrapping station datum. The vertical carriage descends along precision prismatic guides, lowering the rotating ring frame through the coil eye until the integral pneumatic hold-down roller secures the upper coil rim.
- 14 to 20 s (Orbital Eye-Through Wrapping). The orbital ring accelerates to operating speed, driving the film carriage through the coil inner core and around the outer diameter. A multi-layer, pre-tensioned film helix encapsulates the coil section. An operator oversees the automated envelope build from the external pendant station.
- 22 to 28 s (Film Cut, Clamp & Carriage Elevation). The shuttle reaches its programmed turn count, bringing the automatic mechanical cutter and pneumatic film grabber into engagement. The carriage retracts to its upper limit switch, the green beacon signals cycle completion, and the fully wrapped coil indexes downline.
- 30 to 38 s (Secondary Coil Positioning). During the standby window, the conveyor receives the subsequent slit coil. Lighter gauge coils or buffer packs are aligned along the feed rollers against the positioning stops.
- 40 to 46 s (Automatic Re-Engagement). The secondary coil is indexed to the center wrapping line. The carriage descends rapidly, confirming part presence via optical beam sensors before decelerating into clamping position.
- 48 to 56 s (Continuous Production Run). The orbital ring executes the targeted overlap pass on the second coil. Finished coils accumulate smoothly on the powered discharge conveyor without bottlenecks.
Cycle Time and Phase Analysis
| Операционная фаза | Motion Window (Clip) | Чистая продолжительность | Механическая функция |
|---|---|---|---|
| Infeed Indexing & Alignment | От 0 до 8 с | 8 ~ ы | Conveyor transport and center stop positioning |
| Carriage Rapid Descent | От 10 до 12 с | 2 ~ ы | Guided vertical descent and pneumatic hold-down engagement |
| Orbital Ring Wrapping Pass | От 14 до 20 с | 6 ~ ы | Eye-through helical wrapping (variable 20–80 RPM) |
| Cut, Wipe & Carriage Retract | От 22 до 28 с | 6 ~ ы | Mechanical cutoff, tail tuck, and vertical stroke return |
| Gross Machine Cycle (Single Coil) | От 10 до 28 с | 18 ~ ы | Pure automated processing duration per unit |
| Floor-to-Floor Coil Pitch | От 10 до 44 с | 34 ~ ы | Includes manual infeed staging and upstream index time |
Note: Data derived from 2-second timestamp intervals. The pure automated machine cycle runs at approximately 18 seconds. From initial carriage descent on unit one to initial descent on unit two measures between 28 and 34 seconds, including interlock pauses for manual workpiece positioning. Integrating a powered upstream buffer moves staging completely off the critical path.
Why Wrap Slit Strip Coils Inline
Narrow slit steel coils discharged from a slitting arbor present distinct material handling vulnerabilities: exposed edges are prone to burring, telescoping, and ambient atmospheric oxidation.
Wrapping coils directly on the discharge roller line delivers critical operational advantages:
- Zero Crane or Hoist Dependency: Eliminates repetitive C-hook or overhead hoist transfers for secondary packaging stations, freeing up plant cranes for raw master coils.
- Flat Conveying Preserves Edge Geometry: The coil remains in its horizontal eye-to-sky orientation throughout transport and wrapping. Eliminating tilting operations prevents edge nicking and coil telescoping.
- Hermetic Anti-Corrosion Barrier: As observed on bare coils showing rapid surface oxidation, applying a continuous, tensioned VCI film, stretch wrap, or HDPE barrier immediately after slitting isolates the steel from ambient humidity and particulate contamination.
FPS-400 Technical Specifications
The FPS-400 represents our engineered platform for medium-to-wide slit strip packing applications. It employs an eye-through orbital wrapping architecture configured to customer-specified coil envelopes:
| Параметры машины | Спецификация Стандарт |
|---|---|
| Внутренний диаметр катушки (ID) | 508 mm (20 in) or 610 mm (24 in) standard arbors |
| Внешний диаметр катушки (OD) | 800 к 1,400 мм |
| Coil Width (Axial Stack) | 100 к 400 мм |
| Максимальная грузоподъемность | 100 to 2,000 kg (rigid conveyor rating) |
| Совместимые упаковочные материалы | Stretch PE film, VCI anti-rust film, reinforced paper, woven HDPE tape |
| Размеры упаковочного рулона | Core ID: 50 mm; Roll OD: 100 to 450 mm; Width: 100 to 150 mm |
| Коэффициент перекрытия пленки | 10% to 90% (digitally synchronized via VFD) |
| Скорость вращения кольца | 20 to 80 RPM (frequency inverter controlled) |
| Подключенная электрическая нагрузка | 4.0 kW, 380 V ±10%, 50/60 Hz, 3-Phase |
| Pneumatic Service Required | 5 to 7 kgf/cm² (0.5 to 0.7 MPa clean, dry shop air) |
Takt Time and Capacity Verification
For a slitting line producing a target output of 60 slit coils per hour, allowable takt time is:
Takt Time = 3,600 s / 60 coils = 60.0 s per coil
The baseline inline cycle demonstrated in the sequence operates at a floor-to-floor pitch of 28 to 34 seconds:
- Net Wrapping Window: ~ 18 секунды.
- Line Capacity Margin: At 34 seconds per coil, the packaging station sustains an output of approximately 105 coils per hour under continuous demand, operating at roughly 57% of allowable takt.
When specifying higher overlap settings (e.g., 70% to 80% for long-distance maritime export), orbital wrap duration increases proportionately. Our application engineers calculate precise cycle durations based on your target film width and coil thickness. Where slitter output exceeds 80 coils per hour, automated infeed pushers and queue buffers are integrated to decouple line feed from operator interventions.
Selection Checklist for an Inline Strip Coil Wrapping Line
- Габаритные размеры рулона: Confirm minimum and maximum ID, OD, axial width, and unit mass against the FPS-400 engineering boundaries.
- Packaging Media Selection: Determine whether PE stretch, anti-corrosion VCI, or reinforced kraft paper is required to withstand transit durations.
- Target Overlap Ratio: Establish required overlap (10% to 90%) to balance barrier density against cycle time and consumable cost.
- Upstream/Downstream Conveyance: Specify roller pitch, powered chain-driven live rollers (CDLR), or hydraulic walking beams.
- Secondary Finishing Modules: Review requirements for automated OD strapping, robotic labeling, dry-ink jet coding, or downline turnstile stacking.
System Controls, Interlocks, and Operational Safety
The operational sequence prioritizes separation between high-inertia moving elements and line operators:
- Zone Interlocking: The orbital rotating ring and vertical traverse carriage operate inside a defined hazard envelope. Operator interventions for coil alignment are permissible only when the system state register confirms zero-motion standby.
- Safety Light Curtains and Perimeter Enclosures: Standard production units integrate dual-channel Type 4 safety light curtains across the conveyor entry and exit apertures, tied to a certified safety relay or safety PLC (PLe / SIL 3).
- Hazard Isolation (LOTO): Complete isolation and Lockout/Tagout (LOTO) protocols must be enforced before consumable film re-threading, mechanical maintenance, or physical inspection within the ring path.
- Harmonized Compliance: The equipment complies with international machine safety regulations:
- ISO 12100: 2010: Risk assessment and risk reduction principles.
- ЕН 415-10:2014: Safety requirements for packaging machines and integrated lines.
- NFPA 79 / UL 508A: Electrical control enclosure compliance for North American installations.
Часто задаваемые вопросы по инженерным вопросам
Q: What is the net floor-to-floor wrapping cycle time for a single coil? A: The orbital wrapping pass takes approximately 6 seconds. Complete single-station cycle time—including infeed positioning, carriage descent, wrapping, film severing, and discharge—is approximately 18 to 22 seconds, enabling throughputs exceeding 90 coils per hour depending on infeed automation.
Q: Can the FPS-400 handle both narrow slit strips and wide coils on the same bed? A: Yes. The orbital carriage features variable vertical stroke limits and an adjustable pneumatic clamping stroke that accommodates coil widths from 100 mm to 400 mm, provided the inner core diameter remains at or above 508 mm.
Q: What consumable wrapping materials are compatible with the orbital shuttle? A: The shuttle tensioning unit handles LLDPE stretch film (17–35 µm), VCI anti-corrosion film, crepe paper, woven HDPE, and composite barrier films wound on standard 50 mm (2 in) cores.
Next Step: RFQ and Line Sizing
To integrate an FPS-400 inline coil packaging system into your slitting or cut-to-length facility, follow our rapid sizing protocol:
- Отправить производственные данные: Send your coil schedule (minimum/maximum ID, OD, width, weight, and targeted hourly output) along with plant floor layouts to info@fhopepack.com.
- Получите инженерное предложение в течение 48 часов: Our engineering team returns a 2D line layout, roller elevation drawings, takt time simulation, and commercial quotation.
- Factory Acceptance & Virtual Survey: Schedule a live video conference or on-site layout audit to finalize interface boundaries with your slitter exit and downline palletizing cells.
Связанные Чтение
- Steel Coil Packing Machine FPS-400 Platform Details
- Automated Slitting Coil Turnstile and Packaging Lines
- Industrial Coil Packing Solutions and System Architectures
- Automatic Coil Wrapping Stations with Integrated Strapping and Barcode Printers
Sources and Standards
- Технические характеристики оборудования: FPS-400 Steel Coil Packing Machine Technical Data
- Operational Validation: FHOPEPACK In-Plant Performance Test Footage (FPS-400 Series Demonstration)
- Соответствие международным нормам безопасности: ISO 12100:2010 Безопасность машин и механизмов
- European Packaging Line Standard: EN 415-10:2014 Требования безопасности к упаковочным машинам
Последнее обновление: 21.09.2026