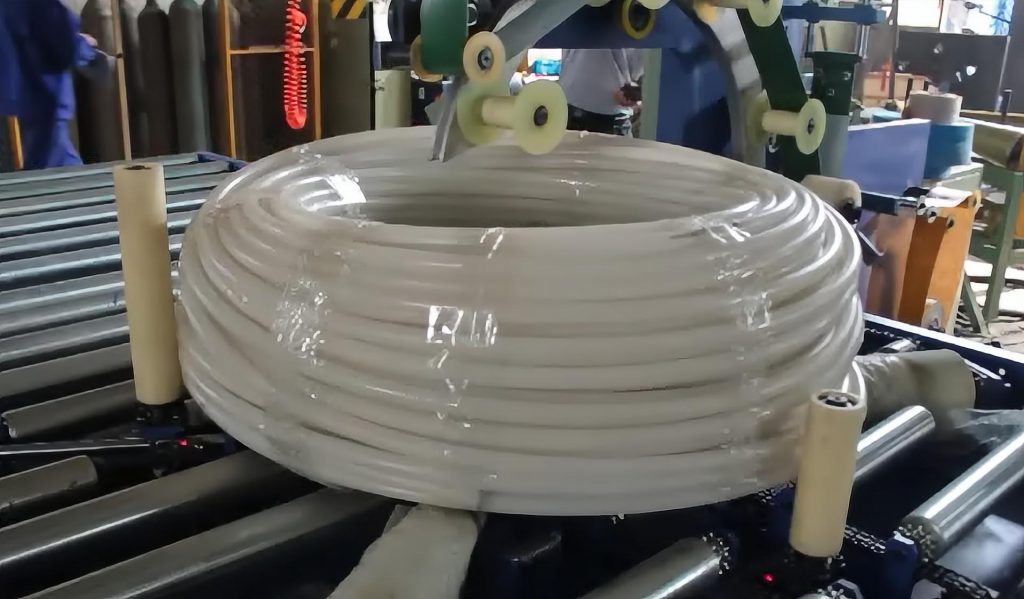
Descriere
An aged steel coil packing line can be upgraded rather than replaced: automatic strapping is retrofitted onto the existing roller conveyors to lift manual strap fitting out of the cycle and raise output without a new foundation or a full line build. This article explains how such a retrofit takes shape — the modules added to an existing steel coil packaging line, how the new machines interface with the existing conveyors and controls, and what is surveyed before work starts. It is addressed to plant managers and maintenance engineers at steel service centers and coil processors who run an older packing line and want to automate the strapping step within a limited shutdown window.
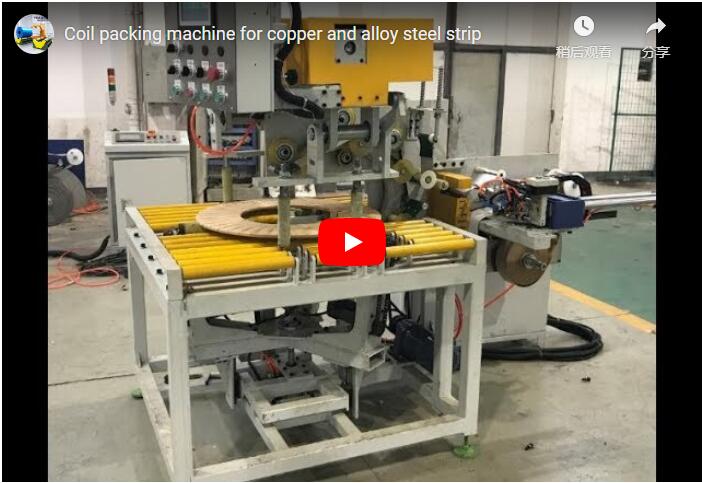
The video below documents the upgraded line running on the original conveyors:
What the Retrofit Adds to the Old Line
The strapping modules are engineered around the existing fixed assets instead of replacing them. Steel coils continue to move on the original yellow roller conveyors; the new equipment is fitted above and beside them and wired into the plant supply. The typical module set is:
| Module | Ce face |
|---|---|
| Controlul poziției | Rollers locate and stop each coil at the strapping station. |
| Indexing / turn devices | Present the coil face for radial or circumferential strap runs. |
| Cap de legat cu banda automată | Feeds, tensions and seals the strap over the coil. |
| Packing / film station | Applies a protective wrap where the project requires it. |
| Hrănire | Moves the strapped and packed coil on for storage or shipment. |
The exact mix is set per project from the old line’s layout and the coil sizes it handles. Keeping the running machines and conveyors is the point of the upgrade: it limits plant-side work to positioning, wiring and commissioning of the new units.
Matching Strapping Time to Line Takt
A retrofit only pays off when the added strapping step stays inside the line cycle. The check is a comparison between strapping time and line takt:
| Articol | Valoare ilustrativă |
|---|---|
| Line takt (3,600 s ÷ 30 coils/h) | 120 s per bobină |
| Curele per bobină (cu titlu ilustrativ) | 4 |
| Timp de legare | 4 × (timp per curea + index între curele) |
| Condiție de acceptare | Timp de legare sub 120 s per bobină |
Where the spare time becomes too small, the solution is extra capacity rather than a slower line: a second strapping head, or moving part of the work upstream of the station. Values in the table are worked examples only — confirm the real coil mix and output with the manufacturer during survey.
What Is Surveyed on the Old Line Before Work Starts
Retrofit work starts with a survey of the line that is being kept. The items below determine whether the new units fit and how they connect:
| Articol | Why it decides the upgrade |
|---|---|
| Înălțimea și lățimea benzii transportoare | The new heads must span the existing rollers. |
| Gama de dimensiuni a bobinei | Sets head travel, strap length and the duration of each strap. |
| Alimentare cu energie electrică și aer | The retrofitted units must suit what the plant provides. |
| Semnale de control | The new cycle must talk to the existing line and its desk. |
| Spațiu deasupra și lângă linie | For the gantry arm, guarding and operator access. |
The upgrade is planned around a defined shutdown window, agreed before work begins, to keep plant downtime short. Safety practice follows the standards that apply to the destination market: for CE markets, ISO 12100 sets the risk-assessment method and EN 415-10 sets general requirements for packaging machines.
Testare și acceptare în fabrică
Two practice points apply to planning acceptance on this machine family. First, the vendor’s stated practice is to run each machine through non-stop functional and safety testing before delivery — about 24 hours where stated — covering control systems and the emergency-stop function; treat this as the stated family practice, not a single-unit measurement. Second, confirm that guarding and documentation for the retrofitted station (ISO 12100 risk assessment and EN 415-10 where CE applies) are delivered with the project.
FAQ
Q: Can automatic strapping be added to an old coil line?
A: Yes. This upgrade retrofits automatic strapping onto the existing roller conveyors rather than replacing the line.
Q: Will the retrofitted machine keep up with the line?
A: Strapping time is checked against line takt. In the worked example, four straps with their index moves must fit inside a 120 s takt.
Q: What needs to be measured on the old line first?
A: Conveyor height and width, coil size range, power and air, control signals, and space around the line.
Q: Do operators still work inside the coil zone?
A: No — the cycle is run from an operator desk outside the moving area, with the guard and safety interlocks in place.
Q: What happens if the strapping time is too long?
A: Add a second head or move part of the work upstream of the station.
Următorul pas
Submit your line layout drawing with conveyor dimensions, coil sizes and target output to the manufacturer, receive a proposal with the upgrade scope and takt check, then book a site survey to confirm the old line’s conveyors and controls.
Resurse conexe
- Automatizarea unei linii de ambalare a bobinelor cu mașini de legat cu banda – How strapping machines are added to an existing coil line.
- Steel Coil Packaging Line Station by Station – Station-by-station layout of a coil packaging line.
- Mașină automată de legat cu banda de oțel – Standalone automatic strapping for steel coils.
- Coil Upperer – Turning and upending equipment compatible with coil packing lines.