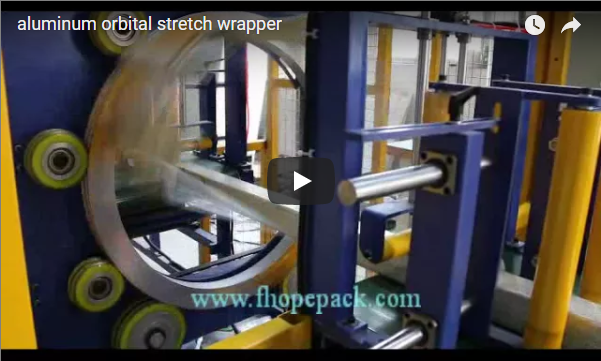
Streszczenie An aluminum profile packing line earns its keep on changeover speed and wrap consistency, not on headline speed. A horizontal orbital wrapper wraps each extrusion bundle under a programmed film pattern, while pre-stretch, guided centering and per-family programs hold quality stable across shifts. Line length, ring size and program set are configured per project.
Spis treści
- From hand wrapping to a packing line
- Ring and conveyor sequence
- Pre-stretch as a practice
- Centering and bundle preparation
- A program per extrusion family
- Kontrola jakości przed wysyłką
- Daily operation checklist
- Sterowanie i bezpieczeństwo
- Często zadawane pytania dotyczące inżynierii
- Następny krok
- Powiązane czytanie
- Źródła i standardy
From hand wrapping to a packing line
Most extrusion plants outgrow hand wrapping in stages. First the wrap pattern becomes the slow step in the line, then film cost climbs, then two operators argue over who pulled last shift’s tension. A wrapping line removes the hand-to-hand variation by making every bundle follow the same sequence.
The step that matters most is the changeover: the line earns its money when the operator can switch from one extrusion family to the next without re-teaching the machine.
Ring and conveyor sequence
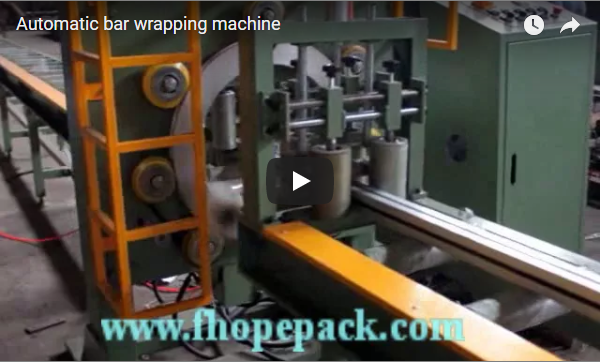
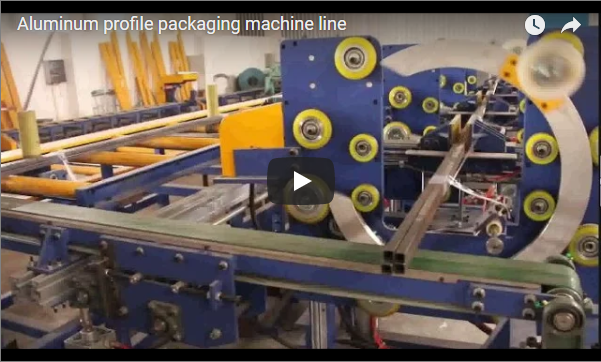
Bundles arrive from the extrusion line and pass straight through a rotating ring on a conveyor. The ring carries the film roll around the bundle while the conveyor moves it forward, laying film in an overlapping spiral over the full length. At each end the wrap pattern locks the loose ends, and a cutter separates the finished bundle from the film.
Alignment matters more than speed. If the bundle enters off-center, the spiral gaps at the edges and the wrap loses strength where it is needed most.
Pre-stretch as a practice
Pre-stretch elongates the film before it reaches the bundle. Done consistently, it does three things at once. Each roll covers more length. Tension stays the same bundle after bundle. And the film hugs the profile, so the bundle holds its shape in the rack and in the truck.
Set pre-stretch in the program rather than on the roll. Operators then cannot over-tighten one bundle and under-tighten the next.
Centering and bundle preparation
A straight bundle wraps cleaner than a stacked one. Before the ring, confirm the bundle is squared and its edges are even; a loose profile inside the bundle shows up on the wrapped surface as a bulge.
Use a guide or side fence at infeed to square the bundle to the conveyor centerline. With a centered bundle the spiral stays even, film use stays predictable, and the wrapped unit holds together through handling.
A program per extrusion family
Architectural trim and heavy structural sections need different wraps. Light trim runs at reduced tension and higher overlap so the profile is not crushed; heavy structural sections run at higher tension with reinforced end wraps to stop shifting. The program is set per project. Our control panel holds a program per family, with its own wrap count, overlap, pre-stretch and tension.
| Program field | Co kontroluje |
|---|---|
| Liczba opakowań | layers applied over the bundle |
| zakładka | spacing between spiral turns |
| Wstępne rozciąganie | film elongation before application |
| Napięcie | how tightly the film compresses the bundle |
| End wraps | reinforced loops at each end |
Store each profile family in the program library once, and changing over is a matter of calling it up. The same program can wrap a narrow trim batch in the morning and a structural section batch in the afternoon without re-calibrating tension by hand. When a new bundle shape or weight range arrives, we set a new program with you at start-up, then lock it so the wrap does not drift between shifts.
Standard line specifications
The figures below are common starting envelopes for this machine class and are confirmed against the bundle per project.
| Parametr | Typowy zakres, potwierdzony dla każdego projektu |
|---|---|
| Długość profilu | 1 to 12 m profile or bundle length; infeed and outfeed conveyor length per project |
| Profile cross-section | 10 x 10 mm do 150 x 150 mm |
| Prędkość obrotowa pierścienia | 10 do 30 XNUMX obr./min |
| Rozciąganie wstępne folii | 200 do 300 procent |
| Dostawy prądu | 380 V trójfazowe 50 Hz lub 220 V jednofazowe, dobierane indywidualnie do projektu i zasilania zakładu |
Kontrola jakości przed wysyłką
- Check that the end wraps cover the bundle ends and lock the film tail.
- Run a hand over the wrapped surface for bulges that signal a loose profile inside.
- Confirm the bundle keeps its shape when lifted from the outfeed conveyor.
- Spot-check film tension on the first bundle of every shift and after each changeover.
Daily operation checklist
| Krok | Działania |
|---|---|
| At shift start | load film, check roll for edge damage, confirm the program matches the bundle |
| Before changeover | wind off partial wrap, load the next family’s program |
| Zmiana środkowa | clear film trimmings, check the cutter and clamp |
| Koniec zmiany | record film use and any tension faults on the log |
Lista kontrolna wyboru maszyny
| Question | Potwierdź dla każdego projektu |
|---|---|
| Longest section | conveyor and ring length for your longest bundle |
| Najszerszy pakiet | ring opening that clears your thickest profile pack |
| Program families | recipes for the extrusion families you actually run |
| Stopień filmowy | pre-stretch range, width and roll size |
| Dostawy prądu | napięcie, faza i częstotliwość na miejscu |
Sterowanie i bezpieczeństwo
The panel drives the program library and shows cycle status. Keep hands clear of the ring while it rotates and keep the guard closed; the machine stops on the e-stop before guarding is opened. Film threading follows the machine manual, and only trained operators change tension settings.
Często zadawane pytania dotyczące inżynierii
Q: What is the difference from a turntable wrapper? A: A turntable wrapper spins the load; an orbital ring wraps the stationary bundle through the ring, which suits long extrusion bundles.
Q: How long does a program changeover take? A: With stored programs it is a panel selection plus a film check; if the new bundle family also changes the physical guides, that adjustment is set with us at start-up.
Q: Does pre-stretch work with any film? A: It suits a clear stretch film of suitable grade; film width and roll size are set with us per project.
Q: Can the line run two extrusion families in one shift? A: Yes. Each family has its own program, and the wrap pattern is held per program.
Q: How is the film secured at start and finish? A: The wrap program applies reinforced loops at each end to lock the loose ends, and an integrated cutter separates the finished bundle from the film.
Q: What bundle sizes does the standard line take? A: Single profiles range from 10 x 10 mm to 150 x 150 mm in section, and total line length covers 1 to 12 m sections. The bundle that can pass the ring is set by the ring opening; both are confirmed per project.
Następny krok
- Email us at info@fhopepack.com with your longest section, bundle weights and daily volume.
- We send ring sizes, program list and a layout drawing within 48 hours.
- We arrange a site survey to confirm infeed and outfeed conveyor length for your line.
Powiązane czytanie
- Pozioma orbitalna owijarka stretch do profili aluminiowych
- Półautomatyczna maszyna do owijania profili aluminiowych folią stretch
- Aluminum profile stretch wrapping and packing machine
- Linie produktów maszyn pakujących FHOPE
Źródła i standardy
- ISO 12100:2010 — Bezpieczeństwo maszyn. Ogólne zasady projektowania, oceny ryzyka i ograniczania ryzyka
- EN 415-10:2014 — Bezpieczeństwo maszyn pakujących. Wymagania ogólne
- EN ISO 13849-1:2023 — Bezpieczeństwo maszyn. Elementy systemów sterowania związane z bezpieczeństwem
- FHOPE aluminum profile packing line demonstration video. Reviewed as a general demonstration; line length and program set confirmed per project.
Ostatnia aktualizacja: 2026-10-10