Samenvatting
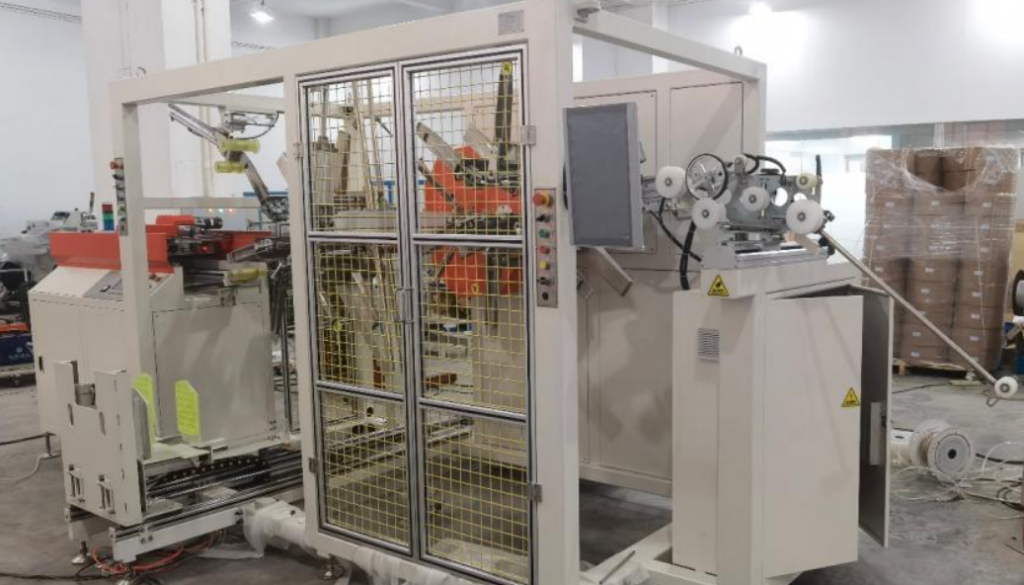
A brick stack is dense, sharp-edged and often shipped without a wooden pallet. Our automatic pallet strapping machine for brick puts the stack under a powered arch, straps it in one direction, turns it on a turntable conveyor and straps it again across, so every course is locked before the forklift lifts it.
The stack arrives on a roller conveyor and stops under a red steel arch. The strap head drives a green PET strap round the arch, tensions it over the top course and seals it. A turntable section under the stack then turns it 90° so the next straps cross the first ones.
Inhoudsopgave
- Why brick is strapped, not only wrapped
- Strapping sequence
- Machinegegevens
- Stacks with fork pockets
- Turning the stack: clearance check
- Strap choice for brick
- Cyclustijd
- Selectie checklist
- Veiligheid
- Veelgestelde vragen over techniek
- Volgende stap
- Gerelateerd lezen
- Bronnen
Why brick is strapped, not only wrapped
Brick is heavy for its size and its edges cut film. Strap carries the load in tension around the whole stack, so the courses cannot slide apart when the forklift tilts or the truck brakes. Film can be added afterwards against rain and dust, but the strap is what holds the stack together.
Strapping sequence
- The stack runs in on the roller conveyor and stops under the arch.
- The strap head feeds strap round the arch track and pulls it back onto the stack.
- The strap is tensioned over the top course and friction-welded.
- The conveyor indexes the stack to the next strap position and the cycle repeats.
- The turntable section turns the stack 90° and the cross straps are applied.
- The strapped stack runs out to the forklift pick-up point.
Machinegegevens
| Item | Waarde |
|---|---|
| Boogopening | up to 1,300 mm wide, 1,800 mm high |
| Strap time | about 15 s per strap |
| Riem | 12–16 mm or 19 mm PET or PP |
| Afdichting | wrijvingslas |
| Transporthoogte | 300–600 mm, verstelbaar |
| Load weight and tension range | bevestigd bij offerte |
Stacks with fork pockets
Many brick plants ship without wooden pallets. The bottom courses are set with two open channels so the forks enter the stack directly. The straps must then pass over solid brick, not over the channels, or they will pull the edge bricks into the gap. Strap positions are set in the program against the stack pattern.
Turning the stack: clearance check
The stack needs room to turn. Its plan diagonal is √(L² + W²). A 1,000 × 1,000 mm stack has a diagonal of about 1,414 mm, more than the 1,300 mm arch width, so it is turned clear of the arch posts and then run back in. The turntable position is laid out for your stack size, confirmed at quote.
Strap choice for brick
PET strap holds its tension under a dense load and resists the abrasion of fired brick edges, so it is the usual choice for export. PP strap costs less but relaxes under load, which suits short handling inside the plant. Corner protectors stop the strap cutting into the top edge bricks.
Cyclustijd
Cycle per stack ≈ (straps × 15 s) + (index moves × index time) + turn time + in-feed and out-feed time.
Each index move runs the stack to the next strap position; index and turn times depend on stack weight and conveyor speed, confirmed at quote.
Example only: 2 straps each way is 4 × 15 = 60 s of strapping. With the turn and transfers added, check the total against the kiln or packing line output in stacks per hour.
Selectie checklist
- Stapellengte, -breedte en -hoogte.
- Stapelgewicht.
- With or without wooden pallet or fork pockets.
- Straps per direction and strap width.
- PET or PP strap.
- Stapels per uur.
Veiligheid
We design to EN ISO 12100:2010 for risk assessment, EN 415-8 for strapping machines, EN 415-10 for the integrated conveyors and turntable and EN 60204-1 for the electrical equipment. The strap path and turntable are guarded, and the cell has interlocked access and an emergency stop.
Veelgestelde vragen over techniek
Q: Why turn the stack? A: So the cross straps lock the courses in both directions.
Q: Which strap is best for brick? A: PET for export and long storage; PP for short in-plant handling.
Q: How long is one strap? A: About 15 s per strap.
Q: Can it strap stacks without a pallet? A: Yes. Strap positions are set to miss the fork channels.
Volgende stap
- Send your stack sizes, weight and stacks per hour naar info@fhopepack.com.
- We gaan zitten the strap pattern, turntable and conveyor layout.
- We reageren binnen 24 uur met een voorstel en een offerte.
Gerelateerd lezen
- Vertical pallet strapping machine (product)
- Automatische palletomsnoeringsmachine
- Auto pallet strapping machine packaging machine
- Automatische palletverpakkingslijn en omsnoeringsmachine
- Volautomatische lijn voor palletwikkelmachines
Bronnen
- FHOPE product page: vertical pallet strapping machine
- EN ISO 12100:2010; EN 415-8; EN 415-10; EN 60204-1
Laatst beoordeeld: 20-10-2026